SZTUKA
Piękno i dobre samopoczucie
RZEMIOSŁO
KULTURA I HISTORIA
ROZRYWKA
ŚRODOWISKO
JEDZENIE I NAPOJE
INŻYNIERIA ODWROTNA
NAUKI
LEKKOATLETYKA
TECHNOLOGIA
URZĄDZENIA DO NOSZENIA
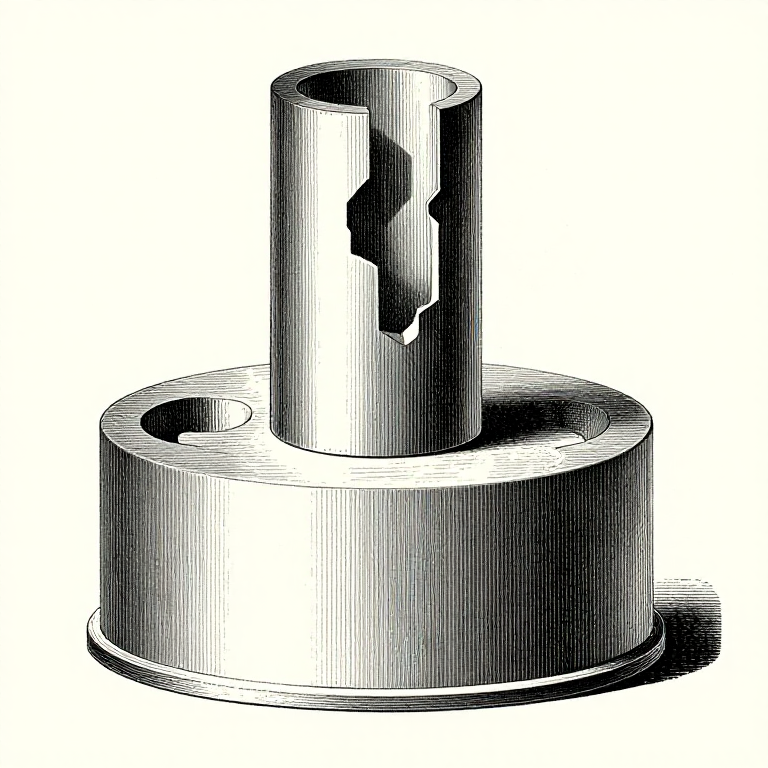


Risers: Metal Shrinks When It Freezes, and the Hole Goes Somewhere
Almost every metal occupies less space solid than liquid. Bronze loses about 5% of its volume on freezing, steel about 3%, aluminium about 6% — and that volume has to come from somewhere.
If there is no reservoir feeding the casting, it comes out of the casting itself: a cavity, usually in the last place to freeze, usually inside a thick section where it cannot be seen until the part is machined or breaks.
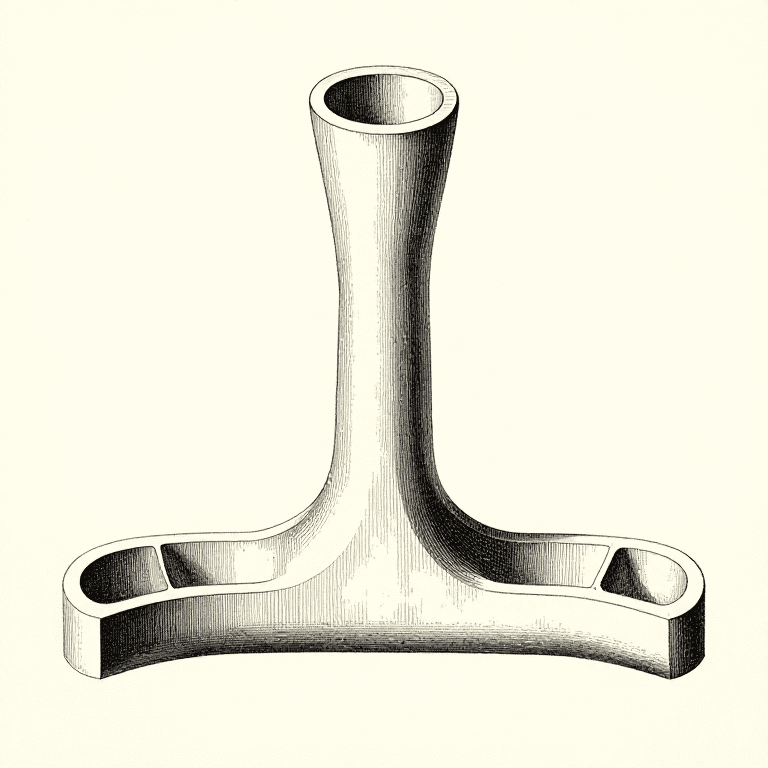
A RISER is that reservoir. It is a lump of extra metal, connected to the casting, designed to stay liquid LONGER than the part it feeds — so when the casting contracts, the hole forms in the riser and the riser is cut off and remelted.
Zaawansowany
3 hours
Instrukcje
1
1
The riser must freeze last, which means it must be chunkier
The riser must freeze last, which means it must be chunkier
Wczytywanie notatnika Jupyter…
Materiały do tego kroku:
 Sztabka brązu1 sztuka
 Piasek formierski1 kg
Potrzebne narzędzia:
 Komputer stacjonarny
 Suwmiarka cyfrowa 6 cali
 Skrzynka formierska (górna i dolna)
2
2
Feed from the top, and keep the path open
Feed from the top, and keep the path open
Gravity does the feeding, so a riser feeds downward and sideways over a limited distance — roughly four times the section thickness along a plate, and less in alloys that freeze over a wide temperature range.
The connection between riser and casting — the riser NECK — must stay liquid until the casting has finished shrinking. A long thin neck freezes first and cuts the riser off from the part it was supposed to feed.
So the neck is short and generous, and the riser sits directly on or beside the heavy section. A riser placed at the end of a thin plate in the hope of feeding a boss at the other end feeds nothing at all.
Materiały do tego kroku:
Piasek formierski1 kgSztabka brązu1 sztukaPotrzebne narzędzia:
Skrzynka formierska (górna i dolna)Suwmiarka cyfrowa 6 cali3
3
Open risers, blind risers, and atmospheric pressure
Open risers, blind risers, and atmospheric pressure
An OPEN riser reaches the top of the mould, so air can push down on the metal as it feeds. It also lets you see when the mould is full and top it up at the end of the pour, which is genuinely useful.
A BLIND riser is enclosed in the sand. It stays hotter because it has no exposed surface, but as the metal drains out it needs air to replace it — otherwise a vacuum forms and stops the feeding.
That is what a WHISTLER or a permeable core in the riser top is for: a small passage that lets atmospheric pressure into the riser cavity. It is a small detail that makes the difference between a blind riser working and doing nothing at all.
Materiały do tego kroku:
Piasek formierski1 kgPotrzebne narzędzia:
Skrzynka formierska (górna i dolna) Linijka
 Lupa zegarmistrzowska
4
4
Budget the metal, including everything you cut off
Budget the metal, including everything you cut off
The gating and risers can easily weigh as much as the casting. That metal is not wasted — it is cut off and remelted — but it must be MELTED, and running out mid-pour ruins the casting and the mould together.
Weigh the pattern, multiply by the ratio of alloy density to pattern-material density, and add the gating and riser volumes. Then add a margin, because a crucible is never poured completely empty.
Write the actual numbers down after the pour: what went in, what came out as casting, what came off as gating. After a few pours those figures let you predict a melt accurately, which is the difference between a foundry that works and one that improvises.
Materiały do tego kroku:
Sztabka brązu1 sztuka Wlewek aluminiowy 99,7 % czystości, 450 g1 sztuka
Potrzebne narzędzia:
 Waga precyzyjna
 Tygiel
Materiały
3- 1 sztukaZastępnik
- Zastępnik
- Zastępnik
Powiązane blueprinty
Te blueprinty dzielą się wiedzą — technikami, materiałami lub zasadami



CC0 Domena publiczna
Ten plan jest udostępniany na licencji CC0. Możesz go swobodnie kopiować, modyfikować, rozpowszechniać i wykorzystywać do dowolnych celów, bez konieczności uzyskiwania zgody.
Wesprzyj Makera kupując produkty przez jego plan, za co zarabia Prowizja Makera ustalony przez sprzedawców, lub stwórz nową iterację tego planu i dołącz go jako połączenie w swoim własnym planie, aby dzielić się przychodami.