SZTUKA
Piękno i dobre samopoczucie
RZEMIOSŁO
KULTURA I HISTORIA
ROZRYWKA
ŚRODOWISKO
JEDZENIE I NAPOJE
INŻYNIERIA ODWROTNA
NAUKI
LEKKOATLETYKA
TECHNOLOGIA
URZĄDZENIA DO NOSZENIA

When a Tap Breaks: Getting It Out, and Not Doing It Again
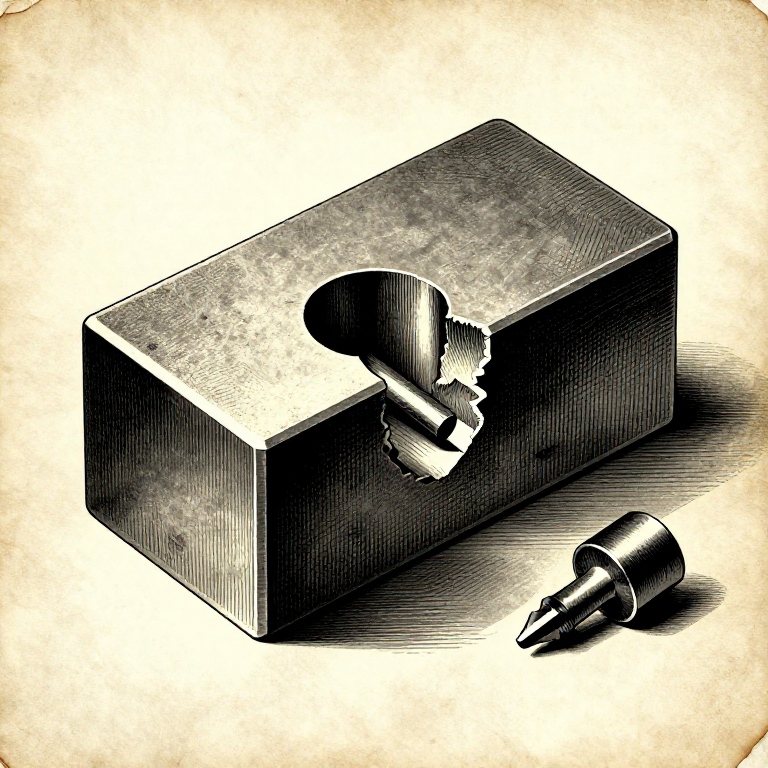
A tap is glass-hard and completely brittle. It does not bend before it breaks, it gives no warning, and when it goes it leaves a piece of the hardest steel in the workshop jammed inside the part you have spent hours making.
A drill will not touch it, because the tap is harder than the drill. That is the whole difficulty, and it is why the honest answer to most broken taps is that the hole, and sometimes the part, is lost.
So this rung is two-thirds prevention. The removal methods are real and worth knowing, but every one of them is slower and less certain than the five seconds of care that would have avoided it.
Zaawansowany
3 hours
Instrukcje
1
1
The five causes, in order of how often they do it
The five causes, in order of how often they do it
One: the tapping drill was too small, so the tap is being asked to cut far more metal than it was designed to. Two: the chip was never broken — no quarter-turn back — so it packed solid. Three: a blind hole bottomed out. Four: the tap was started crooked and then forced. Five: sideways pressure, usually from a spanner on the square instead of a tap wrench.
Every one of those is a decision made before the break, and four of them are made before the tap even enters the hole.
The small sizes break most. An M3 tap will snap under a force you would not notice applying, and below M4 the sensible approach is a tapping stand or a pillar drill used as a guide by hand, never a wrench swung freely.
Potrzebne narzędzia:
 Zestaw do gwintowania
 Pokrętło do gwintowników
 Zestaw wierteł
2
2
If it is proud of the surface, you are in luck
If it is proud of the surface, you are in luck
A tap broken off above the work can often be gripped and wound out. Lock a pair of grips or a small pin vice onto the stub and turn it gently backwards — gently, because what is left in the hole is even easier to break again.
Flood the hole with penetrating oil first and leave it. The tap is jammed by packed chips more often than by the thread itself, and oil plus time does real work here.
If it will not turn backwards, try rocking it: a few degrees back, a few forward, gradually increasing. This breaks the chips loose the way the quarter-turn should have done, and it recovers far more taps than brute force does.
Materiały do tego kroku:
 Olej do cięcia1 sztuka
Potrzebne narzędzia:
 Ciężkie imadło warsztatowe
 Tkanina bawełniana
 Okulary ochronne bezbarwne
3
3
If it is flush or below — the methods, and their honest odds
If it is flush or below — the methods, and their honest odds
A TAP EXTRACTOR has fingers that slide down the tap's flutes and grip from inside. It works well on a clean break in a larger tap and poorly on a shattered small one — and its own fingers break.
SHATTERING works on hardened steel because it is brittle: a sharp centre punch and light taps can break the tap into pieces that pick out. It is genuinely effective and it can also crack the workpiece, so it is a decision, not a default.
ALUM SOLUTION dissolves hardened carbon steel and leaves aluminium and most workpiece metals alone. Hot saturated alum, several hours to a day, and the tap is gone. It is slow and completely non-destructive, which makes it the right answer for a valuable part — and the wrong answer for an HSS tap, which it barely touches. EDM will remove any tap from any part, and it means paying a specialist.
Potrzebne narzędzia:
 Punktak
 MłotekOkulary ochronne bezbarwne
 Lupa zegarmistrzowska
4
4
Save the part instead of the hole
Save the part instead of the hole
When the tap will not come out, stop trying to save that hole and start thinking about the part. Drill the hole out to a larger size on the same centre — if you can get past the tap — and fit a threaded insert or a larger fastener.
Often the better answer is to abandon that hole entirely and put a new one a short distance away, or to fill it and re-drill. A part with an extra hole in it usually still works; a part destroyed by three hours of increasingly violent extraction does not.
Decide early. The damage in these situations is nearly always done in the attempt to fix the first mistake, not by the first mistake — and the same is true of most things in a workshop.
Materiały do tego kroku:
 Blacha gruba ze stali niskowęglowej1 sztuka
Potrzebne narzędzia:
Zestaw wiertełZestaw do gwintowaniaPokrętło do gwintownikówMateriały
2- 1 sztukaZastępnik
- Zastępnik
Wymagane narzędzia
9- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
- Zastępnik
Powiązane blueprinty
Te blueprinty dzielą się wiedzą — technikami, materiałami lub zasadami

CC0 Domena publiczna
Ten plan jest udostępniany na licencji CC0. Możesz go swobodnie kopiować, modyfikować, rozpowszechniać i wykorzystywać do dowolnych celów, bez konieczności uzyskiwania zgody.
Wesprzyj Makera kupując produkty przez jego plan, za co zarabia Prowizja Makera ustalony przez sprzedawców, lub stwórz nową iterację tego planu i dołącz go jako połączenie w swoim własnym planie, aby dzielić się przychodami.