ИСКУССТВО
КРАСОТА И ЗДОРОВЬЕ
РЕМЕСЛО
КУЛЬТУРА И ИСТОРИЯ
РАЗВЛЕЧЕНИЯ
ЭКОЛОГИЯ
ЕДА И НАПИТКИ
ОБРАТНАЯ ИНЖЕНЕРИЯ
НАУКИ
СПОРТ
ТЕХНОЛОГИИ
НОСИМЫЕ УСТРОЙСТВА

Pouring Temperature: Too Cold Misruns, Too Hot Tears the Mould
Metal is not poured at its melting point. It is poured at a SUPERHEAT above it — enough that it can travel through the gating and fill the last thin corner before it starts to freeze.
Too little superheat and the metal stops before the cavity is full, or two streams meet and fail to fuse. Too much and it dissolves more gas, oxidises harder, burns the sand, and shrinks more on the way down — so the porosity gets worse rather than better.
The window is perhaps 100 to 150 degrees wide, it differs by alloy and by casting, and the only way to sit inside it reliably is to MEASURE. Judging melt temperature by colour is the pyrometer rung's warning delivered with molten metal.
Продвинутый
3 hours
Инструкции
1
1
Superheat, by alloy
Superheat, by alloy
Загрузка блокнота Jupyter…
Материалы для этого шага:
 Бронзовый слиток1 штука
 Алюминиевый слиток 99,7 % чистоты, 450 г1 штука
Необходимые инструменты:
 Пирометр
 Термопара с индикатором
 Настольный компьютер
2
2
Skim, and do not stir the dross back in
Skim, and do not stir the dross back in
Oxide and impurities float. Skim them off the surface of the melt immediately before pouring, with a preheated skimmer, and take them right out of the crucible rather than pushing them aside.
Preheat every tool that will touch molten metal. A cold skimmer or ladle chills the metal locally and, far worse, any trace of moisture on it flashes to steam instantly — which throws metal.
Do not stir after skimming. Stirring folds the remaining surface oxide down into the melt, where it becomes inclusions in the casting. Aluminium is the worst for this: its oxide skin is tough, and every disturbance of the surface makes more of it.
Материалы для этого шага:
Бронзовый слиток1 штукаНеобходимые инструменты:
 Шумовка с мелкой сеткой
 Литейный ковш
 Щипцы для тигля
 Кожаные краги
3
3
Dry everything, and mean it
Dry everything, and mean it
Water and molten metal is the one genuinely dangerous combination in a foundry. Water turned to steam expands roughly 1,600 times, instantly, and if it is under metal it throws that metal outward.
So: preheat and dry the crucible, the tongs, the ladle and every ingot before it goes near the melt. An ingot with condensation on it, or a scrap casting with water trapped in a cavity, is the classic cause.
The mould matters too. Green sand contains water by design and that is fine because it is bound in the clay and the mould is permeable — but a sand that is too wet, or a mould left standing so condensation collects, is the same hazard in a different place.
Материалы для этого шага:
Бронзовый слиток1 штука Древесный уголь кусковой1 штука
Необходимые инструменты:
 ТигельЩипцы для тигля
 Затемнённые очки для горнаКожаные краги
4
4
Everything ready before the metal is
Everything ready before the metal is
Once the metal is at temperature it is losing heat and gaining gas every second. The moulds must be closed, weighted, vented and positioned before the crucible comes out of the furnace.
Weight or clamp the cope. Molten metal exerts real upward pressure on the top half of the mould, and an unweighted cope lifts and lets metal run out of the parting line — which is dangerous as well as a lost casting.
Have a clear path, a clear floor, and somewhere planned to put the crucible down. The pour itself takes a few seconds; everything that makes it go well or badly was decided in the minutes before it.
Материалы для этого шага:
 Формовочный песок1 кг
Необходимые инструменты:
 Литейная опока (верхняя и нижняя)Щипцы для тигляЗатемнённые очки для горнаКожаные краги
Материалы
4- 1 штукаЗаполнитель
- Заполнитель
- 1 штукаЗаполнитель
- Заполнитель
Требуемые инструменты
10- Заполнитель
- Заполнитель
- Заполнитель
- Заполнитель
- Заполнитель
- Заполнитель
- Заполнитель
- Заполнитель
- Заполнитель
- Заполнитель
Связанные чертежи
Эти чертежи делятся знаниями — техники, материалы или принципы
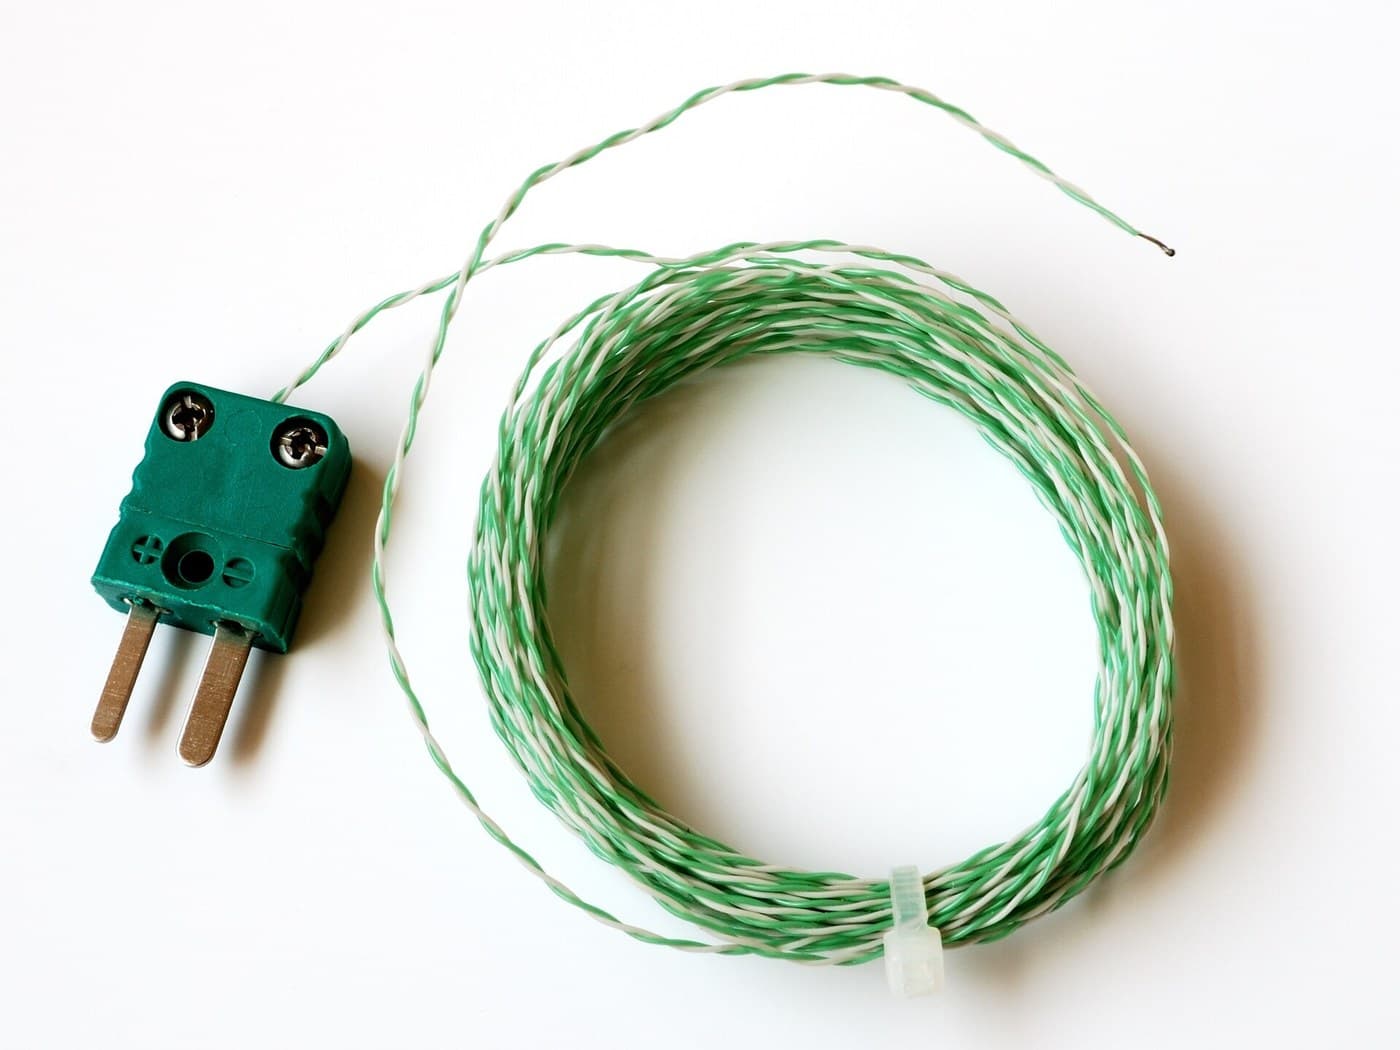
Measuring High Temperature: Thermocouples, Pyrometers, and What Each Lies About
от Penny
Металлообработка
23
0
0
0
0
0

Casting Iron in a Cupola Furnace — Re-Melting Pig Iron into Finished Castings
от Piett
Металлообработка
44
0
0
0
0
0

What Heat Costs: Scale, Grain Growth and Burnt Steel
от Forge
Металлообработка
20
0
0
0
0
0
CC0 Общественное достояние
Этот чертёж выпущен под лицензией CC0. Вы можете свободно копировать, изменять, распространять и использовать эту работу в любых целях без запроса разрешения.
Поддержите мейкера, покупая товары через его чертёж, где он получает Комиссию мейкера установленную продавцами, или создайте новую итерацию этого чертежа и включите его как связь в свой чертёж для распределения дохода.