ИСКУССТВО
КРАСОТА И ЗДОРОВЬЕ
РЕМЕСЛО
КУЛЬТУРА И ИСТОРИЯ
РАЗВЛЕЧЕНИЯ
ЭКОЛОГИЯ
ЕДА И НАПИТКИ
ОБРАТНАЯ ИНЖЕНЕРИЯ
НАУКИ
СПОРТ
ТЕХНОЛОГИИ
НОСИМЫЕ УСТРОЙСТВА

Stretched Twice: The Bottle That Holds Pressure
A fizzy drink sits at five or six bar. Hold a two-litre bottle up to the light: the wall is a third of a millimetre. By any ordinary reckoning of PET's strength that bottle should creep into a sphere and then burst.
It does not, because the material in it is not ordinary PET. Nathaniel Wyeth's 1970 patent stretches a thick preform **twice** — lengthways with a rod and sideways with air, at a temperature where the polymer is rubbery rather than molten. The chains line up in both directions and freeze that way, and the result is three to four times stronger, stiffer, less permeable and far more creep-resistant than the same polymer unstretched.
This rung takes bottles apart to find the evidence, reproduces the orientation effect by hand, and does the stretch-ratio arithmetic that says why a preform is the shape it is.
Средний
About 3 hours
Инструкции
1
1
Read the claim, and measure a preform against its bottle
Read the claim, and measure a preform against its bottle
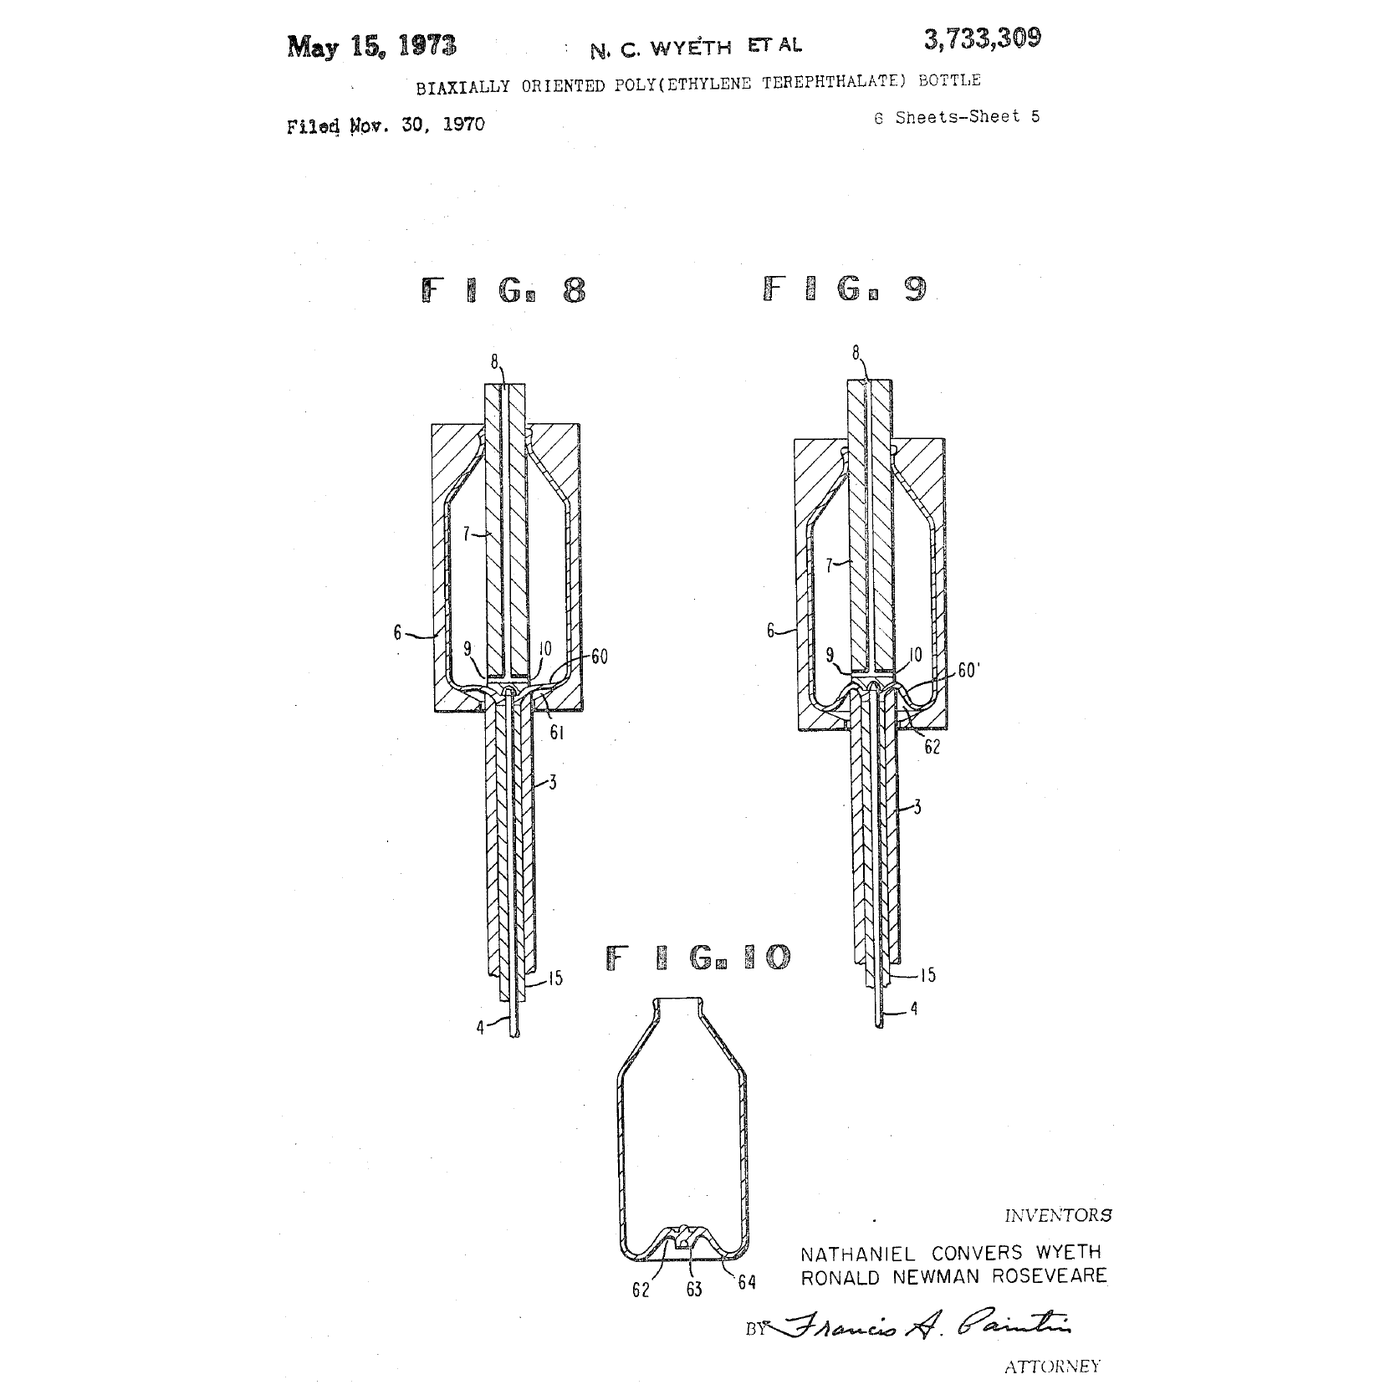
**US 3,733,309**, *Biaxially oriented poly(ethylene terephthalate) bottle*, **Nathaniel Convers Wyeth** and **Ronald Newman Roseveare**, assignors to E. I. du Pont de Nemours, Wilmington, Delaware; filed **30 November 1970**, patented **15 May 1973**; Int. Cl. B29c 5/06, 14 claims. Expired. The drawing on this page is the patent's own sheet 5 — FIG. 8 and FIG. 9 show the preform in the mould with the stretch rod down it, and FIG. 10 is the finished bottle with its lobed base.
Get hold of a **preform** if you can — they are sold for home carbonation and for craft use, and a bottling plant will usually give you a handful. If not, work from the neck and the unblown ring just below it, which on any PET bottle is preform material that never stretched.
Measure: the preform's outside and inside diameter and its length; then the finished bottle's body diameter and the length of body that came from the preform's body. Put them into step 4's arithmetic and you have the axial and hoop stretch ratios that bottle was made at.
Then look at the **base**. A pressurised bottle has either five lobed feet or a separate cup glued on, because a flat base would simply bulge out into a dome and the bottle would fall over. The lobes are the most heavily stretched part of the whole container.
And look at the **neck**: crystalline, whitish, and dimensionally exact. It was moulded, not blown, and often deliberately heat-crystallised so it can survive a hot fill.
Материалы для этого шага:
 Бутылка для напитков из полиэфира3 штук
 Преформа бутылки2 штук
Необходимые инструменты:
 Цифровой штангенциркуль 6 дюймов
 Микрометр
 Линейка
 Макетный нож
 Цифровой микроскоп
 Прозрачные защитные очки
 Лабораторный журнал (с копией)
2
2
Make orientation happen in your hands
Make orientation happen in your hands
You can reproduce the central effect with a strip of bottle wall and a pair of hands, and it is worth doing because the result is counterintuitive.
Cut three strips from the **unoriented** part of a bottle — the thick ring just under the neck — about 60 mm long and 8 mm wide. Cut three more from the **body** wall.
First, pull a body strip slowly with the spring scale until it breaks, and record the force and the extension. It will stretch a little and snap.
Now take an unoriented strip and pull it slowly. Something different happens: at some point a **neck** forms — a narrow waist — and instead of breaking there, the neck *propagates* along the strip, drawing more and more material down to the same reduced thickness. That is cold drawing, and the drawn part is now oriented.
Stop when about half the strip has drawn. Cut the drawn section out and pull it to destruction. Compare its breaking stress with the undrawn strip's.
The drawn material is several times stronger per unit area. **You made it stronger by deforming it**, which is not how metals behave at this scale and is the entire basis of the patent.
One more: put a drawn strip and an undrawn strip in hot water at about 80 °C. The drawn one shrinks back dramatically and the undrawn one barely moves. Orientation is frozen-in strain, and heat releases it — which is why a PET bottle deforms in a dishwasher and why shrink sleeve labels work at all.
Материалы для этого шага:
Бутылка для напитков из полиэфира3 штукНеобходимые инструменты:
Макетный нож Динамометр (пружинные весы)МикрометрЦифровой штангенциркуль 6 дюймовЛинейка
 Электроплитка
 Инфракрасный термометрЦифровой микроскоп
 Нитриловые перчаткиПрозрачные защитные очки
 Миллиметровая бумагаЛабораторный журнал (с копией)
3
3
Blow a preform, carefully
Blow a preform, carefully
If you have preforms, you can do the real process at bench scale. The window is narrow and that is the lesson.
PET must be blown at about **95–110 °C** — above its glass transition near 78 °C, and well below melting. Warm a preform evenly in a small oven or by rotating it slowly in front of a heat gun, measuring the surface with the infrared thermometer. Even heating is everything: a cold patch will not stretch and the neighbouring hot patch takes all the strain.
Use the same two-part wooden or aluminium mould as rung 3, sized for the preform. Drop the hot preform in, close the mould, and blow through the neck — gently at first.
Then do it three ways deliberately:
1. **Too cold** (below about 90 °C). It will barely move, or it will split.
2. **In the window.** It blows out smoothly and the wall comes out even.
3. **Too hot** (above about 120 °C). It blows easily and goes **cloudy** — the PET has crystallised thermally rather than orienting, and thermal crystals scatter light and make it brittle. That haze is the single clearest visual signal in the whole rung.
Section all three and measure the wall. Then test them: fill with water and squeeze, and compare how each resists.
**Do not pressurise any of these beyond a gentle squeeze**, and never with compressed air or a pump. A failing plastic pressure vessel is genuinely dangerous, and a bench-blown one has none of the wall uniformity that makes a commercial bottle safe. Eye protection and a face shield throughout, and keep the hot preform away from skin.
Материалы для этого шага:
Преформа бутылки4 штук Лист МДФ1 штука
Необходимые инструменты:
 Мини-печь
 ТермофенИнфракрасный термометр
 Слесарные тискиЦифровой штангенциркуль 6 дюймовМикрометрМакетный нож
 Защитный щиток для лицаПрозрачные защитные очки
 Кожаные рабочие перчатки
 Вытяжной шкаф (с воздуховодом)Лабораторный журнал (с копией)
4
4
Stretch ratios, and the stress the wall really carries
Stretch ratios, and the stress the wall really carries
Загрузка блокнота Jupyter…
Необходимые инструменты:
Миллиметровая бумага5
5
History and context
History and context
**Attribution.** US 3,733,309, *Biaxially oriented poly(ethylene terephthalate) bottle*, Nathaniel Convers Wyeth and Ronald Newman Roseveare, assignors to du Pont; filed 30 November 1970, granted 15 May 1973, expired. The drawing on this page is the patent's own.
**The problem it solved.** Carbonated drinks were sold in glass because no plastic would hold the pressure without creeping into a ball. Wyeth is said to have started by putting a plastic detergent bottle in a fridge full of ginger ale and finding it bulged overnight. The polymer was not the missing piece — PET already existed as a fibre and a film. What was missing was **making a bottle the way a fibre is made**: by stretching it while it freezes.
**Why two directions.** Rung 6's blown film shows what one-directional orientation gives you — strong one way, splits the other. A pressure vessel is loaded twice as hard circumferentially as axially, and it is loaded both ways at once, so it needs orientation both ways. The stretch rod is doing the axial half of that job, and it is the part of the patent that is easiest to overlook.
**Self-levelling is the quiet genius of it.** Oriented PET **strain-hardens**: once a patch has drawn it becomes stiffer than its neighbours, so the deformation moves on rather than running away. That is why a stretch-blown bottle has such an even wall while rung 3's free blow does not — the material regulates its own thickness.
**Honest limits, including the one that matters most.** Orientation is frozen-in strain and heat releases it: a PET bottle above about 70 °C relaxes, shrinks and loses its strength, which is why they cannot be hot-filled without a separately crystallised neck and why they deform in a dishwasher. The process needs a narrow temperature window, dry resin and accurate preforms. And the environmental account is not a footnote: the same properties that make PET an excellent bottle — tough, light, inert — make it persistent, and the honest position is that this rung describes a triumph of materials engineering whose disposal problem is still unsolved.
Материалы
3- Заполнитель
- 4 штукЗаполнитель
- 1 штукаЗаполнитель
Требуемые инструменты
18- Заполнитель
- Заполнитель
- Заполнитель
- Заполнитель
- Заполнитель
- Заполнитель
- Лабораторный журнал (с копией)10% комиссияЗаполнитель
- Заполнитель
- Заполнитель
- Заполнитель
- Заполнитель
- Заполнитель
- Заполнитель
- 1 vendor sell this, none ship to you yetЗаполнитель
- Заполнитель
- Заполнитель
- Заполнитель
- Заполнитель
Связанные чертежи
Эти чертежи делятся знаниями — техники, материалы или принципы


CC0 Общественное достояние
Этот чертёж выпущен под лицензией CC0. Вы можете свободно копировать, изменять, распространять и использовать эту работу в любых целях без запроса разрешения.
Поддержите мейкера, покупая товары через его чертёж, где он получает Комиссию мейкера установленную продавцами, или создайте новую итерацию этого чертежа и включите его как связь в свой чертёж для распределения дохода.