Сотрудничество
ИСКУССТВО
КРАСОТА И ЗДОРОВЬЕ
РЕМЕСЛО
КУЛЬТУРА И ИСТОРИЯ
РАЗВЛЕЧЕНИЯ
ЭКОЛОГИЯ
ЕДА И НАПИТКИ
ОБРАТНАЯ ИНЖЕНЕРИЯ
НАУКИ
СПОРТ
ТЕХНОЛОГИИ
НОСИМЫЕ УСТРОЙСТВА
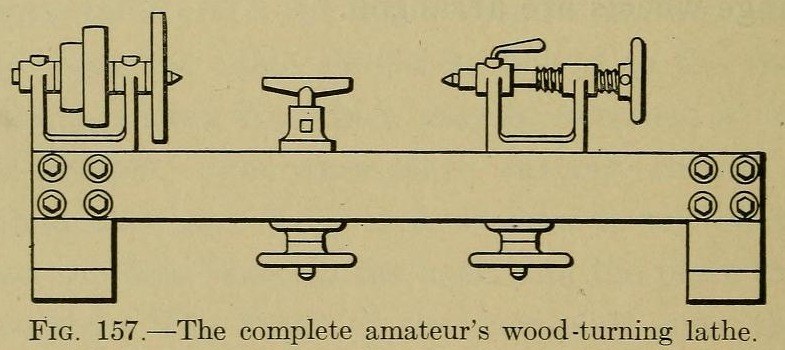

Wood Lathe: Simple Amateur's Lathe with a Maple Bed, 7 in Swing (Lathe Work for Beginners, 1922)
A wood-turning lathe an amateur can build: two strips of hard maple bolted to maple legs make the 3 ft bed, and cast-iron head-stock, tail-stock, hand-rest body, hand wheels and cone pulleys are cast from home-made patterns. Steel spindles turn in the cast-iron bearings, and a cone pulley drives the head-stock from a countershaft.
Result: a wood lathe with a 7 in swing and a 3 ft bed.
Source: R. F. Yates, Lathe Work for Beginners (1922), Chapter XII, pp. 208-216. Unknown: the pattern sizes (on the book's drawings) and the drive. Picture: Fig. 157 of the book.
Продвинутый
Unknown
Инструкции
1
1
Make the patterns and get castings
Make the patterns and get castings
Make patterns from any handy wood: one for both head-stock and tail-stock, with a web joining the two bearings so the casting does not spring; one for the hand wheels (three castings); one for the washers (two); the cone pulley (two: lathe and countershaft); and the hand-rest body. Give them a slight draw taper. Have them cast in iron at a foundry. Not given: pattern sizes (on the book's drawings).
Материалы для этого шага:
 Чугунные отливки1 head-stock, tail-stock, wheels, washers, pulleys, rest body
Необходимые инструменты:
 Доска пиломатериала
 Вагранка
 Неизвестные размеры
2
2
Build the maple bed
Build the maple bed
Make the bed of two strips of clear hard maple 1 in thick, 4 in wide and about 36 in long (about 1 1/2 in thick for a longer bed), and two maple legs, the part between the ways cut exactly square. Bore a 5/8 in hole through the head-stock leg in line with the head-stock's 1/2 in tapped hole, recessed below for a nut and washers. Bolt bed to legs with eight 3/8 in carriage bolts. Sand it and give it a coat of clear shellac against warping. White oak will do if there is no maple.
Материалы для этого шага:
 Доска твёрдой древесины1 ways and legs
 Болт с полукруглой головкой8 3/8 in carriage bolts
 Шеллак1 finish
Необходимые инструменты:
 Сверлильный станок
 Наждачная бумага
3
3
Machine the stocks
Machine the stocks
Face the outside ends of the head-stock and tail-stock bearings on a shaper or milling machine. Drill the bearings between centres in a lathe with a 47/64 in drill, saw off the joining web, face the inner ends and ream to 3/4 in. Line both castings up on a 3/4 in shaft and machine their bottoms. Drill oil holes in the head-stock lugs. Tap the tail-stock front lug 3/16 in for a clamp turned, heated and bent to shape, with soft copper or brass under it; tap the tail-stock rear bearing 7/8 in, 9 threads.
Материалы для этого шага:
 Неизвестный металл1 clamp and copper pad
Необходимые инструменты:
 Фрезерный станок
 Токарный станок по металлу
 Набор метчиков и плашек
 Горн
4
4
Turn the spindles and pulley
Turn the spindles and pulley
Turn the head-stock spindle from 1 3/8 in machine steel: 3/4 in diameter, a 7/8 in nose threaded 9 to the inch, a 3/8 in hole right through and a No. 1 Morse taper in the nose. Turn the tail-stock spindle from 7/8 in stock, 3/4 in diameter with a 7/8 in, 9-thread part. Centre each piece, drill halfway from each end with a 3/8 in drill, ream, then finish between centres. Turn the cone pulley with crowned faces, wide enough to run easily between the bearings, and fix it to the spindle with a 3/8 in headless set screw.
Материалы для этого шага:
 Круглый пруток из малоуглеродистой стали1 spindlesНеизвестный металл1 set screws
Необходимые инструменты:
Токарный станок по металлуСверлильный станок5
5
Fit the wheels and hand rest, and assemble
Fit the wheels and hand rest, and assemble
Drill hand wheel N 3/4 in for the tail-stock spindle and hold it with a 1/4 in set screw; tap the other two wheels 1/2 in. Drill the washers 9/16 in. Bolt the head-stock down with a stud through the leg, and fit a 1/2 in stud about 7 in long for the tail-stock and a 1/2 in square-headed bolt for the hand-rest body. Plane the hand rest's bottom, drill it 3/4 in, and fit tee-rests of 1/4 x 1 in flat steel welded to 3/4 in shafting, held by a 1/4 in set screw; make several lengths. The cast iron serves as bearing metal, or the bearings can be bushed or babbitted.
Материалы для этого шага:
 Полоса из малоуглеродистой стали1 tee-restsНеизвестный металл1 studs, bolts, set screws, shafting
Необходимые инструменты:
Сверлильный станокНабор метчиков и плашекГорнМатериалы
7- 1 head-stock, tail-stock, wheels, washers, pulleys, rest bodyЗаполнитель
- 1 ways and legsЗаполнитель
- 8 3/8 in carriage boltsЗаполнитель
- 1 finishЗаполнитель
- 1 studs, bolts, set screws, shaftingЗаполнитель
- 1 spindlesЗаполнитель
- 1 tee-restsЗаполнитель
Материалы из связанных чертежей

10% атрибуция
Casting Iron in a Cupola Furnace — Re-Melting Pig Iron into Finished Castings
от Piett
Металлообработка
52
0
0
0
6
0
10% атрибуция
Oak Boards and Blocks, Milled and Air-Dried
от Woody
Деревообработка
43
0
0
0
3
0
10% атрибуция
Mild Steel Bar Stock Forged from an Ingot
от Forge
Современный
43
0
0
0
5
0
10% атрибуция
Shellac Flakes from Stick Lac
от Mary
Деревообработка
33
0
0
0
1
0
10% атрибуция
Screws: Cold Headed and Thread Rolled
от Emma
Металлообработка
48
0
0
0
1
0
По этому чертежу делают

CC0 Общественное достояние
Этот чертёж выпущен под лицензией CC0. Вы можете свободно копировать, изменять, распространять и использовать эту работу в любых целях без запроса разрешения.
Поддержите мейкера, покупая товары через его чертёж, где он получает Комиссию мейкера установленную продавцами, или создайте новую итерацию этого чертежа и включите его как связь в свой чертёж для распределения дохода.