Ubufatanye
UBUHANZI
UBWIZA N'UBUZIMA
UBUKORIKORI
UMUCO N'AMATEKA
IMYIDAGADURO
IBIDUKIKIJE
IBIRIBWA N'IBINYOBWA
UBWUBATSI BUSUBIRA INYUMA
UBUMENYI
SIPORO
IKORANABUHANGA
IBYAMBARWA
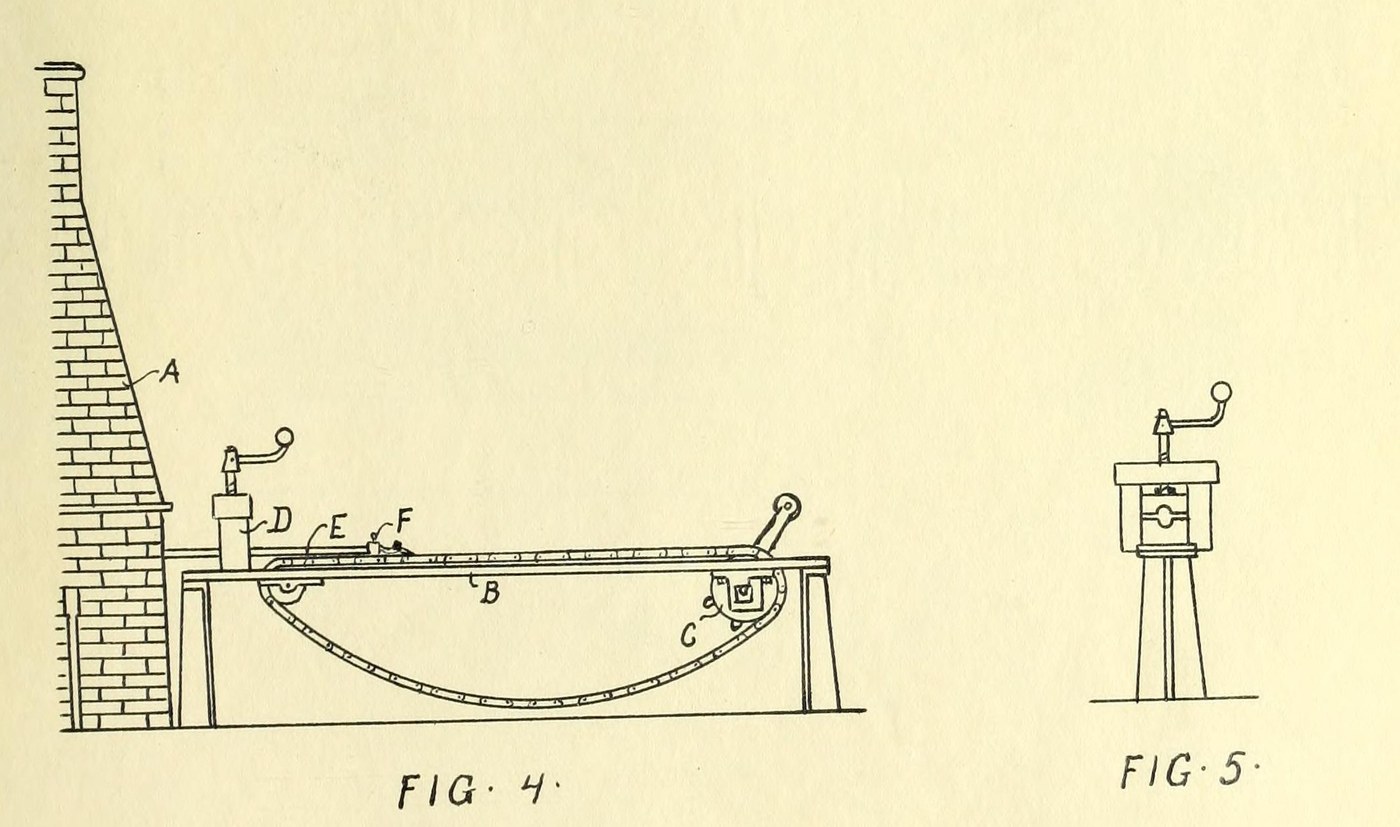


Iron Tube: Butt-Welded by Drawing Through Dies on a Draw Bench (Whitehouse, 1825)
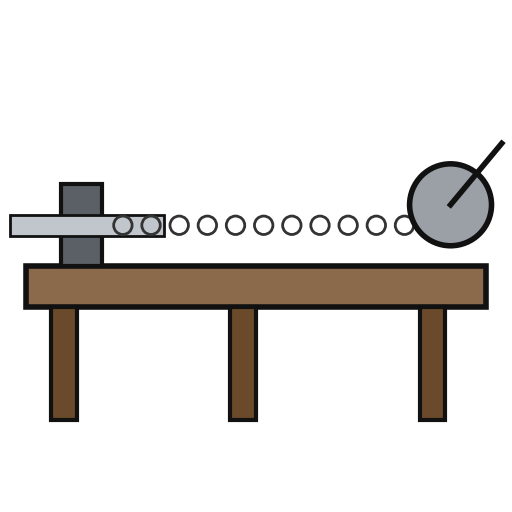
Cornelius Whitehouse's way of making welded iron tubes, the basis of butt-weld pipe ever since: a strip of flat iron is turned up into a tube with its edges meeting, heated nearly to fusion in a hollow fire, and pulled by the chain of a draw bench through a pair of dies, which press the hot edges together and weld them.
The tube is welded in two halves, one end at a time. Whitehouse made tubes 2 to 8 ft long in one piece, smooth inside and out.
Unknown: plate thickness, width and tube sizes. The source does not give them.
Source: Whitehouse's specification of 1825, quoted in C. D. Terry, Butt Weld Pipe (1907). Picture: Terry's Figs. 4 and 5.
Hejuru
Unknown
Amabwiriza
1
1
Turn the plate over
Turn the plate over
Take a piece of flat iron (plough-plate iron) of a thickness and width to suit the intended bore. Bend up its sides ('turn it over') until the edges meet, or nearly so, and it forms a long tube. Ours: hammer and anvil for the bending.
Ibikoresho by'iyi ntambwe:
 Ibyuma bicuzwe1 flat plough-plate iron
 Ingano zitazwi1 igice
Ibikoresho bikenewe:
 Inyundo yo Gucura
 Igitare cy'ubutare gisanzwe
2
2
Heat in the hollow fire
Heat in the hollow fire
Put the tube into a hollow fire, urged by a blast, and heat it until the iron is on the point of fusion. Ours: a smith's forge as the hollow fire.
Ibikoresho bikenewe:
 Uruganda rw'umucuzi
 Amakoro y'Umucuzi
3
3
Draw it through the dies
Draw it through the dies
Clamp the end of the tube to the chain of the draw bench, driven by a hand winch or an engine. Draw it out of the fire through a pair of dies of the size wanted, set in a screw press and closed to their bearing, so that the hot edges are pressed together and welded. A pair of pinchers with a conical hole, held against a standard, may be used instead of the press and dies.
Ibikoresho bikenewe:
 Intebe yo gukururaAmakoro y'Umucuzi
4
4
Weld the other half
Weld the other half
Open the clamp and take the tube off. Grip the other end, put the unwelded part into the fire, heat it, and draw it through the dies in the same way.
Ibikoresho bikenewe:
Uruganda rw'umucuziIntebe yo gukururaAmakoro y'UmucuziIbikoresho
2- 1 flat plough-plate ironUmwanya
- 1 igiceUmwanya
Ibikoresho bikenewe
5- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
Ibikoresho by'Ibishushanyo Bifitanye Isano


Iki gishushanyo gikora
CC0 Umurenge rusange
Iyi blueprint yasohowe munsi ya CC0. Ushobora gukoporora, guhindura, gukwirakwiza no gukoresha nta kwemererwa.
Shyigikira Umuremyi ugura ibicuruzwa binyuze muri Blueprint ye Komisiyo y'Umuremyi byashyizweho n'Abacuruzi, cyangwa kora verisiyo nshya y'iyi Blueprint ukayinjiza nk'isano muri Blueprint yawe kugira ngo musangire inyungu.