Ubufatanye
UBUHANZI
UBWIZA N'UBUZIMA
UBUKORIKORI
UMUCO N'AMATEKA
IMYIDAGADURO
IBIDUKIKIJE
IBIRIBWA N'IBINYOBWA
UBWUBATSI BUSUBIRA INYUMA
UBUMENYI
SIPORO
IKORANABUHANGA
IBYAMBARWA
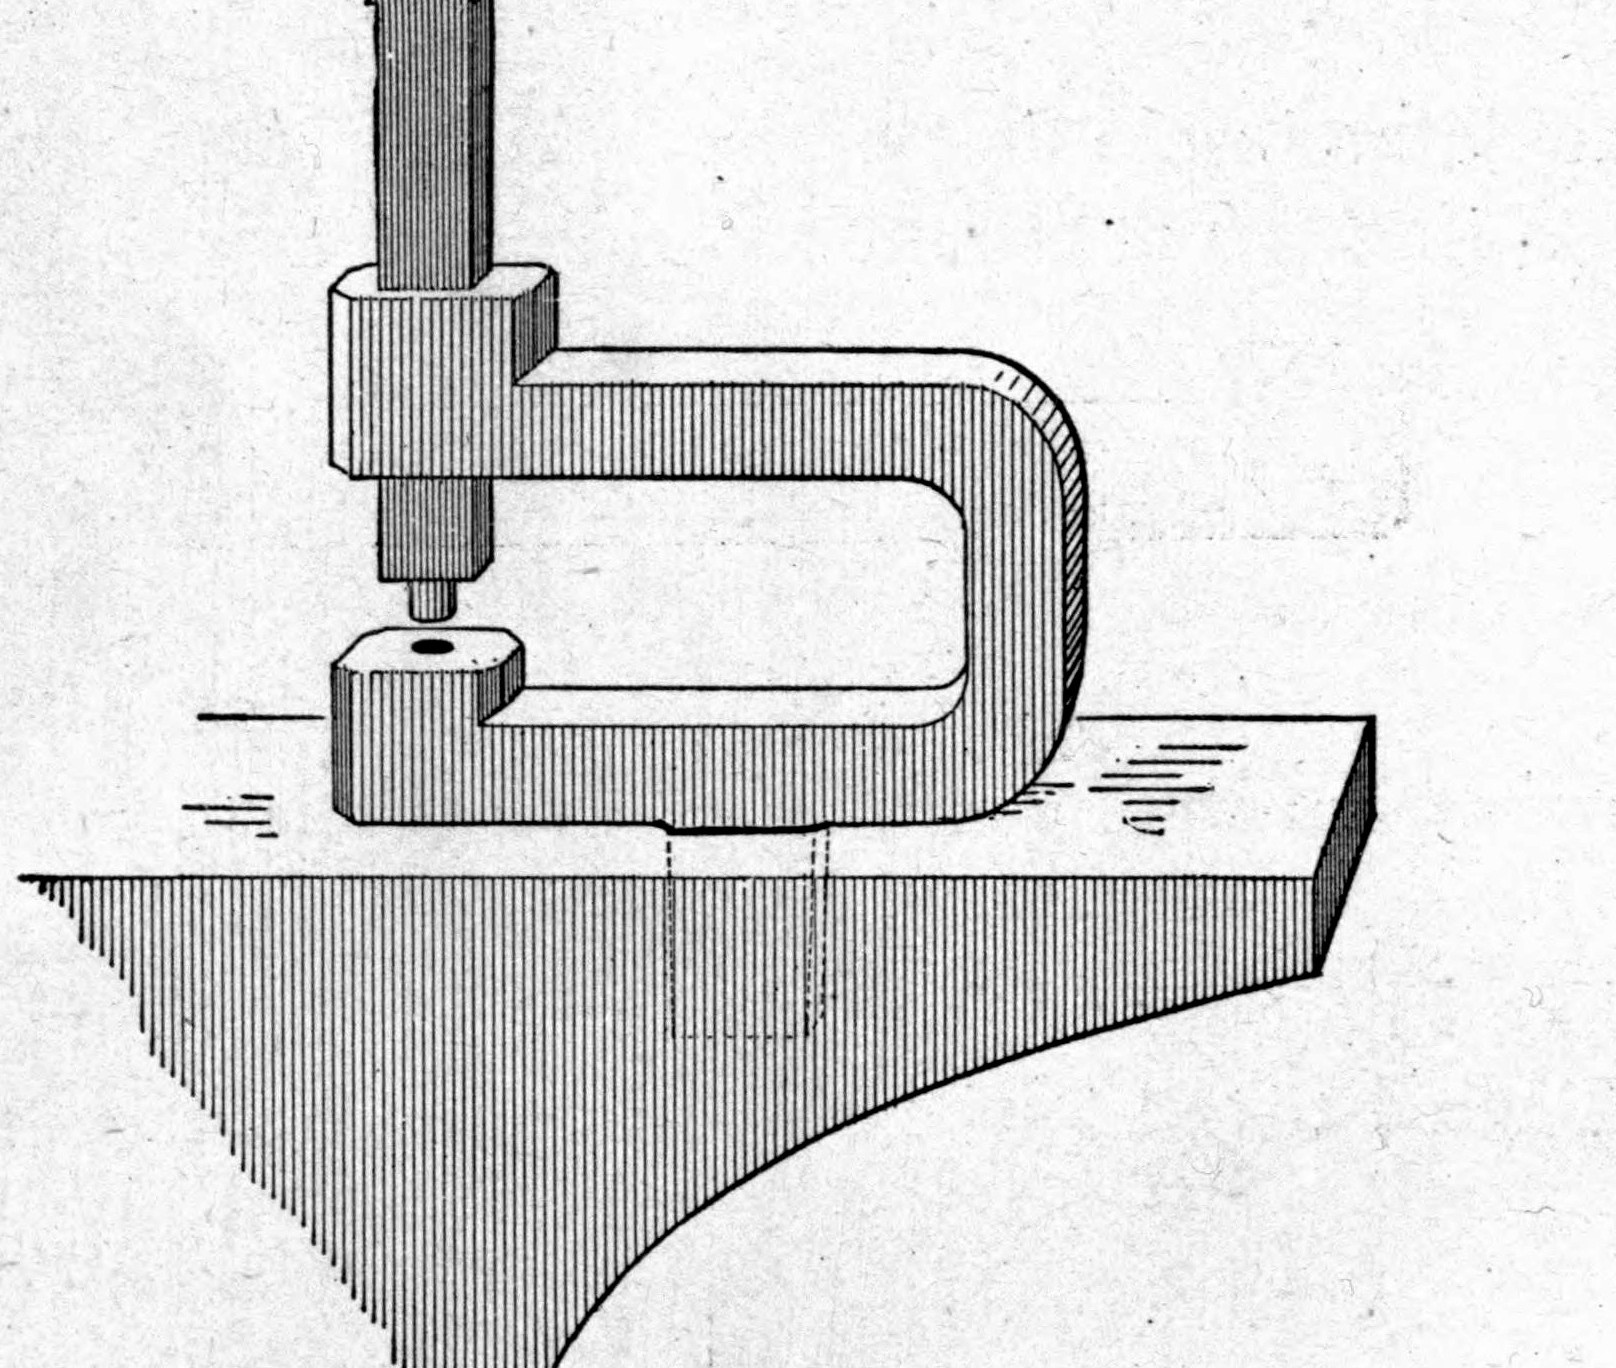


Anvil Hole Punch: Forged C-Frame With a Steel Die Block and Top Die, Set in the Hardy Hole (Richardson, 1889)
A blacksmith's anvil punch from Richardson's Practical Blacksmithing (1889): a bent C-frame of Swedish iron with a steel die block welded on, a square shank that drops into the anvil's hardy hole, and a cast-steel top die struck with a sledge. A set of six, 1/4 to 1 in, punches cold iron up to 5/16 or 3/8 in thick.
Hejuru
About 1 day
Amabwiriza
1
1
The set of six
The set of six
Gupakira ikaye ya Jupyter…
2
2
Read Practical Blacksmithing
Read Practical Blacksmithing
"I think every blacksmith should have a set of them."
3
3
Forge the frame and die block
Forge the frame and die block
Take Swedish iron 1-1/2 by 3/4 by 10 in, upset one end a little, and weld a square of good steel 1-1/2 by 1-1/2 in firmly on it. Punch a hole in the centre of the steel a little larger than the hole to be cut, driving from the iron side so the hole is largest at the bottom and the slugs drop out. Heat the other end, cut it half off 1-1/2 in from the end, bend it over and weld it, then punch and work out a perfectly true 3/4 in square hole (Fig. 68).
Ibikoresho by'iyi ntambwe:
 Umugozi w'icyuma cyacuzwe1 igice
 Inkoni y'icyuma cy'ibikoresho1 igice
Ibikoresho bikenewe:
 Uruganda rw'umucuzi
 Ingoyi
 Inyundo
 Amakoro y'Umucuzi
 Igitobora gishyushye
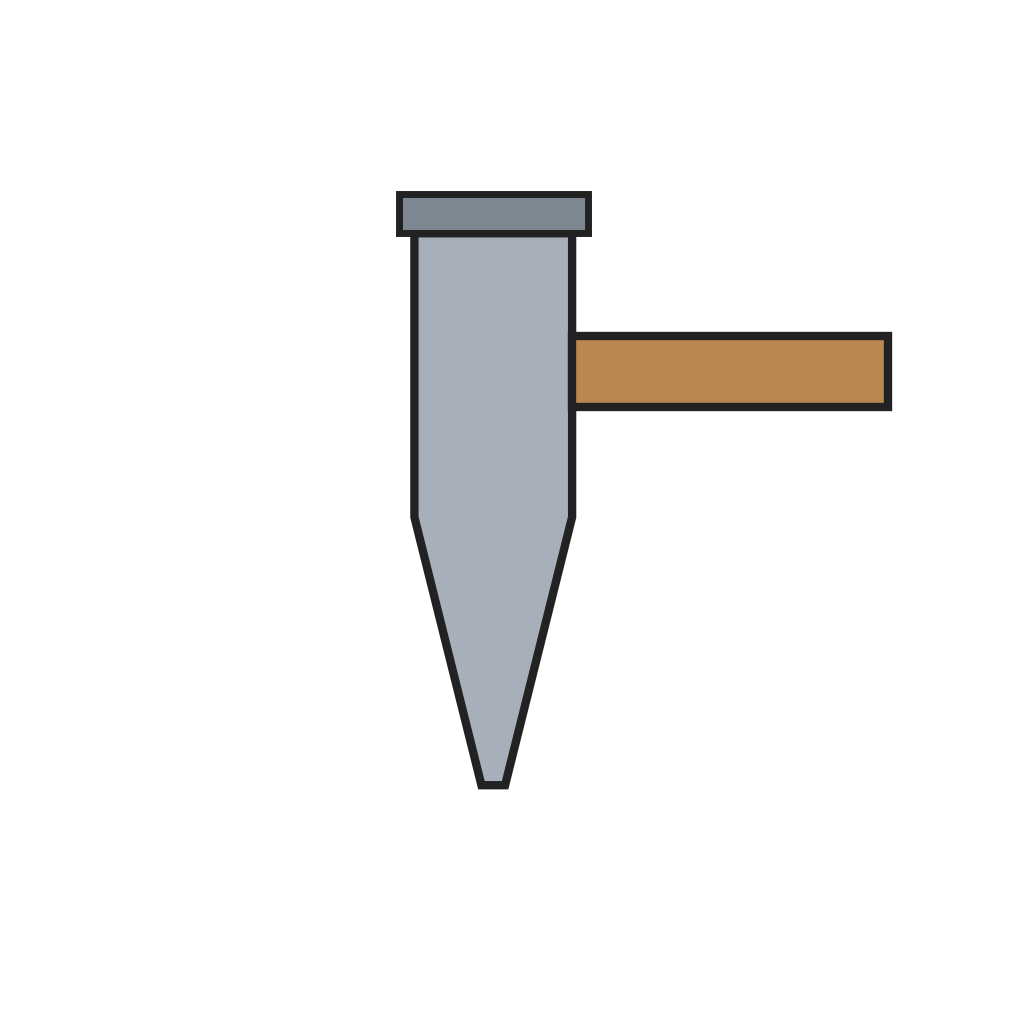 Icyuma gikata gishyushye
 Inyundo nini
4
4
Weld on the shank
Weld on the shank
Weld an iron the size of your anvil's square hole on the bottom side, 2-1/2 in from the round hole (Fig. 69). File and dress the piece.
Ibikoresho by'iyi ntambwe:
Umugozi w'icyuma cyacuzwe1 igiceIbikoresho bikenewe:
Uruganda rw'umucuziIngoyiInyundo Amakariso (Ikariso ry'Intoki)
5
5
Make the top die
Make the top die
Cut 6 in of 3/4 in square cast steel, draw it down and file one end to fit the round hole; for the 1/4 in punch make the round part 5/16 in long, larger for larger punches (Fig. 70).
Ibikoresho by'iyi ntambwe:
Inkoni y'icyuma cy'ibikoresho1 igiceIbikoresho bikenewe:
Uruganda rw'umucuziIngoyiInyundoAmakariso (Ikariso ry'Intoki) Umucumita w'Ibyuma
6
6
Bend, fit and temper
Bend, fit and temper
Heat the frame and bend it so the two holes line up; fit the top die and make sure it enters the hole perfectly true. Let it cool slowly, check the bottom die face and that the die works straight and easily, then temper as for any tool that cuts iron (Fig. 71).
Ibikoresho bikenewe:
Uruganda rw'umucuziIngoyiInyundo Indobo yo gukonjesha
7
7
Troubleshooting
Troubleshooting
Anvil punch troubleshooting.
Flow
Loading...
8
8
History and honest limits
History and honest limits
From M. T. Richardson (ed.), **Practical Blacksmithing**, vol. I (1889), "Making an Anvil Punch" by N. C. M. (checked on the archive.org scan practicalblacksm00richrich, pp. 126-128). He gives no temper colour; the tools and metric figures are ours.
Ibikoresho
2- 1 igiceUmwanya
- Umwanya
Ibikoresho bikenewe
10- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
Iki gishushanyo gikora
Blueprint zijyanye
Izi blueprint zisangira ubumenyi — uburyo, ibikoresho cyangwa amahame
CC0 Umurenge rusange
Iyi blueprint yasohowe munsi ya CC0. Ushobora gukoporora, guhindura, gukwirakwiza no gukoresha nta kwemererwa.
Shyigikira Umuremyi ugura ibicuruzwa binyuze muri Blueprint ye Komisiyo y'Umuremyi byashyizweho n'Abacuruzi, cyangwa kora verisiyo nshya y'iyi Blueprint ukayinjiza nk'isano muri Blueprint yawe kugira ngo musangire inyungu.