UBUHANZI
UBWIZA N'UBUZIMA
UBUKORIKORI
UMUCO N'AMATEKA
IMYIDAGADURO
IBIDUKIKIJE
IBIRIBWA N'IBINYOBWA
UBWUBATSI BUSUBIRA INYUMA
UBUMENYI
SIPORO
IKORANABUHANGA
IBYAMBARWA
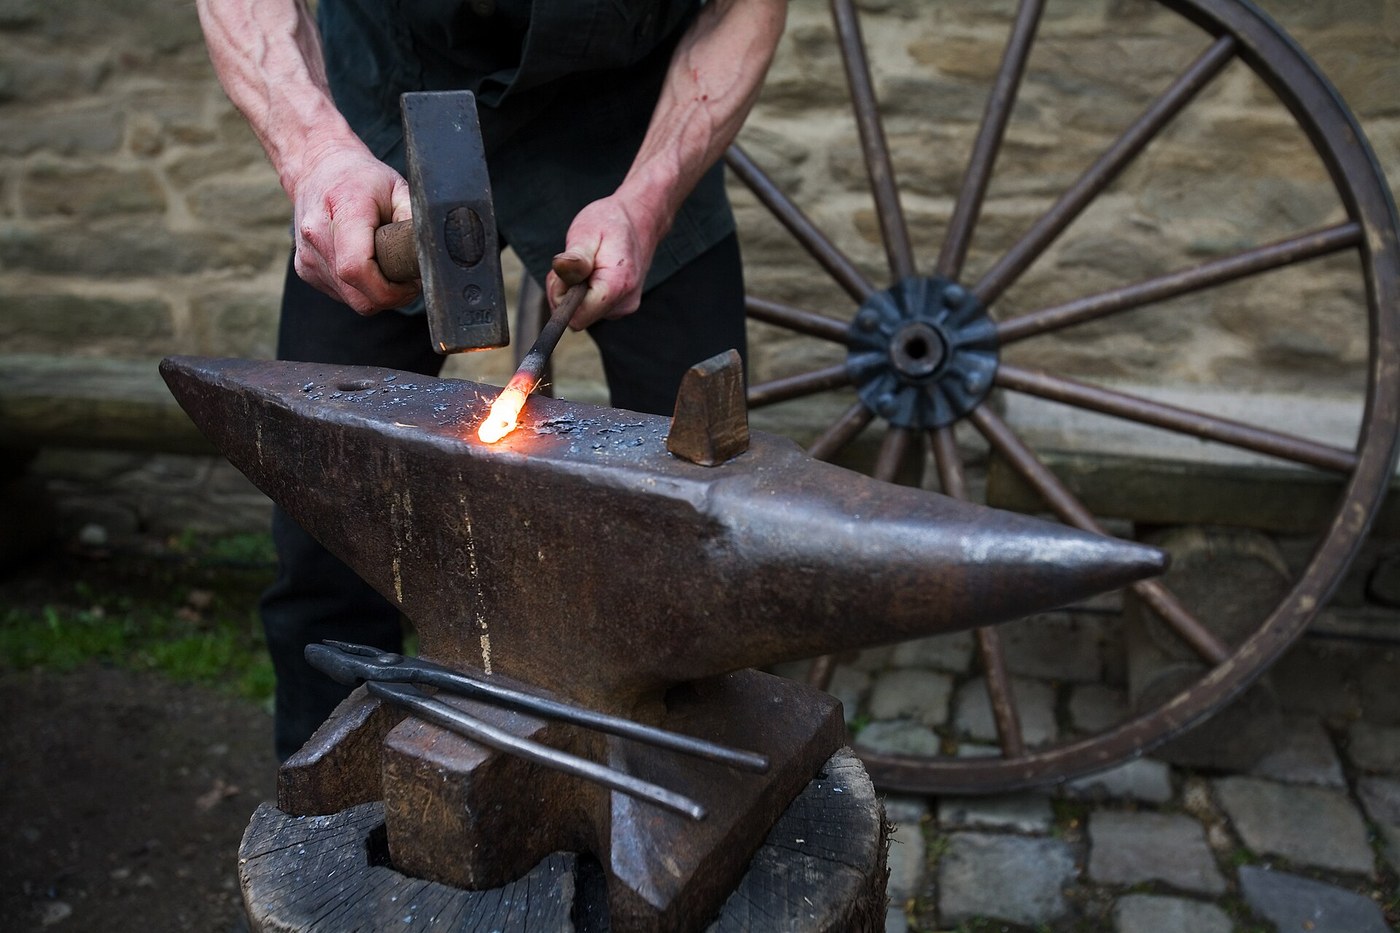


Smith's Top and Bottom Tools: Punch, Drift, Hardy, Fullers, Chisel and Swage
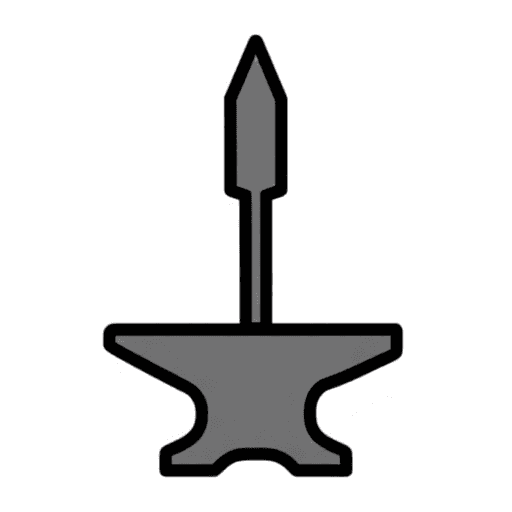
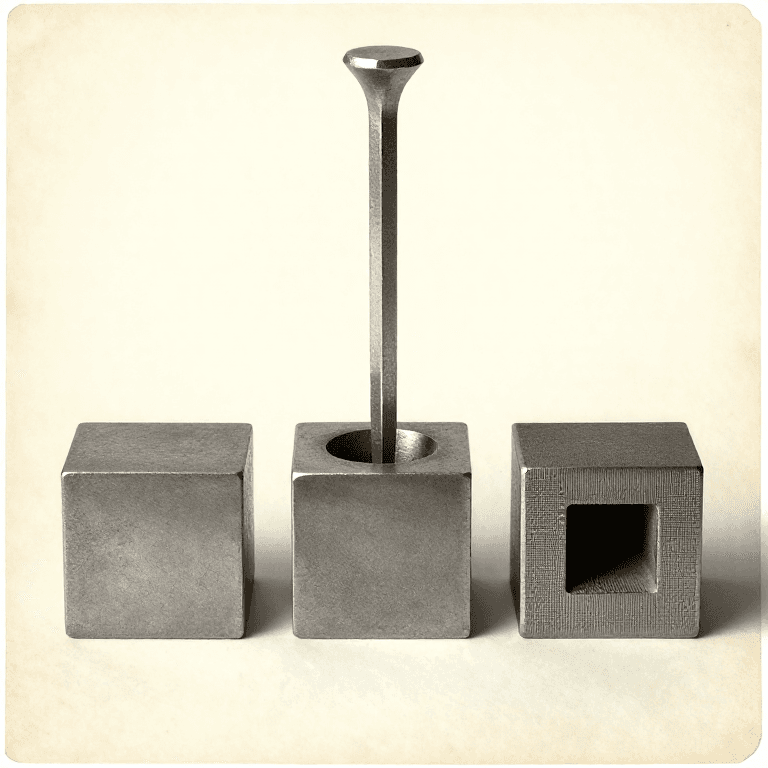
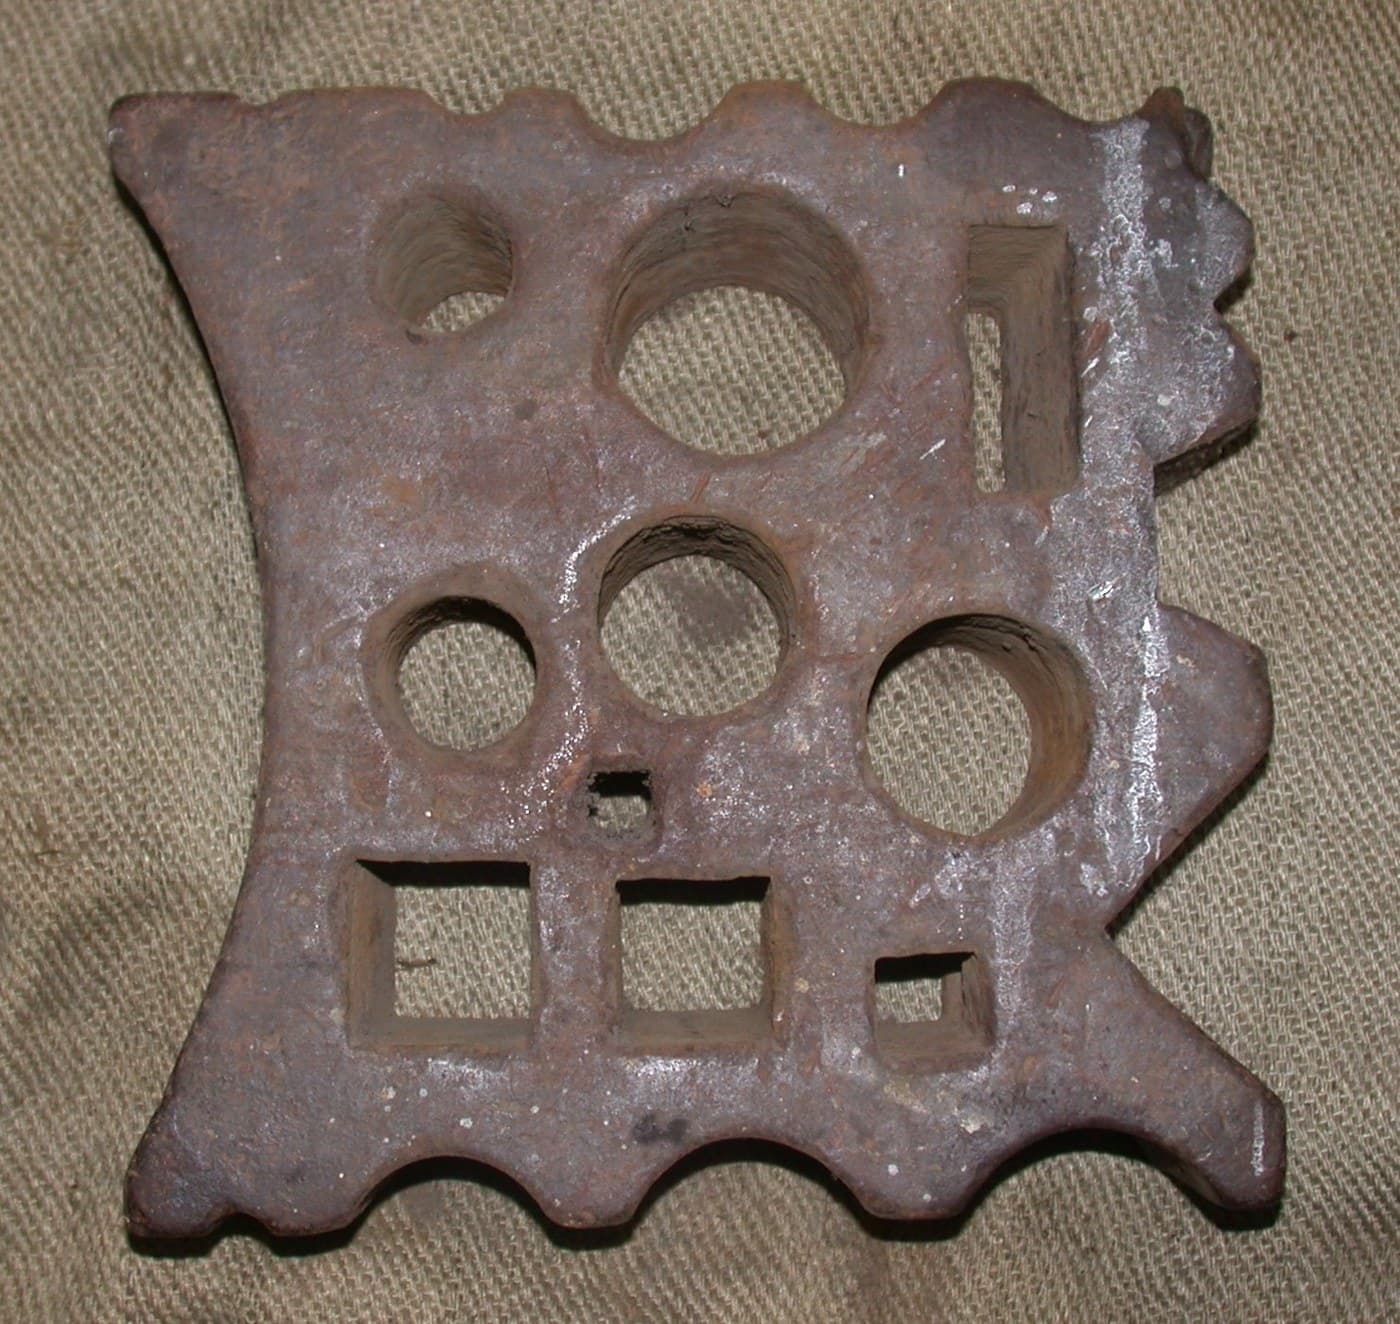
Bottom tools have a square shank that drops into the anvil's hardy hole; top tools have a handle and are held on the work and struck. The hardy cuts hot stock laid over it, the fuller's rounded nose spreads metal, the punch makes a hole and the drift opens it to size, the hot chisel cuts from above, and the bottom swage rounds bar in its groove. Forge them all from tool steel.
The picture: a smith at the anvil, a hardy standing in the hardy hole.
Hejuru
Two days
Amabwiriza
1
1
Shanks for the hardy hole
Shanks for the hardy hole
For each bottom tool, forge a square shank that slips into the hardy hole without rocking, with a shoulder above it that sits on the anvil face.
Ibikoresho by'iyi ntambwe:
 Inkoni ifite impande umunani y'icyuma cy'ibikoresho4 kg
 Amakara6 as required
Ibikoresho bikenewe:
 Uruganda rw'umucuzi
 Ingoyi
 Inyundo ifite umutwe utambitse
 Inyundo nini
 Amafashi y'umucuzi
 Uturindantoki two gukomeza ibyuma
 Amadarubindi y'umutekano
2
2
Hardy and bottom fuller
Hardy and bottom fuller
On one shanked blank forge a wedge with its edge upward: the hot cut hardy. On another, forge a rounded nose: the bottom fuller.
Ibikoresho bikenewe:
Uruganda rw'umucuziIngoyiInyundo ifite umutwe utambitseInyundo niniAmafashi y'umucuziUturindantoki two gukomeza ibyumaAmadarubindi y'umutekano3
3
Bottom swage
Bottom swage
On a third shanked blank, form a half-round groove by forging a hot bar of the size you want into it with the top swage, then file it clean.
Ibikoresho bikenewe:
Uruganda rw'umucuziIngoyiInyundo ifite umutwe utambitseInyundo niniAmafashi y'umucuziUturindantoki two gukomeza ibyumaAmadarubindi y'umutekano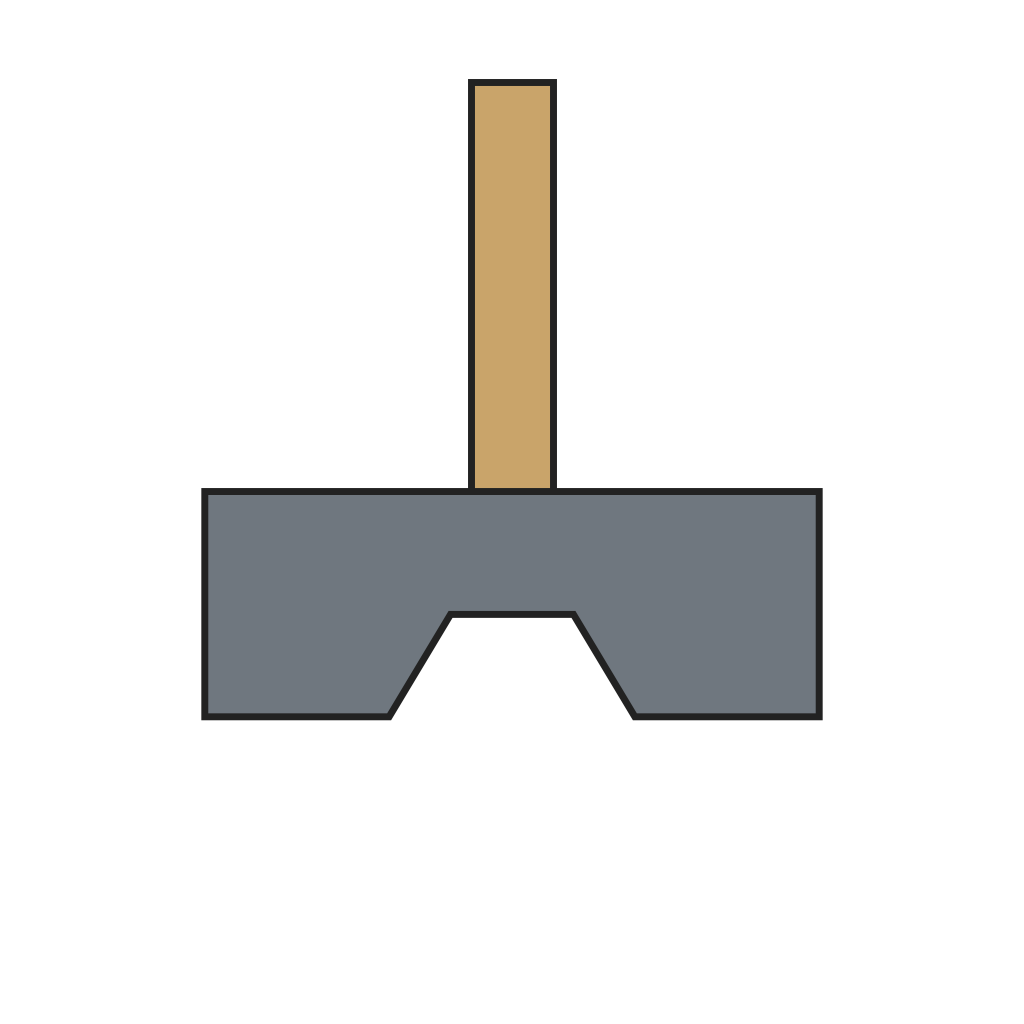 Ikibumbiro cyo hejuru cyo kuzengurutsa
 Ikariso ry'Icyuma
4
4
Top tools
Top tools
Forge the top tools from bar: a hot punch tapering to a small flat end, a drift tapering evenly to the size of the finished hole, a top fuller with a rounded nose, and a hot chisel with a thin edge. Leave a flat face on top of each to be struck.
Ibikoresho bikenewe:
Uruganda rw'umucuziIngoyiInyundo ifite umutwe utambitseInyundo niniAmafashi y'umucuziUturindantoki two gukomeza ibyumaAmadarubindi y'umutekano5
5
Harden the edges and fit handles
Harden the edges and fit handles
Harden the hardy and hot chisel edges in water and temper them to blue; leave the punch, drift and fullers as forged, since they work hot (our practice). Fit ash handles to the hot chisel and top fuller.
Ibikoresho by'iyi ntambwe:
 Igice cy'igiti cya ash cyasatuwe2 ibice
 Amazi10 litiro
Ibikoresho bikenewe:
Uruganda rw'umucuzi Indobo yo gukonjesha
 Ibuye ryo gutyaza ry'uruzigaAmafashi y'umucuziUturindantoki two gukomeza ibyumaAmadarubindi y'umutekano
6
6
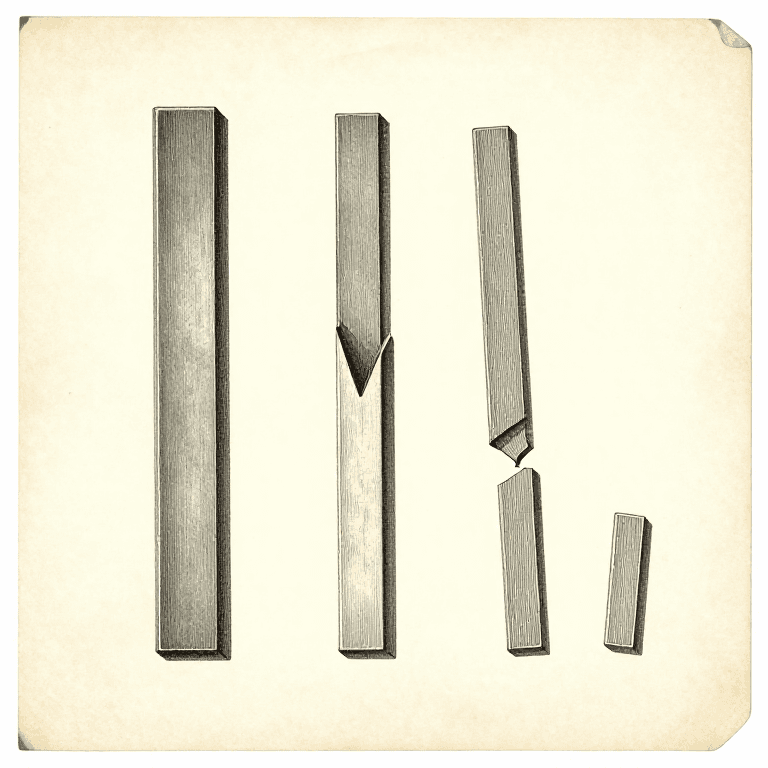
Steel for the set
Steel for the set
Gupakira ikaye ya Jupyter…
Ibikoresho
4- 6 as requiredUmwanya
- Umwanya
- 10 litiroUmwanya
Ibikoresho bikenewe
11- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
Iki gishushanyo gikora
Blueprint zijyanye
Izi blueprint zisangira ubumenyi — uburyo, ibikoresho cyangwa amahame
CC0 Umurenge rusange
Iyi blueprint yasohowe munsi ya CC0. Ushobora gukoporora, guhindura, gukwirakwiza no gukoresha nta kwemererwa.
Shyigikira Umuremyi ugura ibicuruzwa binyuze muri Blueprint ye Komisiyo y'Umuremyi byashyizweho n'Abacuruzi, cyangwa kora verisiyo nshya y'iyi Blueprint ukayinjiza nk'isano muri Blueprint yawe kugira ngo musangire inyungu.