UBUHANZI
UBWIZA N'UBUZIMA
UBUKORIKORI
UMUCO N'AMATEKA
IMYIDAGADURO
IBIDUKIKIJE
IBIRIBWA N'IBINYOBWA
UBWUBATSI BUSUBIRA INYUMA
UBUMENYI
SIPORO
IKORANABUHANGA
IBYAMBARWA
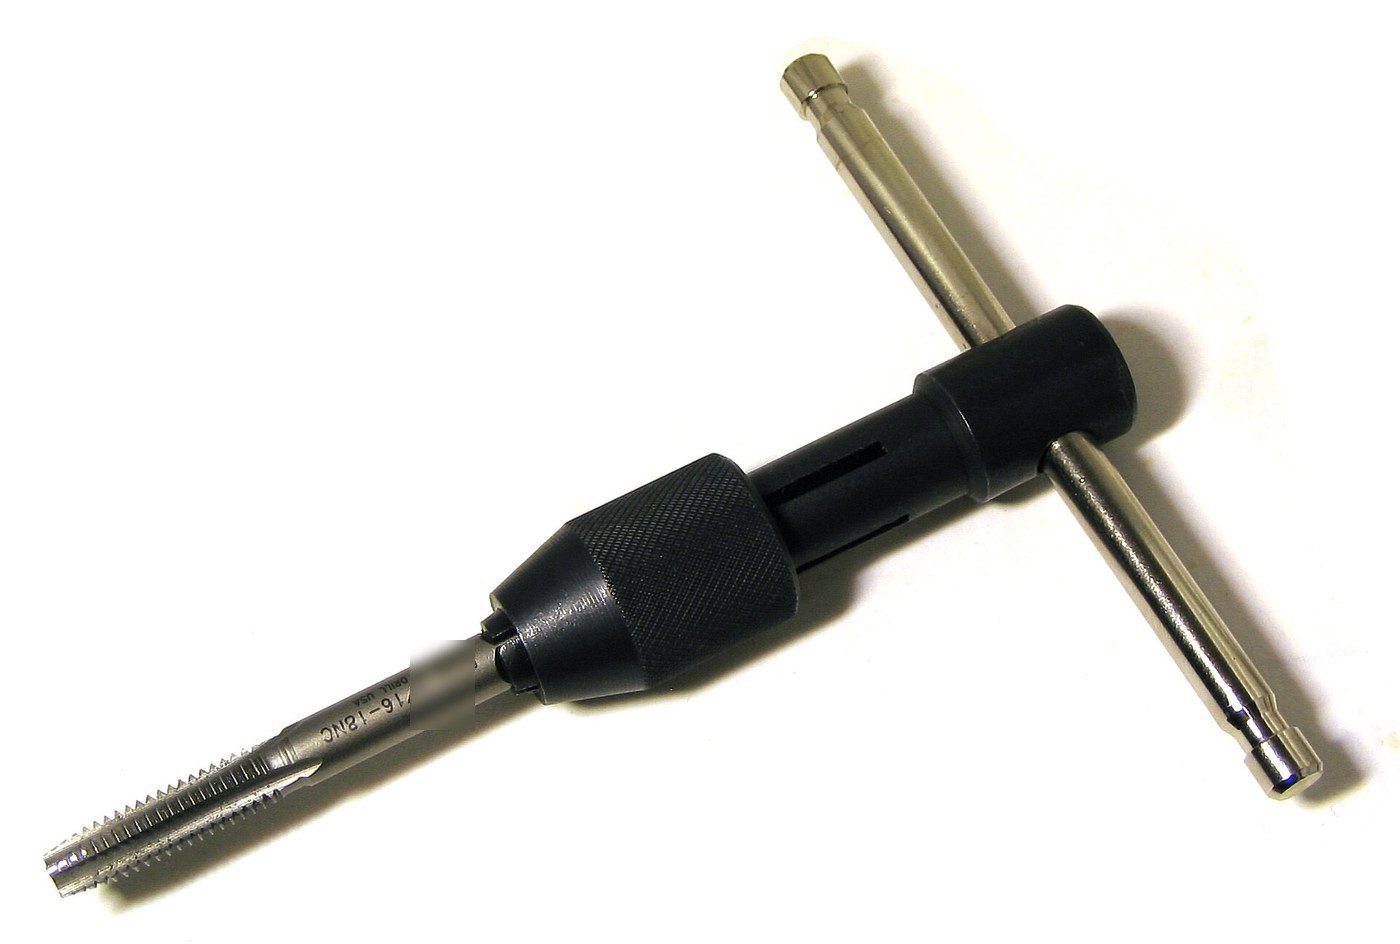

Taps and Dies Cut on the Lathe, with Wrench and Stock
A tap cuts the thread inside a hole; a die cuts it on a rod. Makers made their own in the 16th and 17th centuries. Cut the thread on tool steel in the screw-cutting lathe, file flutes so it cuts, harden it, and use the finished tap to cut the thread in a steel blank that becomes the matching die. A T-wrench turns the tap, a stock holds the die.
The picture: a tap held in a T-wrench.
Hejuru
Two days for a few sizes
Amabwiriza
1
1
Turn and thread the tap
Turn and thread the tap
Turn tool steel to the thread's major diameter with a square on the end for the wrench. Cut the thread in the lathe at the right pitch and check it with the gauge. Taper the first 8–10 threads for a taper tap, or 3–5 for a plug tap.
Ibikoresho by'iyi ntambwe:
 Inkoni ifite impande umunani y'icyuma cy'ibikoresho1 igice
Ibikoresho bikenewe:
 Imashini yo guhinguza icyuma
 Ibikoresho byo Kuzenguruka Ibiti bya HSS
 Ikipimo cy'imizingo
 Ikigereranyo cya Digitale cy'Amasentimetero 6
 Amavuta yo gukata
2
2
Flute and harden the tap
Flute and harden the tap
File three or four lengthwise flutes along the thread so it has cutting edges and room for chips. Harden in water from cherry red and temper to brown.
Ibikoresho by'iyi ntambwe:
 Amazi10 litiro
 Amakara1 as required
Ibikoresho bikenewe:
 Ikariso ry'Icyuma
 Ifatiro ry'Ameza
 Uruganda rw'umucuzi
 Indobo yo gukonjesha
 Amafashi y'umucuzi
 Amadarubindi y'umutekano
3
3
Cut the die with the tap
Cut the die with the tap
Drill a flat tool-steel blank to the tap drill size and run the finished tap through it with oil. Drill clearance holes round the thread so it cuts, saw one side open so it can be set, then harden and temper it to brown.
Ibikoresho by'iyi ntambwe:
 Inkoni iringaniye y'icyuma cy'ibikoresho1 igice
Ibikoresho bikenewe:
 Igikoresho cyo gutobora gikoreshwa n'intokiIfatiro ry'AmezaIkariso ry'IcyumaUruganda rw'umucuziIndobo yo gukonjesha
4
4
Wrench and stock
Wrench and stock
Forge and file a T-wrench with a square hole for the tap, and a die stock from flat bar with a round recess for the die, two handles and a set screw.
Ibikoresho by'iyi ntambwe:
 Umurongo ugororotse w'icyuma cyoroshye1 igice
Ibikoresho bikenewe:
Uruganda rw'umucuziIkariso ry'IcyumaIgikoresho cyo gutobora gikoreshwa n'intokiIfatiro ry'Ameza5
5
Tap drill sizes
Tap drill sizes
Gupakira ikaye ya Jupyter…
Ibikoresho
5- Umwanya
- 10 litiroUmwanya
- 1 as requiredUmwanya
- Umwanya
- Umwanya
Ibikoresho bikenewe
12- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
Iki gishushanyo gikora
Blueprint zijyanye
Izi blueprint zisangira ubumenyi — uburyo, ibikoresho cyangwa amahame


CC0 Umurenge rusange
Iyi blueprint yasohowe munsi ya CC0. Ushobora gukoporora, guhindura, gukwirakwiza no gukoresha nta kwemererwa.
Shyigikira Umuremyi ugura ibicuruzwa binyuze muri Blueprint ye Komisiyo y'Umuremyi byashyizweho n'Abacuruzi, cyangwa kora verisiyo nshya y'iyi Blueprint ukayinjiza nk'isano muri Blueprint yawe kugira ngo musangire inyungu.