UBUHANZI
UBWIZA N'UBUZIMA
UBUKORIKORI
UMUCO N'AMATEKA
IMYIDAGADURO
IBIDUKIKIJE
IBIRIBWA N'IBINYOBWA
UBWUBATSI BUSUBIRA INYUMA
UBUMENYI
SIPORO
IKORANABUHANGA
IBYAMBARWA
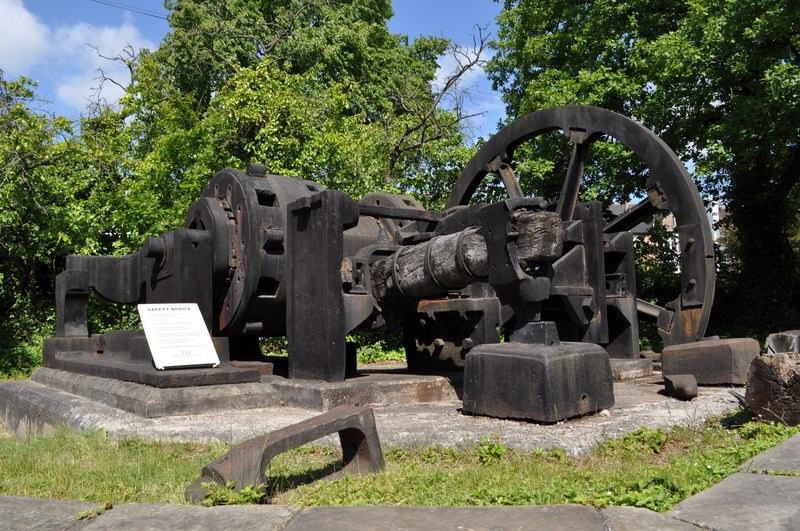


Tool-Steel Bar: Crucible Steel Drawn Out at a Cherry-Red Heat
Sheffield poured its crucible cast steel into octagonal or rectangular iron moulds and drew the ingots out into rods under the tilt hammer. That bar, eight-sided or square, was the stock for chisels, punches, files and blades. Andrew Ure's 1839 warning still holds: this steel must not go much above a cherry-red heat, or it turns brittle.
The picture: a water-driven tilt hammer at Abbeydale Industrial Hamlet, Sheffield.
Hejuru
A day at the forge
Amabwiriza
1
1
Heat gently to cherry red
Heat gently to cherry red
Bring the crucible-steel ingot up slowly in the forge to a cherry-red heat and no hotter. Ure: in its usual state cast steel will not bear much more without becoming brittle, and it will not take a welding heat.
Ibikoresho by'iyi ntambwe:
 Icyuma gikomeye cy'isahani y'ishongesha2 kg
 Amakara1 as required
Ibikoresho bikenewe:
 Uruganda rw'umucuzi
 Amafashi y'umucuzi
 Uturindantoki two gukomeza ibyuma
 Ikanzu y'uruhu
 Amadarubindi y'umutekano
2
2
Draw out a billet
Draw out a billet
On the anvil, with a striker on the sledge, draw the ingot out square, turning it a quarter after each pair of blows. Reheat as soon as the colour drops below red; never hammer it cold. Stop at a square billet of the size you need, or carry on drawing it flat into a rectangular bar for axe heads and picks.
Ibikoresho by'iyi ntambwe:
Amakara1 as requiredIbikoresho bikenewe:
 Ingoyi
 Inyundo nini
 Inyundo ifite umutwe utambitseAmafashi y'umucuziUturindantoki two gukomeza ibyumaIkanzu y'uruhuAmadarubindi y'umutekano
3
3
Knock the corners to an octagon
Knock the corners to an octagon
For octagon bar, set the square bar on a corner and hammer the four corners down evenly until all eight faces are equal, finishing in the matching groove of a swage block.
Ibikoresho bikenewe:
IngoyiInyundo ifite umutwe utambitse Igiti cy'ibyuma gifite imyoboAmafashi y'umucuziUturindantoki two gukomeza ibyumaIkanzu y'uruhuAmadarubindi y'umutekano
4
4
Check and cool slowly
Check and cool slowly
Check the size across the flats with a caliper, then let the bar cool slowly in the dying forge (our choice, to leave it soft for cutting and filing).
Ibikoresho bikenewe:
 Ikigereranyo cya Digitale cy'Amasentimetero 6Uruganda rw'umucuzi
Ibikoresho bikenewe
10- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
Iki gishushanyo gikora

Blueprint zijyanye
Izi blueprint zisangira ubumenyi — uburyo, ibikoresho cyangwa amahame


CC0 Umurenge rusange
Iyi blueprint yasohowe munsi ya CC0. Ushobora gukoporora, guhindura, gukwirakwiza no gukoresha nta kwemererwa.
Shyigikira Umuremyi ugura ibicuruzwa binyuze muri Blueprint ye Komisiyo y'Umuremyi byashyizweho n'Abacuruzi, cyangwa kora verisiyo nshya y'iyi Blueprint ukayinjiza nk'isano muri Blueprint yawe kugira ngo musangire inyungu.