Ubufatanye
UBUHANZI
UBWIZA N'UBUZIMA
UBUKORIKORI
UMUCO N'AMATEKA
IMYIDAGADURO
IBIDUKIKIJE
IBIRIBWA N'IBINYOBWA
UBWUBATSI BUSUBIRA INYUMA
UBUMENYI
SIPORO
IKORANABUHANGA
IBYAMBARWA
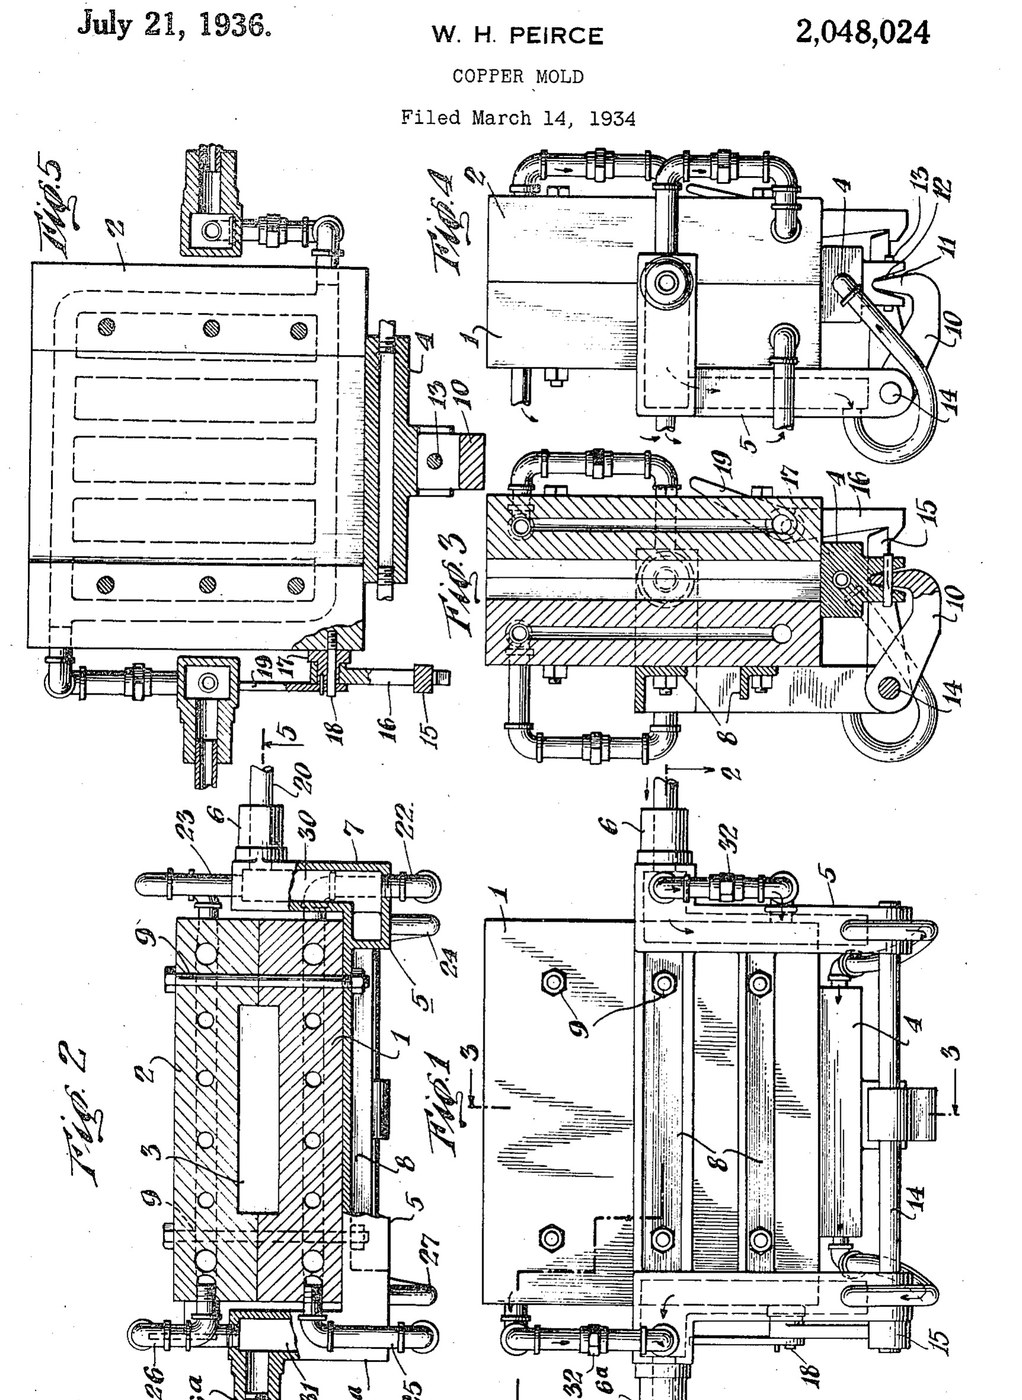

Water-Cooled Copper Mould: Two Halves with Cast-In Pipes, in a Trunnion Yoke (Peirce, US 2,048,024, 1936)
A mould for metals that conduct heat well: two thick copper blocks, each cast round a grid of copper pipes that carry cooling water. They are bolted face to face, so the cavity can be machined accurately, and carried in a steel yoke on hollow trunnions that feed the water. A latched gate closes the bottom. The casting can be dumped out of the top by turning the yoke, or out of the bottom by opening the gate.
Result: a water-cooled copper mould that freezes the metal fast and can be taken apart, machined and cleaned.
Source: W. H. Peirce (American Smelting and Refining), US 2,048,024 (1936). Unknown: sizes and the copper grade. Picture: the patent drawing.
Hejuru
Unknown
Amabwiriza
1
1
Cast the two halves round their pipes
Cast the two halves round their pipes
For each half, assemble copper pipes into a grid: a horizontal inlet pipe at the bottom, an outlet pipe at the top, and several vertical pipes joining them. Any steam formed in casting then rises to the outlet. Cast a block of copper of about the mould's shape over the grid. Ours: copper ingot melted in a crucible furnace. Not given: sizes, the copper grade.
Ibikoresho by'iyi ntambwe:
 Umuyoboro w'umuringa1 cooling-pipe grids
 Ikibumbe cy'umuringa1 mould blocks
Ibikoresho bikenewe:
 Itanura ry'inkono yo gushongesheramo
 Ingano zitazwi
2
2
Machine the cavity
Machine the cavity
Machine the inner faces of the two halves to form the casting space, accurately. The recesses can be cut to different depths, for example five-eighths of the casting's width in one half and three-eighths in the other. Bolt the halves together face to face.
Ibikoresho by'iyi ntambwe:
 Icyuma kitazwi1 bolts
Ibikoresho bikenewe:
 Imashini ibaza icyuma
 Icyuma Cyivumbura Gihagaze
 Agakoresho ko gukata imizingo y'ibyuma
3
3
Make the yoke and the bottom gate
Make the yoke and the bottom gate
Cast a U-shaped steel yoke in one piece: two hollow ends with trunnions in line, joined by struts that carry the mould, bolted on. Make a bottom gate machined to fit tight under the mould, with its own cooling passage. Mount it on a gate arm keyed to a shaft across the yoke, its wedge end pinned in a V slot so the gate rocks to align. Add a lever on the shaft and a latch on an eccentric with a handle, to lock the gate up tight. Ours: steel ingot for the yoke casting.
Ibikoresho by'iyi ntambwe:
 Igice cy'icyuma gikomeye1 yoke castingIcyuma kitazwi1 gate, arm, shaft, lever, latch
Ibikoresho bikenewe:
Itanura ry'inkono yo gushongesheramoImashini ibaza icyuma4
4
Pipe the cooling water
Pipe the cooling water
Bring water in through a pipe in the centre of one trunnion into the hollow yoke end, and from there by fitted pipes to the inlets of both halves and by a flexible metal hose to the gate. Lead the outlets to the other hollow end, and out through a pipe in the centre of the other trunnion, so the water keeps flowing while the yoke turns. Not given: the hose, the flow.
Ibikoresho by'iyi ntambwe:
Umuyoboro w'umuringa1 inlet and outlet pipes Ibikoresho bitazwi1 metallic hoses
Ibikoresho bikenewe:
 Amazi
5
5
Cast and dump a cake
Cast and dump a cake
Latch the gate shut, coat the cavity with a mould dressing such as graphite, circulate the water and fill the mould with molten metal. When the cake has cooled, turn the yoke on its trunnions so it slides out of the top, or trip the latch so the gate swings back and it drops out of the bottom. Unbolt the halves now and then to clean them or machine their faces true again.
Ibikoresho bikenewe:
 Ifu ya girafiteAmazi
Ibikoresho
5- 1 inlet and outlet pipesUmwanya
- 1 mould blocksUmwanya
- 1 gate, arm, shaft, lever, latchUmwanya
- 1 yoke castingUmwanya
- 1 metallic hosesUmwanya
Ibikoresho bikenewe
7- Umwanya
- Umwanya
- Umwanya
- Umwanya
- Umwanya
Ibikoresho by'Ibishushanyo Bifitanye Isano
Akaga
10% igabana
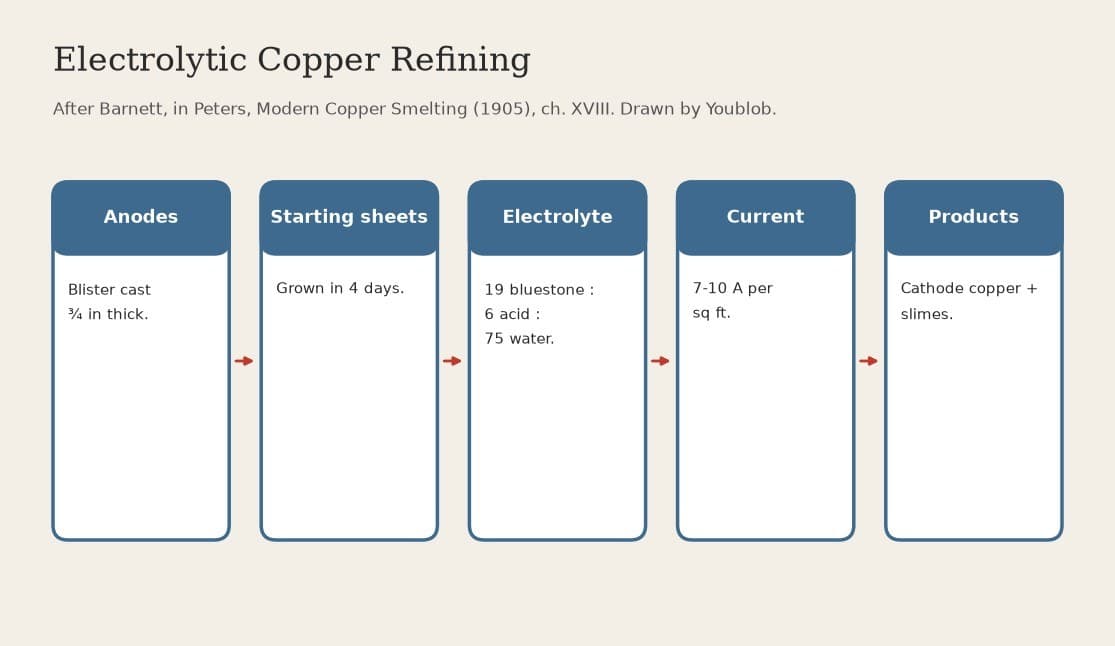
Electrolytic Copper and Refinery Slimes: Blister Anodes Dissolved in Bluestone and Acid (Barnett, in Peters 1905)
na Charlie
Ubucuzi bw'Ibyuma
7
0
0
0
1
0
10% igabana
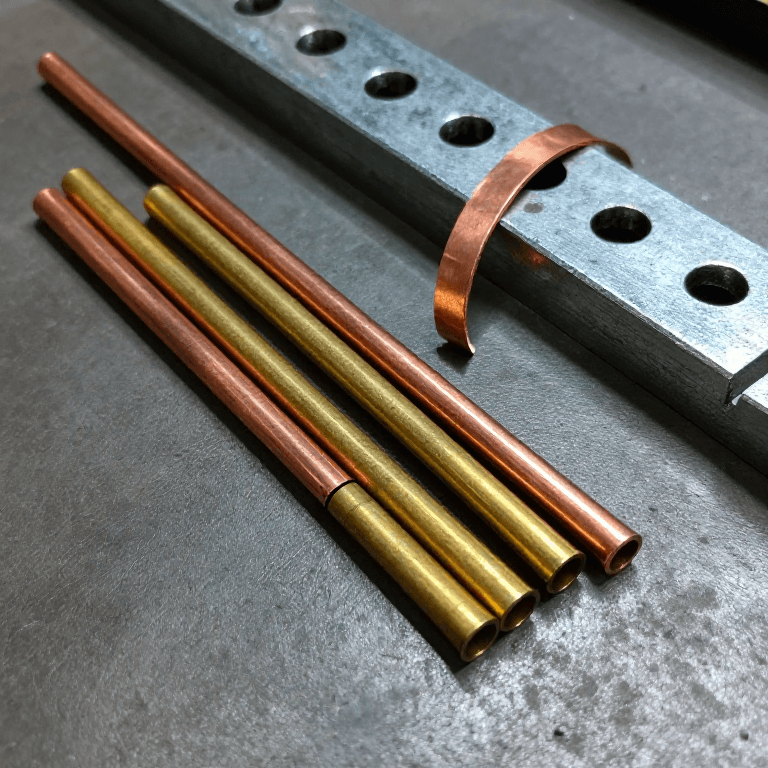
Copper and Brass Tube Drawn from Strip
na Forge
Ubucuzi bw'Ibyuma
47
0
0
0
3
0

10% igabana
Crucible Furnace: the Brass Founder's Sunk Coke Air Furnace (Larkin, 1907)
na Forge
Itanura
8
0
0
0
1
0
10% igabana
Universal Milling Machine
na Martin
UBUKORIKORI
54
0
0
0
1
0
10% igabana
Graphite Powder Ground from Plumbago
na Mary
Bidafite Ubuzima
13
0
0
0
2
0
Iki gishushanyo gikora
CC0 Umurenge rusange
Iyi blueprint yasohowe munsi ya CC0. Ushobora gukoporora, guhindura, gukwirakwiza no gukoresha nta kwemererwa.
Shyigikira Umuremyi ugura ibicuruzwa binyuze muri Blueprint ye Komisiyo y'Umuremyi byashyizweho n'Abacuruzi, cyangwa kora verisiyo nshya y'iyi Blueprint ukayinjiza nk'isano muri Blueprint yawe kugira ngo musangire inyungu.