فنون
الجمال والعناية
حِرَف
الثقافة والتاريخ
ترفيه
البيئة
الطعام والمشروبات
الهندسة العكسية
العلوم
رياضة
التقنية
الأجهزة القابلة للارتداء
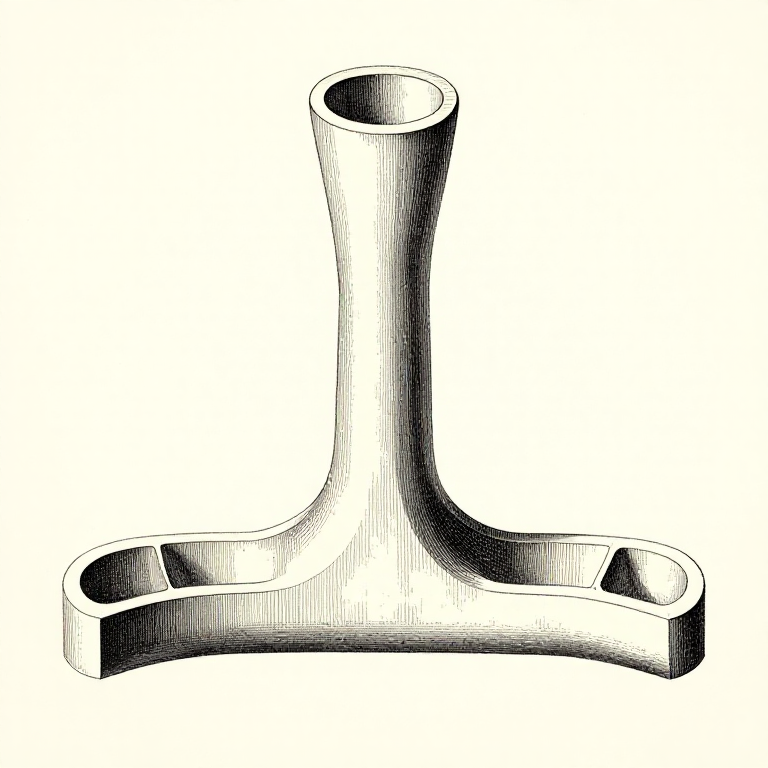


Gating: Getting the Metal In Without Wrecking the Mould
Molten metal poured straight into a cavity arrives fast, turbulent and full of air. It washes sand off the mould walls, folds oxide skin into itself, and the casting is full of inclusions before it has even frozen.
The GATING SYSTEM exists to prevent that. A sprue to take the metal down, a runner to carry it sideways and slow it, and gates to let it into the cavity smoothly — each part doing one job.
The governing principle is that the system should fill and stay full. A gating system running only partly full drags air in with the metal, which is precisely what it was built to avoid.
متقدم
3 hours
التعليمات
1
1
Sprue, runner, gate — three parts, three jobs
Sprue, runner, gate — three parts, three jobs
The SPRUE is the vertical channel the metal is poured into. It should be TAPERED, wider at the top, because falling metal accelerates and narrows — a parallel sprue leaves a gap around the stream that sucks in air.
The RUNNER is the horizontal channel at the bottom. It distributes metal and slows it down, and it is usually in the drag with the gates in the cope so that any floating dross stays in the runner.
The GATES are the small openings from runner into cavity. Several small gates fill more gently than one large one and let the mould fill from more than one place, which matters on anything long or thin.
المواد لهذه الخطوة:
 رمل السباكة1 كغ
الأدوات المطلوبة:
 صندوق سبك (علوي وسفلي)
 مسطرة
 قدمة رقمية 6 بوصات
2
2
Choke the system, and where
Choke the system, and where
جارٍ تحميل دفتر Jupyter…
المواد لهذه الخطوة:
 سبيكة برونز1 قطعةرمل السباكة1 كغ
الأدوات المطلوبة:
 حاسوب مكتبيقدمة رقمية 6 بوصاتصندوق سبك (علوي وسفلي)
3
3
Traps, filters and a pouring basin
Traps, filters and a pouring basin
A POURING BASIN at the top of the sprue lets you fill it and keep it full, so the sprue never runs empty mid-pour. Pouring straight into a bare sprue hole guarantees an interrupted, air-entraining stream at the start.
A runner extension beyond the last gate — a DIRT TRAP — gives the first, dirtiest metal somewhere to go that is not the casting. It costs a few centimetres of runner and catches the slag that came down the sprue first.
Ceramic foam FILTERS do the same job far better and are cheap. They also slow and smooth the flow, which is why a filter often improves a casting for two reasons at once.
المواد لهذه الخطوة:
رمل السباكة1 كغالأدوات المطلوبة:
صندوق سبك (علوي وسفلي)مسطرة مِغْرَفة دقيقة الشبك
4
4
Pour steadily and keep the basin full
Pour steadily and keep the basin full
Start the pour and bring the basin up to full quickly, then hold it there until the mould is full. A pour that starts timidly and then speeds up entrains air at the very start, which is the metal that ends up deepest in the casting.
Never stop and restart. A pause lets the stream break, lets air in, and can leave a COLD SHUT where the metal that stopped has skinned over before the rest arrives.
Have enough metal melted before you start. Running out halfway is the single most avoidable failure in a foundry, and it is prevented by weighing the pattern, multiplying by the alloy's density ratio, and adding a generous allowance for the gating and risers — which is usually a third of the total again.
المواد لهذه الخطوة:
سبيكة برونز1 قطعة فحم نباتي (قطع)1 قطعة
الأدوات المطلوبة:
 مِغرفة صبّ المعدن
 ملقط بوتقة
 نظارات داكنة للفرن
 قفازات جلدية طويلة الساعد
المواد
3- 1 كغعنصر نائب
- 1 قطعةعنصر نائب
- 1 قطعةعنصر نائب
الأدوات المطلوبة
9- عنصر نائب
- عنصر نائب
- عنصر نائب
- عنصر نائب
- عنصر نائب
- عنصر نائب
- عنصر نائب
- عنصر نائب
- عنصر نائب
المخططات ذات الصلة
هذه المخططات تشارك المعرفة مع هذا — التقنيات والمواد والمبادئ


CC0 ملكية عامة
هذا المخطط مُصدر بموجب CC0. يحق لك نسخه وتعديله وتوزيعه واستخدامه لأي غرض، دون طلب إذن.
ادعم الصانع بشراء منتجات عبر مخططه حيث يكسب عمولة الصانع يحددها البائعون، أو أنشئ نسخة جديدة من هذا المخطط وضمّنه كرابط في مخططك لمشاركة الإيرادات.