التعاون
فنون
الجمال والعناية
حِرَف
الثقافة والتاريخ
ترفيه
البيئة
الطعام والمشروبات
الهندسة العكسية
العلوم
رياضة
التقنية
الأجهزة القابلة للارتداء
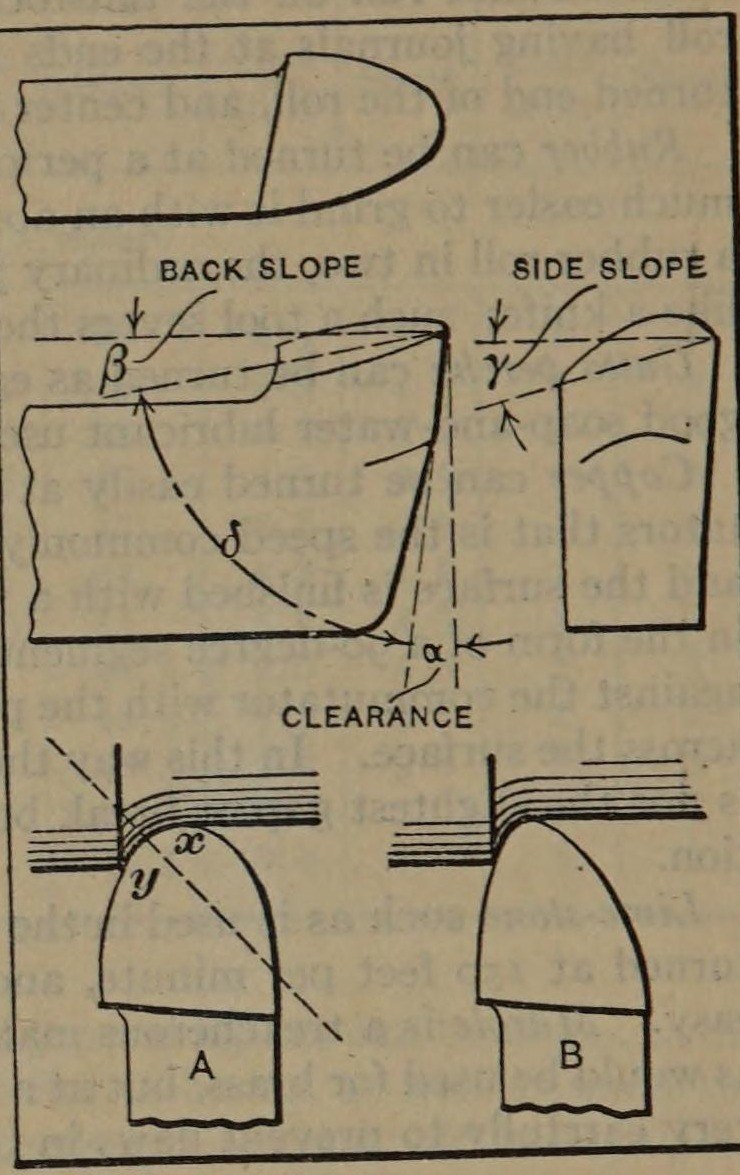


Lathe Cutting Tool: Ground to the Clearance and Slope for Each Metal (Machinery's Handbook, 1924)
A lathe turning tool ground from tool steel bar. Three things decide how well it cuts: the shape of the edge seen from above, the clearance under the edge, and the slope of the top the chip slides over. The Handbook gives the angles for each kind of metal to be turned.
Variable: the metal to be turned. Clearance 8 to 10° for general work, 12 to 14° for brass. Soft steel: back slope 8°, side slope 14 to 20°. Very hard steel: 5° and 9°. Brass: flat on top.
Source: Machinery's Handbook (1924), pp. 887-889, Tool Grinding. Unknown: the steel and the bar size. Picture: the Handbook's figure.
متوسط
Unknown
التعليمات
1
1
Choose the edge shape
Choose the edge shape
Grind the edge, seen from above, to suit the job. A large-radius edge roughs and keeps its edge at higher speed; a smaller point is better on flexible work that would chatter. A parting tool must be widest at the cutting edge so it does not bind in its groove. Ours: square tool steel bar. Not given: the steel, the bar size.
المواد لهذه الخطوة:
 قضيب مربّع من فولاذ العدد1 tool blank
الأدوات المطلوبة:
 حجر سنّ دوّار
 ماء
2
2
Grind the clearance and the slope
Grind the clearance and the slope
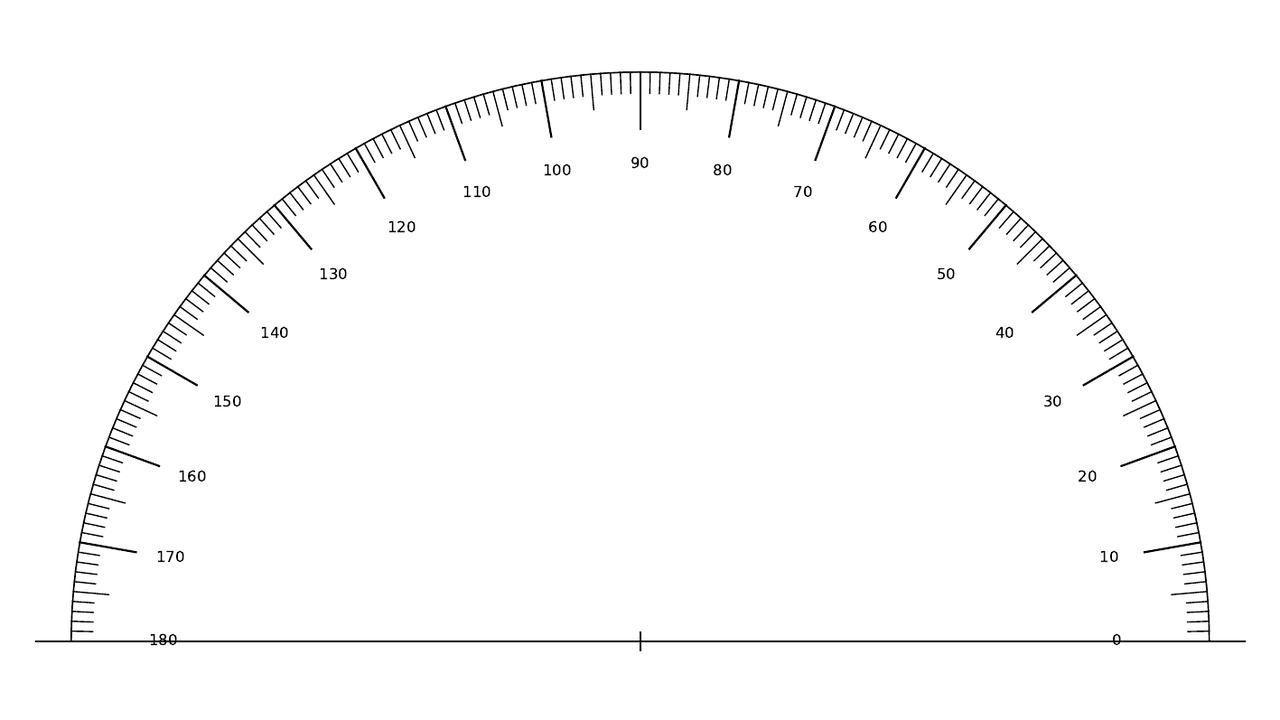
Grind clearance under the edge: 8 to 10° for general turning, 12 to 14° for brass and soft metals; too much weakens the edge. Slope the top away from the working part of the edge. A roughing tool for medium or soft steel gets a back slope of 8° and a side slope of 14 to 20°; for very hard steel, 5° and 9°. A broad finishing tool slopes straight back. Thread tools and tools for brass or chilled iron are flat on top; very hard metals get almost no slope and little clearance. Roughing tools cut fastest with a lip angle near 61°, but cast iron cuts better at about 68°.
الأدوات المطلوبة:
حجر سنّ دوّار منقلة
3
3
Grind without burning
Grind without burning
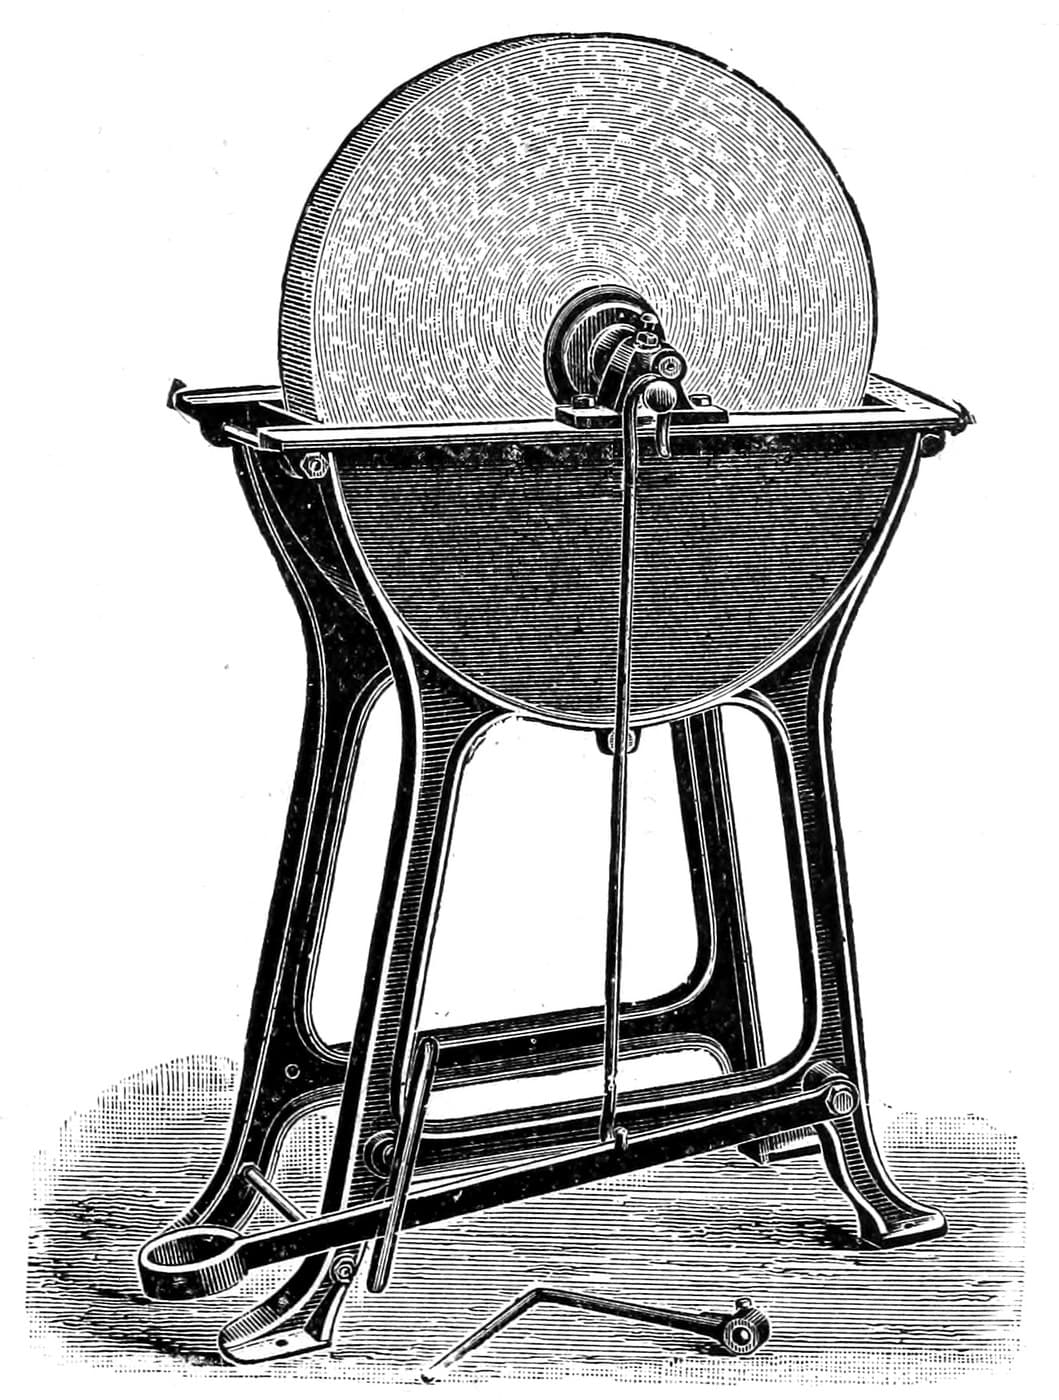
Press the tool only moderately against the wheel and draw it away often, especially when grinding a broad flat face, so the edge does not overheat and burn. Keep the wheel supplied with plenty of cooling water.
الأدوات المطلوبة:
حجر سنّ دوّارماءالمواد
1- 1 tool blankعنصر نائب
مواد المخططات المرتبطة

هذا المخطط يصنع

CC0 ملكية عامة
هذا المخطط مُصدر بموجب CC0. يحق لك نسخه وتعديله وتوزيعه واستخدامه لأي غرض، دون طلب إذن.
ادعم الصانع بشراء منتجات عبر مخططه حيث يكسب عمولة الصانع يحددها البائعون، أو أنشئ نسخة جديدة من هذا المخطط وضمّنه كرابط في مخططك لمشاركة الإيرادات.