التعاون
فنون
الجمال والعناية
حِرَف
الثقافة والتاريخ
ترفيه
البيئة
الطعام والمشروبات
الهندسة العكسية
العلوم
رياضة
التقنية
الأجهزة القابلة للارتداء
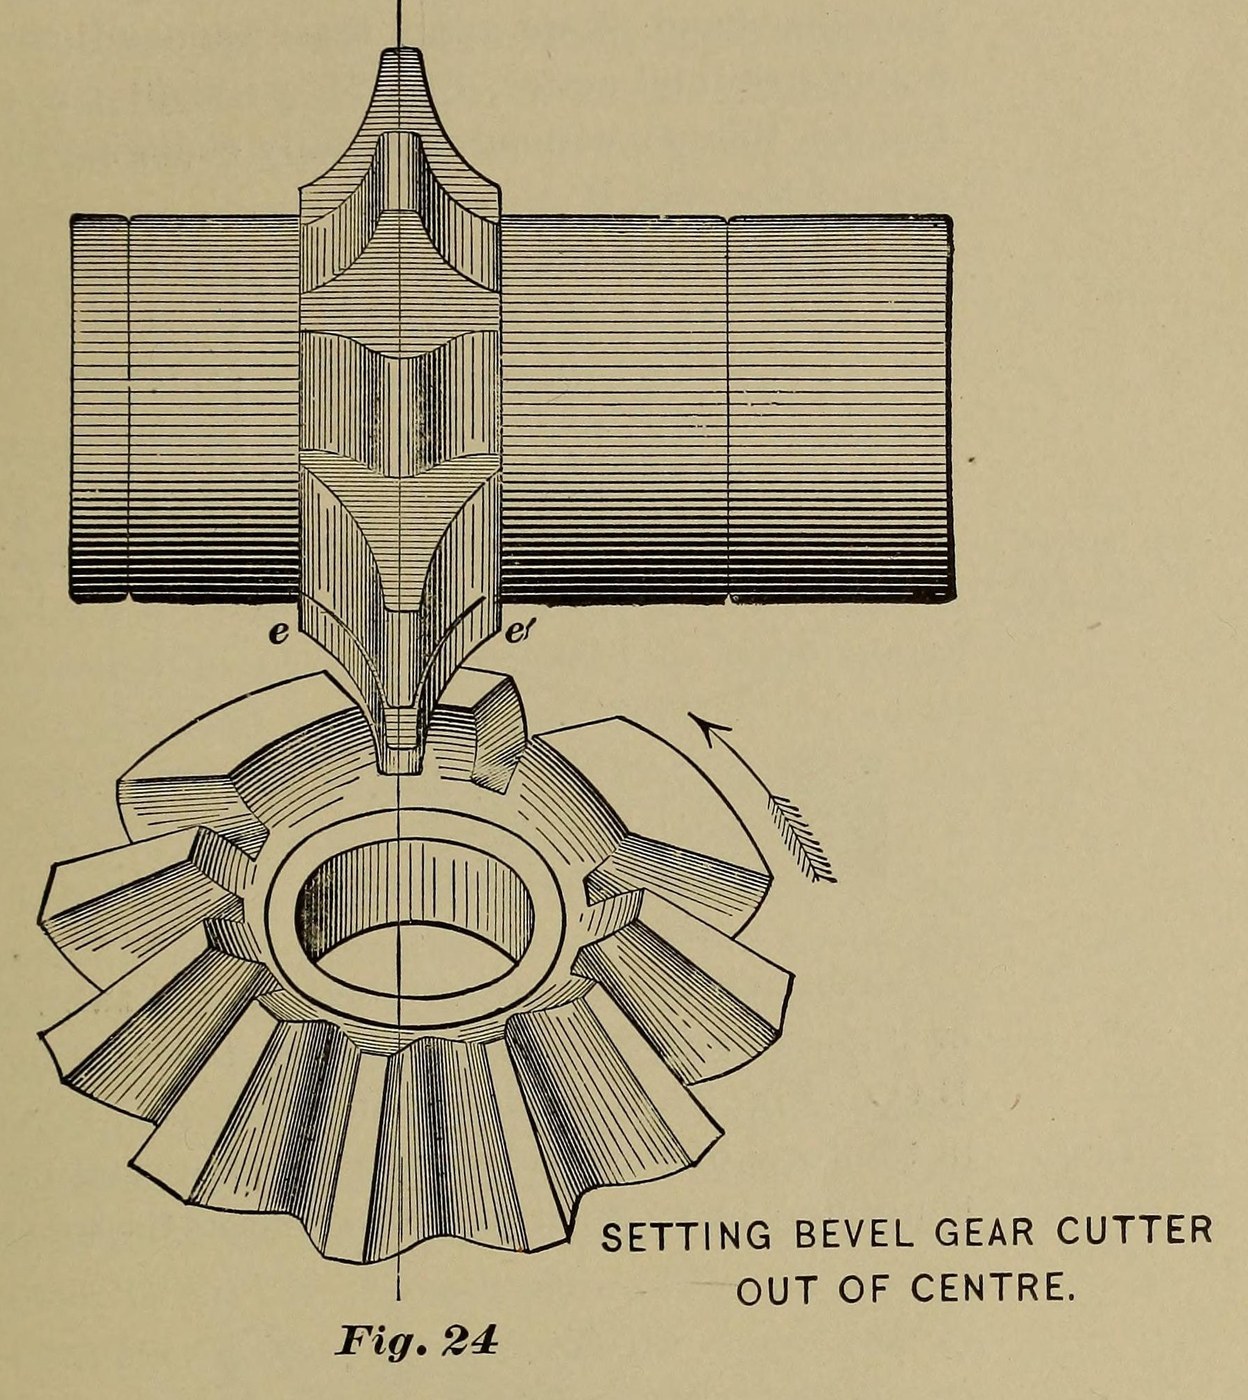


Mitre Gears: a 1:1 Bevel Pair Cut on the Milling Machine (Brown & Sharpe 1911)
Two equal bevel gears on shafts at right angles are mitre gears, and one cutter cuts both. A rotary cutter can only be right for one end of a bevel tooth, so Brown & Sharpe cut each space twice, set off centre to each side, then file the small ends round. Every figure here comes from their rules, worked out for a pair of 16 teeth, 8 pitch.
Source: Brown & Sharpe, Practical Treatise on Gearing (1911), Part I ch. IX–X and Part II ch. III; set-over table p. 58. The tooth count, pitch, face width, steel and bore are ours, and so is the arithmetic. Picture: Brown & Sharpe's Fig. 24.
متقدم
2 days
التعليمات
1
1
Work out and turn two blanks
Work out and turn two blanks
Ours: 16 teeth, 8 pitch, so pitch diameter 2.000 in. Mitre gears have a 45° centre angle (tangent 16/16). Diameter increment = cos 45° × working depth 0.250 = 0.177 in. Apex distance 1.414 in. Angle increment: tan = sin 45° ÷ 8, giving 5° 03′; cutting and face angle 45° − 5° 03′ = 39° 57′. Turn two blanks from steel to 2.18 in outside diameter, with the angle of edge 45° and the angle of face 39° 57′, tried with a protractor against the end of the hub. Face length ⅜ in (ours; no more than a third of the 1.414 in apex distance). Bore and hub are ours.
المواد لهذه الخطوة:
 قضيب فولاذ طري1 length for two blanks
الأدوات المطلوبة:
 مخرطة معادن
 عدّة قطع للمخرطة
 منقلة
 ميكرومتر
2
2
Choose the cutter
Choose the cutter
Back cone radius 1.414 in: twice that × 8 pitch = 22.6 teeth, so a No. 5, 8-pitch bevel gear cutter (21 to 25 teeth). One cutter does both gears. Measure its thickness Tc at the pitch line, 0.145 in (1.157 ÷ 8) from its tip.
الأدوات المطلوبة:
 فريزة التروس المخروطية
 قدمة ورنية لأسنان التروس
3
3
Set the head and the depth
Set the head and the depth
Mount the blank on the dividing head, set to the cutting angle of 39° 57′, to index 16 spaces. Set the depth at the large end to the working depth plus clearance, 0.270 in. Clearance stays the same at the small end.
الأدوات المطلوبة:
 آلة التفريز
 رأس التقسيمفريزة التروس المخروطية
4
4
Set over and cut one side of every tooth
Set over and cut one side of every tooth
Set-over: apex distance ÷ face = 1.414 ÷ 0.375 = 3.77, so use the 3¾ column, where a No. 5 cutter has the factor .293. Set-over = Tc ÷ 2 − .293 ÷ 8 = Tc ÷ 2 − 0.037 in. Set the work off centre by that amount to one side, taking up backlash. Run the cutter through, indexing round all 16 spaces.
الأدوات المطلوبة:
آلة التفريزرأس التقسيمفريزة التروس المخروطية5
5
Set over the other way and trim to thickness
Set over the other way and trim to thickness
Set over by the same amount on the other side of centre and rotate the blank to line the cutter up with the space at the small end. Take a trial cut, then rotate the blank toward the cutter until the tooth is right: 0.196 in thick at the large end and 0.144 in at the small end. Check both ends with the gear tooth vernier. Right at the large end but thick at the small end means too much set-over; the other way round, too little.
الأدوات المطلوبة:
آلة التفريزرأس التقسيمفريزة التروس المخروطيةقدمة ورنية لأسنان التروس6
6
Cut round, then make the second gear
Cut round, then make the second gear
Cut the second side of every tooth with that setting. Cut the second blank the same way with the same cutter.
الأدوات المطلوبة:
آلة التفريزرأس التقسيمفريزة التروس المخروطية7
7
File the small ends
File the small ends
Round the teeth over at the small ends with a file, where the cutter could not. Do not file them thinner at the pitch line.
الأدوات المطلوبة:
 مبرد ناعم
المواد
1- 1 length for two blanksعنصر نائب
هذا المخطط يصنع

CC0 ملكية عامة
هذا المخطط مُصدر بموجب CC0. يحق لك نسخه وتعديله وتوزيعه واستخدامه لأي غرض، دون طلب إذن.
ادعم الصانع بشراء منتجات عبر مخططه حيث يكسب عمولة الصانع يحددها البائعون، أو أنشئ نسخة جديدة من هذا المخطط وضمّنه كرابط في مخططك لمشاركة الإيرادات.