ศิลปะ
ความงามและสุขภาพ
งานฝีมือ
วัฒนธรรมและประวัติศาสตร์
ความบันเทิง
สิ่งแวดล้อม
อาหารและเครื่องดื่ม
วิศวกรรมย้อนรอย
วิทยาศาสตร์
กีฬา
เทคโนโลยี
อุปกรณ์สวมใส่
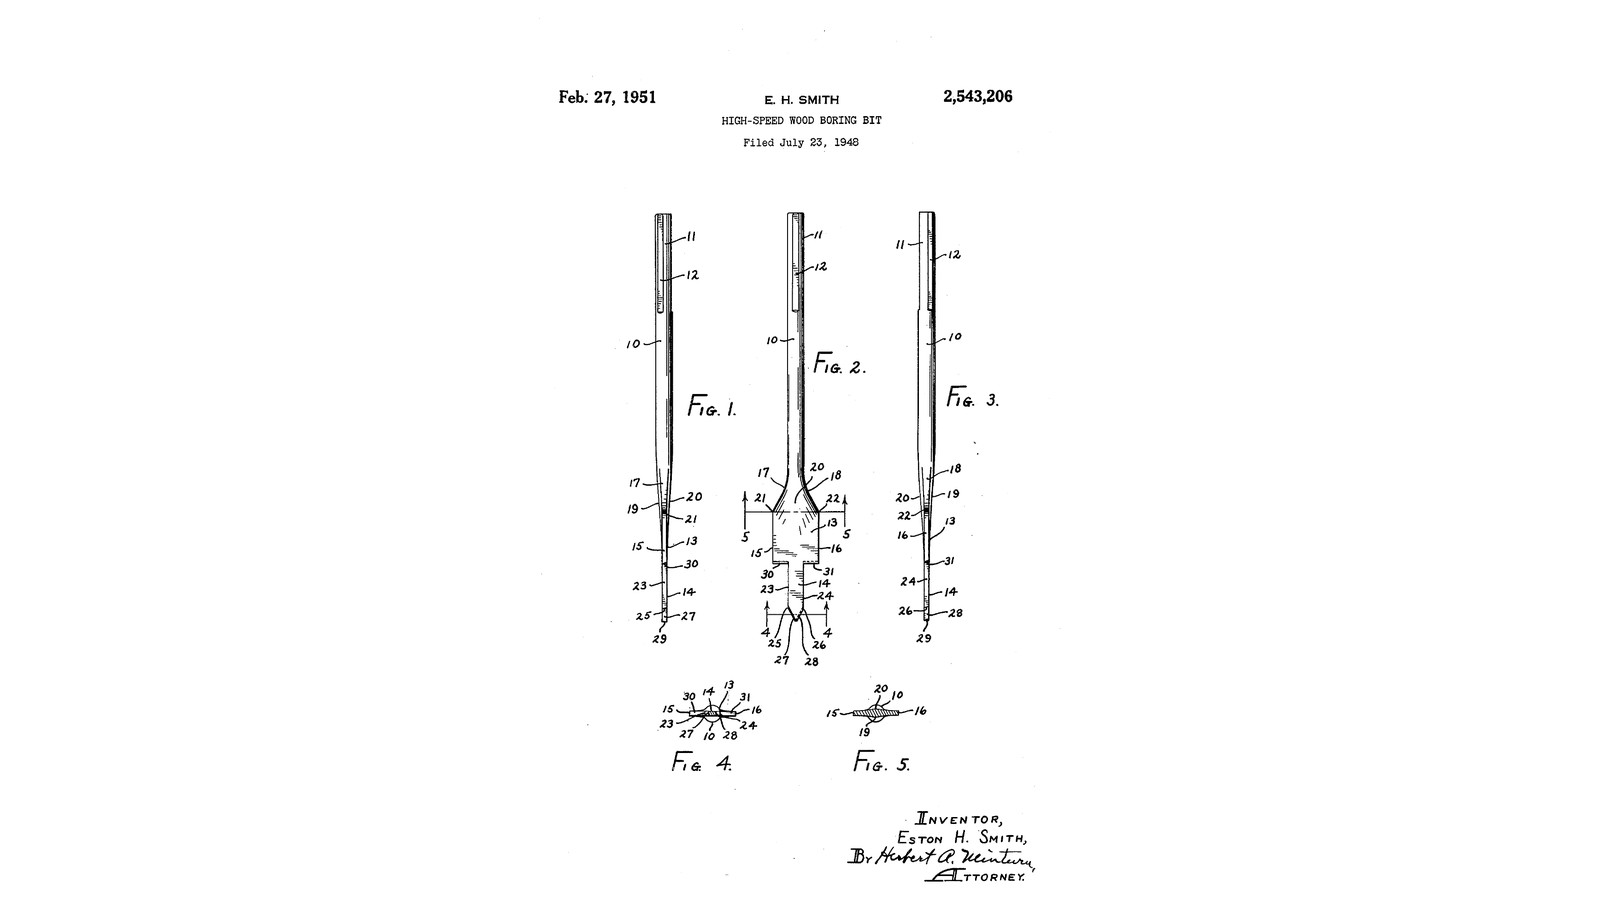


Long-Pilot High-Speed Wood Bits: A Flat Plate and a Long Square-Edged Pilot, No Screw Feed (Smith, 1951)
Eston H. Smith of Indianapolis received US 2,543,206, dated 27 February 1951, for a flat wood-boring bit made for the high speeds of an electric drill, 2,000 to 3,500 revolutions a minute. A flat plate on a thin stem has edges square to its faces and exactly the same width all the way down. A long flat pilot below it keeps the bit centred until it is through. With no screw feed it can bore at an angle, into another hole, or overlapping one, without splitting the wood. The thin stem leaves room for the shavings to come out.
We forge his 3/4 inch bit to his figures, with 1/2 and 1 inch bits beside it.
ระดับกลาง
About 1 day
คำแนะนำ
1
1
His figures in millimetres
His figures in millimetres
กำลังโหลดสมุด Jupyter…
2
2
Read US 2,543,206
Read US 2,543,206
"It is extremely important however that these edges 15 and 16 be of exactly constant width from top to bottom, else the holes will not be bored true, and chattering and heating might develop."
3
3
Forge the blades
Forge the blades
Cut three 170 mm lengths of 10 mm octagonal tool steel. Heat 50 mm of one end to a bright orange in the forge and flatten it on the anvil to about 3 mm thick, centred on the bar. Hammer across it with the peen to spread it wider than the bit, about 2 mm over its size: 15, 21 and 27 mm. Draw the neck down smoothly where the blade meets the bar and keep the blade in line with it. Reheat as soon as the colour fades to red. Finally heat each one to a cherry red and let it cool slowly in the air, to soften it for filing.
วัสดุสำหรับขั้นตอนนี้:
 เหล็กเครื่องมือแปดเหลี่ยม3 ชิ้น
เครื่องมือที่ต้องใช้:
 เลื่อยตัดเหล็ก
 ปากกาจับชิ้นงานหน้าโต๊ะ
 เตาตีเหล็ก
 ทั่ง
 ค้อนตีเหล็ก
 คีมช่างตีเหล็ก
 ถุงมืองานเชื่อม
 แว่นนิรภัย
4
4
Print the grinding template
Print the grinding template
Full-size A4 template: the outlines of the 1/2, 3/4 and 1 inch bits with the long flat pilot. Print at 100 %; its 50 mm bar must measure 50 mm.
5
5
Grind the outline
Grind the outline
Glue each outline on its blade, centred on the bar, and grind to the lines on the bench grinder, dipping the steel in water often. Grind the faces flat and parallel to 2.4 mm (3/32 inch). Grind the plate's two side edges and the pilot's two side edges square to the faces and exactly parallel; check the plate's width with the caliper at the top and the bottom, it must not change. Grind three flats on the end of the stem, 20 mm long, for the chuck's jaws.
เครื่องมือที่ต้องใช้:
 เครื่องพิมพ์อิงก์เจ็ต
 กาว
 เครื่องเจียรตั้งโต๊ะ
 ถังชุบน้ำ
 น้ำ
 ชุดตะไบปากกาจับชิ้นงานหน้าโต๊ะ
 เวอร์เนียร์ดิจิทัล 6 นิ้วแว่นนิรภัย
6
6
Grind the clearances
Grind the clearances
The bit turns clockwise seen from the stem. Grind each cutting edge either side of the pilot square to the axis, with no top rake, and a clearance of 15 degrees behind it, on the face that trails. Grind the pilot's two point edges to 58 degrees included and give each a clearance of 9 degrees the same way. Leave a 1 mm flat at the tip, square to the axis.
เครื่องมือที่ต้องใช้:
เครื่องเจียรตั้งโต๊ะถังชุบน้ำน้ำชุดตะไบปากกาจับชิ้นงานหน้าโต๊ะ7
7
Harden and temper
Harden and temper
Heat the blade and the neck evenly to a cherry red, until a magnet no longer sticks to it, and quench it straight down in water, moving it up and down. Rub the faces bright with a stone. Heat the shank gently 30 mm behind the blade and watch the colours run down; quench again as soon as a dark straw colour reaches the shoulders and the point. Do the other two.
เครื่องมือที่ต้องใช้:
เตาตีเหล็กคีมช่างตีเหล็ก แม่เหล็กเล็กถังชุบน้ำน้ำ
 หินลับมีดถุงมืองานเชื่อมแว่นนิรภัย
8
8
Sharpen and test
Sharpen and test
Hone the cutting edges on the shoulders and the point with the stone, keeping their angles, and take the burr off. Chuck a bit by its flats and bore a scrap of hardwood: it should start on the point without wandering, cut two clean shavings from the shoulders and leave a round hole of its own size; check it with the caliper.
เครื่องมือที่ต้องใช้:
หินลับมีด สว่านไร้สาย
 แผ่นไม้เนื้อแข็งเวอร์เนียร์ดิจิทัล 6 นิ้วแว่นนิรภัย
9
9
Troubleshooting
Troubleshooting
Long-pilot bit troubleshooting.
Flow
Loading...
10
10
History and honest limits
History and honest limits
**Eston H. Smith** of Indianapolis, assignor to Benjamin B. Aufderheide, US 2,543,206, dated 27 February 1951, filed 23 July 1948. He claimed a flat plate on a stem with a flat pilot, their edge faces at ninety degrees to their faces, a pilot point of 55 to 60 degrees with 8 to 10 degree clearances, and cutting edges square to the pilot with a clearance of between 15 and 20 degrees (his text says 10 to 20). His figures are for the 3/4 inch bit; the 1/2 and 1 inch bits are ours, with his pilot and edge height. His stem is about 1/4 inch with flats; ours is octagonal tool steel with three ground flats. He gives no material or heat treatment; those are ours.
วัสดุ
1- ตัวยึดตำแหน่ง
เครื่องมือที่จำเป็น
19- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
- 1 vendor sell this, none ship to you yetตัวยึดตำแหน่ง
- ตัวยึดตำแหน่ง
ไฟล์ออกแบบ
1พิมพ์เขียวนี้สร้าง

บลูพริ้นท์ที่เกี่ยวข้อง
บลูพริ้นท์เหล่านี้แบ่งปันความรู้ — เทคนิค วัสดุ หรือหลักการ
CC0 สาธารณสมบัติ
พิมพ์เขียวนี้เผยแพร่ภายใต้ CC0 คุณสามารถคัดลอก แก้ไข แจกจ่าย และใช้งานผลงานนี้เพื่อวัตถุประสงค์ใดก็ได้ โดยไม่ต้องขออนุญาต
สนับสนุนเมกเกอร์โดยซื้อสินค้าผ่านพิมพ์เขียวของพวกเขา ซึ่งพวกเขาจะได้รับ ค่าคอมมิชชันเมกเกอร์ ที่ผู้ขายกำหนด หรือสร้างเวอร์ชันใหม่ของพิมพ์เขียวนี้และรวมเป็นการเชื่อมต่อในพิมพ์เขียวของคุณเพื่อแบ่งรายได้