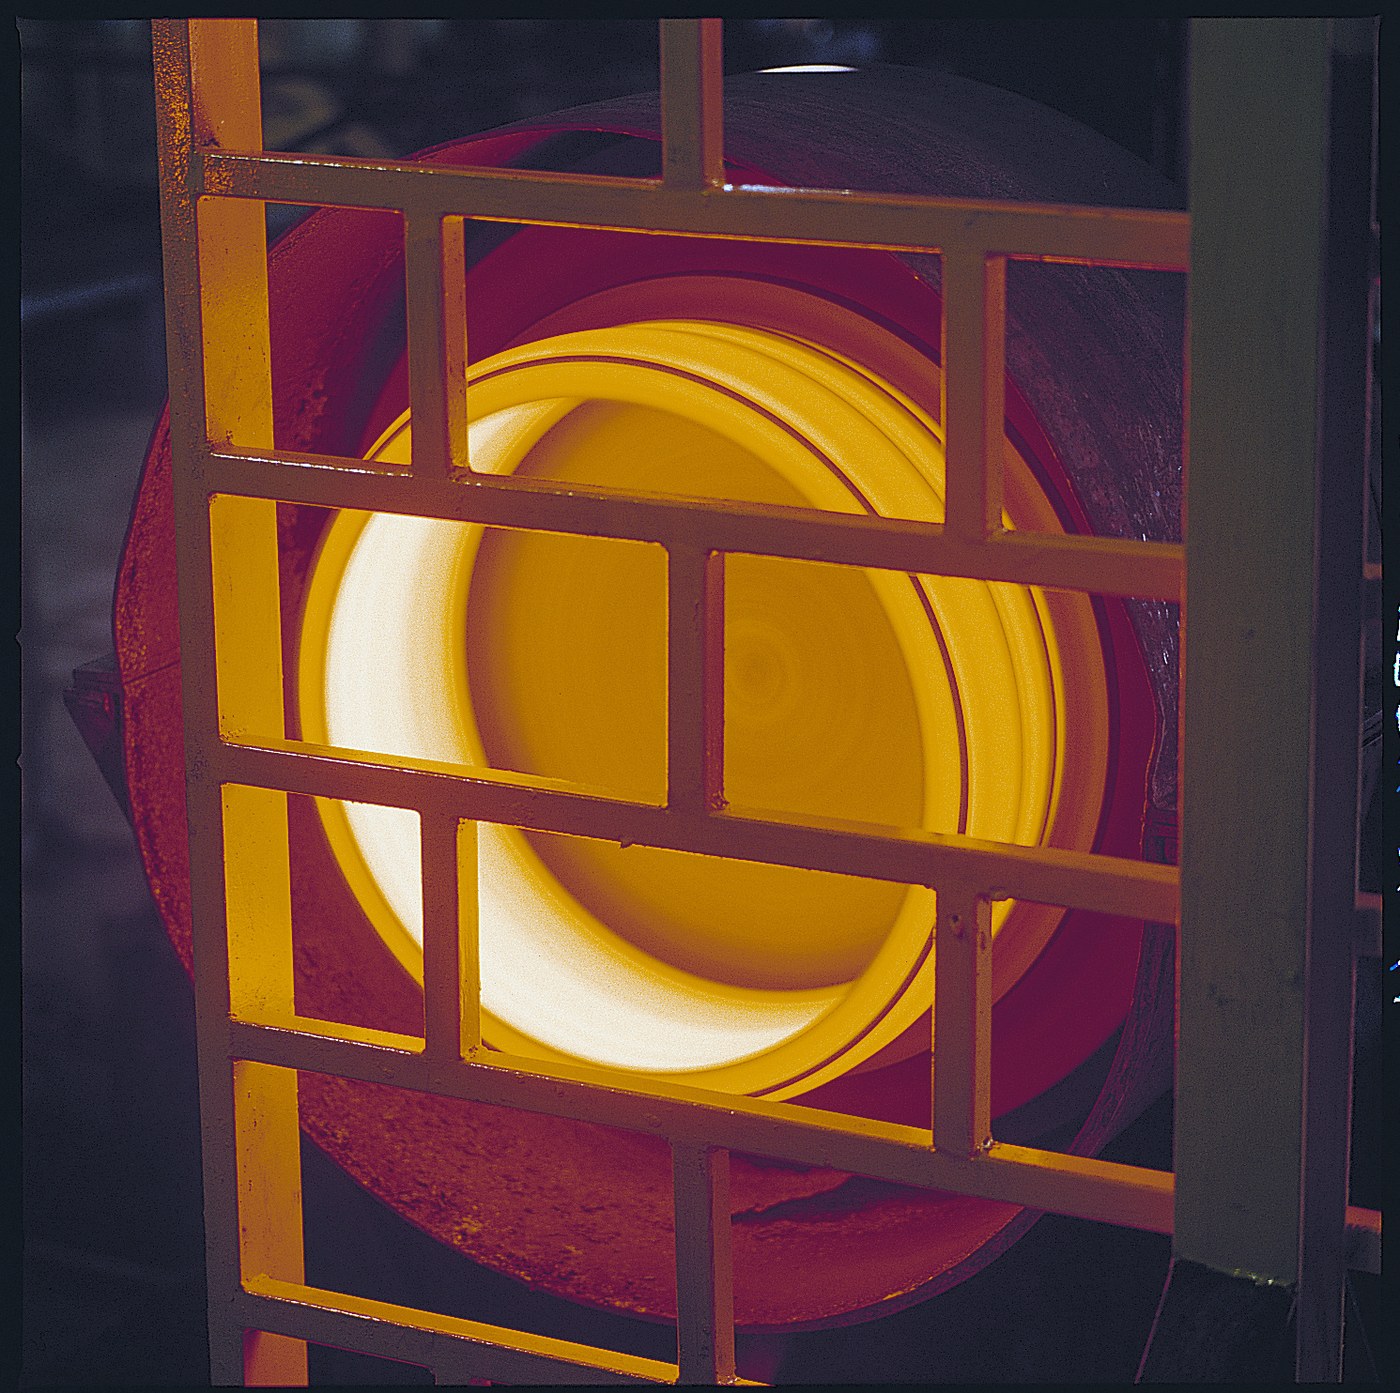

Centrifugal Casting
Talimatlar
Build the spinning mould and its guard
Build the spinning mould and its guard
Molten metal at speed demands a containment you would trust with your hands off it.
- Make a cylindrical steel mould, 100 mm bore and 200 mm long, closed at one end.
- Mount it on a shaft in two 608 bearings, balanced as well as you can manage.
- Build a FULL enclosure around it — a steel drum or thick plywood box lined with sheet metal.
- Drive it with a belt from a motor placed outside the enclosure.
- Fit a pouring chute that reaches through the guard, so nobody's hands go near the spinning mould.
Balance is a safety requirement here, not a refinement. An unbalanced mould at speed shakes the whole rig, and the failure mode is molten metal leaving the machine. Spin it up empty to full speed first and watch it; if it vibrates, fix that before any metal is melted.
Coat the mould bore with a refractory wash before each pour. It protects the mould, controls the cooling rate, and lets the casting release — a steel mould with bare metal inside will weld itself to the casting.Bu adım için malzemeler:
 Demir pota1 adet
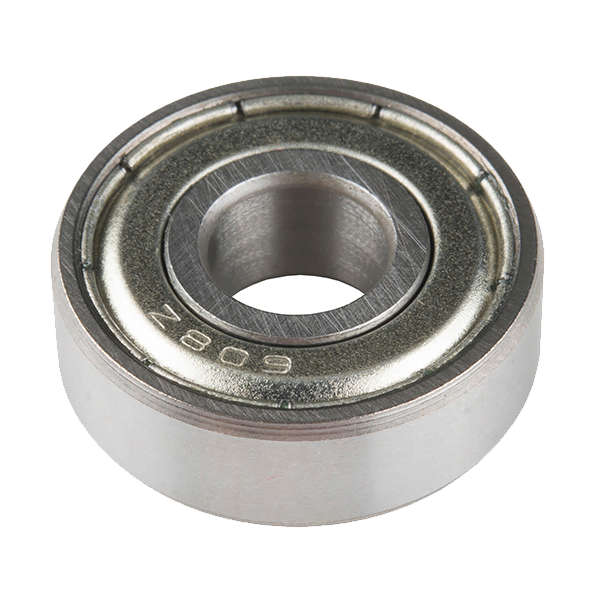 Ball Bearing - Non-Flanged (8mm Bore, 22mm OD)2 adet
 Baltık Huş Kontrplak1 yaprak
 Düz Pul8 adet
 Altıgen Somun4 adet
Gerekli aletler:
 Kablosuz Matkap
 Matkap Ucu Takımı
 Dekupaj Testere
 Alyan Anahtar Takımı
 Dijital Kumpas 6 İnç
 Kombine Gönye
Work out the speed you actually need
Work out the speed you actually need
Too slow and the metal rains down the inside instead of clinging.
- The requirement is that centrifugal acceleration at the bore exceeds gravity by a comfortable margin — aim for 60 to 80 times g.
- Acceleration = (2πn/60)² × r, with n in revolutions per minute and r the bore radius in metres.
- For a 50 mm radius and 70g, solve for n — around 1100 rpm.
- Check your drive can reach and hold that under load.
- Mark the calculated speed on the rig.
Below the threshold the casting fails visibly. Metal that is not held firmly against the wall slumps and freezes in a crescent, thick at the bottom and thin at the top — a phenomenon called raining. That is the direct evidence that centrifugal force is doing the mould's job, and it is why the speed calculation is done before the melt rather than after.
Higher is not automatically better: excessive speed can crack the solidifying shell as it contracts against a mould that will not yield. The band between raining and cracking is the operating window.Bu adım için malzemeler:
 Milimetrik Kağıt1 pad
Gerekli aletler:
 KronometreDijital Kumpas 6 İnç
Pour a spinning mould
Pour a spinning mould
Steady, into a mould already at speed.
- Bring the mould to full speed before any metal is poured.
- Melt the charge — pewter, aluminium or lead for a demonstration.
- Pour steadily down the chute; the metal will climb the wall as it enters.
- Keep spinning until the casting has fully solidified, then let it slow.
- Extract the casting once cool.
Wall thickness is set by volume alone. There is no core and no inner mould surface: pour more metal and the wall is thicker with a smaller bore, pour less and the reverse. The outer diameter is fixed by the mould, the inner is chosen at the ladle — a degree of freedom no other casting method offers.
Never slow the mould before solidification. A partly frozen casting that stops spinning slumps immediately, and the result is a lopsided ring welded to one side of the mould.Bu adım için malzemeler:
 Ham kurşun külçesi (galen izabesinden)1 ingot
 Grafit-kil pota1 adet
Gerekli aletler:
 Pota MaşasıKronometreDijital Kumpas 6 İnç
Section it and find where the impurities went
Section it and find where the impurities went
The metallurgical benefit is visible on a cut face.
- Cut a ring from the casting and polish one face.
- Etch it lightly and examine from bore to outer surface.
- Look for porosity, inclusions and dross concentrated near the BORE.
- Compare with a section from a conventionally sand-cast piece of the same alloy.
- Machine the bore out by a couple of millimetres and re-examine.
Gerekli aletler:
 Demir Testeresi Gövdesi ve Ağızları
 Eğe TakımıDijital Kumpas 6 İnç
 Tezgah Mengenesi
The mould you do not have to make, and history
The mould you do not have to make, and history
Dimitri Sensaud de Lavaud developed centrifugal casting into an industrial pipe process around 1918 in Brazil, and the de Lavaud process is still the name used for making ductile iron water pipe. Earlier patents for spinning moulds date back to the nineteenth century, but making it work reliably at production scale is what mattered.
The idea is the same family as the shot tower at the start of this batch. Both let a physical force do work that would otherwise need tooling: surface tension makes the sphere, centrifugal force makes the bore. Neither needs a mould surface for the shape it produces, and both therefore have nothing to wear out on that surface. When a force already produces the geometry you want, the cheapest process is the one that gets out of its way.
Against the other tube processes in this batch: extrusion needs a die and a mandrel and leaves weld lines; Mannesmann piercing needs a ductile billet and makes only round sections; centrifugal casting works directly from melt with no core and gives excellent outer-surface metal — but only for shapes that are surfaces of revolution, and only where a machined bore is acceptable.
Its honest limits: rotational symmetry only; a bore that is rough and impurity-rich and must be machined; segregation of alloying elements by density, which can be a defect as easily as a benefit; and a machine that is genuinely dangerous, since it combines high speed with molten metal. The guard in step 1 is the most important part of the build.
Malzemeler
8- 1 adetYer Tutucu
- Ball Bearing - Non-Flanged (8mm Bore, 22mm OD)%10 komisyon2 adet$1.26
- 1 yaprakYer Tutucu
- 8 adetYer Tutucu
- 4 adetYer Tutucu
- 1 padYer Tutucu
- Yer Tutucu
- 1 adetYer Tutucu
Gerekli Aletler
11- 1 vendor sell this, none ship to you yetYer Tutucu
- Yer Tutucu
- 1 vendor sell this, none ship to you yetYer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
İlgili Blueprint'ler
Bu blueprint'ler bilgi paylaşır — teknikler, malzemeler veya ilkeler


CC0 Kamu Malı
Bu plan CC0 lisansıyla yayınlanmıştır. İzin almadan kopyalayabilir, değiştirebilir, dağıtabilir ve herhangi bir amaçla kullanabilirsiniz.
Planı üzerinden ürün satın alarak Maker'ı destekleyin, böylece Maker Komisyonu Satıcılar tarafından belirlenen komisyonu kazanırlar veya bu Planın yeni bir versiyonunu oluşturun ve gelir paylaşımı için kendi Planınıza bağlantı olarak ekleyin.