SANAT
GÜZELLİK & SAĞLIK
ZANAAT
KÜLTÜR & TARİH
EĞLENCE
ÇEVRE
YİYECEK & İÇECEK
TERS MÜHENDİSLİK
BİLİMLER
SPOR
TEKNOLOJİ
GİYİLEBİLİR ÜRÜNLER
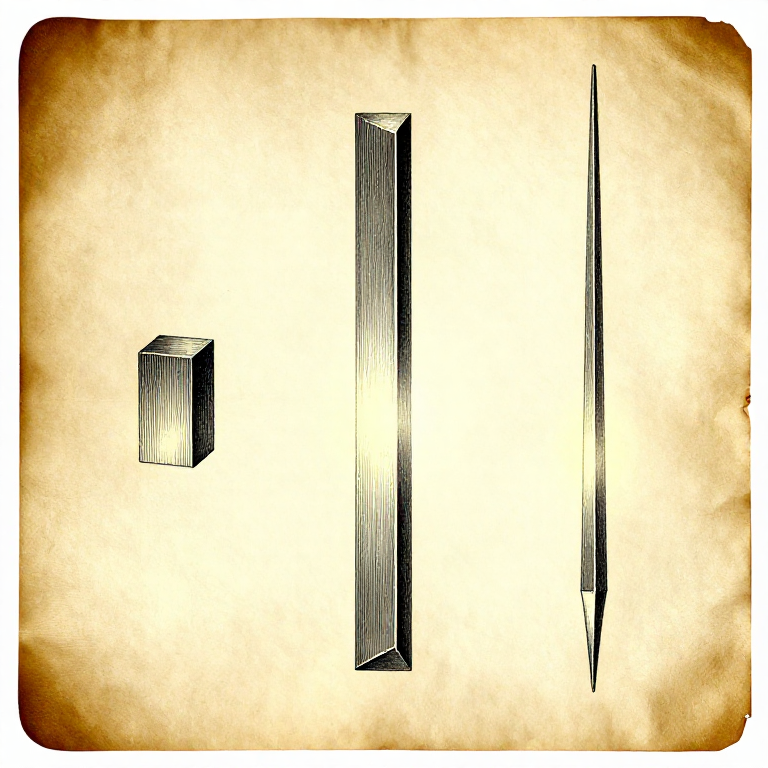

Drawing Out: Making It Longer by Making It Thinner
Drawing out is the commonest forging operation: making a bar longer and thinner. A taper, a blade, a spike, a leaf — all of them are drawn out.
The metal is not compressed; it is MOVED. Volume is conserved, so everything that leaves the thickness has to appear somewhere in the length and the width. Controlling which of those two it goes into is the whole skill.
The trick that makes it fast is counter-intuitive: hitting a smaller area moves metal quicker than hitting a large one, because the pressure is higher. That is why a smith reaches for the horn or a fuller rather than flattening away on the face.
Orta
3 hours
Talimatlar
1
1
Volume is conserved — so plan the stock first
Volume is conserved — so plan the stock first
Jupyter defteri yükleniyor…
Bu adım için malzemeler:
 Yumuşak çelik lama1 adet
Gerekli aletler:
 Hesap Makinesi
 Cetvel
2
2
Work over the horn or the edge, not the flat
Work over the horn or the edge, not the flat
Hammering a bar on the flat face squashes it wider as much as longer. Lay it across the horn or over the radiused edge of the anvil and the contact patch shrinks, the pressure rises, and the metal is forced to flow along the bar.
A FULLER does the same thing deliberately: a rounded tool, top or bottom, that concentrates the blow into a narrow band. Fullering a series of grooves and then flattening them out draws metal far faster than direct hammering.
This is the single biggest difference between a beginner who is exhausted after twenty minutes and a smith who is still going. It is not strength — it is choosing a smaller contact patch.
Bu adım için malzemeler:
Yumuşak çelik lama1 adet Parça Odun Kömürü1 adet
Gerekli aletler:
 Örs
 Fuller (oluk açma demiri)
 Fuller aleti
 Demirci çekici
3
3
Turn it 90 degrees every few blows
Turn it 90 degrees every few blows
Draw a square bar by hammering one face, turning a quarter turn, hammering again, and repeating. Keep it square as it gets smaller, then round it at the end if you want round.
Hammering only one face makes a flat strip, and once it has spread sideways it is very hard to get back. The quarter-turn habit is what keeps a taper square and even, and it is worth counting blows out loud while you learn it.
To go from square to octagonal to round: knock the four corners off the square to make an octagon, then roll it under light blows to round it. Trying to go straight from square to round leaves flats that never quite disappear.
Bu adım için malzemeler:
Yumuşak çelik lama1 adetGerekli aletler:
Demirci çekiciÖrs Demirci kerpeteni
 Yuvarlatma çekici
4
4
Work the hot part, and stop when it dulls
Work the hot part, and stop when it dulls
Metal only moves where it is hot. As a heat fades, the thin end cools first and stops moving while the thick part is still workable, which is exactly the surface-to-volume effect the heating rung describes.
So work the hottest region and go back to the fire before the colour drops out of the forging range. Hammering steel that has gone below red achieves almost nothing, work-hardens it, and can crack it.
Plan what you will do with each heat before it comes out of the fire. Three deliberate operations per heat is a good working rhythm; one operation and back in the fire wastes fuel and costs scale on every trip.
Bu adım için malzemeler:
Yumuşak çelik lama1 adetParça Odun Kömürü2 adetGerekli aletler:
 Demirci ocağıDemirci kerpeteniDemirci çekici
 Koyu camlı ocak gözlüğü
Gerekli Aletler
10- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
İlgili Blueprint'ler
Bu blueprint'ler bilgi paylaşır — teknikler, malzemeler veya ilkeler
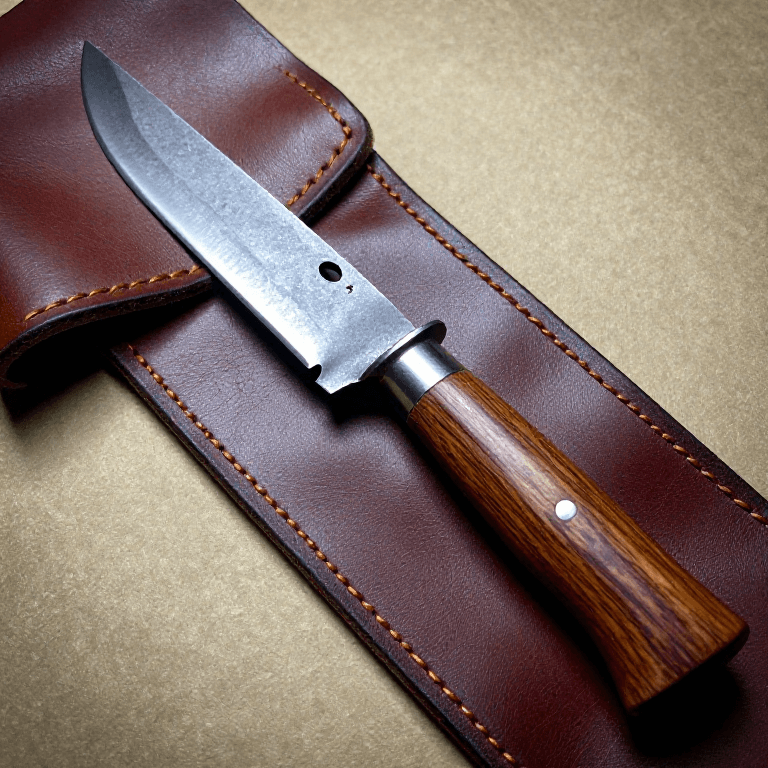
Forging an Iron Knife from a Wrought Iron Bar — The Smith's First Project
Forge tarafından
Metal işleme
50
0
0
0
0
0
Heating Evenly: Why Thin Bits Burn While Thick Bits Are Still Cold
Forge tarafından
Metal işleme
22
0
0
0
0
0
Reading Heat by Colour: The Oldest Thermometer, and Its Two Conditions
Forge tarafından
Metal işleme
20
0
0
0
0
0
CC0 Kamu Malı
Bu plan CC0 lisansıyla yayınlanmıştır. İzin almadan kopyalayabilir, değiştirebilir, dağıtabilir ve herhangi bir amaçla kullanabilirsiniz.
Planı üzerinden ürün satın alarak Maker'ı destekleyin, böylece Maker Komisyonu Satıcılar tarafından belirlenen komisyonu kazanırlar veya bu Planın yeni bir versiyonunu oluşturun ve gelir paylaşımı için kendi Planınıza bağlantı olarak ekleyin.