
İşbirliği
SANAT
GÜZELLİK & SAĞLIK
ZANAAT
KÜLTÜR & TARİH
EĞLENCE
ÇEVRE
YİYECEK & İÇECEK
TERS MÜHENDİSLİK
BİLİMLER
SPOR
TEKNOLOJİ
GİYİLEBİLİR ÜRÜNLER
Forge Blast Fan: Riveted Sheet-Iron Drum, Shrunk-Collar Spindle and Four Screwed Blades, Belt-Driven at 360 rpm (Edwinson, 1886)
Forge

Oluşturan

Forge

14. Kasım 2026NO
9
0
0
0
0

Forge Blast Fan: Riveted Sheet-Iron Drum, Shrunk-Collar Spindle and Four Screwed Blades, Belt-Driven at 360 rpm (Edwinson, 1886)

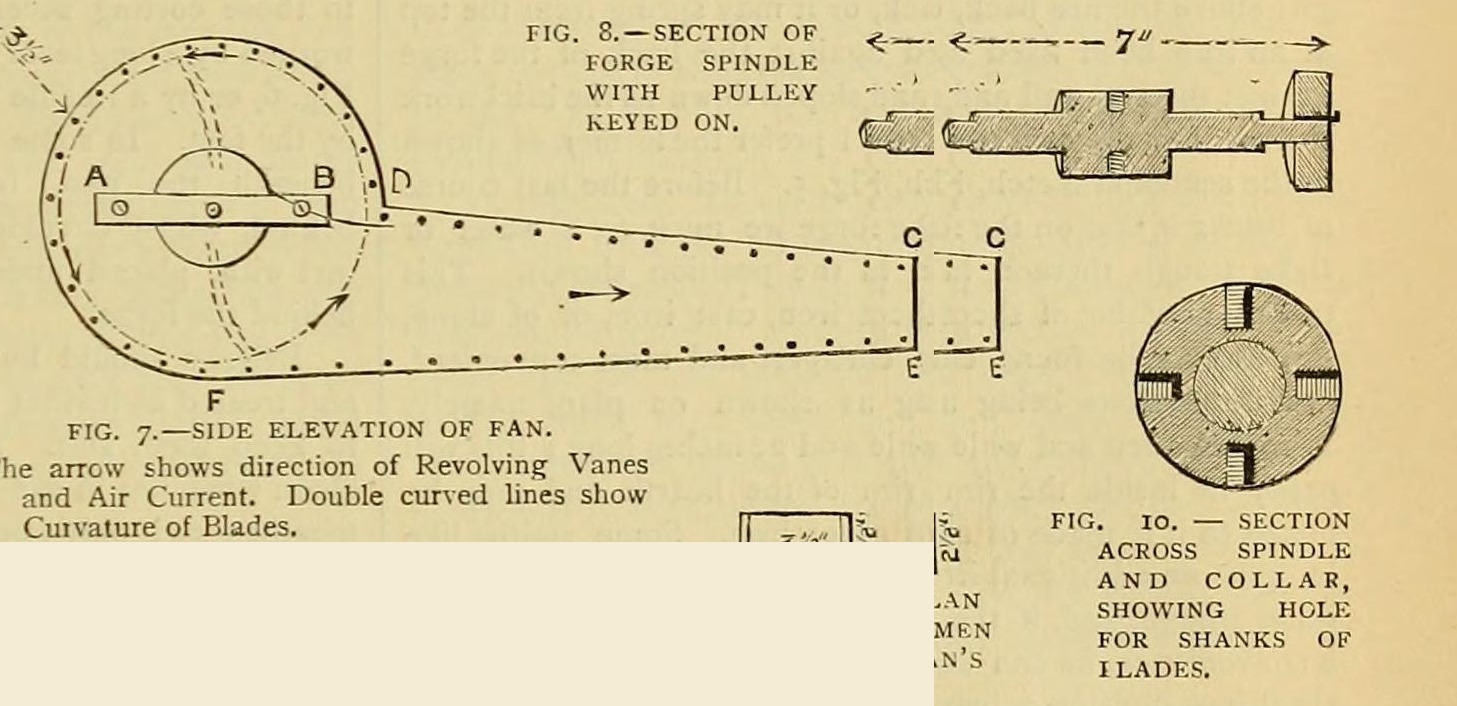
George Edwinson's home-made forge fan (Amateur Work, 1886), which he preferred to bellows: two 1/8 in. sheet-iron sides with a 3 1/2 in. intake, a riveted 1/16 in. casing, a turned 3/4 in. spindle with a shrunk-on collar holding four forged, slightly scooped blades, brass bearings, and a 2 in. pulley driven from a 2 ft hand wheel at 30 rpm for 360 rpm.
İleri
Three to four days

Talimatlar

1

His sizes

Jupyter defteri yükleniyor…
2

Read Edwinson

"Under no circumstances should I advise an amateur to make his own bellows, but he may be able to make a fan."
3

Cut the sides

Cut two sides from 1/8 in. sheet iron to his fig. 7: 9 in. across at the widest, 2 1/2 in. at the narrowest, 2 ft long. Cut a 3 1/2 in. hole in each for the spindle and air intake, drill two 3/8 in. holes for bolts A and B (filed square), and drill the rivet holes round the edge.

Bu adım için malzemeler:

Yumuşak Çelik SacYumuşak Çelik Sac1 adet

Gerekli aletler:

Sac makasıSac makası
Sütunlu MatkapSütunlu Matkap
Eğeler (El Eğesi)Eğeler (El Eğesi)
Nokta ZımbasıNokta Zımbası
4

Rivet the casing

Cut 5 in. strips of 1/16 in. sheet with 3/4 in. margins bent down (4 in. clear): 14 in. from C to D, 20 in. from E to F, and about 22 in. round the drum from D to F (measure it). Mark the rivet holes through the side holes, nick between holes so the drum strip bends without buckling, and rivet, backing each head with stout iron. Leave a foot of the drum strip open. (Easier: make the sides 2 in. larger with outward flanges and rivet the strips to them.)

Bu adım için malzemeler:

Yumuşak Çelik SacYumuşak Çelik Sac1 adet
Demir perçinlerDemir perçinler1 adet

Gerekli aletler:

Sac makasıSac makası
Sütunlu MatkapSütunlu Matkap
Perçin takımıPerçin takımı
ÇekiçÇekiç
Şerit MetreŞerit Metre
5

Turn the spindle

Turn 7 in. of 3/4 in. round iron smooth. Turn one end to 1/2 in. for 5/8 in. and the other to 1/2 in. for 2 1/8 in., with sharp shoulders. Bore a 2 x 2 in. collar a shade under size, heat it red and slip it on 1 in. in from a shoulder, then cool it in water to shrink it tight.

Bu adım için malzemeler:

Dövme demir çubukDövme demir çubuk1 adet
SuSu1 adet

Gerekli aletler:

Metal Torna TezgâhıMetal Torna Tezgâhı
Demirci ocağıDemirci ocağı
Demirci kerpeteniDemirci kerpeteni
6

Drill the collar

Drill four 5/16 in. holes 5/8 in. deep at quarters round the middle of the collar and tap them 3/8 in. (fig. 10).

Gerekli aletler:

Sütunlu MatkapSütunlu Matkap
El kılavuzlarıEl kılavuzları
Kılavuz koluKılavuz kolu
7

Forge the blades

Forge four blades (fig. 9) from 5/8 or 3/4 in. round iron, upsetting and flattening the ends to 1/16 in. thick (or weld 1/4 in. plate to 5/8 in. arms and thin it). Thread the arm ends to fit the collar, curve the blades slightly into a scoop, and bend the arms a little off concentric for a steadier blast.

Bu adım için malzemeler:

Dövme demir çubukDövme demir çubuk1 adet

Gerekli aletler:

Demirci ocağıDemirci ocağı
ÖrsÖrs
ÇekiçÇekiç
El kılavuzlarıEl kılavuzları
8

Bearings and assembly

Bolt a 1/2 in. brass bar at least 1 1/4 in. wide across each intake hole (A-B) and bore it true for the spindle. Fit one bearing, pass the spindle in, fit the other and bolt up. Screw the blades in through the open part of the drum, each slightly askew, check they turn without touching, and close the drum with thin-headed bolts, nuts outside.

Bu adım için malzemeler:

Pirinç ÇubukPirinç Çubuk1 adet
Altıköşe cıvata takımıAltıköşe cıvata takımı1 adet

Gerekli aletler:

Sütunlu MatkapSütunlu Matkap
Metal Torna TezgâhıMetal Torna Tezgâhı
Eğeler (El Eğesi)Eğeler (El Eğesi)
9

Drive it

File a flat on the 1 1/2 in. of spindle that stands out on the pulley side and key a 2 in. pulley with a 1 1/2 in. face to it. Belt it from a 2 ft wheel turned at 30 rpm: the fan runs at 360 rpm. Put the crank by the forge head, worked by hand or a foot lever (ours: details left to the reader in the source), and pipe the 3 1/2 x 2 1/2 in. mouth to the tuyere.

Bu adım için malzemeler:

MakaraMakara1 adet
Tahrik kayışıTahrik kayışı1 adet

Gerekli aletler:

Eğeler (El Eğesi)Eğeler (El Eğesi)
ÇekiçÇekiç
10

Troubleshooting

Fan troubleshooting.

Flow

Loading...
11

History and honest limits

From George Edwinson, "Smithing and Forging" I, **Amateur Work, Illustrated**, vol. V (1886), pp. 162-164 and figs. 7-11 (checked on the archive.org scan amateurworkillus05lond). He leaves the crank, wheel frame and pipe to the reader; the metric figures and tools are ours.

Malzemeler

8

Gerekli Aletler

13

CC0 Kamu Malı

Bu plan CC0 lisansıyla yayınlanmıştır. İzin almadan kopyalayabilir, değiştirebilir, dağıtabilir ve herhangi bir amaçla kullanabilirsiniz.

Planı üzerinden ürün satın alarak Maker'ı destekleyin, böylece Maker Komisyonu Satıcılar tarafından belirlenen komisyonu kazanırlar veya bu Planın yeni bir versiyonunu oluşturun ve gelir paylaşımı için kendi Planınıza bağlantı olarak ekleyin.

Tartışma

(0)

Giriş yapın tartışmaya katılmak için

Yorumlar yükleniyor...