SANAT
GÜZELLİK & SAĞLIK
ZANAAT
KÜLTÜR & TARİH
EĞLENCE
ÇEVRE
YİYECEK & İÇECEK
TERS MÜHENDİSLİK
BİLİMLER
SPOR
TEKNOLOJİ
GİYİLEBİLİR ÜRÜNLER
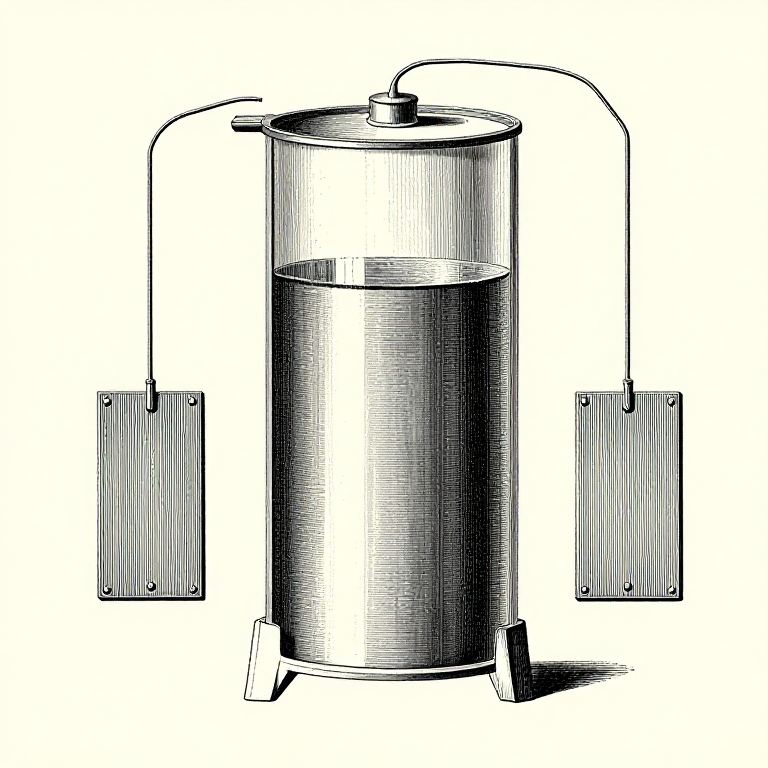

Faraday's Law: The One Process You Can Calculate Exactly
Electroplating is unusual among manufacturing processes: the amount of metal deposited can be calculated exactly, in advance, from the current and the time.
Each metal ion needs a fixed number of electrons to become an atom, so the charge that passes is a direct count of the atoms deposited. Faraday worked this out in the 1830s and it has not needed amending.
What the calculation does not give for free is the **current efficiency** — the fraction of the current that actually deposits metal rather than splitting water. For nickel it is about 95%; for chromium it is about 15%, which is why chrome plating is slow, hot and extravagant.
Orta
3 hours
Talimatlar
1
1
Setting up so the numbers mean something
Setting up so the numbers mean something
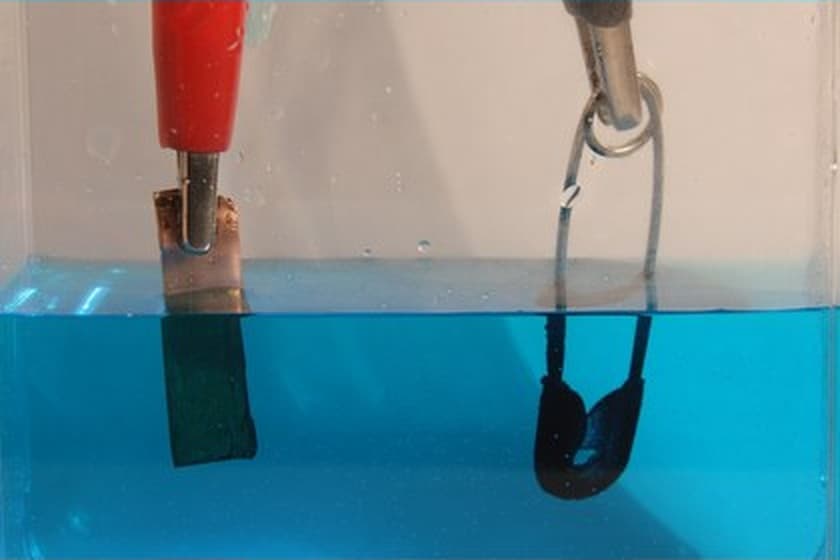
**The part is the cathode**, connected to the negative terminal. Metal ions in solution are positive, so they are attracted to it and are reduced to metal there.
**The anode is usually the same metal being plated**, and it dissolves at the same rate as the cathode gains, keeping the bath concentration constant. That is why a nickel bath has nickel anodes and a copper bath has copper.
**An inert anode** — lead, platinised titanium, graphite — is used where a soluble one would not work, chromium being the main case. Then the bath is depleted as plating proceeds and must be topped up.
**Measure the current, do not assume it.** A bench supply's display is a guide; a meter in series is the measurement. Every number in this rung depends on the current actually being what it says.
**Measure the area properly**, including both faces and the edges of a flat part. A part plated at "1 amp" with its area guessed at half its real value gets half the thickness intended.
**Agitate.** Solution next to the cathode is depleted of ions as it plates, and without movement the deposit goes rough and burnt. A magnetic stirrer, air sparging, or moving the work — every real plating bath moves.
Bu adım için malzemeler:
 Bakır sülfat (laboratuvar kalitesi)1 adet
 Bakır Levha2 adet
 Damıtılmış Su1 adet
Gerekli aletler:
 Ayarlanabilir Tezgâh Güç Kaynağı
 Dijital Multimetre — Otomatik Kademe, Gerçek RMS
 Borosilikat Beher
 Manyetik karıştırıcılı ısıtıcı tabla
2
2
The calculation, and the thicknesses actually used
The calculation, and the thicknesses actually used
Jupyter defteri yükleniyor…
Gerekli aletler:
 Masaüstü Bilgisayar
3
3
Measuring what actually happened
Measuring what actually happened
The calculation predicts; the balance confirms. Doing both is how the current efficiency of a particular bath is discovered, and after that the calculation can be trusted.
**Weigh before and after**, dry, on a scale reading to a milligram for a small part. The gain is the metal deposited.
**Compare with the prediction.** The ratio is the current efficiency of that bath at that current density and temperature, and it is worth writing on the tank.
**An efficiency above 100% means something is wrong** — the part was not dry, or it gained weight some other way, or the current was higher than recorded. It is the same impossible-number rule as a chemical yield.
**Measure the thickness directly** where it matters: a micrometer across a flat part before and after, which works down to a few microns; or a magnetic or eddy current gauge, which is what industry uses; or a cross-section under a microscope, which is destructive and definitive.
**Expect the thickness to vary across the part**, and that is not an error in the calculation — Faraday's law gives the TOTAL metal deposited, and the distribution is the next rung's subject.
Bu adım için malzemeler:
 Nikel levha1 adet
 Yumuşak çelik plaka1 adet
Gerekli aletler:
 Hassas Terazi
 Mikrometre
 Dijital Kumpas 6 İnç
4
4
Running a bath: temperature, pH and what to log
Running a bath: temperature, pH and what to log
A plating bath is a chemical system with a working window, and drifting outside it degrades the deposit long before the bath stops working.
**Temperature.** Higher temperature allows higher current density and gives a softer, less stressed deposit; too cold and the deposit is brittle and burns at modest current. A Watts nickel bath runs at 45 to 60 C.
**pH.** Nickel wants about 4.0 to 4.5. Too low and the efficiency falls as more current goes to hydrogen; too high and basic salts precipitate into the deposit as roughness.
**Concentration.** Falls as the bath is used if the anodes cannot keep up, and low metal concentration shows up first as burning at the edges.
**Additives.** Brighteners, levellers and wetting agents. They are consumed, they break down into products that accumulate, and they are the usual reason a bath that worked last month does not now.
**Log every run:** date, part, area, current, time, temperature, pH, and the measured weight gain. Six lines, and they turn "the plating has gone dull" into a curve with a cause.
**A Hull cell** is the standard diagnostic: a small tank shaped so one test panel sees a whole range of current densities at once. One panel shows the bath's working range, where it burns and where it is too thin — and it uses a few hundred millilitres of solution.
Bu adım için malzemeler:
 Nikel sülfat heksahidrat1 adet
 Elektrokaplama seti (nikel)1 adet
Gerekli aletler:
 Laboratuvar TermometresiAyarlanabilir Tezgâh Güç KaynağıDijital Multimetre — Otomatik Kademe, Gerçek RMS
Malzemeler
7- Yer Tutucu
- 2 adetYer Tutucu
- 1 adetYer Tutucu
- 1 adetYer Tutucu
- 1 adetYer Tutucu
- 1 adetYer Tutucu
- Yer Tutucu
Gerekli Aletler
9- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
İlgili Blueprint'ler
Bu blueprint'ler bilgi paylaşır — teknikler, malzemeler veya ilkeler
CC0 Kamu Malı
Bu plan CC0 lisansıyla yayınlanmıştır. İzin almadan kopyalayabilir, değiştirebilir, dağıtabilir ve herhangi bir amaçla kullanabilirsiniz.
Planı üzerinden ürün satın alarak Maker'ı destekleyin, böylece Maker Komisyonu Satıcılar tarafından belirlenen komisyonu kazanırlar veya bu Planın yeni bir versiyonunu oluşturun ve gelir paylaşımı için kendi Planınıza bağlantı olarak ekleyin.