SANAT
GÜZELLİK & SAĞLIK
ZANAAT
KÜLTÜR & TARİH
EĞLENCE
ÇEVRE
YİYECEK & İÇECEK
TERS MÜHENDİSLİK
BİLİMLER
SPOR
TEKNOLOJİ
GİYİLEBİLİR ÜRÜNLER

Plastic Syringe Set: Moulded Barrel and a Soft Polyethylene Piston
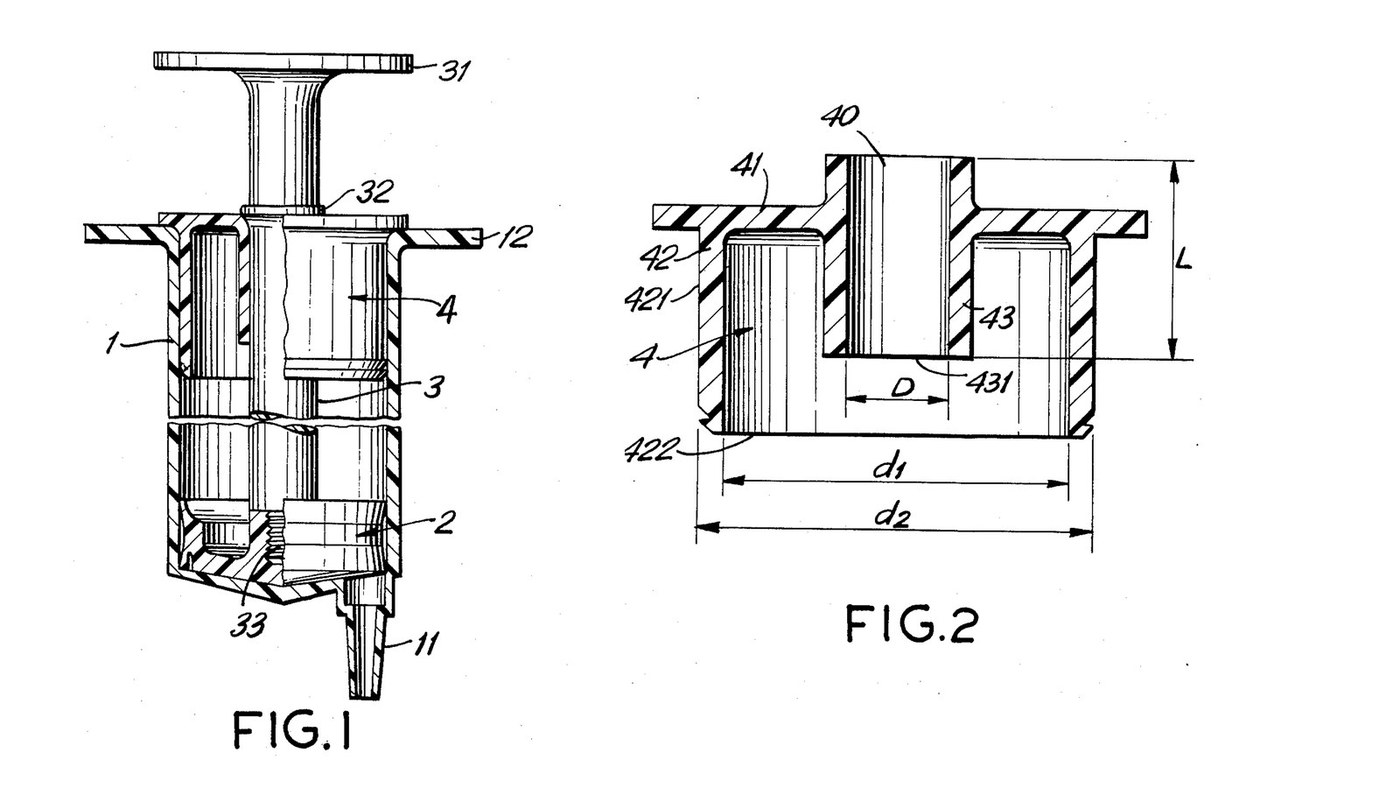
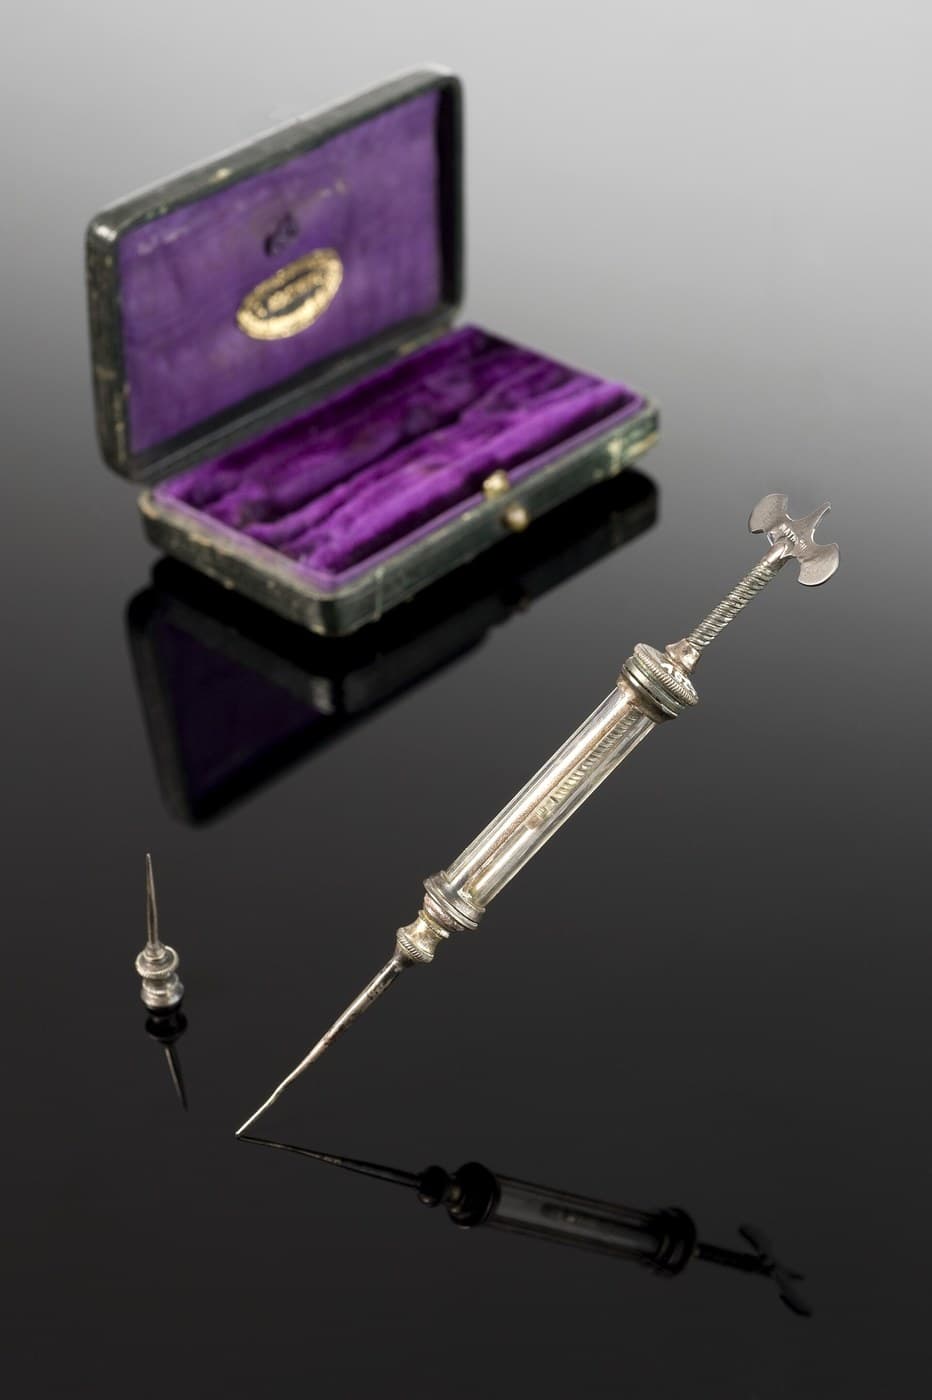
Four moulded parts make a plastic syringe with no rubber seal and no grease: a stiff barrel with a taper nozzle, a bell-shaped piston whose thin polyethylene lips seal against the wall, a slim plunger shaft, and a cap whose long sleeve guides the shaft so it cannot bend and tilt the piston (Adorján & Dávid, US 4,704,105, 1987). Mould one set of moulds per size for a set of syringes for hydraulic models.
The piston figures are the patent's. Polypropylene, LDPE, the sizes and the mould making are ours. Not for medical use. The picture: Figs. 1-2.
İleri
3 days (moulds) + 1 hour per batch
Talimatlar
1
1
The moulding process
The moulding process
Drying, mould, injection, cooling and inspection all follow this blueprint. The steps below add only what the syringe needs.
2
2
Mill the barrel mould
Mill the barrel mould
Mill a two-plate mould for the barrel (1): a stiff-walled tube closed at one end by a nozzle (11) with a standard needle taper (ours: the Luer taper), and two finger grips (12) at the open end. One mould per syringe size you want, for example 5, 50 and 60 ml (ours).
Gerekli aletler:
 Freze Tezgâhı
 Enjeksiyon kalıbı alüminyum bloğu (2 plakalı)
 Enjeksiyon kalıp çerçevesi
3
3
Mill the piston mould
Mill the piston mould
The piston (2) is a bell: a rim 5-7 mm high whose two edges flare out into lips 0.3-0.5 mm thick, a front groove 0.3-0.5 mm wide and 2-2.5 mm deep, and a central shank. The lips must come out 0.2-0.6 mm wider than the barrel bore; the rim between them no wider than the bore.
Gerekli aletler:
Freze TezgâhıEnjeksiyon kalıbı alüminyum bloğu (2 plakalı)Enjeksiyon kalıp çerçevesi Dijital Kumpas 6 İnç
4
4
Mill the shaft and cap moulds
Mill the shaft and cap moulds
Shaft (3): thumb rest (31), a bead (32) and an end projection (33) a little larger than the piston's bore. Cap (4): a disc with an outer collar (42) that force-fits the barrel and an inner sleeve (43) at least as long as the shaft is thick.
Gerekli aletler:
Freze TezgâhıEnjeksiyon kalıbı alüminyum bloğu (2 plakalı)Enjeksiyon kalıp çerçevesi5
5
Mould the barrels
Mould the barrels
Mould the barrels from virgin plastic. The patent asks only for a rigid plastic; ours: polypropylene.
Bu adım için malzemeler:
 Polipropilen granül1 batch
Gerekli aletler:
 Granül kurutucu
 Enjeksiyon kalıplama makinesi
6
6
Mould the pistons
Mould the pistons
Mould the pistons from virgin polyethylene, which the patent wants at 65-90 degrees Shore (scale not stated). Ours: LDPE; check your grade's data sheet.
Bu adım için malzemeler:
 LDPE granül1 batch
Gerekli aletler:
Granül kurutucuEnjeksiyon kalıplama makinesi7
7
Mould the shafts and caps
Mould the shafts and caps
Mould shafts and caps. These may be reprocessed plastic, as they never touch the liquid. Ours: polypropylene.
Bu adım için malzemeler:
Polipropilen granül1 batchGerekli aletler:
Enjeksiyon kalıplama makinesi8
8
Check the lip size
Check the lip size
Measure the barrel bore and a piston's lips. The lips must be 0.2-0.6 mm wider than the bore. Adjust the mould if not.
Gerekli aletler:
Dijital Kumpas 6 İnç9
9
Snap the shaft into the piston
Snap the shaft into the piston
Push the shaft's projection through the small bore at the back of the piston until it snaps into the wider cavity behind it.
10
10
Assemble
Assemble
Push the piston into the barrel. Thread the shaft through the cap's sleeve and force the cap's outer collar into the open end of the barrel. Its end face now stops the piston when you draw it fully back.
11
11
Lock the cap
Lock the cap
Press two dents, opposite each other, through the barrel wall into the cap collar with a hot tool so the cap cannot pull out. Ours: a soldering iron tip.
Gerekli aletler:
 Elektrikli Havya
12
12
Test the seal
Test the seal
Draw water and push it out, along the whole stroke, with no grease. It should move smoothly from the start and not leak past the lips. Note the size and file it into your set.
Gerekli aletler:
 Su
 Cam Beher
Malzemeler
2- 1 batchYer Tutucu
- 1 batchYer Tutucu
Gerekli Aletler
9- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
Bu planla yapılan
İlgili Blueprint'ler
Bu blueprint'ler bilgi paylaşır — teknikler, malzemeler veya ilkeler
CC0 Kamu Malı
Bu plan CC0 lisansıyla yayınlanmıştır. İzin almadan kopyalayabilir, değiştirebilir, dağıtabilir ve herhangi bir amaçla kullanabilirsiniz.
Planı üzerinden ürün satın alarak Maker'ı destekleyin, böylece Maker Komisyonu Satıcılar tarafından belirlenen komisyonu kazanırlar veya bu Planın yeni bir versiyonunu oluşturun ve gelir paylaşımı için kendi Planınıza bağlantı olarak ekleyin.