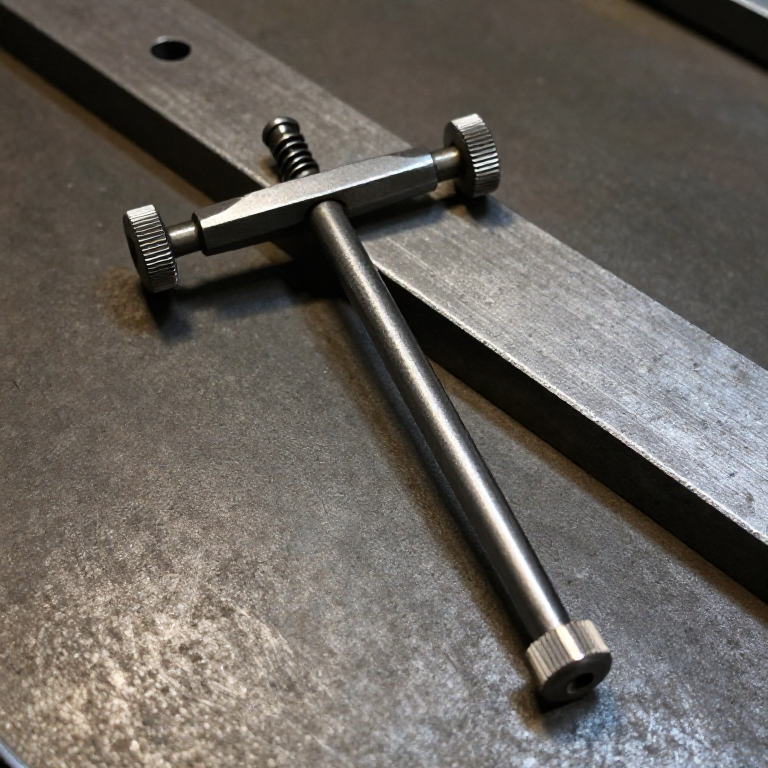

Telescoping Bore Gauge
Talimatlar
Build the T-head and its bore
Build the T-head and its bore
Two plungers sliding in a cross tube, pushed apart by a spring.
- Cut a cross tube 40 mm long from 12 mm aluminium round bar and drill it through at 6.0 mm.
- Turn or file two plungers from 6 mm bar, each 25 mm long, to slide freely in that bore.
- Round the outer end of each plunger to a smooth radius.
- Fit a light compression spring between them inside the tube.
The rounded ends matter more than they look. A flat-ended plunger contacts the bore wall on an edge, and the edge digs in or rides on a burr. A radius contacts on a single point at the true diameter, which is what makes the rocking technique in step 4 work.
Fit the plungers so they slide with no perceptible side play but no stiffness. Any looseness here is added directly to your measurement error.Bu adım için malzemeler:
 Alüminyum Yuvarlak Çubuk1 adet
 Baskı Yayı Seti1 takım
Gerekli aletler:
 Demir Testeresi Gövdesi ve Ağızları
 Kablosuz Matkap
 Matkap Ucu Takımı
 Eğe Takımı
 Tezgah Mengenesi
 Dijital Kumpas 6 İnç
Add the handle and the locking screw
Add the handle and the locking screw
The lock must clamp the plungers without moving them.
- Cut a handle 90 mm from 10 mm round bar and fix it square to the middle of the cross tube.
- Drill and tap the handle's far end M4, running down to a pin that bears on the plungers.
- Fit an M4 × 30 socket head cap screw as the lock, with a knurled knob or cross-bar for finger tightening.
- Test: expand the plungers, lock, and check they cannot be pushed in by hand.
What a commercial gauge does: the knurled knob at the handle end turns a rod that wedges the plungers, and it is designed so that tightening applies pressure ALONG the plunger axis rather than sideways. Modern build spec (derived): an M4 screw onto a pin does the same job — but check for the failure mode below.
Lock it, then measure across the plungers, then unlock and re-lock and measure again. If the two differ, your lock is nudging the plungers as it tightens and every measurement will carry that error.Bu adım için malzemeler:
Alüminyum Yuvarlak Çubuk1 adet İçten Altıgen Başlı Silindirik Vida1 adet
 Altıgen Somun1 adet
Gerekli aletler:
Kablosuz MatkapMatkap Ucu Takımı Alyan Anahtar TakımıEğe TakımıDijital Kumpas 6 İnç
Transfer a measurement
Transfer a measurement
The gauge finds the size; something else reads it.
- Compress the plungers, insert into the bore, release so they spring against the walls.
- Lock lightly.
- Withdraw the gauge without knocking it.
- Measure across the plunger tips with a micrometer or caliper.
Gerekli aletler:
Dijital Kumpas 6 İnçLearn the rocking technique — the smallest reading is the true one
Learn the rocking technique — the smallest reading is the true one
Insert it carelessly and you will measure a chord, not the diameter.
- Insert the gauge deliberately TILTED in the bore and lock it. Measure.
- Now insert it, and before locking, rock the handle gently through the bore's axis.
- Feel for the point of least resistance — that is where the plungers lie on the true diameter.
- Lock at that point and measure.
- Repeat five times and compare the spread.
Bu adım için malzemeler:
 Alüminyum Lama1 adet
Gerekli aletler:
Dijital Kumpas 6 İnçKablosuz MatkapTransfer versus direct reading, and history
Transfer versus direct reading, and history
Transfer instruments are a whole family. Small hole gauges, inside calipers, firm-joint calipers and this gauge all do the same thing: capture a dimension mechanically where no scale will fit, then carry it out to a scale. Before dial bore gauges and modern internal micrometers, this is how internal work was measured at all.
The trade against direct reading. An internal micrometer reads the bore directly with no transfer step and no feel involved — fewer places to go wrong — but it is expensive, comes in limited ranges and will not enter a small hole. The telescoping gauge is cheap, covers a wide range with a few sizes, and puts the burden on the operator's touch. Two answers to one problem, and workshops keep both.
Why feel is a real skill. The rocking technique in step 4 cannot be automated away in a manual gauge, and two people measuring the same bore will differ by more than the instrument's resolution. That is not a flaw in the tool; it is the honest cost of the transfer approach, and it is why critical production bores are checked with plug gauges or air gauges that remove the operator entirely.
Its neighbours in this catalogue: the micrometer reads directly to a fine scale but only from outside; the vernier caliper reads both inside and outside but with lower resolution and jaw-flex error; this gauge reaches where neither can and carries the answer out. Each covers a region the others cannot.
Malzemeler
5- 1 adetYer Tutucu
- 1 takımYer Tutucu
- Yer Tutucu
- 1 adetYer Tutucu
- 1 adetYer Tutucu
Gerekli Aletler
7- Yer Tutucu
- 1 vendor sell this, none ship to you yetYer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
İlgili Blueprint'ler
Bu blueprint'ler bilgi paylaşır — teknikler, malzemeler veya ilkeler


CC0 Kamu Malı
Bu plan CC0 lisansıyla yayınlanmıştır. İzin almadan kopyalayabilir, değiştirebilir, dağıtabilir ve herhangi bir amaçla kullanabilirsiniz.
Planı üzerinden ürün satın alarak Maker'ı destekleyin, böylece Maker Komisyonu Satıcılar tarafından belirlenen komisyonu kazanırlar veya bu Planın yeni bir versiyonunu oluşturun ve gelir paylaşımı için kendi Planınıza bağlantı olarak ekleyin.