İşbirliği
SANAT
GÜZELLİK & SAĞLIK
ZANAAT
KÜLTÜR & TARİH
EĞLENCE
ÇEVRE
YİYECEK & İÇECEK
TERS MÜHENDİSLİK
BİLİMLER
SPOR
TEKNOLOJİ
GİYİLEBİLİR ÜRÜNLER
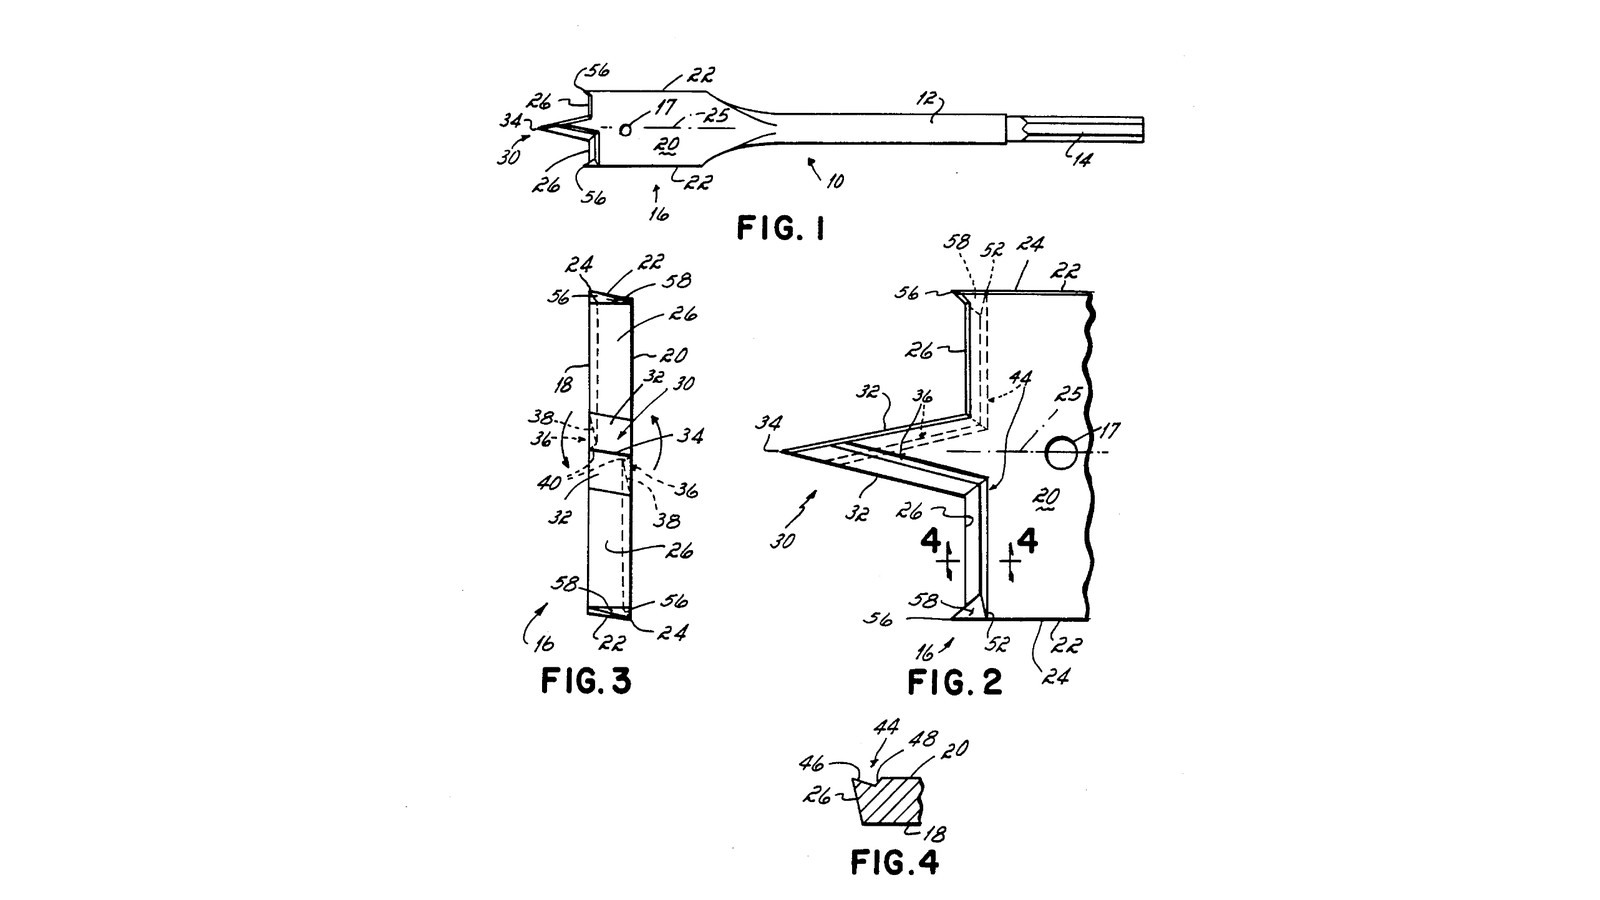


Fluted-Shoulder Spade Bits With Spurs: Flutes Along the Shoulders, Stopped by Corner Spurs (Williams & Thackston, 1987)
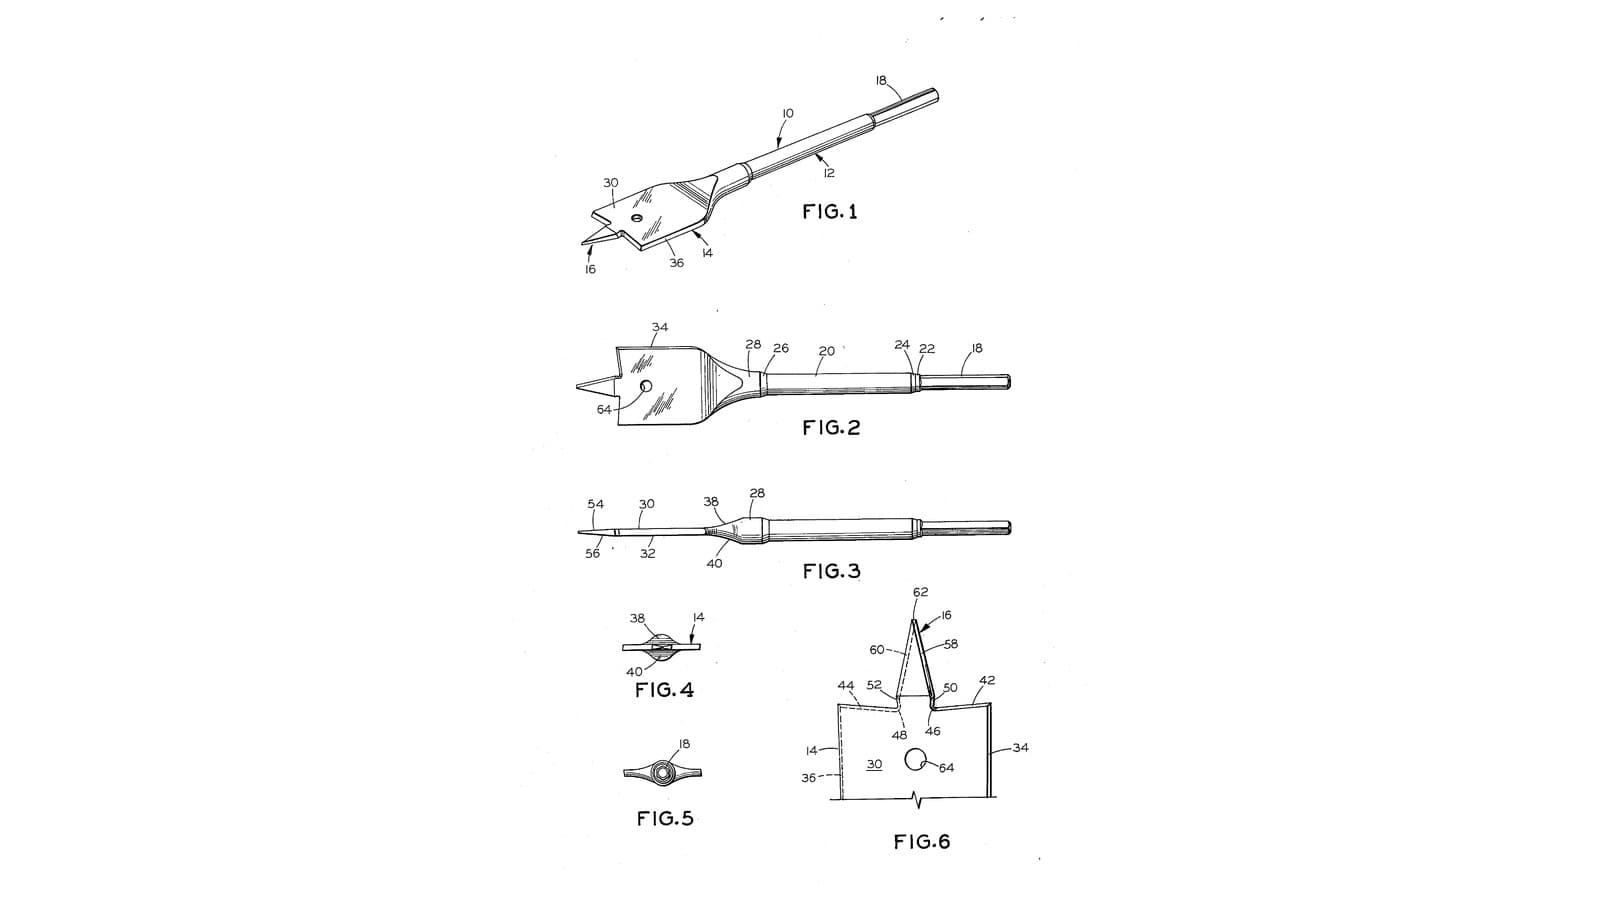
A. Graves Williams III and Ronald L. Thackston of Ohio received US 4,682,917, dated 28 July 1987, for The Irwin Company. They kept Robinson's flutes on the point and added a flute along each shoulder's cutting edge, joining the point flute. Each flute stops just short of the outside, closed by a sharp spur at the corner whose inner edge slopes into it. The spur scores the rim of the hole. In oak their bits bored up to twice as fast as Robinson's, and left a clean exit instead of a splintered one.
We forge three of their test sizes, 5/8, 7/8 and 1 inch. The patent gives the angles; the other sizes are ours.
İleri
About 1 day
Talimatlar
1
1
Their tests
Their tests
Jupyter defteri yükleniyor…
2
2
Read US 4,682,917
Read US 4,682,917
"If the flutes are 'stopped', that is, if they do not extend or 'open' to the respective outer sides of the blade, and if cutting spurs are provided at the outer corners of the shoulders so that the spurs 'close' the flutes, then this splitting is virtually eliminated and cutting proceeds more smoothly."
3
3
Forge the blades
Forge the blades
Cut three 170 mm lengths of 10 mm octagonal tool steel. Heat 50 mm of one end to a bright orange in the forge and flatten it on the anvil to about 3 mm thick, centred on the bar. Hammer across it with the peen to spread it wider than the bit, about 2 mm over its size: 18, 24 and 27 mm. Draw the neck down smoothly where the blade meets the bar and keep the blade in line with it. Reheat as soon as the colour fades to red. Finally heat each one to a cherry red and let it cool slowly in the air, to soften it for filing.
Bu adım için malzemeler:
 Sekizgen takım çeliği çubuk3 adet
Gerekli aletler:
 Demir Testeresi
 Tezgah Mengenesi
 Demirci Ocağı
 Örs
 Dövme Çekici
 Demirci Maşası
 Kaynak eldivenleri
 Koruyucu gözlük
4
4
Print the grinding template
Print the grinding template
Full-size A4 template: the outlines of the 5/8, 7/8 and 1 inch bits with square shoulders and corner spurs, the joined point and shoulder flutes on one face, and the hanging hole. Print at 100 %; its 50 mm bar must measure 50 mm.
5
5
Grind the outline
Grind the outline
Glue each bit's outline from the template on its blade, centred on the bar. Grind to the lines on the bench grinder, dipping the steel in water often: the two sides parallel, the shoulders square across, the point in the middle. Grind the blade's two faces flat and parallel to 2.5 mm. Grind three flats on the end of the shank, a third of the way round from each other, 20 mm long, for the chuck's jaws. Leave a spur 2 mm wide and 2 mm high at each outer corner of the shoulders. Drill a 3 mm hole at the template's circle.
Gerekli aletler:
 Mürekkep püskürtmeli yazıcı
 Tutkal
 Taşlama motoru
 Su verme kovası
 Su
 Eğe TakımıTezgah Mengenesi
 Dijital Kumpas 6 İnçKoruyucu gözlük
6
6
Bevel the edges and file the flutes
Bevel the edges and file the flutes
Bevel the outer sides and the shoulders' cutting edges slightly, so each edge meets its leading face at about 86 degrees. On the face towards you, file the point flute along the point's left edge with the 3 mm round needle file, 0.3 mm deep. Then file the shoulder flute with the three-square needle file along the left shoulder, right behind its cutting edge and square to the bit's axis, from the point flute to the spur, and stop there. Bevel the spur's inner edge into the flute so the spur has a sharp outer edge. Turn the bit over and do the same along that face's left edge and shoulder.
Gerekli aletler:
Taşlama motoruSu verme kovasıSuTezgah Mengenesi İğne Eğe TakımıDijital Kumpas 6 İnç
7
7
Harden and temper
Harden and temper
Heat the blade and the neck evenly to a cherry red, until a magnet no longer sticks to it, and quench it straight down in water, moving it up and down. Rub the faces bright with a stone. Heat the shank gently 30 mm behind the blade and watch the colours run down; quench again as soon as a dark straw colour reaches the shoulders and the point. Do the other two.
Gerekli aletler:
Demirci OcağıDemirci Maşası Küçük MıknatısSu verme kovasıSu
 Bileği TaşıKaynak eldivenleriKoruyucu gözlük
8
8
Sharpen and test
Sharpen and test
Hone the cutting edges on the shoulders and the point with the stone, keeping their angles, and take the burr off. Chuck a bit by its flats and bore a scrap of hardwood: it should start on the point without wandering, cut two clean shavings from the shoulders and leave a round hole of its own size; check it with the caliper.
Gerekli aletler:
Bileği Taşı Kablosuz Matkap
 Sert Ağaç TahtasıDijital Kumpas 6 İnçKoruyucu gözlük
9
9
Troubleshooting
Troubleshooting
Spade bit troubleshooting.
Flow
Loading...
10
10
History and honest limits
History and honest limits
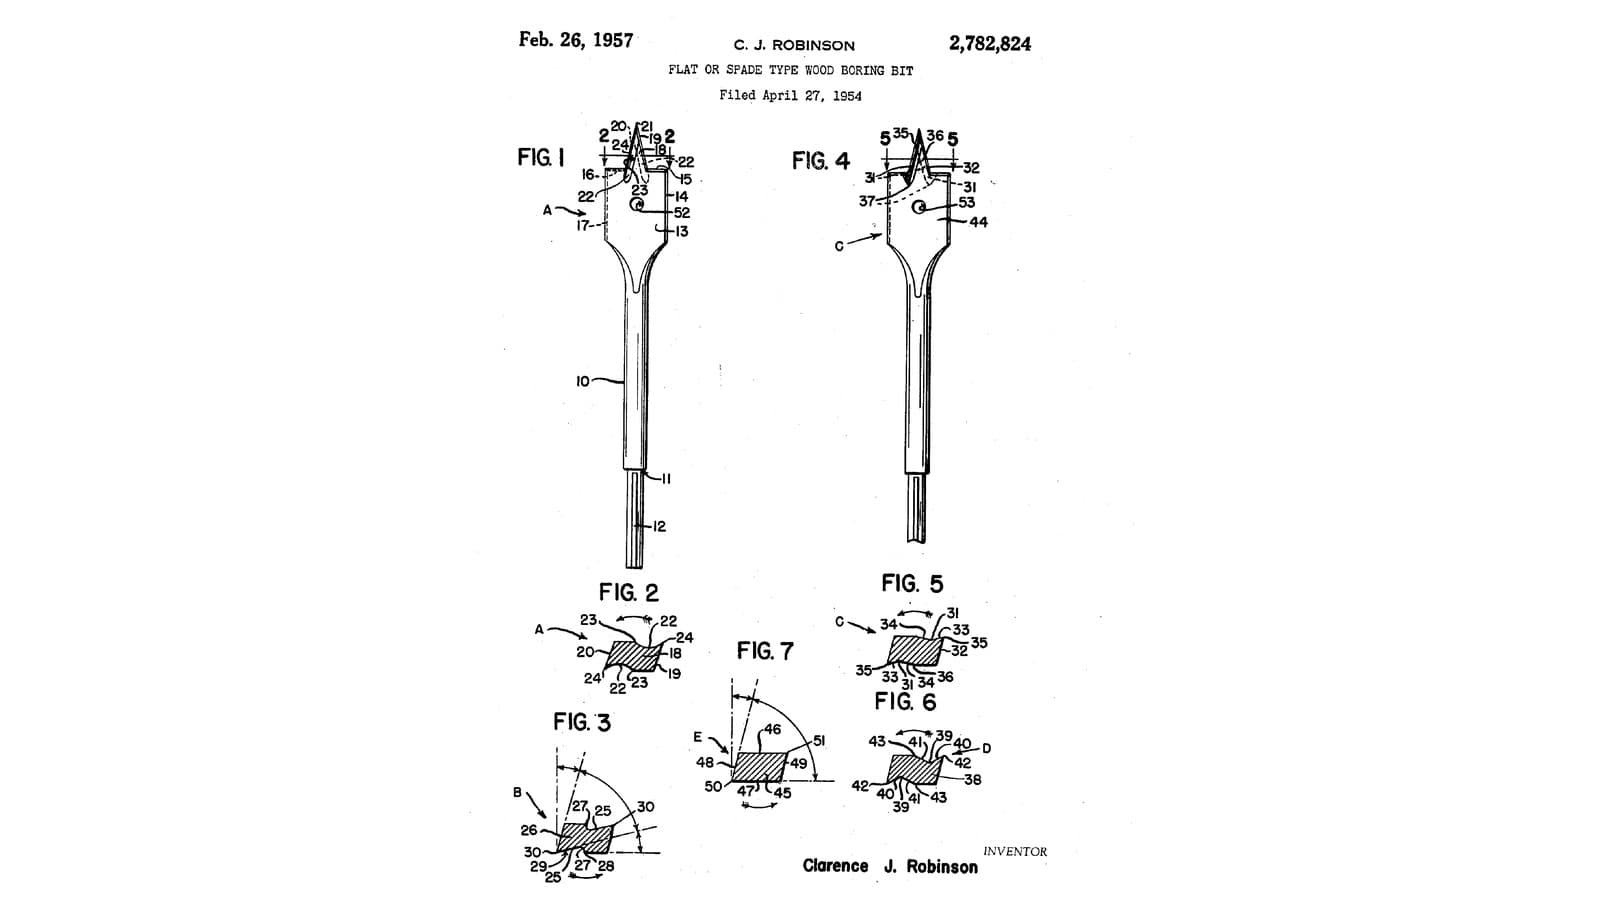
**A. Graves Williams III**, Wilmington, and **Ronald L. Thackston**, Hillsboro, Ohio, assignors to The Irwin Company, US 4,682,917, dated 28 July 1987, filed 24 January 1986. They claimed "cutting spurs projecting forwardly from the shoulders" with sharp outer edges, and shoulder flutes from the point flutes towards the spurs, "terminating at the spurs so that the shoulder flutes do not extend across the spurs to the outer sides of the blades". They prefer the flutes forged and the flute wall at about 68 degrees; we file them, with a three-square file at 60 degrees, inside their "less than about 78". Their shank has a hexagonal end; ours is octagonal tool steel with three ground flats. They give no heat treatment or spur size; those are ours.
Malzemeler
1- Yer Tutucu
Gerekli Aletler
20- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- Yer Tutucu
- 1 vendor sell this, none ship to you yetYer Tutucu
- Yer Tutucu
Tasarım dosyaları
1Bu planla yapılan

İlgili Blueprint'ler
Bu blueprint'ler bilgi paylaşır — teknikler, malzemeler veya ilkeler
CC0 Kamu Malı
Bu plan CC0 lisansıyla yayınlanmıştır. İzin almadan kopyalayabilir, değiştirebilir, dağıtabilir ve herhangi bir amaçla kullanabilirsiniz.
Planı üzerinden ürün satın alarak Maker'ı destekleyin, böylece Maker Komisyonu Satıcılar tarafından belirlenen komisyonu kazanırlar veya bu Planın yeni bir versiyonunu oluşturun ve gelir paylaşımı için kendi Planınıza bağlantı olarak ekleyin.