МИСТЕЦТВО
КРАСА ТА ЗДОРОВ'Я
РЕМЕСЛО
КУЛЬТУРА ТА ІСТОРІЯ
РОЗВАГИ
СЕРЕДОВИЩЕ
ЇЖА ТА НАПІЇ
ЗБОРНА ІНЖЕНЕРІЯ
НАУК
СПОРТ
ТЕХНОЛОГІЯ
НОСИМО
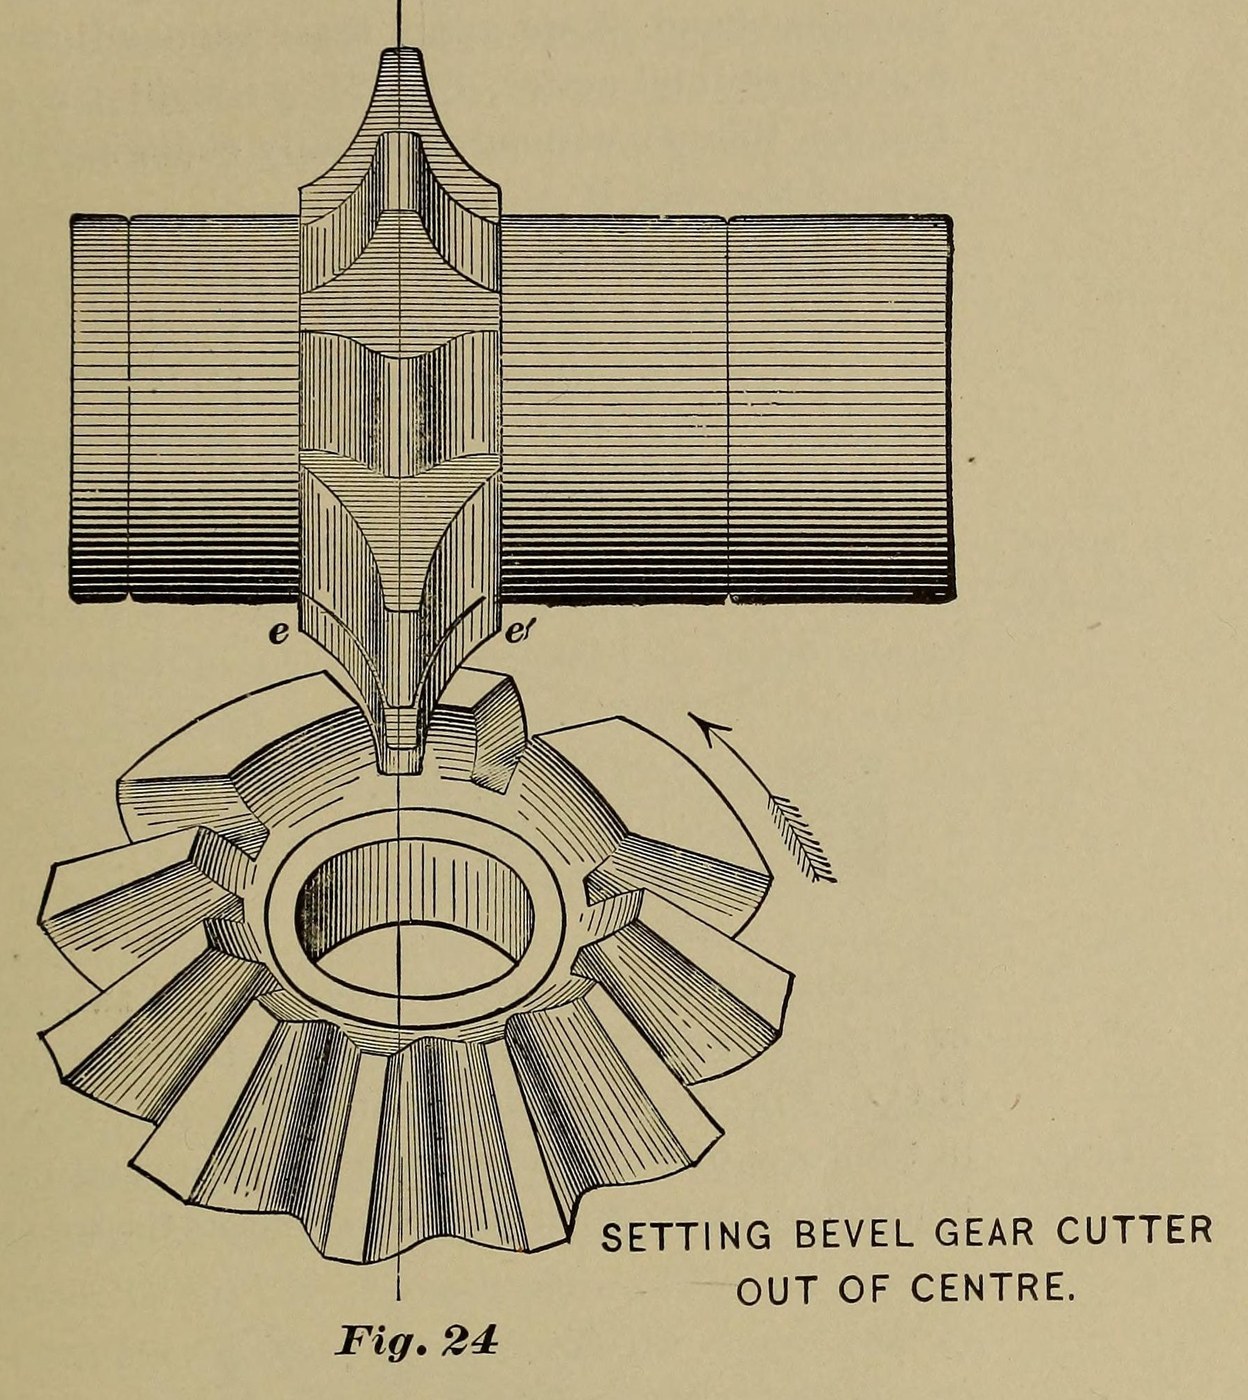


Mitre Gears: a 1:1 Bevel Pair Cut on the Milling Machine (Brown & Sharpe 1911)
Two equal bevel gears on shafts at right angles are mitre gears, and one cutter cuts both. A rotary cutter can only be right for one end of a bevel tooth, so Brown & Sharpe cut each space twice, set off centre to each side, then file the small ends round. Every figure here comes from their rules, worked out for a pair of 16 teeth, 8 pitch.
Source: Brown & Sharpe, Practical Treatise on Gearing (1911), Part I ch. IX–X and Part II ch. III; set-over table p. 58. The tooth count, pitch, face width, steel and bore are ours, and so is the arithmetic. Picture: Brown & Sharpe's Fig. 24.
Просунутий
2 days
Інструкції
1
1
Work out and turn two blanks
Work out and turn two blanks
Ours: 16 teeth, 8 pitch, so pitch diameter 2.000 in. Mitre gears have a 45° centre angle (tangent 16/16). Diameter increment = cos 45° × working depth 0.250 = 0.177 in. Apex distance 1.414 in. Angle increment: tan = sin 45° ÷ 8, giving 5° 03′; cutting and face angle 45° − 5° 03′ = 39° 57′. Turn two blanks from steel to 2.18 in outside diameter, with the angle of edge 45° and the angle of face 39° 57′, tried with a protractor against the end of the hub. Face length ⅜ in (ours; no more than a third of the 1.414 in apex distance). Bore and hub are ours.
Матеріали для цього кроку:
 Пруток із низьковуглецевої сталі1 length for two blanks
Необхідні інструменти ({count})
 Токарний верстат по металу
 Токарний різець
 Транспортир
 Мікрометр
2
2
Choose the cutter
Choose the cutter
Back cone radius 1.414 in: twice that × 8 pitch = 22.6 teeth, so a No. 5, 8-pitch bevel gear cutter (21 to 25 teeth). One cutter does both gears. Measure its thickness Tc at the pitch line, 0.145 in (1.157 ÷ 8) from its tip.
Необхідні інструменти ({count})
 Фреза для конічних коліс
 Зубомірний штангенциркуль
3
3
Set the head and the depth
Set the head and the depth
Mount the blank on the dividing head, set to the cutting angle of 39° 57′, to index 16 spaces. Set the depth at the large end to the working depth plus clearance, 0.270 in. Clearance stays the same at the small end.
Необхідні інструменти ({count})
 Фрезерний верстат
 Ділильна головкаФреза для конічних коліс
4
4
Set over and cut one side of every tooth
Set over and cut one side of every tooth
Set-over: apex distance ÷ face = 1.414 ÷ 0.375 = 3.77, so use the 3¾ column, where a No. 5 cutter has the factor .293. Set-over = Tc ÷ 2 − .293 ÷ 8 = Tc ÷ 2 − 0.037 in. Set the work off centre by that amount to one side, taking up backlash. Run the cutter through, indexing round all 16 spaces.
Необхідні інструменти ({count})
Фрезерний верстатДілильна головкаФреза для конічних коліс5
5
Set over the other way and trim to thickness
Set over the other way and trim to thickness
Set over by the same amount on the other side of centre and rotate the blank to line the cutter up with the space at the small end. Take a trial cut, then rotate the blank toward the cutter until the tooth is right: 0.196 in thick at the large end and 0.144 in at the small end. Check both ends with the gear tooth vernier. Right at the large end but thick at the small end means too much set-over; the other way round, too little.
Необхідні інструменти ({count})
Фрезерний верстатДілильна головкаФреза для конічних колісЗубомірний штангенциркуль6
6
Cut round, then make the second gear
Cut round, then make the second gear
Cut the second side of every tooth with that setting. Cut the second blank the same way with the same cutter.
Необхідні інструменти ({count})
Фрезерний верстатДілильна головкаФреза для конічних коліс7
7
File the small ends
File the small ends
Round the teeth over at the small ends with a file, where the cutter could not. Do not file them thinner at the pitch line.
Необхідні інструменти ({count})
 Тонкий напилок
Матеріали
1- 1 length for two blanksЗаповнювач
Необхідні інструменти
9- Заповнювач
- Заповнювач
- Заповнювач
- Заповнювач
- Заповнювач
- Заповнювач
- Заповнювач
- Заповнювач
- Заповнювач
За цим кресленням виготовляють

CC0 Суспільне надбання
Це креслення випущено під ліцензією CC0. Ви можете вільно копіювати, змінювати, поширювати та використовувати цю роботу для будь-яких цілей без запиту дозволу.
Підтримайте мейкера, купуючи продукти через його креслення, де він отримує Комісію мейкера встановлену вендорами, або створіть нову ітерацію цього креслення та включіть його як зв'язок у власне креслення для розподілу доходу.