ART
BEAUTY & WELLNESS
CRAFT
CULTURE & HISTORY
ENTERTAINMENT
ENVIRONMENT
FOOD & DRINKS
REVERSE ENGINEERING
SCIENCES
SPORTS
TECHNOLOGY
WEARABLES
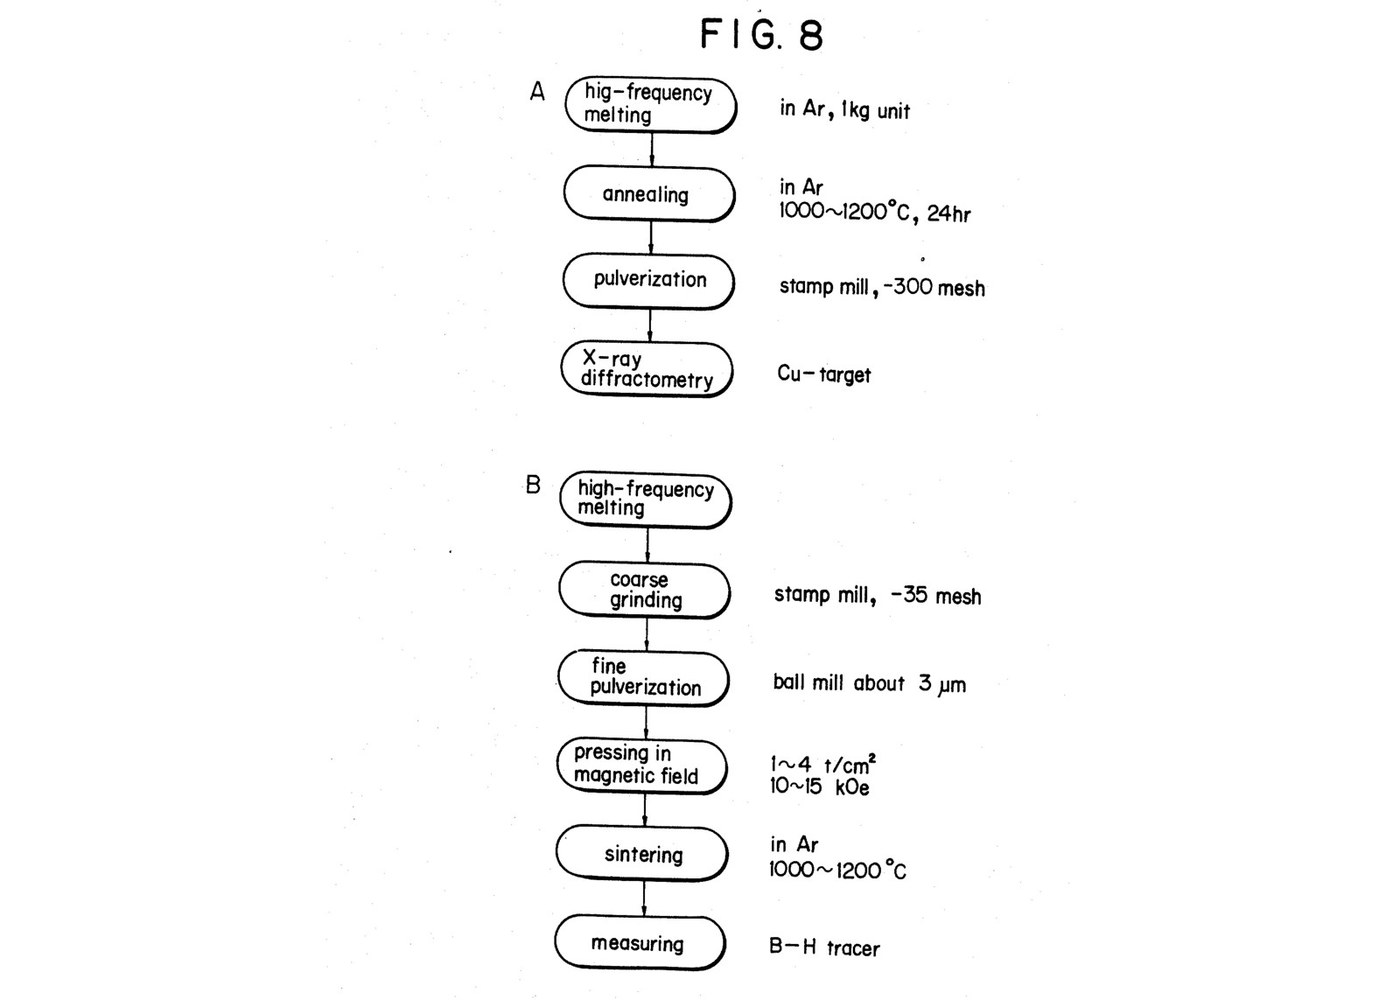


Neodymium Magnets, Sample 8: 75Fe-10B-15Nd Sintered (Sagawa 1988)
Neodymium magnets are iron, boron and neodymium. Sagawa's team at Sumitomo melted the three together, ground the casting to a powder finer than 10 µm, lined the grains up in a magnetic field while pressing them, and sintered the compact in argon. This is their sample 8, 75 % iron, 10 % boron and 15 % neodymium by atoms: 31.9 MGOe.
Source: M. Sagawa et al. (Sumitomo Special Metals), US 4,770,723 (1988). Unknown: how the pure iron, the ferroboron and the neodymium metal are made, and how the finished magnets are magnetised; the patent does not say. The 1 kg weights are our arithmetic from the patent's atomic percentages. Picture: the patent's Fig. 8.
Expert
2 days
Instructions
1
1
Weigh sample 8: 75 Fe, 10 B, 15 Nd
Weigh sample 8: 75 Fe, 10 B, 15 Nd
Sample 8 is 75 % iron, 10 % boron and 15 % neodymium by atoms. Use 99.9 % electrolytic iron, ferroboron (19.38 % B, 5.32 % Al, 0.74 % Si, 0.03 % C, the rest iron) and neodymium of 99.7 % or better. Ours: a 1 kg melt, by arithmetic: 584.0 g iron, 86.4 g ferroboron, 334.9 g neodymium. Unknown: how these three are made.
Materials for this step:
 Electrolytic Iron584 g
 Ferroboron86.4 g
 Neodymium Metal334.9 g
Tools needed:
 Balance Scale
2
2
Melt by high frequency in argon and cast
Melt by high frequency in argon and cast
Melt the charge in a high-frequency (induction) furnace under argon and pour it into a water-cooled copper mould.
Tools needed:
 Induction Furnace
 Clay Crucible - Refractory
 Argon
 Pressure Gas Cylinder
 Water-Cooled Copper Mould
 Heat-Resistant Gloves
3
3
Stamp to 35 mesh, ball-mill to 3-10 µm
Stamp to 35 mesh, ball-mill to 3-10 µm
Crush the casting in a stamp mill until it passes a 35-mesh sieve. Then grind it in a ball mill for 3 hours, to 3-10 µm.
Tools needed:
 Stamp Mill
 Sieve Set (Graded Mesh)
 Iron Ball Mill
 Safety Glasses
4
4
Press in a 10 kOe field at 1.5 t/cm²
Press in a 10 kOe field at 1.5 t/cm²
Line the powder up in a magnetic field of 10 kOe and press it at 1.5 tonnes per cm². Unknown: the size and shape of the magnets.
Tools needed:
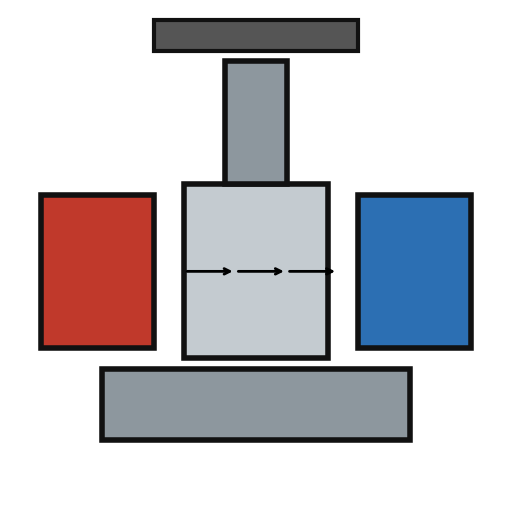 Magnetic-Field Press
5
5
Sinter in argon at 1000-1200 °C
Sinter in argon at 1000-1200 °C
Sinter the compacts at 1000-1200 °C for about one hour in argon, then let them cool. Sample 8 measured 11.9 kG remanence, 8.0 kOe coercivity and 31.9 MGOe.
Tools needed:
 Tube FurnaceArgonPressure Gas CylinderHeat-Resistant Gloves
6
6
Magnetise the magnets
Magnetise the magnets
Unknown: how the sintered magnets are magnetised. Sagawa measures them on a B-H tracer but gives no magnetising field or apparatus.
Tools needed:
 Unknown Magnetising Method
Materials
3- 584 gPlaceholder
- 86.4 gPlaceholder
- 334.9 gPlaceholder
Tools Required
14- Placeholder
- Placeholder
- Placeholder
- Placeholder
- Placeholder
- Placeholder
- Placeholder
- Placeholder
- Placeholder
- Placeholder
- Placeholder
- Placeholder
- Placeholder
- Placeholder
This blueprint makes
Related Blueprints
These blueprints share knowledge with this one — techniques, materials, or principles that connect them in the learning graph.

CC0 Public Domain
This blueprint is released under CC0. You are free to copy, modify, distribute, and use this work for any purpose, without asking permission.
Support the Maker by purchasing products through their Blueprint where they earn a Maker Commission set by Vendors, or create a new iteration of this Blueprint and include it as a connection in your own Blueprint to share revenue.