NGHỆ THUẬT
LÀM ĐẸP VÀ SỨC KHỎE
THỦ CÔNG
VĂN HÓA VÀ LỊCH SỬ
GIẢI TRÍ
MÔI TRƯỜNG
THỰC PHẨM VÀ ĐỒ UỐNG
KỸ THUẬT NGƯỢC
KHOA HỌC
THỂ THAO
CÔNG NGHỆ
THIẾT BỊ ĐEO

The Surface Is the Job: Plating Fails Before the Current Is Switched On
A plated coating is held on by nothing but the bond between two metals in contact. There is no glue, no key, no mechanical interlock worth counting on — just atoms of one metal sitting on atoms of another.
So anything between them prevents it: oxide, grease, dust, fingerprints, polishing compound, the film of oil that a bare hand leaves. A coating deposited on a dirty surface looks identical to one deposited on a clean surface and peels off in a month.
**Adhesion is decided entirely before the current is switched on.** That is the single most important fact in metal finishing, and it is why the preparation takes longer than the plating.
Trung cấp
3 hours
Hướng dẫn
1
1
What is actually on a metal surface
What is actually on a metal surface
A piece of metal that looks clean carries several layers, and each needs a different removal method.
**Oxide.** Every metal except gold grows one in air, within seconds. On aluminium it re-forms faster than it can be removed, which is why aluminium is plated through a special intermediate process rather than directly.
**Oil and grease.** Machining oil, rust preventative, and skin oil. A fingerprint is a real and sufficient cause of failure.
**Solid soils.** Polishing compound, buffing wax, abrasive grit embedded in a soft metal, swarf.
**Scale.** Heavy oxide from heat treatment or hot working, which is a different problem from the thin air-formed film.
**Previous coatings.** Paint, lacquer, or an old plating layer.
**The order matters and it is always the same:** mechanical first, then degrease, then pickle, then plate — because degreasing a scaly part just makes clean scale, and pickling a greasy part does nothing at all, since the acid cannot reach the metal through the oil.
Vật liệu cho bước này:
 Tấm thép mềm2 cái
 Tấm đồng đỏ1 cái
Công cụ cần thiết:
 Kính lúp thợ kim hoàn
2
2
The water-break test, which settles it
The water-break test, which settles it
There is one test for surface cleanliness and it takes five seconds.
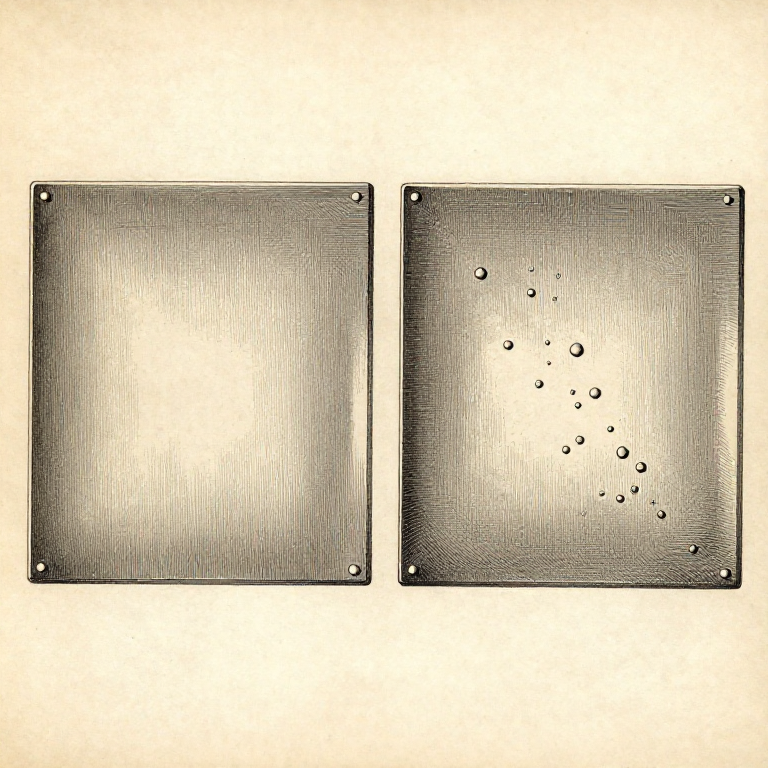
**Rinse the part in clean water and lift it out.** A properly clean metal surface holds an unbroken continuous film of water over its whole area. A surface with any oil left on it makes the water pull back into beads and patches, and where it breaks is where the plating will fail.
That is the **water-break test**, and it is the only cleanliness check the industry relies on, because it tests the thing that actually matters — whether the solution can wet the surface.
**A part that passes must go straight into the next bath.** A clean surface re-oxidises in air in seconds and picks up airborne oil in minutes. This is why a plating line is a sequence with no pauses, and why the part is never put down or handled after cleaning.
**Never touch it again with bare hands.** Gloves or clean tongs from the degreasing stage onwards. The commonest single cause of a peeling patch is a thumb print in the middle of it, and its shape gives it away.
**Rinse between every bath, thoroughly.** Carrying acid into an alkaline bath or alkali into an acid one neutralises both and contaminates the plating solution.
Vật liệu cho bước này:
Tấm thép mềm2 cái Nước cất1 cái
Công cụ cần thiết:
 Găng tay chống hóa chất
 Cốc thuỷ tinh borosilicat
3
3
Mechanical preparation, and what it leaves behind
Mechanical preparation, and what it leaves behind
**Plating does not hide anything — it reveals it.** A bright nickel coating on a scratched surface is a bright scratched surface, and often more visible than before, because the bright finish catches the light on every mark.
So the substrate must be finished to the standard the final part needs, before plating, not after.
**Abrasive stages, each removing the last one's marks:** coarse to fine emery, then polishing compound if a bright finish is wanted, working in alternate directions so the previous grit's scratches are visibly gone before moving on. This is exactly the sequence the stropping and mirror-polishing blueprints describe, and it is the same discipline.
**Then remove what the polishing left.** Polishing compound is grease plus abrasive, and it is bonded into the surface by the heat of buffing. It is one of the most stubborn soils there is, and it is why a highly polished part needs the most aggressive degreasing.
**Blasting** gives a matt, uniform, genuinely clean surface with a slight roughness that helps adhesion — but it embeds particles of the blast medium, so the medium must be chosen with the plating in mind.
**Sharp edges and burrs will not plate evenly.** The next rungs explain why: the current crowds onto them. Break every edge before plating.
Vật liệu cho bước này:
Tấm thép mềm2 cáiCông cụ cần thiết:
 Bộ bàn chải sắt
 Thước cặp điện tử 6 inch
 Vải nhám emeri
4
4
Choosing the coating for the job
Choosing the coating for the job
Different coatings protect in completely different ways, and choosing on appearance alone is how a part rusts from a scratch.
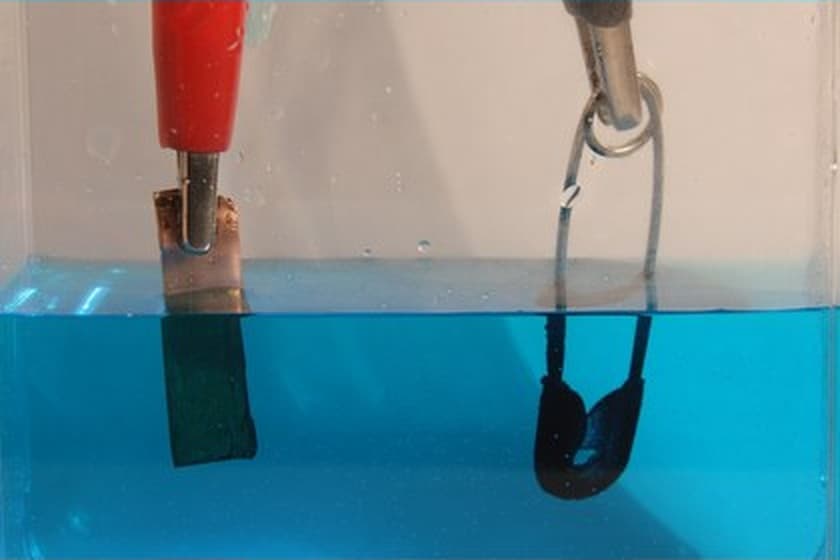
**Sacrificial coatings** are less noble than the substrate, so they corrode instead of it. **Zinc on steel** is the classic: scratch galvanized steel and the zinc around the scratch protects the exposed iron electrochemically. This is why galvanizing works on a rough part in weather.
**Barrier coatings** are more noble than the substrate and protect only by covering it. **Nickel or chromium on steel** is a barrier — scratch it and the steel rusts faster than bare steel would, because the coating drives the corrosion at the break. A barrier coating must be complete to be worth anything.
That single distinction explains most plating decisions:
* **zinc** — cheap corrosion protection for steel in weather, sacrificial
* **nickel** — hard, corrosion resistant, the usual undercoat, barrier
* **chromium** — very hard and bright, always over nickel, very thin, barrier
* **copper** — soft, an excellent undercoat because it levels and it plates onto awkward substrates
* **tin** — non-toxic, solderable, food contact
* **anodising** — not a plating at all: it grows a thick oxide out of the aluminium itself, so it cannot peel
Most decorative work is copper, then nickel, then chromium, each doing a different job.
Vật liệu cho bước này:
 Tấm niken1 cáiTấm đồng đỏ1 cáiTấm thép mềm1 cái
Vật liệu
4- 2 cáiTạm thời
- 1 cáiTạm thời
- 1 cáiTạm thời
- 1 cáiTạm thời
Công cụ yêu cầu
6- Tạm thời
- Tạm thời
- Tạm thời
- Tạm thời
- Tạm thời
- Tạm thời
Blueprint liên quan
Các blueprint này chia sẻ kiến thức — kỹ thuật, vật liệu hoặc nguyên tắc

CC0 Phạm vi công cộng
Bản thiết kế này được phát hành theo CC0. Bạn tự do sao chép, sửa đổi, phân phối và sử dụng cho bất kỳ mục đích nào mà không cần xin phép.
Hỗ trợ nhà sáng tạo bằng cách mua sản phẩm qua bản thiết kế, nơi họ nhận Hoa hồng nhà sáng tạo do nhà bán hàng đặt, hoặc tạo phiên bản mới và kết nối trong bản thiết kế riêng để chia sẻ doanh thu.