NGHỆ THUẬT
LÀM ĐẸP VÀ SỨC KHỎE
THỦ CÔNG
VĂN HÓA VÀ LỊCH SỬ
GIẢI TRÍ
MÔI TRƯỜNG
THỰC PHẨM VÀ ĐỒ UỐNG
KỸ THUẬT NGƯỢC
KHOA HỌC
THỂ THAO
CÔNG NGHỆ
THIẾT BỊ ĐEO
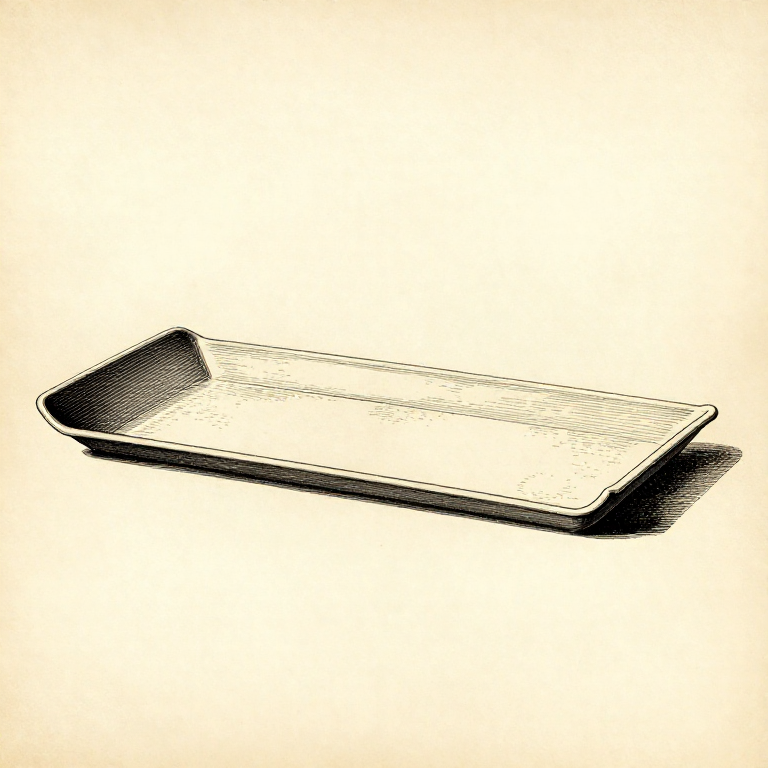


Warping: Why Big Flat Parts Lift at the Corners
Plastic goes down hot and shrinks as it cools. Each new layer shrinks onto the layers below, which have already cooled and cannot follow — so every layer pulls inward on the one beneath it.
Near the middle of a part those pulls cancel. At a corner they do not, and the corner lifts off the plate. That is warping, and it is why it always starts at corners and always on long flat parts.
The cure is not more adhesive. It is keeping the whole part near one temperature so the shrinkage happens evenly — which is what a heated bed does, what an enclosure does, and what choosing PLA over ABS does.
Trung cấp
3 hours
Hướng dẫn
1
1
Material first: some plastics barely warp
Material first: some plastics barely warp
PLA shrinks very little and warps very little. ABS shrinks several times as much and will warp off an open printer almost regardless of what else you do. PETG and ASA sit between them.
So the first question about a warping part is whether it needs to be in that material at all. A prototype that only has to hold a shape is a PLA part; ABS is chosen for heat resistance or solvent smoothing, and then the warping is a cost accepted in exchange.
Wet filament makes everything worse. Moisture absorbed from the air turns to steam at the nozzle, which gives poor layer welds and a rough surface — and a part with weak layers warps more because the layers cannot hold each other. A filament dryer is not an accessory for hygroscopic materials, it is required.
Vật liệu cho bước này:
 Sợi in 3D (PLA)1 cái
 Sợi ABS1 cái
 Sợi nhựa ASA1 cái
Công cụ cần thiết:
 Máy sấy sợi in
 Máy in 3D sợi nhựa (FDM)
2
2
Keep the part hot: bed, enclosure, no draughts
Keep the part hot: bed, enclosure, no draughts
A heated bed keeps the lower layers above the temperature where the plastic goes rigid, so they can still move as the upper ones shrink. That is why bed temperature matters far beyond the first layer.
An ENCLOSURE does the same for the whole part. It is the single most effective measure for ABS and ASA, and it costs nothing to test — a cardboard box over the printer will tell you in one print whether it is the answer.
And stop the draughts. A printer near an open window or a door will produce a part that warps on one side only, which is a genuinely confusing fault until the cause is noticed. Turning the cooling fan DOWN for ABS is the same idea applied deliberately.
Vật liệu cho bước này:
Sợi ABS1 cáiCông cụ cần thiết:
 Buồng che máy in 3D (chống cháy)Máy in 3D sợi nhựa (FDM)
 Tấm in của máy in 3D (thép lò xo phủ PEI)
3
3
Design the corners away
Design the corners away
Warping concentrates at sharp corners, so round them. A 5 mm radius on the corners of a large flat part removes most of the stress concentration and often fixes warping on its own — at no cost in material or time.
MOUSE EARS are the crude version: small thin discs added at each corner that spread the adhesion, printed as part of the model and snapped off afterwards. They are ugly and they work.
A BRIM does the same thing all the way round: a flat skirt of extra first layer attached to the part. A RAFT goes further and prints the whole part on a sacrificial platform, which helps adhesion but adds a rough bottom face — so a brim is usually the better trade.
Vật liệu cho bước này:
Sợi in 3D (PLA)1 cáiCông cụ cần thiết:
 Phần mềm cắt lớp tệp 3MF
 Máy tính để bàn
 Dụng cụ gọt ba via
4
4
Reduce the area that can pull
Reduce the area that can pull
A long flat part warps because there is a long flat run of cooling plastic pulling on itself. Break that up and the force has nowhere to accumulate.
Splitting a big part into two printed pieces and joining them removes the problem entirely, and often prints faster because both halves can be oriented better. Cutting large windows or lightening holes into a flat panel does the same thing for the same reason.
Lower infill also helps, because there is less material contracting. That is a real trade against strength, and it is the next rung — but it is worth knowing that a warping part and an over-infilled part are often the same part.
Vật liệu cho bước này:
Sợi in 3D (PLA)1 cáiCông cụ cần thiết:
Phần mềm cắt lớp tệp 3MFMáy tính để bàn Thước cặp điện tử 6 inch
Công cụ yêu cầu
8- Máy sấy sợi inHoa hồng 10%Tạm thời
- Tạm thời
- Buồng che máy in 3D (chống cháy)Hoa hồng 10%Tạm thời
- Tấm in của máy in 3D (thép lò xo phủ PEI)Hoa hồng 10%Tạm thời
- Tạm thời
- Tạm thời
- Tạm thời
- Tạm thời
Blueprint liên quan
Các blueprint này chia sẻ kiến thức — kỹ thuật, vật liệu hoặc nguyên tắc


CC0 Phạm vi công cộng
Bản thiết kế này được phát hành theo CC0. Bạn tự do sao chép, sửa đổi, phân phối và sử dụng cho bất kỳ mục đích nào mà không cần xin phép.
Hỗ trợ nhà sáng tạo bằng cách mua sản phẩm qua bản thiết kế, nơi họ nhận Hoa hồng nhà sáng tạo do nhà bán hàng đặt, hoặc tạo phiên bản mới và kết nối trong bản thiết kế riêng để chia sẻ doanh thu.