Ukusebenzisana
UBUCIKO
UBUHLE NEMPILO
UBUCIKO BEZANDLA
AMASIKO NOMLANDO
EZOKUZIJABULISA
IMVELO
UKUDLA NEZIPHUZO
REVERSE ENGINEERING
IZAYENSI
EZEMIDLALO
UBUCHWEPHESHE
IZINTO EZIGQOKWAYO
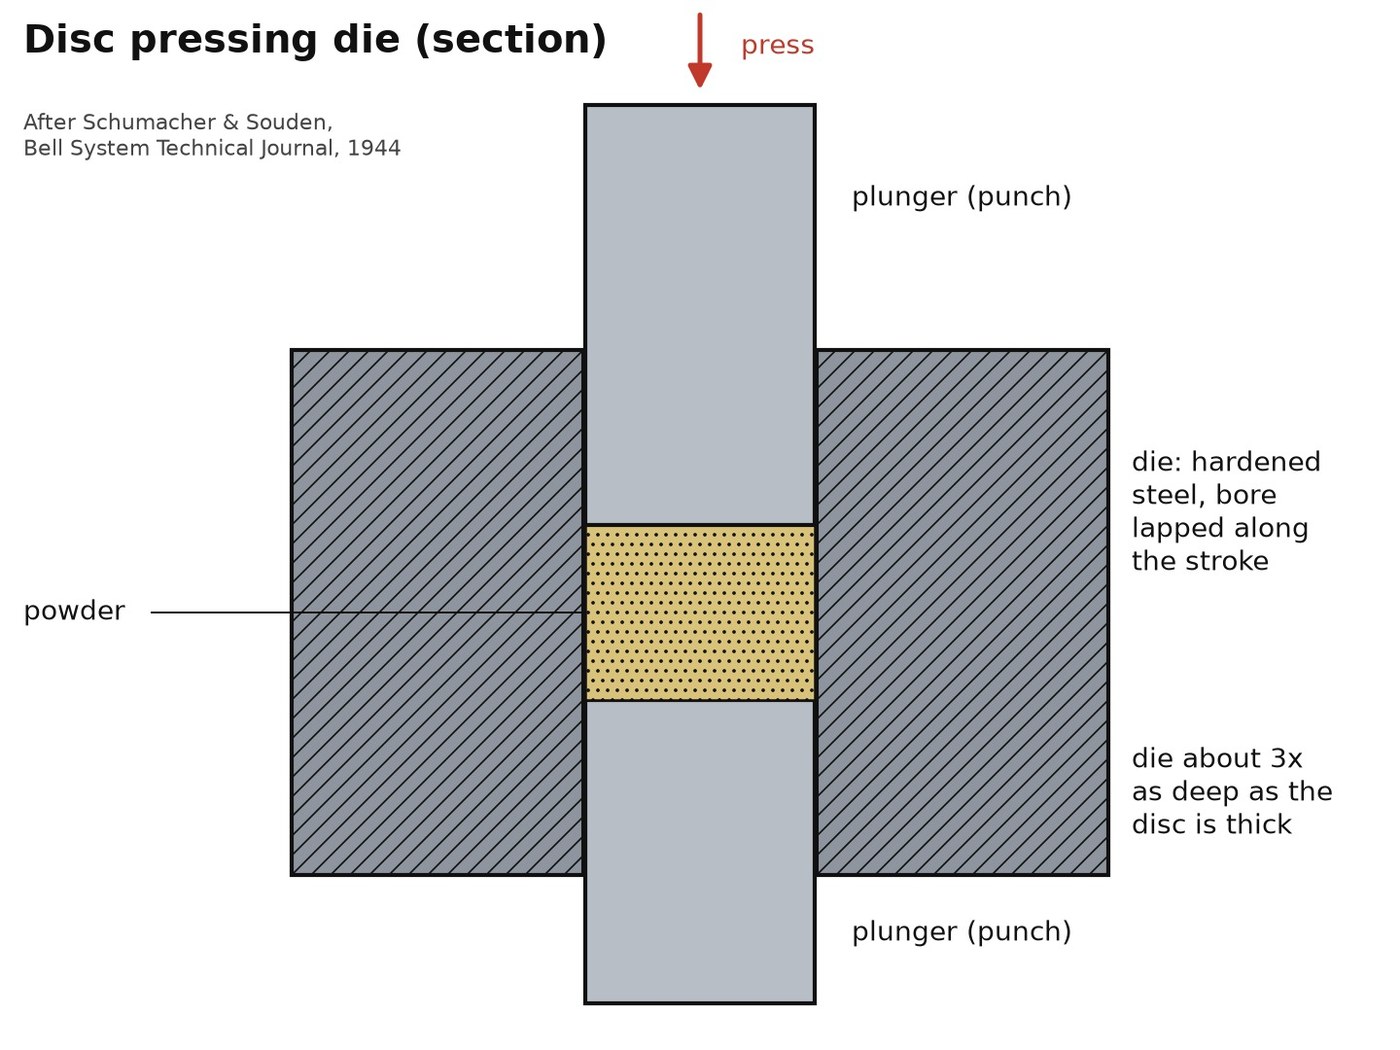

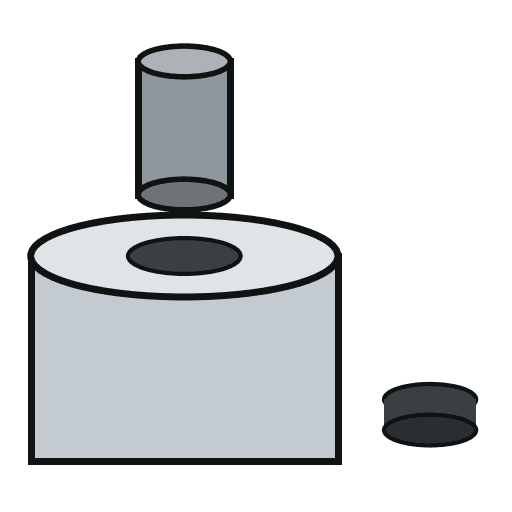
Disc Pressing Die: Hardened Steel, the Bore Lapped Along the Stroke (Schumacher & Souden, 1944)
The die in which powder is pressed into a flat disc: a block of hardened steel with a round bore, and close-fitting plungers that press the powder in it. The bore is lapped with rouge along the stroke, so its last fine scratches run the way the disc comes out.
Result: a die for pressing metal or ceramic powders into discs, at 5 to over 100 tons per square inch.
Source: E. E. Schumacher and A. G. Souden, Some Aspects of Powder Metallurgy, Bell System Technical Journal 23 (1944), pp. 431-433 and 454-455. Unknown: the steel, the hardening, sizes and clearances. Picture drawn by Youblob.
Osezingeni eliphezulu
Unknown
Imiyalelo
1
1
Make the die and plungers
Make the die and plungers
Make the die of steel with a round bore through it, and plungers that fit the bore closely; there must be some clearance between them. Make the bore about three times as deep as the disc will be thick. Light, fluffy powders need a deeper die and longer plungers. Ours: tool steel for the die, and a lathe to bore and turn. Not given: the steel, sizes, clearance, the plungers' metal.
Izinto zokwakha zalesi sinyathelo:
 Induku eyisikwele yensimbi yamathuluzi1 die
 Insimbi engaziwa1 plungers
Amathuluzi adingekayo:
 Umshini Wokuphendula Insimbi
 Izilinganiso ezingaziwa
2
2
Harden the die
Harden the die
Harden the die. For very abrasive powders, make the die of hard carbide or line it with carbide instead. Ours: a heat-treating oven and a quench. Not given: the hardening heat and quench.
Amathuluzi adingekayo:
 Uhhavini lokwelapha ngokushisa
 Ibhakede lokupholisa
3
3
Lap the bore along the stroke
Lap the bore along the stroke
Polish the bore to a high finish by lapping with polishing rouge, moving the lap in the direction of the plunger stroke. The fine scratches that remain then run the way the pressed disc is pushed out, not across it.
Amathuluzi adingekayo:
 Ubomvu bomenzi wobucwebe
4
4
Press a disc
Press a disc
Fill the bore with powder and press it with the plungers in a mechanical or hydraulic press, at 5 to over 100 tons per square inch. The powder hardly flows sideways, and friction at the die wall makes the pressure uneven: a part that is long for its width may come out with a soft, less dense middle. Push the disc out along the bore.
Amathuluzi adingekayo:
 Umshini wokucindezela we-hydraulic
Izinto
2- Isibambeli
- 1 plungersIsibambeli
Amathuluzi Adingekayo
6- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
Izinto Zokwakha Ze-Blueprint Exhunyiwe
10% Ukwabiwa
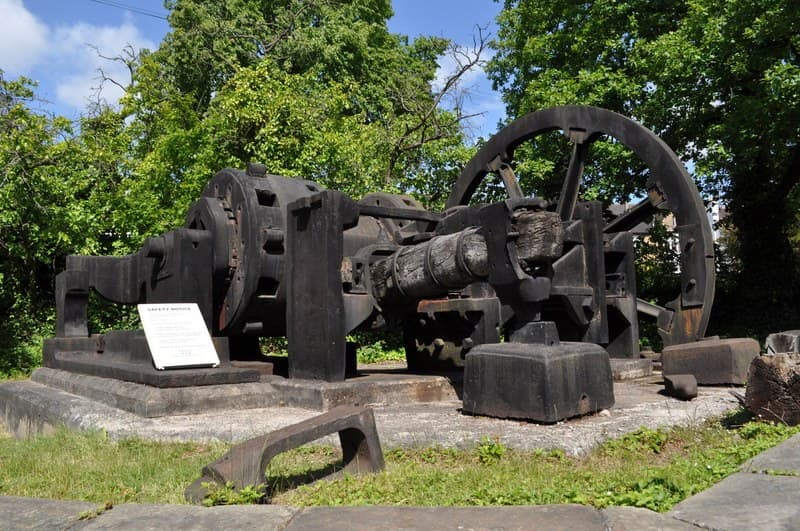
Tool-Steel Bar: Crucible Steel Drawn Out at a Cherry-Red Heat
ngu-Forge
Umkhandi
32
0
0
0
5
0
10% Ukwabiwa
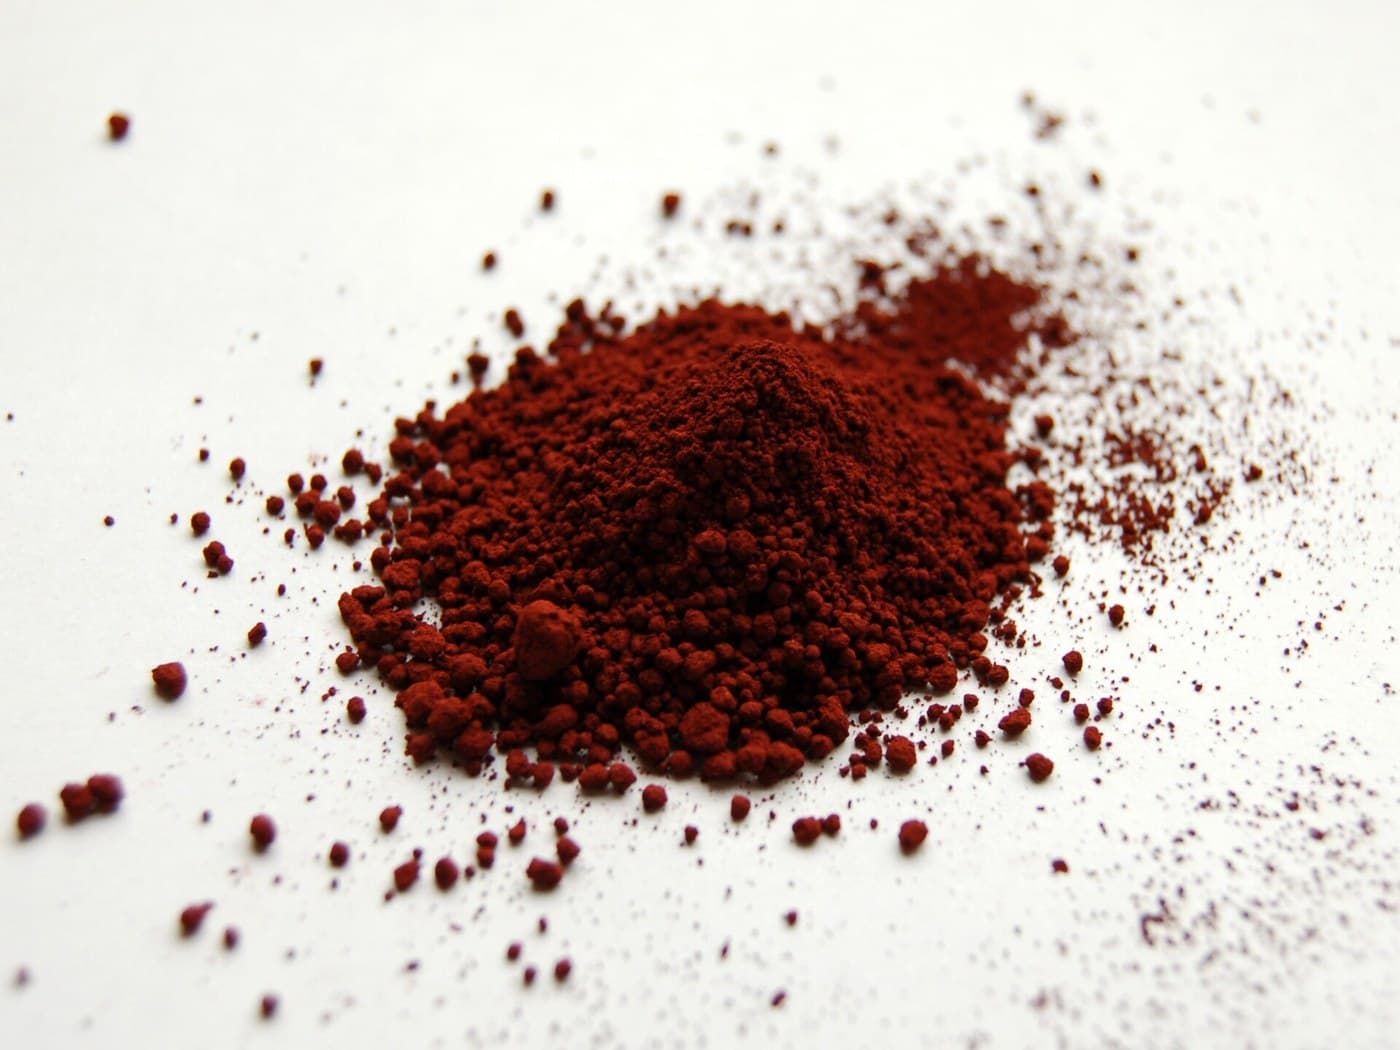
Jewellers' Rouge Precipitated from Copperas, Ure 1839
ngu-Charlie
Inorganic
12
0
0
0
1
0
10% Ukwabiwa
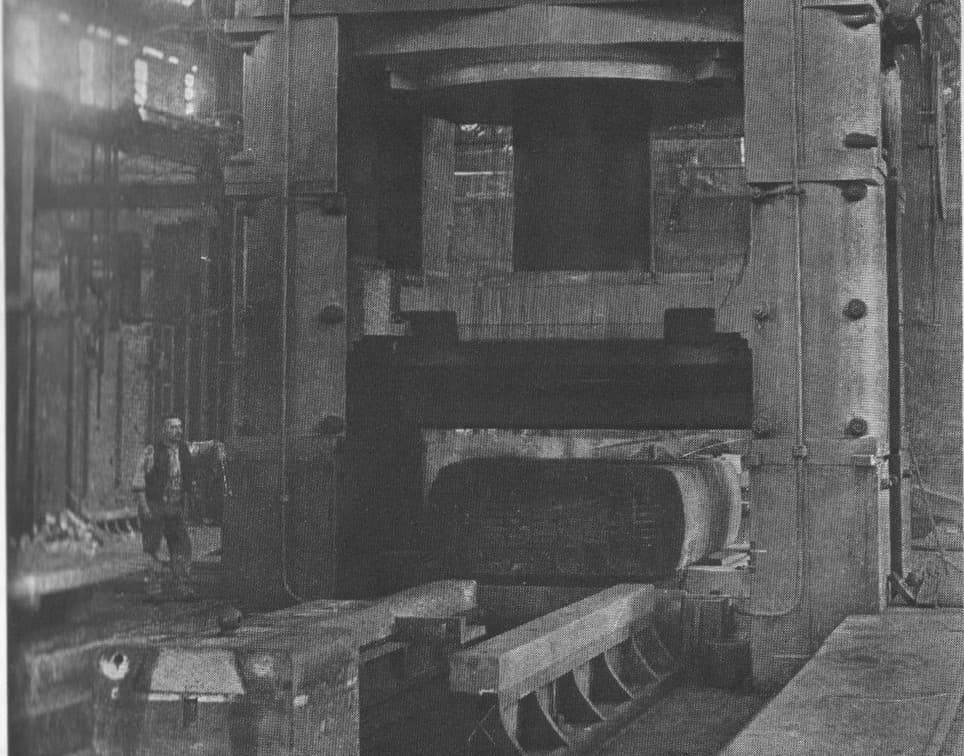
Hydraulic Press
ngu-Emma
Umsebenzi Wensimbi
54
0
0
0
10
0

10% Ukwabiwa
Building a Screw-Cutting Lathe — The Machine That Makes Other Machines
ngu-Gimli
Umsebenzi Wensimbi
57
0
0
0
4
0
Le blueprint yenza
CC0 Isizinda Somphakathi
Le blueprint ikhishwe ngaphansi kwe-CC0. Ukhululekile ukukopisha, ukuguqula, ukusabalalisa, nokusebenzisa ngaphandle kwemvume.
Sekela uMenzi ngokuthenga imikhiqizo nge-Blueprint yabo IKhomishane Yomenzi kumiswe ngabathengisi, noma dala inguqulo entsha yale Blueprint bese uyifaka njengoxhumaniso ku-Blueprint yakho ukuze wabelane ngemali engenayo.