UBUCIKO
UBUHLE NEMPILO
UBUCIKO BEZANDLA
AMASIKO NOMLANDO
EZOKUZIJABULISA
IMVELO
UKUDLA NEZIPHUZO
REVERSE ENGINEERING
IZAYENSI
EZEMIDLALO
UBUCHWEPHESHE
IZINTO EZIGQOKWAYO
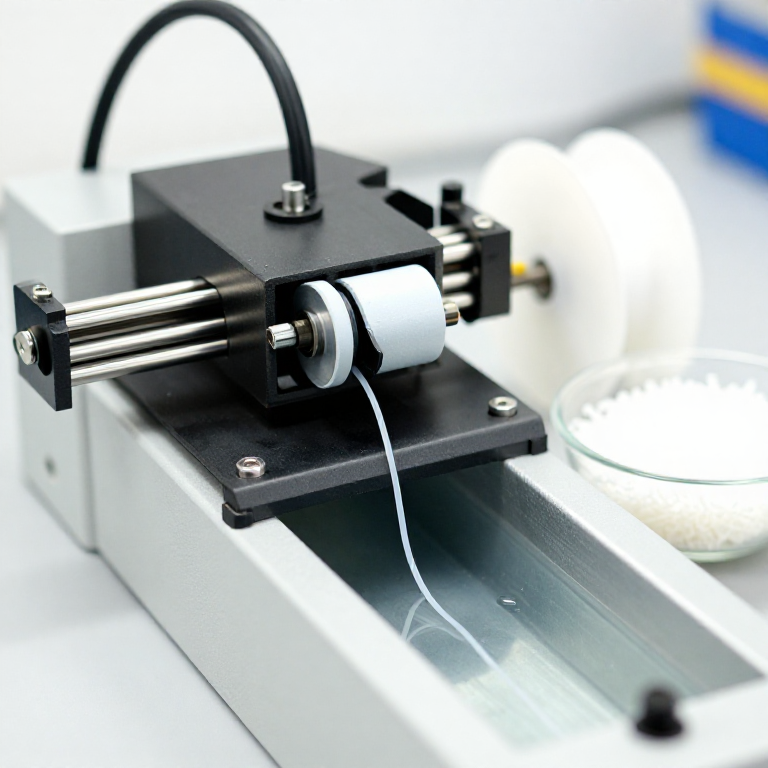

3D Printer Filament Extruded from Pellets
Filament is made the way a 3D printer prints, only continuously: dry plastic pellets fall from a hopper onto a turning screw inside a heated barrel, melt as they are carried forward, and are pushed out through a round nozzle. The strand is cooled in air or a water bath, drawn by a puller at a steady speed so it keeps its diameter, and wound on a spool. Commercial 1.75 mm filament is typically held to about ±0.02 mm; a small line should be measured.
PETG and many other plastics take up moisture, which makes bubbles and weak prints: makers dry PETG at about 55–70 °C for 5–8 hours, depending on the resin. Melt temperatures follow the resin's datasheet; PETG is usually printed at about 230–260 °C.
Ophakathi
A day per few kilograms
Imiyalelo
1
1
Dry the pellets
Dry the pellets
Dry the pellets in a dryer as the resin maker specifies; for PETG about 55–70 °C for 5–8 hours.
Izinto zokwakha zalesi sinyathelo:
 Ama-pellet e-PETG2 kg
 Amagremu wepulasitiki eliphelayo (PLA)2 kg
 Ama-pellet e-ABS2 kg
Amathuluzi adingekayo:
 Isomisi sama-pellet
 Isikali Sedijithali Sasekhishini
2
2
Heat the barrel
Heat the barrel
Set the barrel's heating zones to rise from the hopper end to the nozzle within the resin's datasheet range and let them settle.
Amathuluzi adingekayo:
 Ibharela Ye-extruder Enesikulufu Esisodwa
 Isitsha sokufaka amaphilisi
3
3
Extrude
Extrude
Fill the hopper and start the screw slowly. Purge until the strand comes out clear of old material and bubbles.
Amathuluzi adingekayo:
Ibharela Ye-extruder Enesikulufu EsisodwaIsitsha sokufaka amaphilisi Amagilavu Amelana Nokushisa
 Izibuko zokuphepha
4
4
Cool and pull
Cool and pull
Lead the strand through a water bath or past the fan to the puller. Adjust the puller's speed: faster pulls the strand thinner, slower lets it swell.
Izinto zokwakha zalesi sinyathelo:
 Amanzi50 amalitha
Amathuluzi adingekayo:
 Umgqomo omkhulu wepulasitiki wamalitha angu-100
 Ifeni yebhokisi (isivinini esiguqukayo)
 Isidonsi nesisongi sentambo
5
5
Measure and wind
Measure and wind
Measure the diameter every few metres and wind the filament on a spool. Keep it sealed and dry.
Amathuluzi adingekayo:
 I-Caliper Yedijithali Yamayintshi Ayi-6Isidonsi nesisongi sentamboIsikali Sedijithali Sasekhishini
6
6
Troubleshooting
Troubleshooting
Filament extrusion troubleshooting.
Flow
Loading...
Izinto
4- Isibambeli
- Isibambeli
- 2 kgIsibambeli
- 50 amalithaIsibambeli
Amathuluzi Adingekayo
10- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
Le blueprint yenza



CC0 Isizinda Somphakathi
Le blueprint ikhishwe ngaphansi kwe-CC0. Ukhululekile ukukopisha, ukuguqula, ukusabalalisa, nokusebenzisa ngaphandle kwemvume.
Sekela uMenzi ngokuthenga imikhiqizo nge-Blueprint yabo IKhomishane Yomenzi kumiswe ngabathengisi, noma dala inguqulo entsha yale Blueprint bese uyifaka njengoxhumaniso ku-Blueprint yakho ukuze wabelane ngemali engenayo.