UBUCIKO
UBUHLE NEMPILO
UBUCIKO BEZANDLA
AMASIKO NOMLANDO
EZOKUZIJABULISA
IMVELO
UKUDLA NEZIPHUZO
REVERSE ENGINEERING
IZAYENSI
EZEMIDLALO
UBUCHWEPHESHE
IZINTO EZIGQOKWAYO
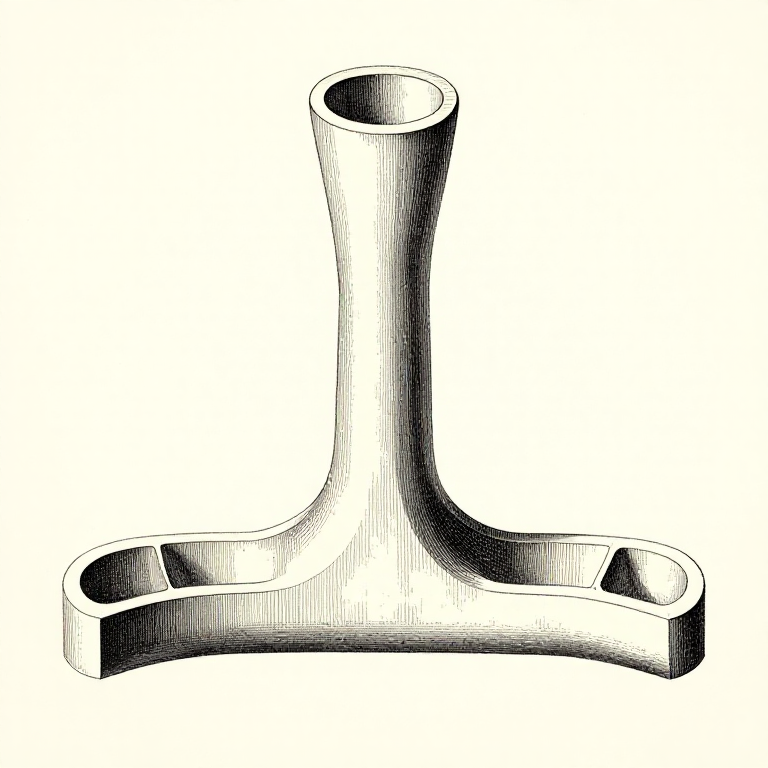


Gating: Getting the Metal In Without Wrecking the Mould
Molten metal poured straight into a cavity arrives fast, turbulent and full of air. It washes sand off the mould walls, folds oxide skin into itself, and the casting is full of inclusions before it has even frozen.
The GATING SYSTEM exists to prevent that. A sprue to take the metal down, a runner to carry it sideways and slow it, and gates to let it into the cavity smoothly — each part doing one job.
The governing principle is that the system should fill and stay full. A gating system running only partly full drags air in with the metal, which is precisely what it was built to avoid.
Osezingeni eliphezulu
3 hours
Imiyalelo
1
1
Sprue, runner, gate — three parts, three jobs
Sprue, runner, gate — three parts, three jobs
The SPRUE is the vertical channel the metal is poured into. It should be TAPERED, wider at the top, because falling metal accelerates and narrows — a parallel sprue leaves a gap around the stream that sucks in air.
The RUNNER is the horizontal channel at the bottom. It distributes metal and slows it down, and it is usually in the drag with the gates in the cope so that any floating dross stays in the runner.
The GATES are the small openings from runner into cavity. Several small gates fill more gently than one large one and let the mould fill from more than one place, which matters on anything long or thin.
Izinto zokwakha zalesi sinyathelo:
 Isihlabathi sokubumba1 kg
Amathuluzi adingekayo:
 Ibhokisi lokubumba (elingaphezulu nelingaphansi)
 Irula
 I-Caliper Yedijithali Yamayintshi Ayi-6
2
2
Choke the system, and where
Choke the system, and where
Ilayisha incwadi ye-Jupyter…
Izinto zokwakha zalesi sinyathelo:
 Ingqimba yebhronzi1 ucezuIsihlabathi sokubumba1 kg
Amathuluzi adingekayo:
 Ikhompyutha YasetafuleniI-Caliper Yedijithali Yamayintshi Ayi-6Ibhokisi lokubumba (elingaphezulu nelingaphansi)
3
3
Traps, filters and a pouring basin
Traps, filters and a pouring basin
A POURING BASIN at the top of the sprue lets you fill it and keep it full, so the sprue never runs empty mid-pour. Pouring straight into a bare sprue hole guarantees an interrupted, air-entraining stream at the start.
A runner extension beyond the last gate — a DIRT TRAP — gives the first, dirtiest metal somewhere to go that is not the casting. It costs a few centimetres of runner and catches the slag that came down the sprue first.
Ceramic foam FILTERS do the same job far better and are cheap. They also slow and smooth the flow, which is why a filter often improves a casting for two reasons at once.
Izinto zokwakha zalesi sinyathelo:
Isihlabathi sokubumba1 kgAmathuluzi adingekayo:
Ibhokisi lokubumba (elingaphezulu nelingaphansi)Irula Isikhethi esinenetha encane
4
4
Pour steadily and keep the basin full
Pour steadily and keep the basin full
Start the pour and bring the basin up to full quickly, then hold it there until the mould is full. A pour that starts timidly and then speeds up entrains air at the very start, which is the metal that ends up deepest in the casting.
Never stop and restart. A pause lets the stream break, lets air in, and can leave a COLD SHUT where the metal that stopped has skinned over before the rest arrives.
Have enough metal melted before you start. Running out halfway is the single most avoidable failure in a foundry, and it is prevented by weighing the pattern, multiplying by the alloy's density ratio, and adding a generous allowance for the gating and risers — which is usually a third of the total again.
Izinto zokwakha zalesi sinyathelo:
Ingqimba yebhronzi1 ucezu Amalahle1 ucezu
Amathuluzi adingekayo:
 Ikhezo lokuthela insimbi encibilikile
 Udlawu Lwesitsha Sokuncibilikisa
 Izibuko ezimnyama zokubasa
 Amagilavu Esikhumba Anemikhono Emide
Izinto
3- Isibambeli
- 1 ucezuIsibambeli
- 1 ucezuIsibambeli
Amathuluzi Adingekayo
9- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
Le blueprint yenza
Ama-blueprint ahlobene
Lama-blueprint abelana ngolwazi — amasu, izinto noma izimiso


CC0 Isizinda Somphakathi
Le blueprint ikhishwe ngaphansi kwe-CC0. Ukhululekile ukukopisha, ukuguqula, ukusabalalisa, nokusebenzisa ngaphandle kwemvume.
Sekela uMenzi ngokuthenga imikhiqizo nge-Blueprint yabo IKhomishane Yomenzi kumiswe ngabathengisi, noma dala inguqulo entsha yale Blueprint bese uyifaka njengoxhumaniso ku-Blueprint yakho ukuze wabelane ngemali engenayo.