Ukusebenzisana
UBUCIKO
UBUHLE NEMPILO
UBUCIKO BEZANDLA
AMASIKO NOMLANDO
EZOKUZIJABULISA
IMVELO
UKUDLA NEZIPHUZO
REVERSE ENGINEERING
IZAYENSI
EZEMIDLALO
UBUCHWEPHESHE
IZINTO EZIGQOKWAYO
English


Plastic Syringe Set: Moulded Barrel and a Soft Polyethylene Piston
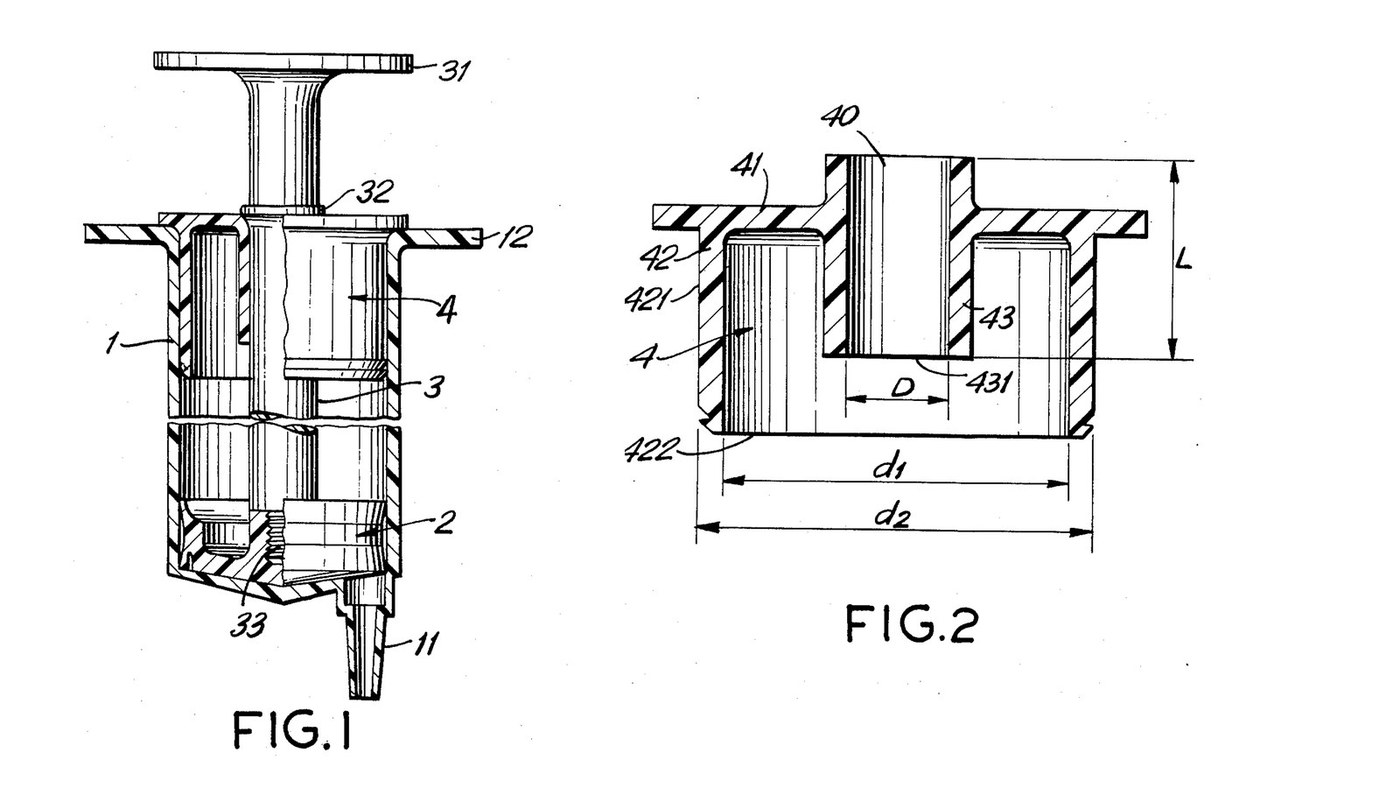
Four moulded parts make a plastic syringe with no rubber seal and no grease: a stiff barrel with a taper nozzle, a bell-shaped piston whose thin polyethylene lips seal against the wall, a slim plunger shaft, and a cap whose long sleeve guides the shaft so it cannot bend and tilt the piston (Adorján & Dávid, US 4,704,105, 1987). Mould one set of moulds per size for a set of syringes for hydraulic models.
The piston figures are the patent's. Polypropylene, LDPE, the sizes and the mould making are ours. Not for medical use. The picture: Figs. 1-2.
Osezingeni eliphezulu
3 days (moulds) + 1 hour per batch
Imiyalelo
1
1
The moulding process
The moulding process
Drying, mould, injection, cooling and inspection all follow this blueprint. The steps below add only what the syringe needs.
2
2
Mill the barrel mould
Mill the barrel mould
Mill a two-plate mould for the barrel (1): a stiff-walled tube closed at one end by a nozzle (11) with a standard needle taper (ours: the Luer taper), and two finger grips (12) at the open end. One mould per syringe size you want, for example 5, 50 and 60 ml (ours).
Amathuluzi adingekayo:
 Umshini Wokusika Insimbi
 Ingxenye ye-aluminium yesibumbo sokujova (amapuleti 2)
 Uhlaka lwembumbo yokujova
3
3
Mill the piston mould
Mill the piston mould
The piston (2) is a bell: a rim 5-7 mm high whose two edges flare out into lips 0.3-0.5 mm thick, a front groove 0.3-0.5 mm wide and 2-2.5 mm deep, and a central shank. The lips must come out 0.2-0.6 mm wider than the barrel bore; the rim between them no wider than the bore.
Amathuluzi adingekayo:
Umshini Wokusika InsimbiIngxenye ye-aluminium yesibumbo sokujova (amapuleti 2)Uhlaka lwembumbo yokujova I-Caliper Yedijithali Yamayintshi Ayi-6
4
4
Mill the shaft and cap moulds
Mill the shaft and cap moulds
Shaft (3): thumb rest (31), a bead (32) and an end projection (33) a little larger than the piston's bore. Cap (4): a disc with an outer collar (42) that force-fits the barrel and an inner sleeve (43) at least as long as the shaft is thick.
Amathuluzi adingekayo:
Umshini Wokusika InsimbiIngxenye ye-aluminium yesibumbo sokujova (amapuleti 2)Uhlaka lwembumbo yokujova5
5
Mould the barrels
Mould the barrels
Mould the barrels from virgin plastic. The patent asks only for a rigid plastic; ours: polypropylene.
Izinto zokwakha zalesi sinyathelo:
 Ama-pellet e-polypropylene1 batch
Amathuluzi adingekayo:
 Isomisi sama-pellet
 Umshini wokubumba ngokujova
6
6
Mould the pistons
Mould the pistons
Mould the pistons from virgin polyethylene, which the patent wants at 65-90 degrees Shore (scale not stated). Ours: LDPE; check your grade's data sheet.
Izinto zokwakha zalesi sinyathelo:
 Ama-pellet e-LDPE1 batch
Amathuluzi adingekayo:
Isomisi sama-pelletUmshini wokubumba ngokujova7
7
Mould the shafts and caps
Mould the shafts and caps
Mould shafts and caps. These may be reprocessed plastic, as they never touch the liquid. Ours: polypropylene.
Izinto zokwakha zalesi sinyathelo:
Ama-pellet e-polypropylene1 batchAmathuluzi adingekayo:
Umshini wokubumba ngokujova8
8
Check the lip size
Check the lip size
Measure the barrel bore and a piston's lips. The lips must be 0.2-0.6 mm wider than the bore. Adjust the mould if not.
Amathuluzi adingekayo:
I-Caliper Yedijithali Yamayintshi Ayi-69
9
Snap the shaft into the piston
Snap the shaft into the piston
Push the shaft's projection through the small bore at the back of the piston until it snaps into the wider cavity behind it.
10
10
Assemble
Assemble
Push the piston into the barrel. Thread the shaft through the cap's sleeve and force the cap's outer collar into the open end of the barrel. Its end face now stops the piston when you draw it fully back.
11
11
Lock the cap
Lock the cap
Press two dents, opposite each other, through the barrel wall into the cap collar with a hot tool so the cap cannot pull out. Ours: a soldering iron tip.
Amathuluzi adingekayo:
 Insimbi Yokusoda Kagesi
12
12
Test the seal
Test the seal
Draw water and push it out, along the whole stroke, with no grease. It should move smoothly from the start and not leak past the lips. Note the size and file it into your set.
Amathuluzi adingekayo:
 Amanzi
 Ibhikha Lengilazi
Izinto
2- 1 batchIsibambeli
- 1 batchIsibambeli
Amathuluzi Adingekayo
9- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
- Isibambeli
Ama-blueprint ahlobene
Lama-blueprint abelana ngolwazi — amasu, izinto noma izimiso
CC0 Isizinda Somphakathi
Le blueprint ikhishwe ngaphansi kwe-CC0. Ukhululekile ukukopisha, ukuguqula, ukusabalalisa, nokusebenzisa ngaphandle kwemvume.
Sekela uMenzi ngokuthenga imikhiqizo nge-Blueprint yabo IKhomishane Yomenzi kumiswe ngabathengisi, noma dala inguqulo entsha yale Blueprint bese uyifaka njengoxhumaniso ku-Blueprint yakho ukuze wabelane ngemali engenayo.