ARTE
BELEZA E BEM-ESTAR
ARTESANATO
CULTURA E HISTÓRIA
ENTRETENIMENTO
MEIO AMBIENTE
COMIDA E BEBIDAS
ENGENHARIA REVERSA
CIÊNCIAS
ESPORTES
TECNOLOGIA
TECNOLOGIA VESTÍVEL
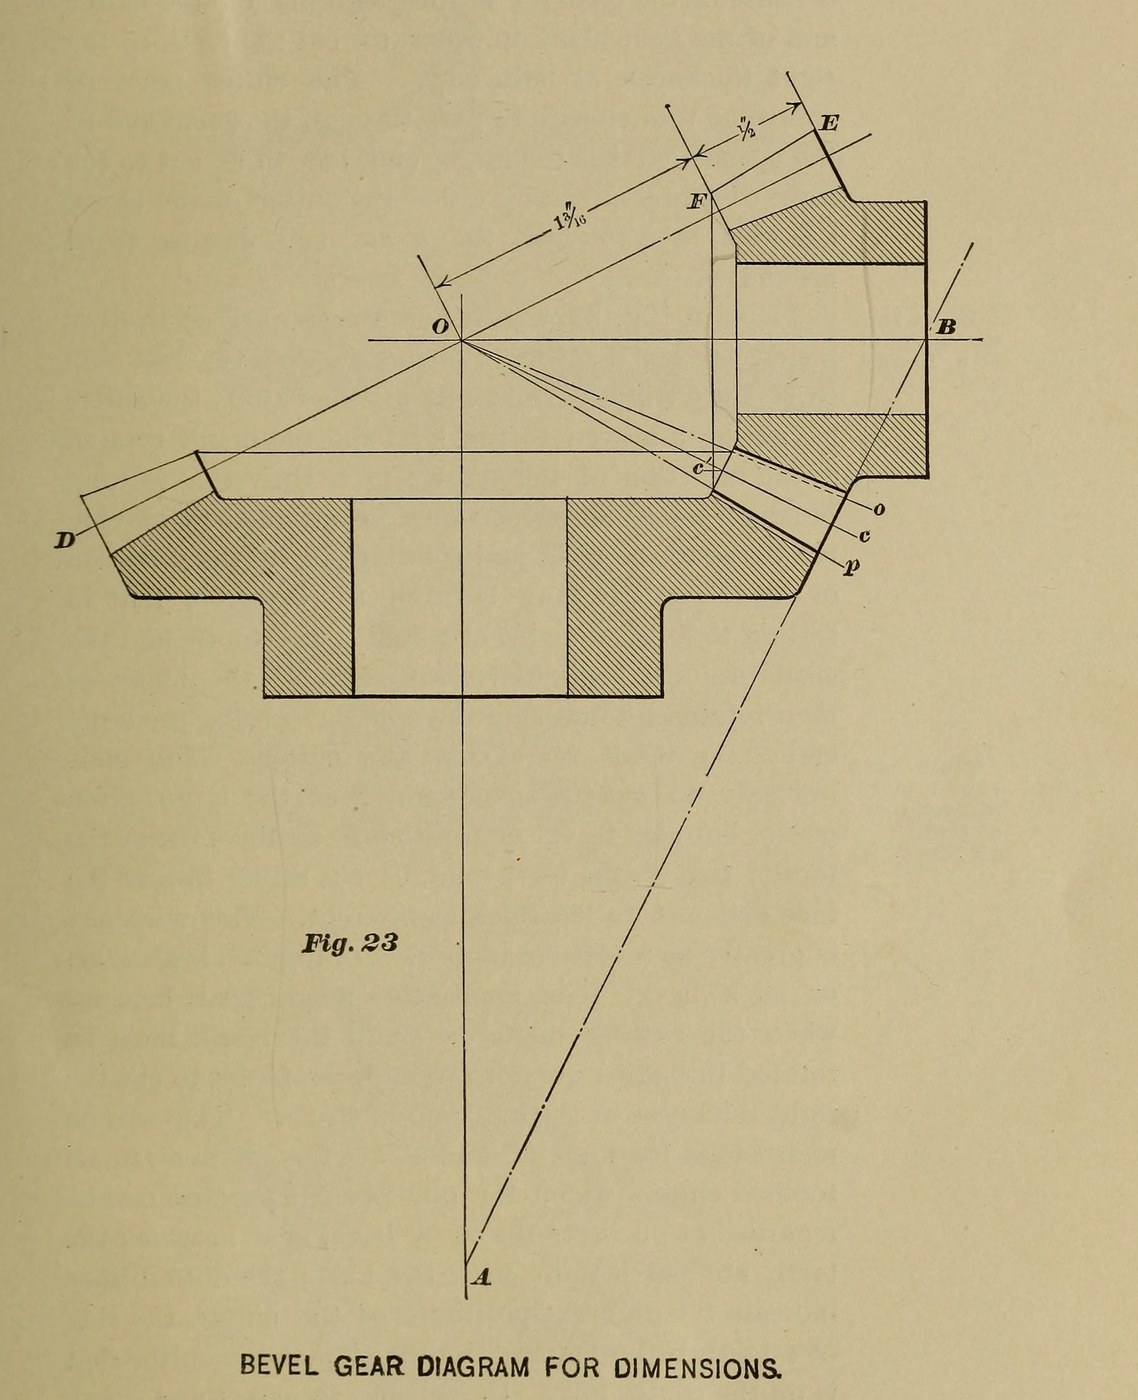


Bevel Pinion: 12 Teeth, 8 Pitch, for a 24-Tooth Gear (Brown & Sharpe 1911)
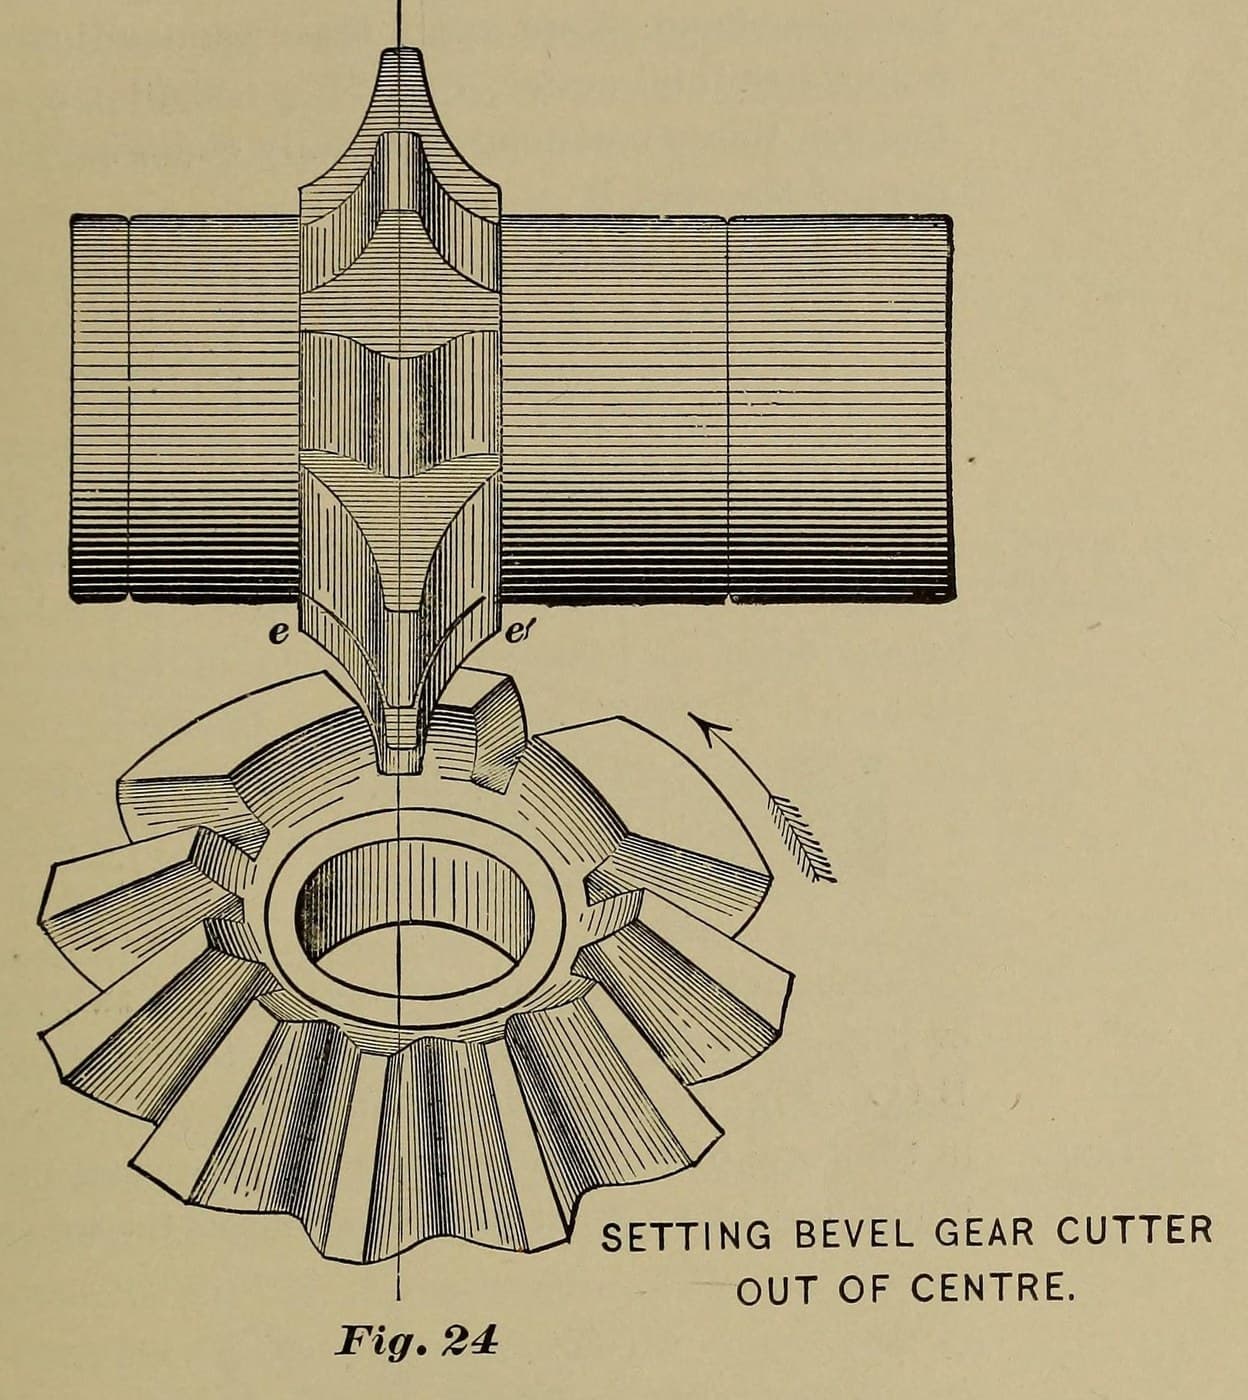
Brown & Sharpe's own worked example: the small gear of a 12 and 24 tooth bevel pair, 8 pitch, shafts at right angles, cut with the No. 8 cutter they send to anyone who orders one for this pinion. The method is the same as for mitre gears: set off centre, cut each side, file the small ends.
Source: Brown & Sharpe, Practical Treatise on Gearing (1911), Fig. 23 example, Part I ch. IX–X, Part II ch. III and the set-over table p. 58. The blank sizes are our arithmetic with their rules; the steel and bore are ours. Picture: their Fig. 23.
Avançado
1 day
Instruções
1
1
Work out and turn the blank
Work out and turn the blank
Pitch diameter 12 ÷ 8 = 1.500 in. Angle of edge 26° 34′ and angle of face 59° 11′ (Brown & Sharpe's figures for every 12 and 24 tooth pair). Diameter increment = cos 26° 34′ × 0.250 = 0.224 in, so turn the steel blank to 1.72 in outside diameter. Face ½ in long. Try both angles with a protractor against the end of the hub.
Materiais para este passo:
 Barra de aço macio1 length for one blank
Ferramentas necessárias:
 Torno mecânico
 Ferramenta de corte para torno
 Transferidor
 Micrómetro
2
2
Choose the cutter
Choose the cutter
Twice the back cone radius × 8 comes to about 13, so a No. 8, 8-pitch bevel gear cutter. Measure its thickness Tc at the pitch line, 0.145 in from its tip.
Ferramentas necessárias:
 Fresa para engrenagens cónicas
 Paquímetro para dentes de engrenagem
3
3
Set the head at 22° 18′
Set the head at 22° 18′
Apex distance = sec 26° 34′ × 1.5 = 1.677 in. Angle increment: tan = sin 26° 34′ ÷ 6, giving 4° 16′. Set the dividing head to the cutting angle 26° 34′ − 4° 16′ = 22° 18′ and index 12 spaces. Depth at the large end 0.270 in.
Ferramentas necessárias:
 Fresadora
 Cabeçote divisorFresa para engrenagens cónicas
4
4
Set over and cut one side
Set over and cut one side
Apex distance ÷ face = 3.35; we take the nearest column, 3¼, where a No. 8 cutter has the factor .286. Set-over = Tc ÷ 2 − .286 ÷ 8 = Tc ÷ 2 − 0.036 in. Set off centre by that amount, take up backlash, and cut round all 12 spaces.
Ferramentas necessárias:
FresadoraCabeçote divisorFresa para engrenagens cónicas5
5
Set over the other way and trim
Set over the other way and trim
Set over the same amount the other side, line the cutter up with the space at the small end, take a trial cut, and rotate toward the cutter until the tooth is 0.196 in thick at the large end and 0.138 in at the small end. Check with the gear tooth vernier, then cut round.
Ferramentas necessárias:
FresadoraCabeçote divisorFresa para engrenagens cónicasPaquímetro para dentes de engrenagem6
6
File the small ends
File the small ends
File the teeth rounder at the small ends, where the cutter could not, without filing them thinner at the pitch line. The cutting angle is under 30°, so the spaces may come out narrower at the face than the cutter suggests; Brown & Sharpe's own shop used a No. 6 cutter here instead.
Ferramentas necessárias:
 Lima fina
Materiais
1- 1 length for one blankReferência
Ferramentas necessárias
9- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
Este projeto faz
Blueprints relacionados
Estes blueprints compartilham conhecimento — técnicas, materiais ou princípios
CC0 Domínio Público
Este blueprint é liberado sob CC0. Você é livre para copiar, modificar, distribuir e usar este trabalho para qualquer finalidade, sem pedir permissão.
Apoie o Maker comprando produtos através do Blueprint, onde ele ganha uma Comissão Maker definida pelos vendedores, ou crie uma nova versão deste Blueprint e inclua-o como conexão no seu próprio Blueprint para compartilhar receita.