ARTE
BELEZA E BEM-ESTAR
ARTESANATO
CULTURA E HISTÓRIA
ENTRETENIMENTO
MEIO AMBIENTE
COMIDA E BEBIDAS
ENGENHARIA REVERSA
CIÊNCIAS
ESPORTES
TECNOLOGIA
TECNOLOGIA VESTÍVEL
Cooling Is a Process Too: Still Air, Insulated, or Quenched
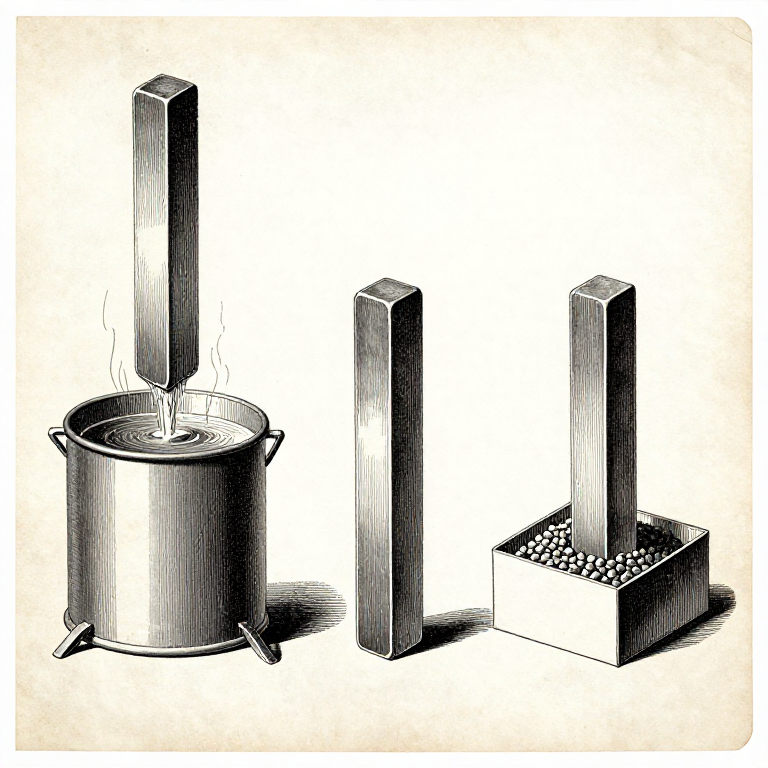
How something cools decides as much about its final state as how it was heated. The same steel, at the same temperature, becomes glass-hard, tough, or dead soft depending entirely on the rate it comes down.
There are three speeds a workshop uses deliberately. QUENCHING is as fast as possible. NORMALISING is still air. ANNEALING is as slow as you can contrive, usually by burying the work in something insulating and leaving it overnight.
Choosing one is choosing the properties of the finished piece, and doing it by accident is how a part ends up too hard to file or too soft to hold an edge.
Intermediário
3 hours
Instruções
1
1
The three rates and what each produces
The three rates and what each produces
QUENCH into water, brine or oil and the steel has no time to transform gradually — it traps into a hard, brittle structure that then must be tempered. The published heat-treatment blueprint is this sequence in full.
NORMALISE by standing the work in still air and it cools at a moderate rate, giving a fine even grain and a predictable, machinable state. This is the default after forging and the reset button for a piece with a confused history.
ANNEAL by burying it in ash, vermiculite or dry lime, or by switching off the furnace and letting it cool with the work inside. That gives the softest, most workable condition — which is what you want before machining, filing or cold bending, and what the steel supplier delivers bar stock in.
Materiais para este passo:
 Barra de aço macio2 peças
 Água1 peça
Ferramentas necessárias:
 Forja de ferreiro
 Tenazes de ferreiro
 Luvas de couro de canhão longo
2
2
Thin cools faster than thick, in the same piece
Thin cools faster than thick, in the same piece
The surface-to-volume argument from the heating rung runs unchanged in reverse. A thin edge in a quench cools far faster than a thick spine a centimetre away.
That is exploited deliberately: a blade hardens at the edge and stays tougher in the spine because of this alone, and clay-coating the spine — as Japanese swordmaking does — exaggerates the effect on purpose.
It is also a hazard. Sharp changes of section cool at very different rates, so they contract at different rates, and the stress from that is what cracks a piece in the quench. A generous radius at every corner is the fix, and it is designed in rather than added later.
Materiais para este passo:
Barra de aço macio1 peçaÁgua1 peçaFerramentas necessárias:
Tenazes de ferreiro Lupa de joalheiroLuvas de couro de canhão longo
3
3
Slow cooling for ceramics and glass, and why
Slow cooling for ceramics and glass, and why
Glass and glazed ceramics must be cooled slowly through a particular range or they crack — sometimes on the way down, sometimes days later on the shelf.
The reason is the same temperature difference across the wall that the soak rung described, acting in reverse: the outside contracts while the inside is still hot and large, and the resulting tension exceeds what a brittle material can take. Metal yields and survives; ceramic and glass do not yield, so they break.
Annealing glass means holding it at a temperature where stress can relax, then cooling slowly enough that none builds again. It is the single most common reason an otherwise good piece fails, and the failure often happens long after the kiln is cold — which makes it hard to connect to its cause.
Ferramentas necessárias:
 Forno cerâmico
 Forno de alta temperatura
 Termopar com mostrador
4
4
Never guess with something hot, and never put it down carelessly
Never guess with something hot, and never put it down carelessly
Hot steel looks identical to cold steel below about 500 °C, and it stays hot enough to cause a serious burn for a long time after it stops glowing.
Adopt one habit and keep it absolutely: anything that has been in the fire is hot until you have proved otherwise. Test by bringing a hand near it rather than touching, or by touching a scrap of paper to it and seeing whether it scorches. Put hot work in one designated place, always the same place, and tell anyone else in the shop where that is.
The same applies to quench tanks — water thrown out of one by a large hot piece is scalding — and to fire itself: a banked fire looks dead and is not. None of this is a reason not to do the work; it is the small set of habits that make it ordinary rather than risky.
Materiais para este passo:
Água1 peçaFerramentas necessárias:
Luvas de couro de canhão longoTenazes de ferreiro Óculos escuros de forja
Ferramentas necessárias
8- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
Blueprints relacionados
Estes blueprints compartilham conhecimento — técnicas, materiais ou princípios
Quench Hardening and Tempering a Steel Blade — Heat Treatment Fundamentals
por Forge
Trabalho em Metal
72
0
0
0
4
0
The Surface Is Not the Centre: Thermal Mass and Soak Time
por Penny
Trabalho em Metal
23
0
0
0
0
0
Reading Heat by Colour: The Oldest Thermometer, and Its Two Conditions
por Forge
Trabalho em Metal
20
0
0
0
0
0
CC0 Domínio Público
Este blueprint é liberado sob CC0. Você é livre para copiar, modificar, distribuir e usar este trabalho para qualquer finalidade, sem pedir permissão.
Apoie o Maker comprando produtos através do Blueprint, onde ele ganha uma Comissão Maker definida pelos vendedores, ou crie uma nova versão deste Blueprint e inclua-o como conexão no seu próprio Blueprint para compartilhar receita.