Colaboração
ARTE
BELEZA E BEM-ESTAR
ARTESANATO
CULTURA E HISTÓRIA
ENTRETENIMENTO
MEIO AMBIENTE
COMIDA E BEBIDAS
ENGENHARIA REVERSA
CIÊNCIAS
ESPORTES
TECNOLOGIA
TECNOLOGIA VESTÍVEL
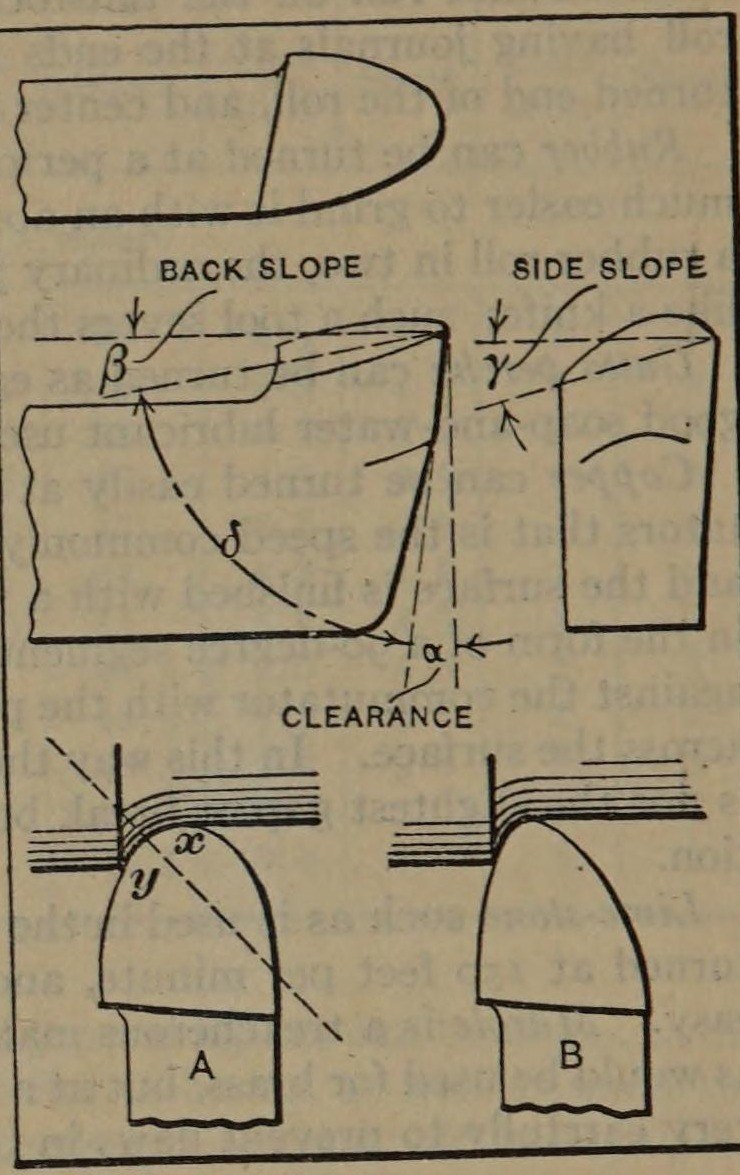


Lathe Cutting Tool: Ground to the Clearance and Slope for Each Metal (Machinery's Handbook, 1924)
A lathe turning tool ground from tool steel bar. Three things decide how well it cuts: the shape of the edge seen from above, the clearance under the edge, and the slope of the top the chip slides over. The Handbook gives the angles for each kind of metal to be turned.
Variable: the metal to be turned. Clearance 8 to 10° for general work, 12 to 14° for brass. Soft steel: back slope 8°, side slope 14 to 20°. Very hard steel: 5° and 9°. Brass: flat on top.
Source: Machinery's Handbook (1924), pp. 887-889, Tool Grinding. Unknown: the steel and the bar size. Picture: the Handbook's figure.
Intermediário
Unknown
Instruções
1
1
Choose the edge shape
Choose the edge shape
Grind the edge, seen from above, to suit the job. A large-radius edge roughs and keeps its edge at higher speed; a smaller point is better on flexible work that would chatter. A parting tool must be widest at the cutting edge so it does not bind in its groove. Ours: square tool steel bar. Not given: the steel, the bar size.
Materiais para este passo:
 Barra quadrada de aço para ferramentas1 tool blank
Ferramentas necessárias:
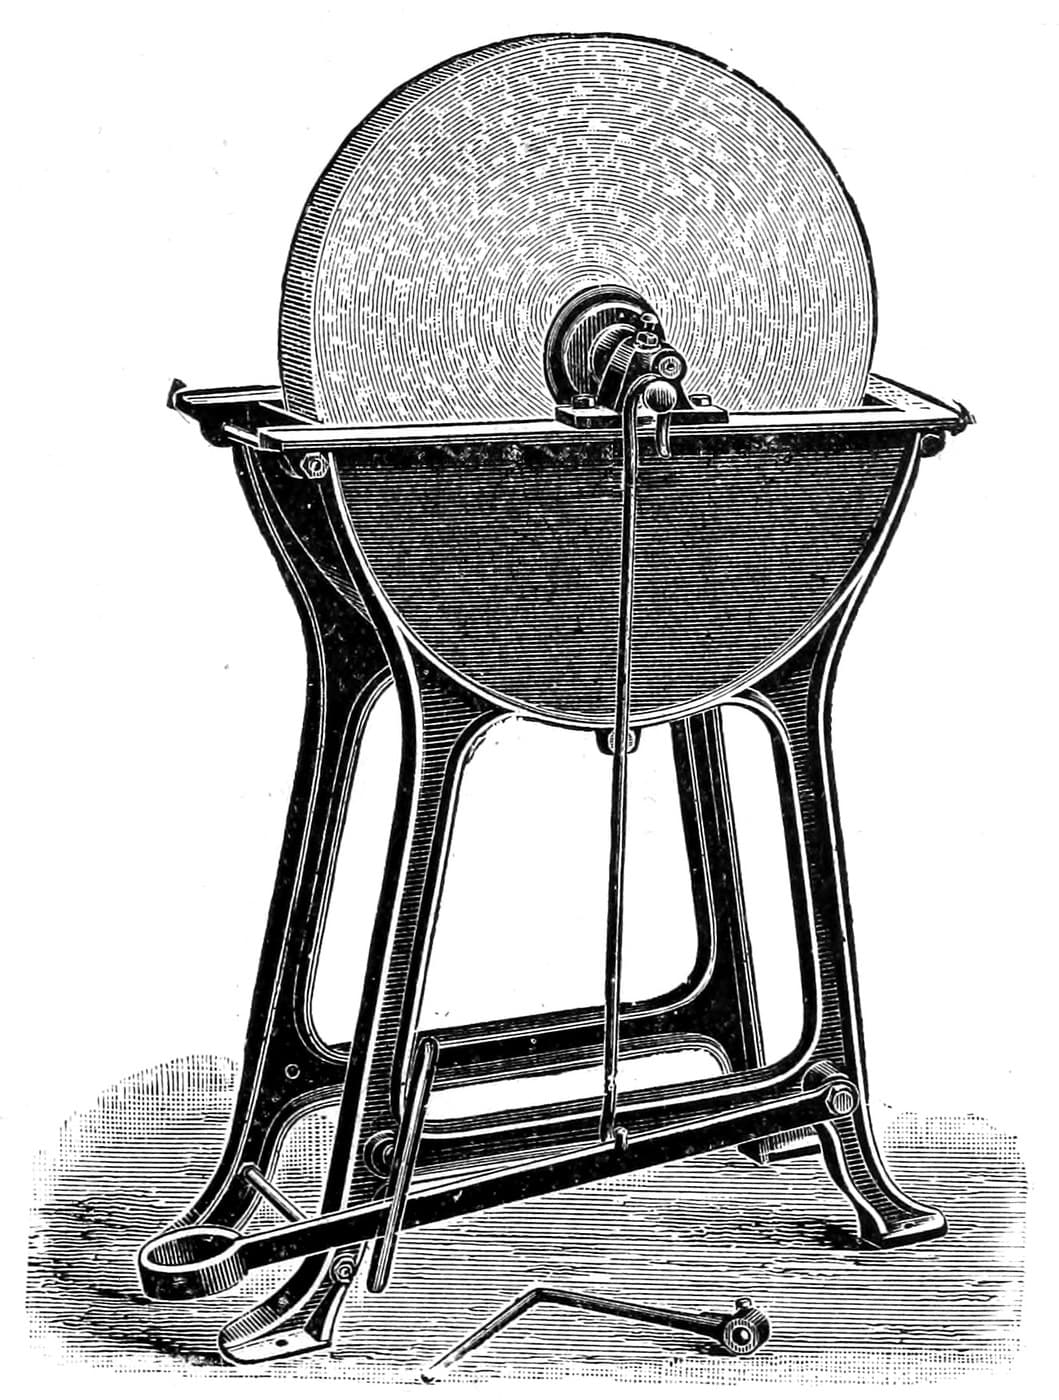
 Mó de afiar
 Água
2
2
Grind the clearance and the slope
Grind the clearance and the slope
Grind clearance under the edge: 8 to 10° for general turning, 12 to 14° for brass and soft metals; too much weakens the edge. Slope the top away from the working part of the edge. A roughing tool for medium or soft steel gets a back slope of 8° and a side slope of 14 to 20°; for very hard steel, 5° and 9°. A broad finishing tool slopes straight back. Thread tools and tools for brass or chilled iron are flat on top; very hard metals get almost no slope and little clearance. Roughing tools cut fastest with a lip angle near 61°, but cast iron cuts better at about 68°.
Ferramentas necessárias:
Mó de afiar Transferidor
3
3
Grind without burning
Grind without burning
Press the tool only moderately against the wheel and draw it away often, especially when grinding a broad flat face, so the edge does not overheat and burn. Keep the wheel supplied with plenty of cooling water.
Ferramentas necessárias:
Mó de afiarÁguaMateriais
1- 1 tool blankReferência
Materiais de Blueprints conectados

Este projeto faz

CC0 Domínio Público
Este blueprint é liberado sob CC0. Você é livre para copiar, modificar, distribuir e usar este trabalho para qualquer finalidade, sem pedir permissão.
Apoie o Maker comprando produtos através do Blueprint, onde ele ganha uma Comissão Maker definida pelos vendedores, ou crie uma nova versão deste Blueprint e inclua-o como conexão no seu próprio Blueprint para compartilhar receita.