Colaboração
ARTE
BELEZA E BEM-ESTAR
ARTESANATO
CULTURA E HISTÓRIA
ENTRETENIMENTO
MEIO AMBIENTE
COMIDA E BEBIDAS
ENGENHARIA REVERSA
CIÊNCIAS
ESPORTES
TECNOLOGIA
TECNOLOGIA VESTÍVEL
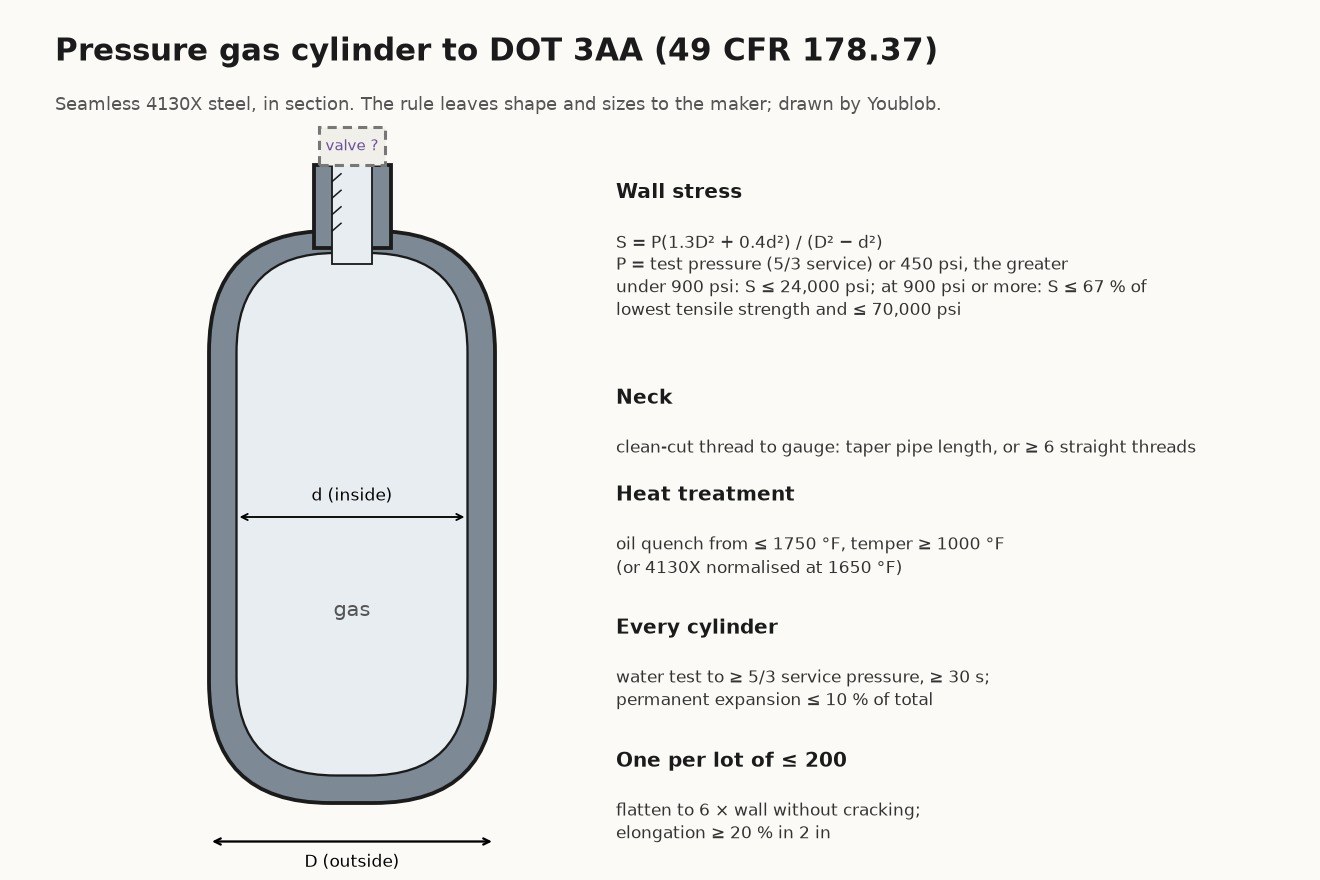


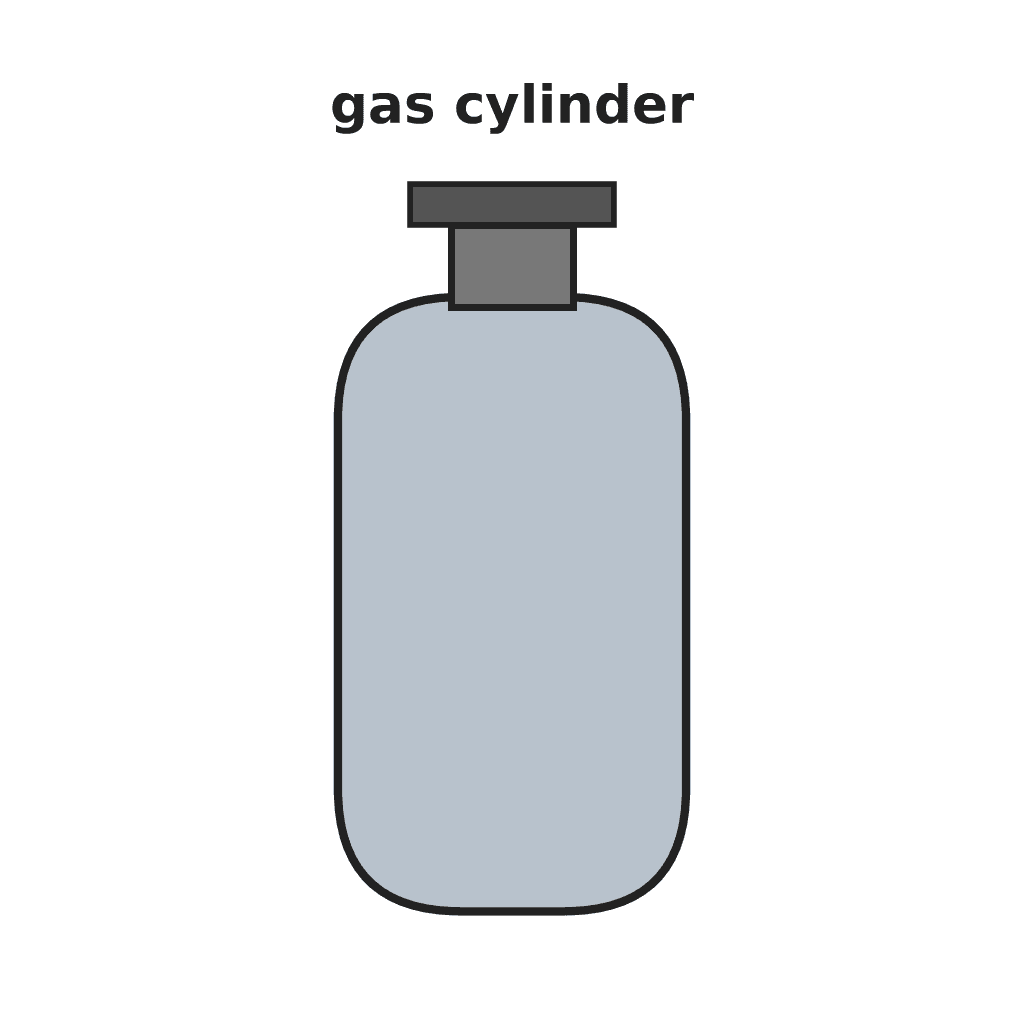
Pressure Gas Cylinder: Seamless 4130X Steel to DOT 3AA (49 CFR 178.37)
A seamless steel cylinder for compressed or liquefied gas, made to the US rule DOT 3AA: at least 150 psi service pressure, up to 1,000 lb of water capacity. The rule gives the steel, a formula for the wall, the heat treatment and the tests every cylinder or lot must pass. It does not say how the shell is formed.
Result: a seamless 4130X steel cylinder, heat-treated and proof-tested to 5/3 of its service pressure, with a threaded neck for its valve.
Source: 49 CFR 178.37, Specification 3AA. Unknown: how the shell is formed, the valve, the test apparatus. Picture drawn by Youblob.
Avançado
Unknown
Instruções
1
1
Size the wall
Size the wall
Pick the service pressure (at least 150 psi) and the diameter. Find the wall stress S = P(1.3D² + 0.4d²) / (D² − d²), with D and d the outside and inside diameters in inches and P the test pressure (5/3 of service pressure) or 450 psi, whichever is greater. Below 900 psi service, S may not pass 24,000 psi, and a cylinder over 5 in across needs a wall of at least 0.100 in. At 900 psi or more, S may not pass 67 % of the steel's lowest tensile strength, nor 70,000 psi.
Ferramentas necessárias:
 Dimensões desconhecidas
2
2
Get the steel
Get the steel
Use open-hearth, basic oxygen or electric steel of uniform quality, here 4130X: carbon 0.25-0.35 %, manganese 0.40-0.90 %, silicon 0.15-0.35 %, chromium 0.80-1.10 %, molybdenum 0.15-0.25 %, phosphorus 0.04 % and sulphur 0.05 % at most. For hot-drawn cylinders, mark each billet with its heat number.
Materiais para este passo:
 Tarugo de aço 41301 per cylinder
Ferramentas necessárias:
Dimensões desconhecidas3
3
Form the seamless shell
Form the seamless shell
Form the billet into a seamless cylinder with no fissures and a smooth, even surface; machine away any defects. A bottom closed by welding or spinning must be at least twice the minimum wall thick. Do not weld anything else, except neck and foot rings on cylinders of 500 psi or less. Not given: how the shell is formed (the rule names hot drawing from billet or plate, and spinning).
Ferramentas necessárias:
 Método de conformação desconhecidoDimensões desconhecidas
4
4
Thread the neck
Thread the neck
Cut a clean, even thread in the neck opening, to gauge. A taper thread must be at least as long as an American Standard taper pipe thread. A straight thread needs at least six engaged threads, a tight fit, a gasket, and a shear strength of at least ten times the test pressure.
Ferramentas necessárias:
 Jogo de machos e cossinetes
5
5
Heat-treat
Heat-treat
Heat-treat each finished cylinder evenly before testing. Quench it in oil or another suitable medium from the temperature right for the steel, no higher than 1750 °F, then temper at 1000 °F or more. Or normalise 4130X at 1650 °F instead, with no tempering. A cylinder quenched in water, or in anything cooling more than 80 % as fast, must be checked for quench cracks by magnetic particle, dye penetrant or ultrasound; a cracked one is scrapped.
Ferramentas necessárias:
 Forno de tratamento térmico
 Tina de têmpera com óleo
 Forno de revenido
6
6
Pressure-test every cylinder
Pressure-test every cylinder
Test each cylinder with water by the water-jacket or direct-expansion method of CGA C-1, to at least 5/3 of service pressure, held for at least 30 seconds and until it stops expanding. Between heat treatment and this test, never go above 90 % of test pressure. The permanent expansion may not pass 10 % of the total expansion. Not given: the CGA C-1 apparatus.
Ferramentas necessárias:
 Kit de ensaio de pressão hidráulica
7
7
Test one from each lot
Test one from each lot
From each lot of 200 or fewer, take one cylinder. Flatten it between two 60° knife edges rounded to ½ in radius, set across its axis: it must reach six times the wall thickness without cracking. Cut two tensile specimens from it: find the yield at 0.2 % offset, moving the cross-head no faster than ⅛ in per minute, and the tensile strength; elongation must be at least 20 % over 2 in (10 % on other gauge lengths). A rejected cylinder may be heat-treated again and retested, never repaired by welding or spinning.
Ferramentas necessárias:
 Prensa hidráulica
 Máquina de ensaio de materiais
8
8
Fit the valve
Fit the valve
Screw the valve into the threaded neck. A cylinder whose bottom was closed by spinning or by a plug must also pass a gas leak test: apply at least service pressure to one side of the clean, dry bottom for at least a minute, with the other side under water, and reject it at any leak. Not given: the valve.
Materiais para este passo:
 Válvula desconhecida1 peça
Ferramentas necessárias:
 Chave inglesa ajustável
Materiais
2- 1 per cylinderReferência
- 1 peçaReferência
Ferramentas necessárias
10- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
Materiais de Blueprints conectados


Este projeto faz
Blueprints relacionados
Estes blueprints compartilham conhecimento — técnicas, materiais ou princípios

CC0 Domínio Público
Este blueprint é liberado sob CC0. Você é livre para copiar, modificar, distribuir e usar este trabalho para qualquer finalidade, sem pedir permissão.
Apoie o Maker comprando produtos através do Blueprint, onde ele ganha uma Comissão Maker definida pelos vendedores, ou crie uma nova versão deste Blueprint e inclua-o como conexão no seu próprio Blueprint para compartilhar receita.