Colaboração
ARTE
BELEZA E BEM-ESTAR
ARTESANATO
CULTURA E HISTÓRIA
ENTRETENIMENTO
MEIO AMBIENTE
COMIDA E BEBIDAS
ENGENHARIA REVERSA
CIÊNCIAS
ESPORTES
TECNOLOGIA
TECNOLOGIA VESTÍVEL
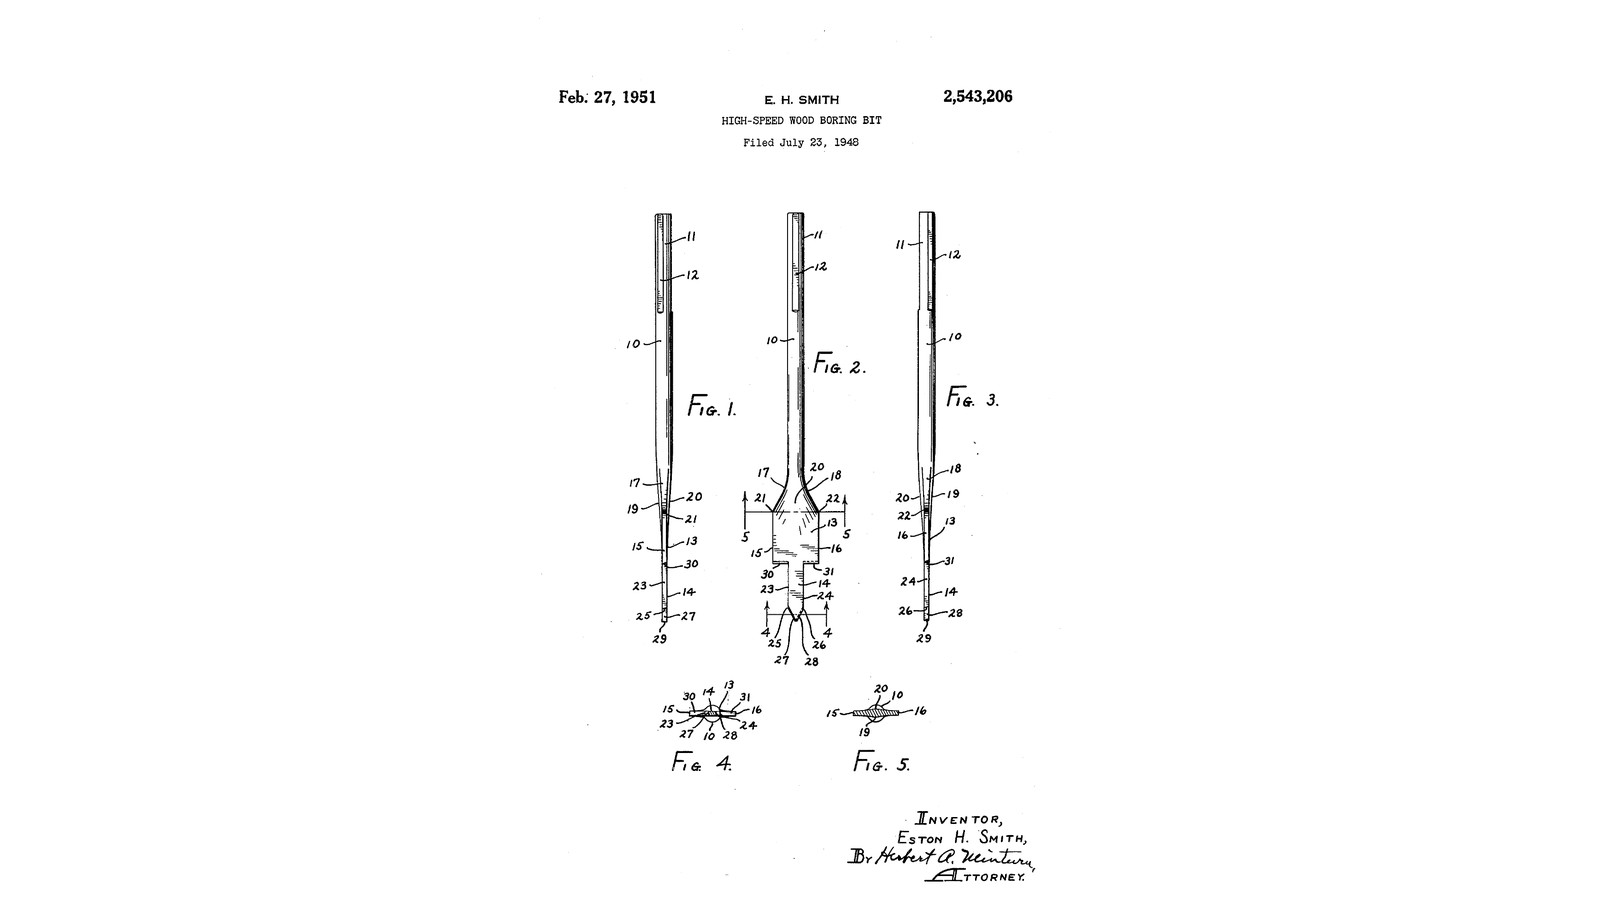


Long-Pilot High-Speed Wood Bits: A Flat Plate and a Long Square-Edged Pilot, No Screw Feed (Smith, 1951)
Eston H. Smith of Indianapolis received US 2,543,206, dated 27 February 1951, for a flat wood-boring bit made for the high speeds of an electric drill, 2,000 to 3,500 revolutions a minute. A flat plate on a thin stem has edges square to its faces and exactly the same width all the way down. A long flat pilot below it keeps the bit centred until it is through. With no screw feed it can bore at an angle, into another hole, or overlapping one, without splitting the wood. The thin stem leaves room for the shavings to come out.
We forge his 3/4 inch bit to his figures, with 1/2 and 1 inch bits beside it.
Intermediário
About 1 day
Instruções
1
1
His figures in millimetres
His figures in millimetres
A carregar o notebook Jupyter…
2
2
Read US 2,543,206
Read US 2,543,206
"It is extremely important however that these edges 15 and 16 be of exactly constant width from top to bottom, else the holes will not be bored true, and chattering and heating might develop."
3
3
Forge the blades
Forge the blades
Cut three 170 mm lengths of 10 mm octagonal tool steel. Heat 50 mm of one end to a bright orange in the forge and flatten it on the anvil to about 3 mm thick, centred on the bar. Hammer across it with the peen to spread it wider than the bit, about 2 mm over its size: 15, 21 and 27 mm. Draw the neck down smoothly where the blade meets the bar and keep the blade in line with it. Reheat as soon as the colour fades to red. Finally heat each one to a cherry red and let it cool slowly in the air, to soften it for filing.
Materiais para este passo:
 Barra octogonal de aço para ferramentas3 peças
Ferramentas necessárias:
 Serra de arco para metais
 Torno de bancada
 Forja
 Bigorna
 Martelo de forja
 Tenaz de forja
 Luvas de soldador
 Óculos de segurança
4
4
Print the grinding template
Print the grinding template
Full-size A4 template: the outlines of the 1/2, 3/4 and 1 inch bits with the long flat pilot. Print at 100 %; its 50 mm bar must measure 50 mm.
5
5
Grind the outline
Grind the outline
Glue each outline on its blade, centred on the bar, and grind to the lines on the bench grinder, dipping the steel in water often. Grind the faces flat and parallel to 2.4 mm (3/32 inch). Grind the plate's two side edges and the pilot's two side edges square to the faces and exactly parallel; check the plate's width with the caliper at the top and the bottom, it must not change. Grind three flats on the end of the stem, 20 mm long, for the chuck's jaws.
Ferramentas necessárias:
 Impressora de jato de tinta
 Cola
 Esmeriladora de bancada
 Balde de têmpera
 Água
 Jogo de limasTorno de bancada
 Paquímetro digital de 6 polegadasÓculos de segurança
6
6
Grind the clearances
Grind the clearances
The bit turns clockwise seen from the stem. Grind each cutting edge either side of the pilot square to the axis, with no top rake, and a clearance of 15 degrees behind it, on the face that trails. Grind the pilot's two point edges to 58 degrees included and give each a clearance of 9 degrees the same way. Leave a 1 mm flat at the tip, square to the axis.
Ferramentas necessárias:
Esmeriladora de bancadaBalde de têmperaÁguaJogo de limasTorno de bancada7
7
Harden and temper
Harden and temper
Heat the blade and the neck evenly to a cherry red, until a magnet no longer sticks to it, and quench it straight down in water, moving it up and down. Rub the faces bright with a stone. Heat the shank gently 30 mm behind the blade and watch the colours run down; quench again as soon as a dark straw colour reaches the shoulders and the point. Do the other two.
Ferramentas necessárias:
ForjaTenaz de forja Íman pequenoBalde de têmperaÁgua
 Pedra de amolarLuvas de soldadorÓculos de segurança
8
8
Sharpen and test
Sharpen and test
Hone the cutting edges on the shoulders and the point with the stone, keeping their angles, and take the burr off. Chuck a bit by its flats and bore a scrap of hardwood: it should start on the point without wandering, cut two clean shavings from the shoulders and leave a round hole of its own size; check it with the caliper.
Ferramentas necessárias:
Pedra de amolar Berbequim sem fios
 Tábua de madeira de leiPaquímetro digital de 6 polegadasÓculos de segurança
9
9
Troubleshooting
Troubleshooting
Long-pilot bit troubleshooting.
Flow
Loading...
10
10
History and honest limits
History and honest limits
**Eston H. Smith** of Indianapolis, assignor to Benjamin B. Aufderheide, US 2,543,206, dated 27 February 1951, filed 23 July 1948. He claimed a flat plate on a stem with a flat pilot, their edge faces at ninety degrees to their faces, a pilot point of 55 to 60 degrees with 8 to 10 degree clearances, and cutting edges square to the pilot with a clearance of between 15 and 20 degrees (his text says 10 to 20). His figures are for the 3/4 inch bit; the 1/2 and 1 inch bits are ours, with his pilot and edge height. His stem is about 1/4 inch with flats; ours is octagonal tool steel with three ground flats. He gives no material or heat treatment; those are ours.
Materiais
1- Referência
Ferramentas necessárias
19- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- Referência
- 1 vendor sell this, none ship to you yetReferência
- Referência
Ficheiros de design
1Este projeto faz

Blueprints relacionados
Estes blueprints compartilham conhecimento — técnicas, materiais ou princípios
CC0 Domínio Público
Este blueprint é liberado sob CC0. Você é livre para copiar, modificar, distribuir e usar este trabalho para qualquer finalidade, sem pedir permissão.
Apoie o Maker comprando produtos através do Blueprint, onde ele ganha uma Comissão Maker definida pelos vendedores, ou crie uma nova versão deste Blueprint e inclua-o como conexão no seu próprio Blueprint para compartilhar receita.