སྒྱུ་རྩལ
མཛེས་སྡུག་དང་བདེ་ཐང
བཟོ་རིག
རིག་གནས་དང་ལོ་རྒྱུས
དགའ་སྟོན
ཁོར་ཡུག
ཟས་དང་བཏུང་རྫས
ཕྱིར་འཕྲུལ་རིག
ཚན་རིག
རྩེད་འགྲན
རིག་རྩལ
གྱོན་རུང
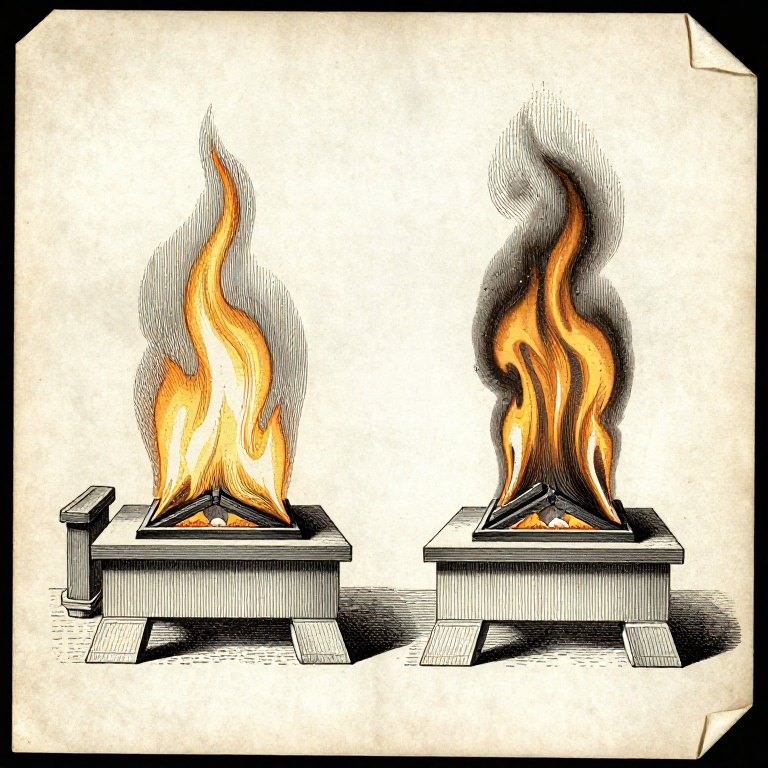

Oxidising, Neutral and Reducing: What the Fire Does to the Work
A fire is a chemical environment, not just a source of heat, and it changes the work while it heats it. Too much air and the surface oxidises and burns away; too little and the fire is cool and sooty; in between it does almost nothing to the steel.
Smiths call these OXIDISING, REDUCING and NEUTRAL. Potters call them the same and use them deliberately — a reduction firing is how copper glazes turn red and celadon turns green, which is a chemical effect rather than a colour choice.
Recognising which one you have is a matter of looking at the flame and the work, and it is directly controllable with the air.
བར་མ
3 hours
ལམ་སྟོན
1
1
Recognising the three by eye
Recognising the three by eye
An OXIDISING fire has excess air: the flame is short, clear and blue-tinged, the fire looks clean, and the work scales heavily and sparkles at high heat.
A REDUCING fire has excess fuel: the flame is long, lazy and yellow with a smoky tip, there is visible flame licking out of the top of the fuel bed, and the work comes out relatively clean and dark.
NEUTRAL sits between and is what most forging wants. Move the blast up and down and watch the flame change — half a minute doing that teaches the three states better than any description, and after that you will recognise them without thinking.
གོམ་པ་འདིའི་རྫས་རིགས:
 སོལ་བའི་སྒོ་རྡོག2 དུམ་བུ།
 ལྕགས་འཇམ་གྱི་དབྱུག་ཏོ།1 དུམ་བུ།
ལག་ཆས་དགོས་མཁོ:
 མགར་བའི་ཐབ་ཁུང་།
 རླུང་སྦུད་ཆས།
 མེ་ཐབ་ཀྱི་མིག་ཤེལ་ནག་པོ།
2
2
Scale: what an oxidising fire costs you
Scale: what an oxidising fire costs you
Every heat in an oxidising fire converts some of the surface to iron oxide — SCALE — which flakes off on the anvil. That metal is gone permanently, and on a piece reheated many times the loss is significant.
It also damages the surface. Scale hammered into hot steel leaves pits that have to be ground or filed out later, which costs more metal again. Brushing the work before each blow keeps the surface clean and is the reason a wire brush lives beside every anvil.
A reducing fire produces far less scale, which is one reason forge welding is done in one: the surfaces must be clean and oxide-free at the moment they are joined, and an oxidising fire is actively working against that.
གོམ་པ་འདིའི་རྫས་རིགས:
ལྕགས་འཇམ་གྱི་དབྱུག་ཏོ།1 དུམ་བུ།ལག་ཆས་དགོས་མཁོ:
མགར་བའི་ཐབ་ཁུང་། མགར་བའི་རྡོ་ལེབ།
 མགར་བའི་ཐོ་བ།
 མགར་བའི་ལག་བཟུང་།
3
3
Decarburisation: the damage you cannot see
Decarburisation: the damage you cannot see
At high temperature in an oxidising atmosphere, carbon is drawn out of the surface layer of steel. The metal is still there; its carbon is not.
That layer will not harden. A blade held too long at high heat in a dirty fire can be decarburised a few tenths of a millimetre deep, quench perfectly, and still have a soft edge — and nothing about its appearance reveals this before the hardness test fails.
Keep high-carbon steel out of oxidising conditions, minimise the time at temperature, and leave enough stock to grind the surface layer away afterwards. This is the failure most often misdiagnosed as a bad quench.
གོམ་པ་འདིའི་རྫས་རིགས:
ལྕགས་འཇམ་གྱི་དབྱུག་ཏོ།1 དུམ་བུ།ལག་ཆས་དགོས་མཁོ:
མགར་བའི་ཐབ་ཁུང་། ལྷག་ཆས་ཡོད་པའི་ཐར་མོ་ཀཔཱལ།
 ཆེ་བཟོའི་ལུབ།
4
4
Deliberate reduction: when the atmosphere is the point
Deliberate reduction: when the atmosphere is the point
Potters reduce on purpose. Starving the kiln of oxygen pulls it out of the metal oxides in the glaze instead, and copper that would be green in oxidation turns blood red, while iron gives celadon green rather than tan.
It is the same chemistry that smelting depends on: a reducing atmosphere is what takes the oxygen out of iron ore and leaves metallic iron. The published bloomery and smelting blueprints are this effect used at its largest scale.
The control is the same everywhere — restrict air, add fuel. What differs is only what you are trying to reduce, and whether you want the effect on the surface of a pot, throughout a glaze, or in a furnace full of ore.
གོམ་པ་འདིའི་རྫས་རིགས:
སོལ་བའི་སྒོ་རྡོག2 དུམ་བུ།ལག་ཆས་དགོས་མཁོ:
 ཐབ།
 ཚ་དྲོད་མཐོ་བའི་ཐབ་ཁུང་།
 སོལ་བའི་མེ་ཐབ།
 ཟིན་དེབ།
ལག་ཆས་དགོས་མཁོ
12- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
- ས་ཆ་འཛིན
འབྲེལ་ཡོད་བིལུ་པིརིན་ཊི
བིལུ་པིརིན་ཊི་འདི་ཚུ་ཐབས་ལམ་དང་རྫས་རིགས། སྤྱི་ཆོས་བགོ་བཤའ་བྱེད
CC0 སྤྱི་དབང
བིལུ་པིརིན་ཊི་འདི་CC0 འོག་བཀྲམས་ཡོད། ཁྱེད་རང་གིས་ཆོག་མཆན་མ་བཞེས་པར་ཕབ་ལེན་དང་བཟོ་བཅོས། བགོ་བཤའ། དགོས་མཁོ་གང་ལའང་བཀོལ་སྤྱོད་བྱས་ཆོག
བཟོ་མཁན་ལ་རྒྱབ་སྐྱོར་བྱེད་པའི་ཆེད་ཁོང་ཚོའི་བིལུ་པིརིན་ཊི་བརྒྱུད་ཐོན་སྐྱེད་ཉོ། བཟོ་མཁན་གྱིས བཟོ་མཁན་གྱི་ཁེ་ཕོགས ཚོང་པས་གཏན་འཁེལ་བྱས་པ། ཡང་ན་བིལུ་པིརིན་ཊི་འདིའི་པར་གསར་བཟོས་ཏེ་ཁྱེད་རང་གི་བིལུ་པིརིན་ཊི་ནང་མཐུད་སྦྲེལ་བྱས་ཏེ་ཡོང་སྒོ་བགོ་བཤའ་བྱེད།