艺术
美容与健康
工艺
文化与历史
娱乐
环境
食品与饮料
逆向工程
科学
体育
技术
可穿戴设备
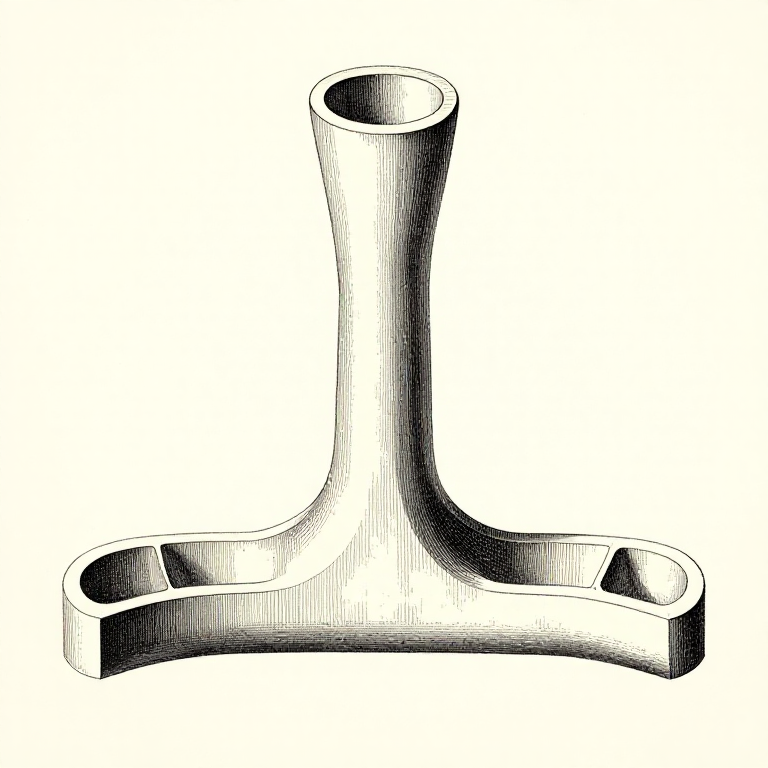


Gating: Getting the Metal In Without Wrecking the Mould
Molten metal poured straight into a cavity arrives fast, turbulent and full of air. It washes sand off the mould walls, folds oxide skin into itself, and the casting is full of inclusions before it has even frozen.
The GATING SYSTEM exists to prevent that. A sprue to take the metal down, a runner to carry it sideways and slow it, and gates to let it into the cavity smoothly — each part doing one job.
The governing principle is that the system should fill and stay full. A gating system running only partly full drags air in with the metal, which is precisely what it was built to avoid.
高级
3 hours
说明
1
1
Sprue, runner, gate — three parts, three jobs
Sprue, runner, gate — three parts, three jobs
The SPRUE is the vertical channel the metal is poured into. It should be TAPERED, wider at the top, because falling metal accelerates and narrows — a parallel sprue leaves a gap around the stream that sucks in air.
The RUNNER is the horizontal channel at the bottom. It distributes metal and slows it down, and it is usually in the drag with the gates in the cope so that any floating dross stays in the runner.
The GATES are the small openings from runner into cavity. Several small gates fill more gently than one large one and let the mould fill from more than one place, which matters on anything long or thin.
此步骤所需材料:
 铸造砂1 公斤
所需工具:
 砂型箱(上箱与下箱)
 直尺
 6 英寸数显卡尺
2
2
Choke the system, and where
Choke the system, and where
正在加载 Jupyter 笔记本…
此步骤所需材料:
 青铜锭1 个铸造砂1 公斤
所需工具:
 台式电脑6 英寸数显卡尺砂型箱(上箱与下箱)
3
3
Traps, filters and a pouring basin
Traps, filters and a pouring basin
A POURING BASIN at the top of the sprue lets you fill it and keep it full, so the sprue never runs empty mid-pour. Pouring straight into a bare sprue hole guarantees an interrupted, air-entraining stream at the start.
A runner extension beyond the last gate — a DIRT TRAP — gives the first, dirtiest metal somewhere to go that is not the casting. It costs a few centimetres of runner and catches the slag that came down the sprue first.
Ceramic foam FILTERS do the same job far better and are cheap. They also slow and smooth the flow, which is why a filter often improves a casting for two reasons at once.
此步骤所需材料:
铸造砂1 公斤所需工具:
砂型箱(上箱与下箱)直尺 细网撇沫勺
4
4
Pour steadily and keep the basin full
Pour steadily and keep the basin full
Start the pour and bring the basin up to full quickly, then hold it there until the mould is full. A pour that starts timidly and then speeds up entrains air at the very start, which is the metal that ends up deepest in the casting.
Never stop and restart. A pause lets the stream break, lets air in, and can leave a COLD SHUT where the metal that stopped has skinned over before the rest arrives.
Have enough metal melted before you start. Running out halfway is the single most avoidable failure in a foundry, and it is prevented by weighing the pattern, multiplying by the alloy's density ratio, and adding a generous allowance for the gating and risers — which is usually a third of the total again.
此步骤所需材料:
青铜锭1 个 木炭1 个
所需工具:
 铸造浇包
 坩埚钳
 锻造遮光护目镜
 长袖皮手套
此蓝图制作
相关蓝图
这些蓝图共享知识——技术、材料或原理


CC0 公共领域
此蓝图以 CC0 协议发布。你可以自由复制、修改、分发和使用此作品,无需征得许可。
通过购买蓝图中的产品支持创客,他们将获得 创客佣金 (由供应商设定),或创建此蓝图的新版本并将其作为连接包含在你自己的蓝图中以分享收入。