艺术
美容与健康
工艺
文化与历史
娱乐
环境
食品与饮料
逆向工程
科学
体育
技术
可穿戴设备


Pouring Temperature: Too Cold Misruns, Too Hot Tears the Mould
Metal is not poured at its melting point. It is poured at a SUPERHEAT above it — enough that it can travel through the gating and fill the last thin corner before it starts to freeze.
Too little superheat and the metal stops before the cavity is full, or two streams meet and fail to fuse. Too much and it dissolves more gas, oxidises harder, burns the sand, and shrinks more on the way down — so the porosity gets worse rather than better.
The window is perhaps 100 to 150 degrees wide, it differs by alloy and by casting, and the only way to sit inside it reliably is to MEASURE. Judging melt temperature by colour is the pyrometer rung's warning delivered with molten metal.
高级
3 hours
说明
1
1
Superheat, by alloy
Superheat, by alloy
正在加载 Jupyter 笔记本…
此步骤所需材料:
 青铜锭1 个
 铝锭 99.7 % 纯度,450 g1 个
所需工具:
 高温计
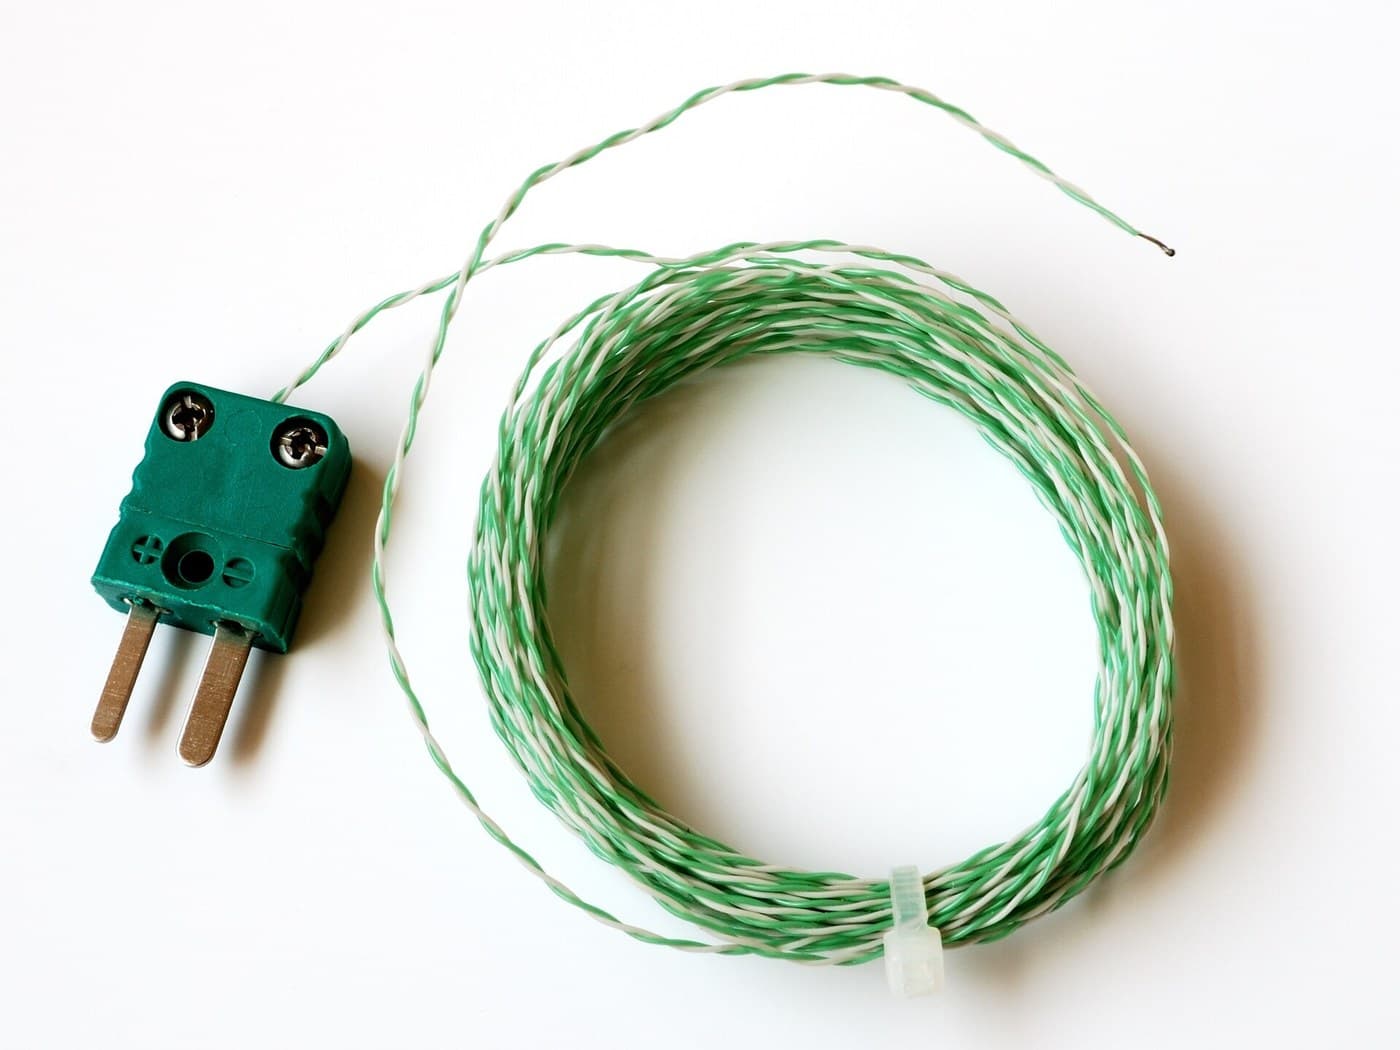
 带读数的热电偶
 台式电脑
2
2
Skim, and do not stir the dross back in
Skim, and do not stir the dross back in
Oxide and impurities float. Skim them off the surface of the melt immediately before pouring, with a preheated skimmer, and take them right out of the crucible rather than pushing them aside.
Preheat every tool that will touch molten metal. A cold skimmer or ladle chills the metal locally and, far worse, any trace of moisture on it flashes to steam instantly — which throws metal.
Do not stir after skimming. Stirring folds the remaining surface oxide down into the melt, where it becomes inclusions in the casting. Aluminium is the worst for this: its oxide skin is tough, and every disturbance of the surface makes more of it.
此步骤所需材料:
青铜锭1 个所需工具:
 细网撇沫勺
 铸造浇包
 坩埚钳
 长袖皮手套
3
3
Dry everything, and mean it
Dry everything, and mean it
Water and molten metal is the one genuinely dangerous combination in a foundry. Water turned to steam expands roughly 1,600 times, instantly, and if it is under metal it throws that metal outward.
So: preheat and dry the crucible, the tongs, the ladle and every ingot before it goes near the melt. An ingot with condensation on it, or a scrap casting with water trapped in a cavity, is the classic cause.
The mould matters too. Green sand contains water by design and that is fine because it is bound in the clay and the mould is permeable — but a sand that is too wet, or a mould left standing so condensation collects, is the same hazard in a different place.
此步骤所需材料:
青铜锭1 个 块状木炭1 个
所需工具:
 坩埚坩埚钳
 锻造遮光护目镜长袖皮手套
4
4
Everything ready before the metal is
Everything ready before the metal is
Once the metal is at temperature it is losing heat and gaining gas every second. The moulds must be closed, weighted, vented and positioned before the crucible comes out of the furnace.
Weight or clamp the cope. Molten metal exerts real upward pressure on the top half of the mould, and an unweighted cope lifts and lets metal run out of the parting line — which is dangerous as well as a lost casting.
Have a clear path, a clear floor, and somewhere planned to put the crucible down. The pour itself takes a few seconds; everything that makes it go well or badly was decided in the minutes before it.
此步骤所需材料:
 铸造砂1 公斤
所需工具:
 砂型箱(上箱与下箱)坩埚钳锻造遮光护目镜长袖皮手套
相关蓝图
这些蓝图共享知识——技术、材料或原理



CC0 公共领域
此蓝图以 CC0 协议发布。你可以自由复制、修改、分发和使用此作品,无需征得许可。
通过购买蓝图中的产品支持创客,他们将获得 创客佣金 (由供应商设定),或创建此蓝图的新版本并将其作为连接包含在你自己的蓝图中以分享收入。