ARTE
BELLEZA Y BIENESTAR
ARTESANÍA
CULTURA E HISTORIA
ENTRETENIMIENTO
MEDIO AMBIENTE
COMIDA Y BEBIDAS
INGENIERÍA INVERSA
CIENCIAS
DEPORTES
TECNOLOGÍA
TECNOLOGÍA VESTIBLE
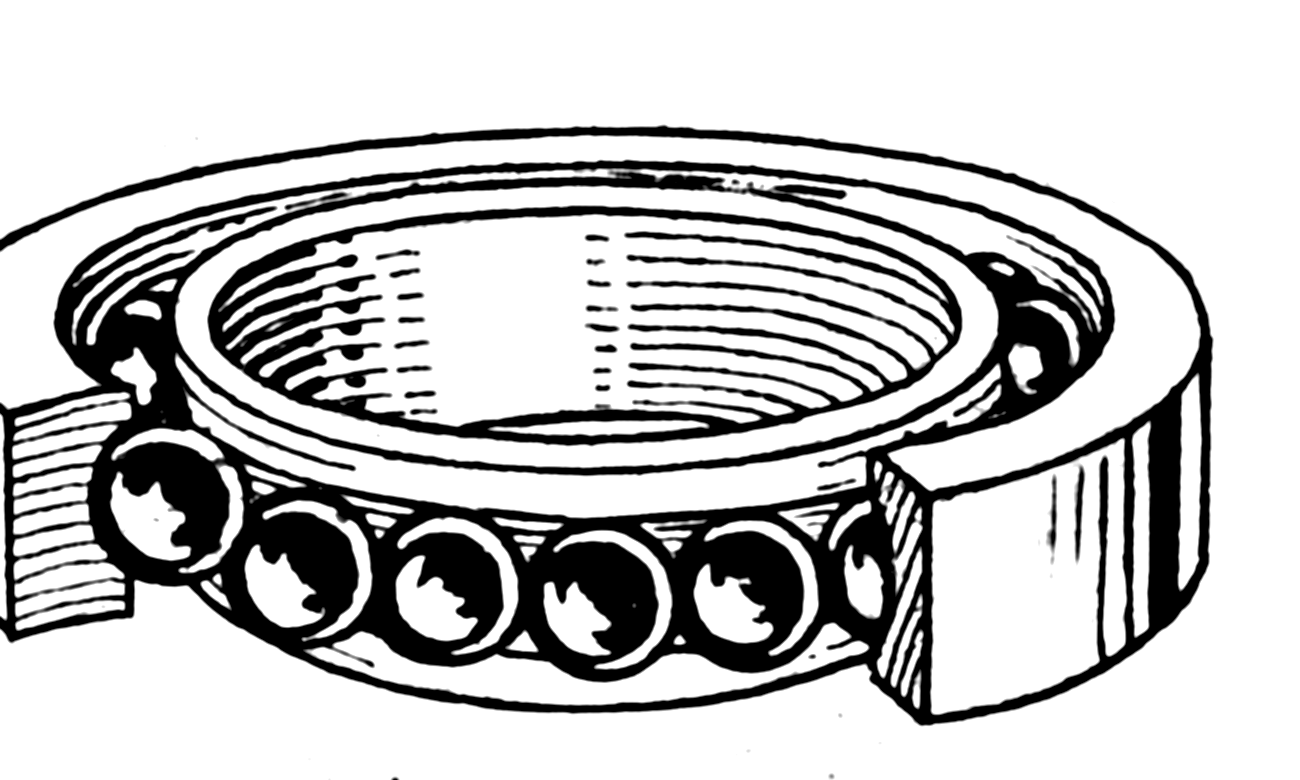

Ball Bearings: Races, Balls and Cage
A ball bearing has four parts: an outer race, an inner race, the balls that roll between them, and a cage that keeps the balls evenly spaced. Almost all of it is steel, usually 52100 (1.5% chromium, 1% carbon), which can be made very hard and tough by heat treating; 440C stainless is used where rust is a problem. The races are turned from tubing, the balls are cold headed from thick wire, both are hardened, tempered, ground and lapped to an almost mirror finish, and the cage is stamped from thin sheet. Even an inexpensive bearing's balls may be out of round by no more than 25 millionths of an inch; precision bearings allow five millionths.
Avanzado
Factory process
Instrucciones
1
1
Turn the races
Turn the races
Cut the basic shape of both races from steel tubing on automatic lathe-like machines, leaving every dimension slightly oversize: the steel usually warps in heat treatment.
Materiales para este paso:
 Tubo de acero para rodamientos (52100)1 as required
Herramientas necesarias:
 Torno automático
2
2
Harden and temper the races
Harden and temper the races
Heat to about 843 °C (1,550 °F) for up to several hours depending on size, then quench in oil: hard but brittle. Temper at about 149 °C (300 °F) and let cool in air: hard and tough.
Herramientas necesarias:
 Horno de temple continuo con baño de aceite
 Horno de revenido
3
3
Grind and lap the races
Grind and lap the races
The hardened steel is too hard to cut, so grind almost every surface: the fitting surfaces round, the sides flat. Grind the ball track, then lap it for several hours with a very fine abrasive slurry to an almost mirror finish.
Herramientas necesarias:
 Rectificadora de pistas de rodamiento
 Lapeadora de pistas
 Pasta de lapear
4
4
Cold head the balls
Cold head the balls
Feed thick wire from a roll into a machine that cuts off a short piece and smashes both ends in toward the middle between two dies, without heating. The ball comes out with a ring of "flash" round its middle.
Materiales para este paso:
 Alambre de acero para rodamientos (52100)1 as required
Herramientas necesarias:
 Máquina de estampación en frío
5
5
Remove the flash
Remove the flash
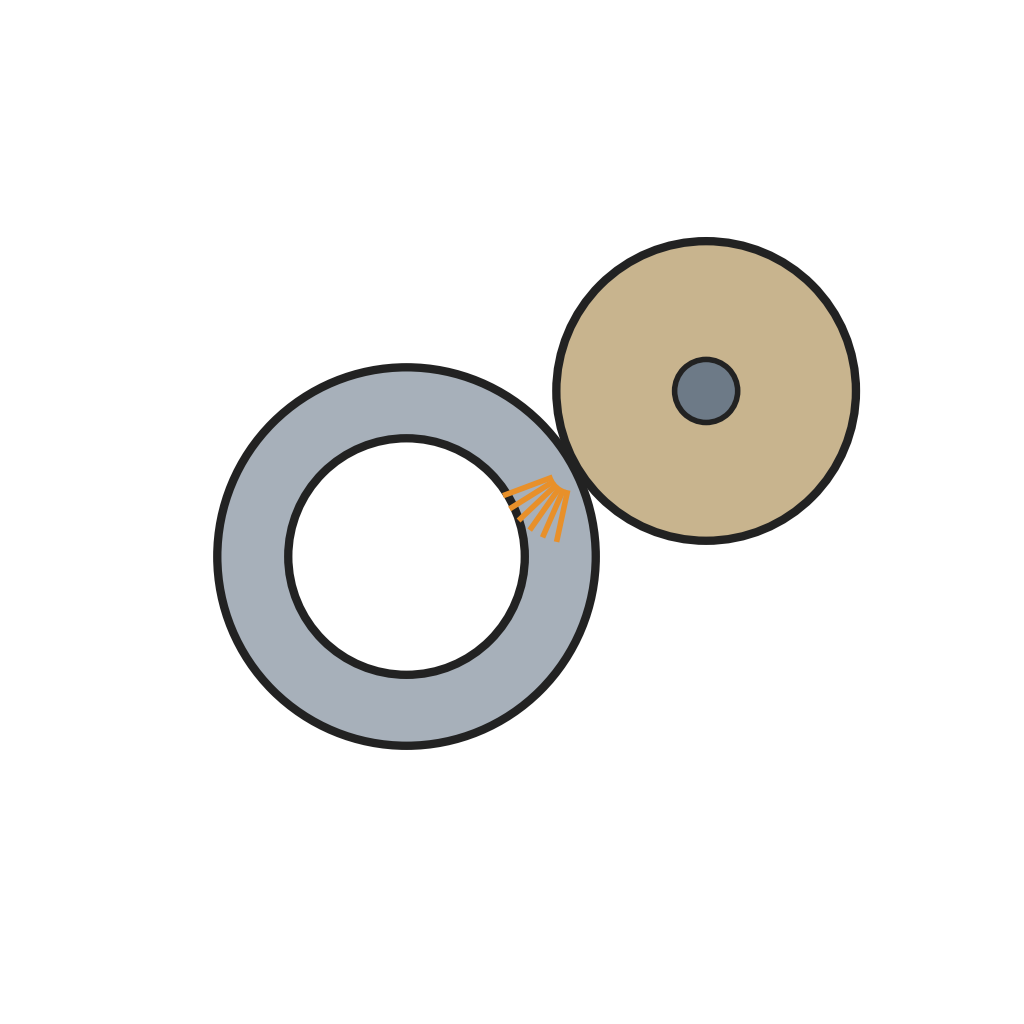
Run the balls many times round rough grooves between two cast-iron discs, one turning and one fixed, until the flash is gone and they are nearly round. Leave about 0.008 in (0.2 mm) for finishing.
Herramientas necesarias:
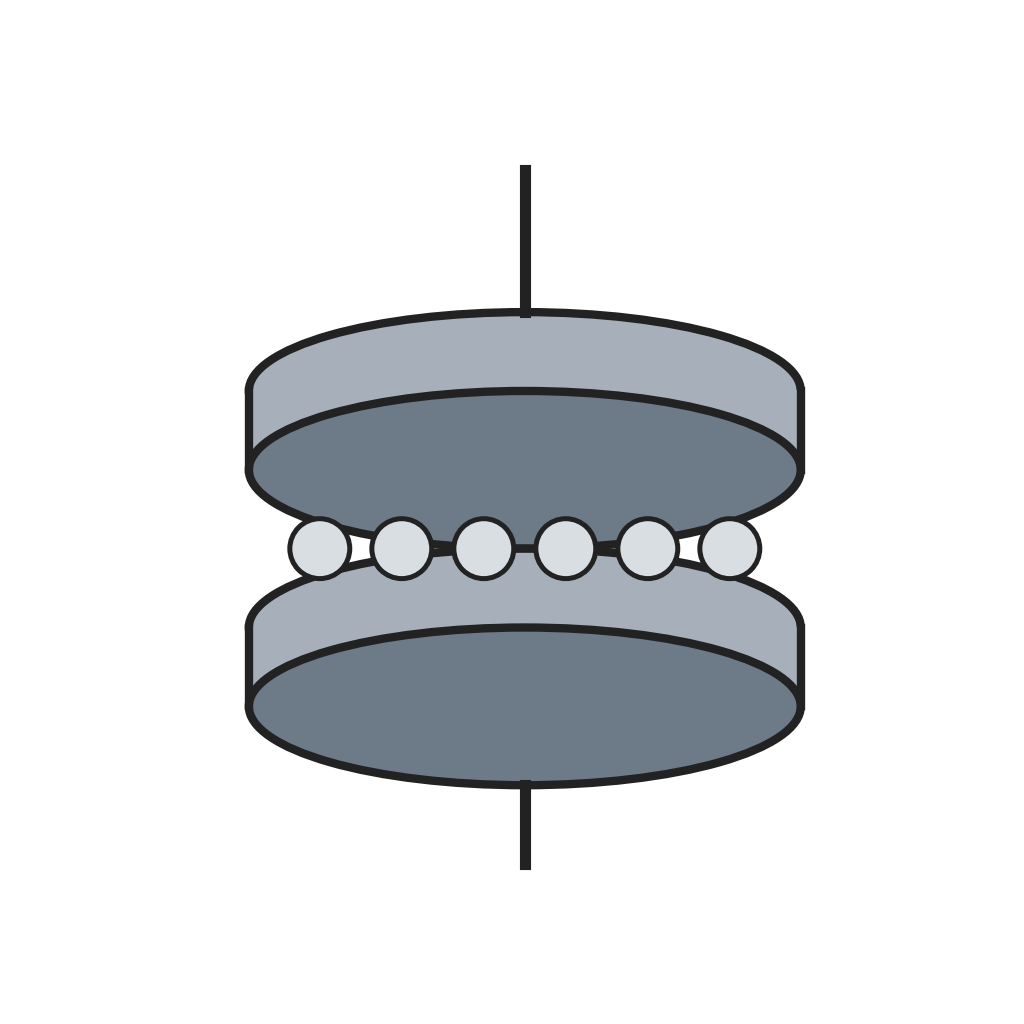 Máquina desbarbadora de bolas
6
6
Harden, grind and lap the balls
Harden, grind and lap the balls
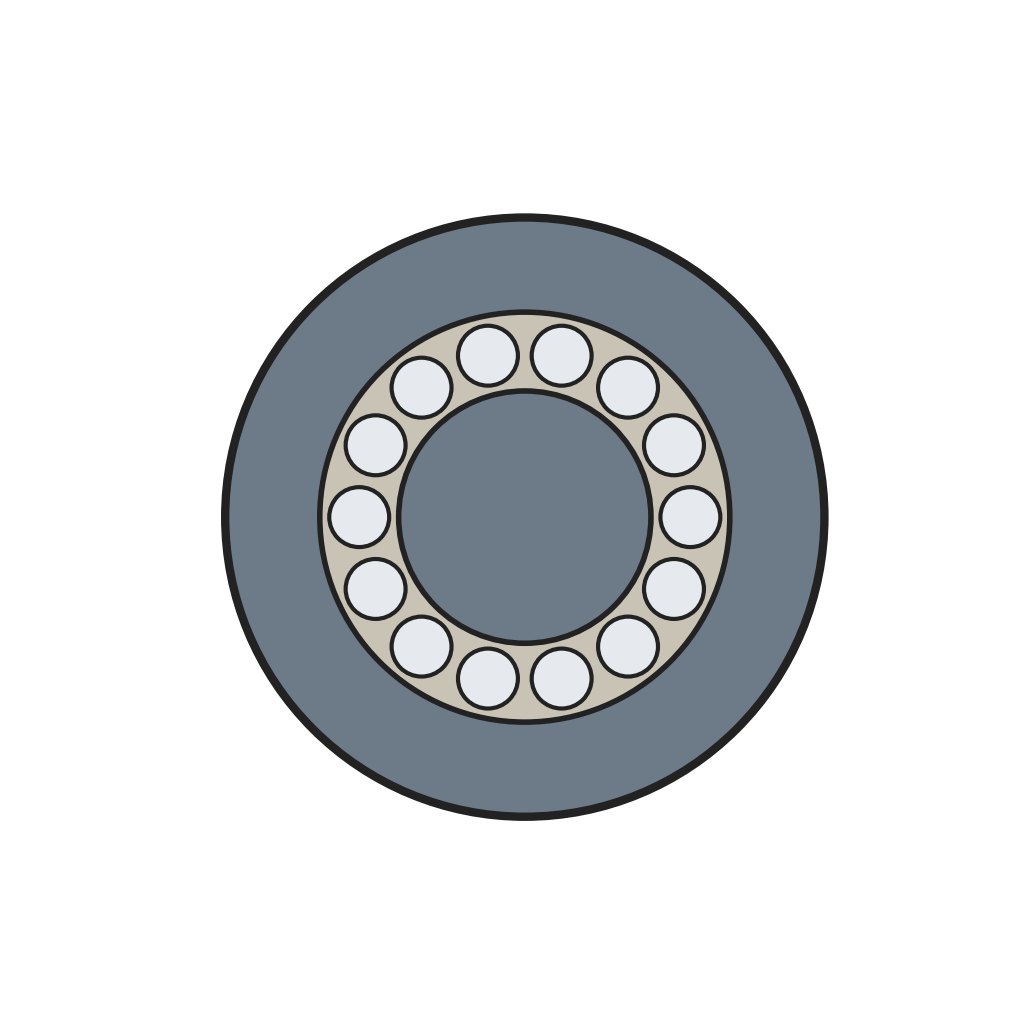
Heat treat and temper the balls like the races. Grind them in the same kind of disc machine with grinding wheels to within a few ten-thousandths of an inch, then lap them 8–10 hours on cast-iron wheels with lapping compound.
Herramientas necesarias:
Horno de temple continuo con baño de aceiteHorno de revenido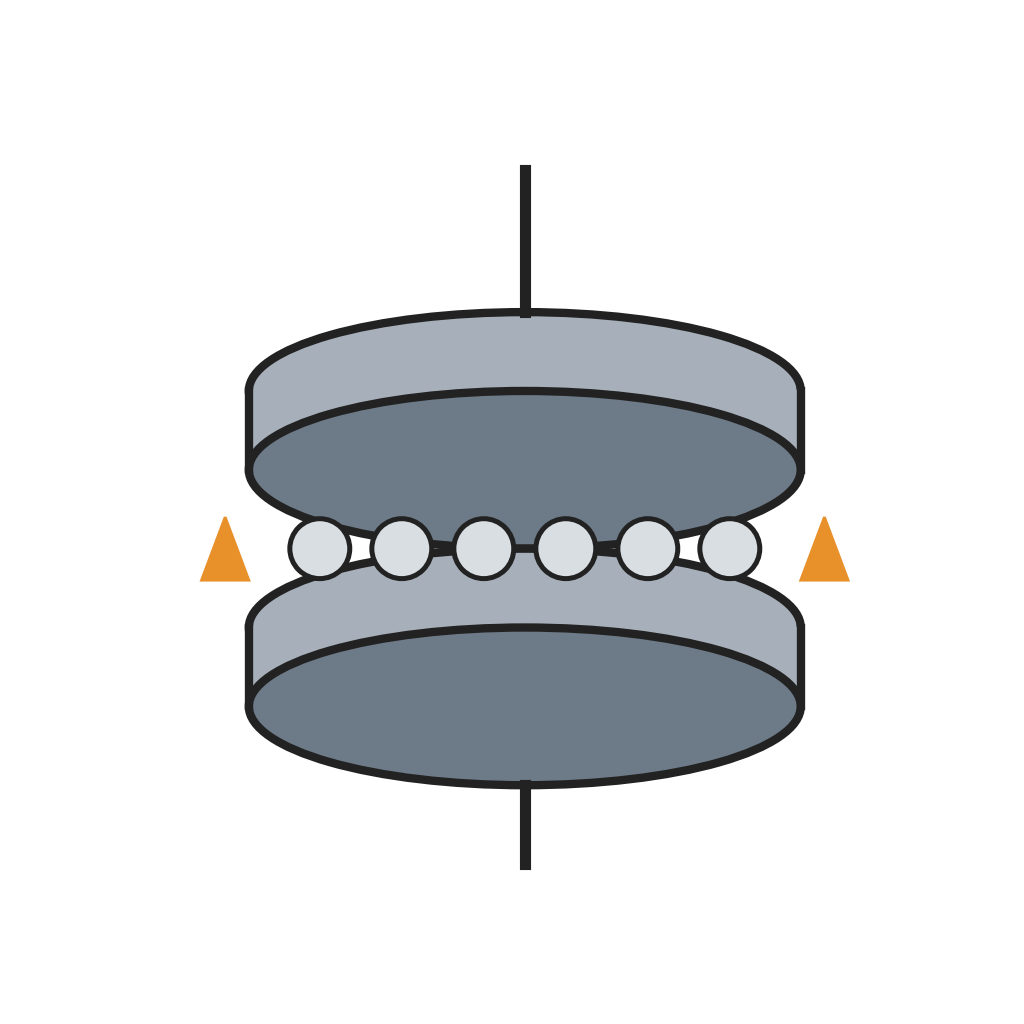 Rectificadora de bolas
 Lapeadora de bolasPasta de lapear
7
7
Stamp the cage
Stamp the cage
Stamp the cage halves from thin steel sheet and bend them to shape in a die. (Plastic cages are injection moulded instead.)
Materiales para este paso:
 Chapa de acero1 as required
Herramientas necesarias:
 Prensa de estampación
8
8
Assemble
Assemble
Put the inner race inside the outer race, pushed as far to one side as it goes, and drop the balls into the gap opposite. Centre the races and spread the balls evenly, fit the cage (steel cages riveted, plastic ones snapped in) and coat the bearing with a thin film of petroleum jelly against rust.
Materiales para este paso:
 Remaches de acero1 as required
 Vaselina1 as required
Materiales
5- 1 as requiredMarcador de posición
- 1 as requiredMarcador de posición
- 1 as requiredMarcador de posición
- 1 as requiredMarcador de posición
- 1 as requiredMarcador de posición
Herramientas requeridas
11- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
Blueprints relacionados
Estos blueprints comparten conocimiento — técnicas, materiales o principios
CC0 Dominio público
Este Blueprint se publica bajo CC0. Eres libre de copiar, modificar, distribuir y usar este trabajo para cualquier propósito, sin pedir permiso.
Apoya al Maker comprando productos a través de su Blueprint, donde gana una Comisión del Maker establecida por los vendedores, o crea una nueva iteración de este Blueprint e inclúyela como conexión en tu propio Blueprint para compartir ingresos.