Colaboración
ARTE
BELLEZA Y BIENESTAR
ARTESANÍA
CULTURA E HISTORIA
ENTRETENIMIENTO
MEDIO AMBIENTE
COMIDA Y BEBIDAS
INGENIERÍA INVERSA
CIENCIAS
DEPORTES
TECNOLOGÍA
TECNOLOGÍA VESTIBLE
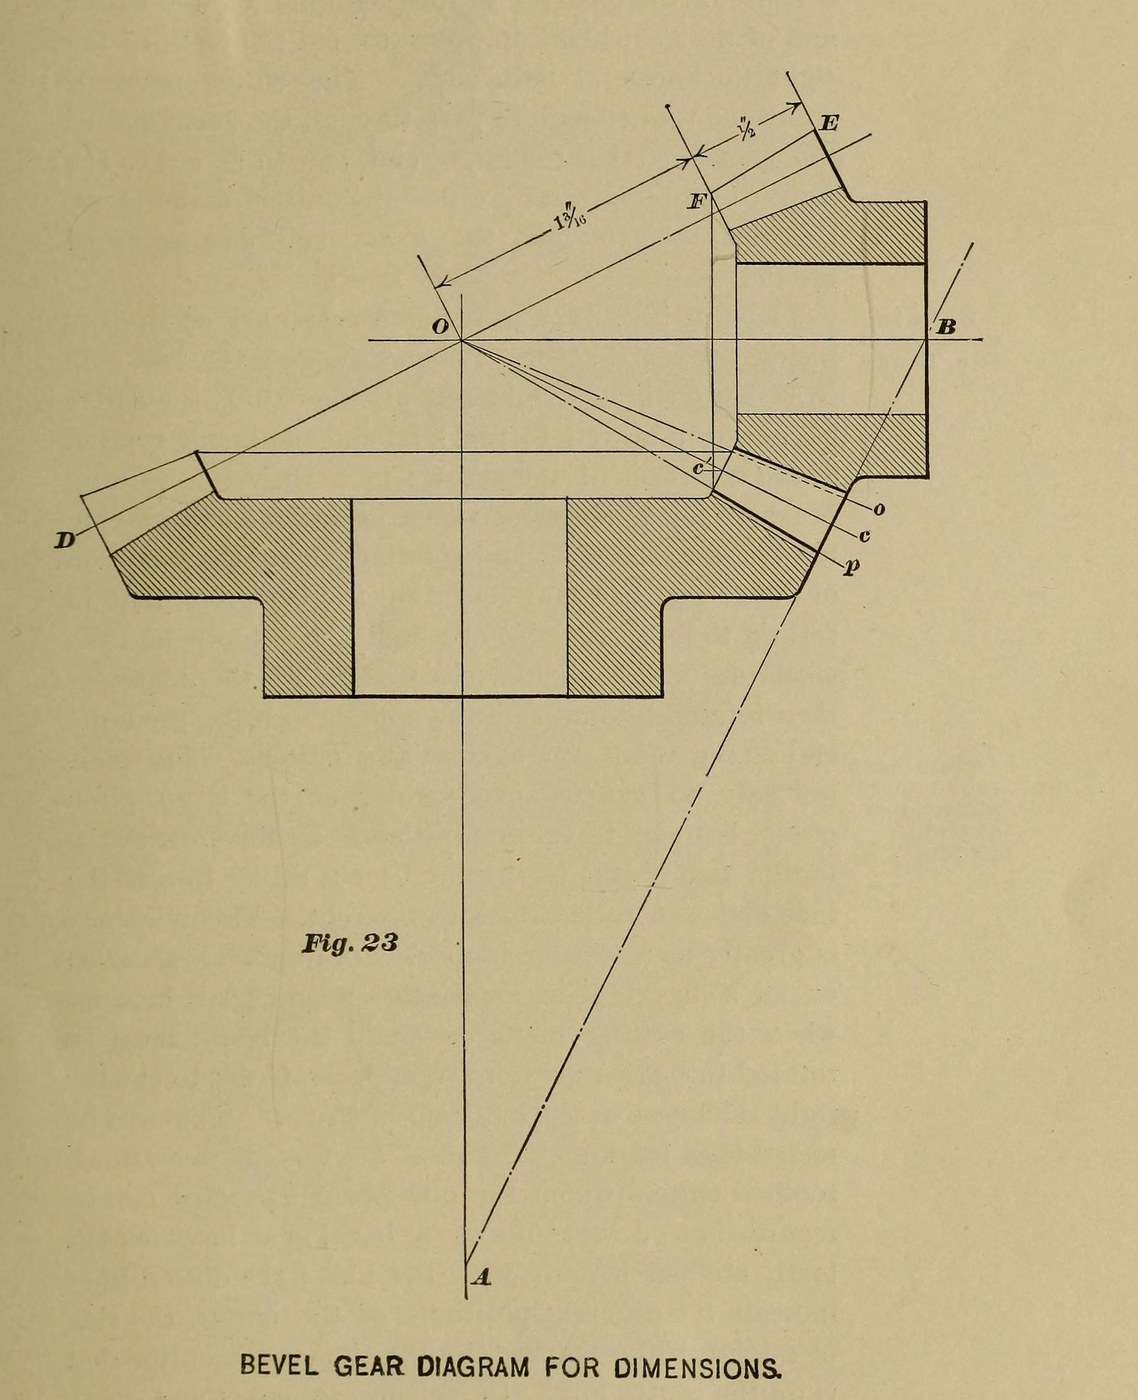


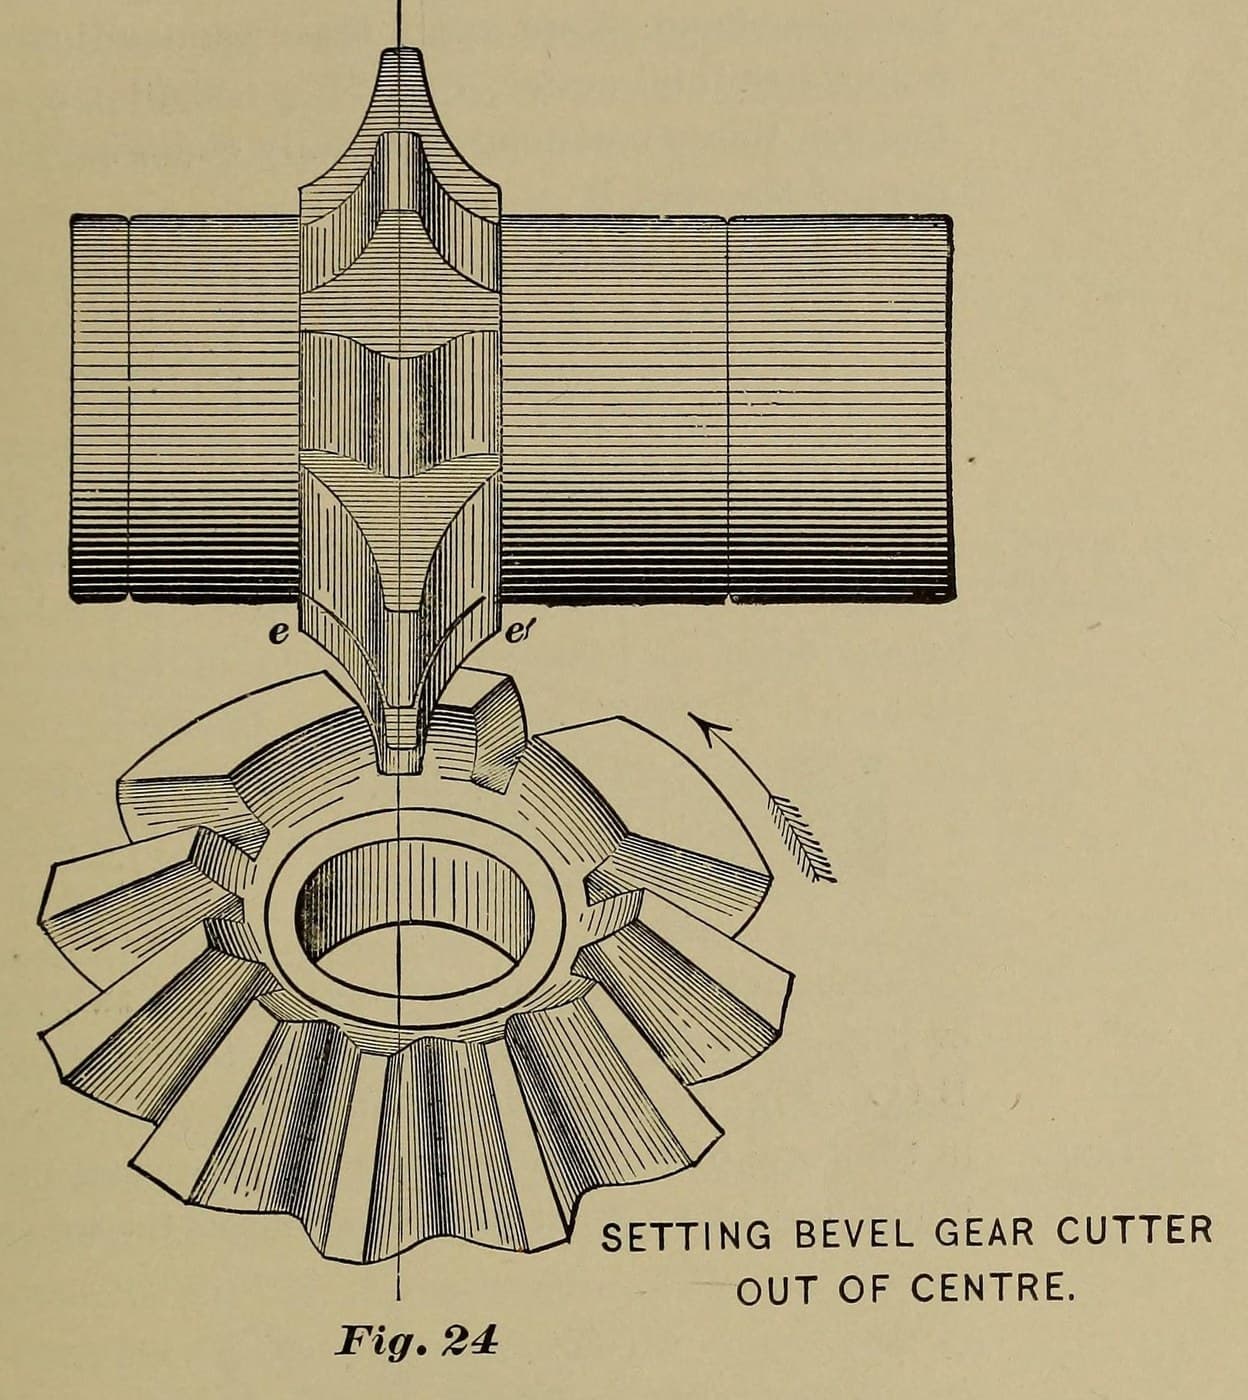
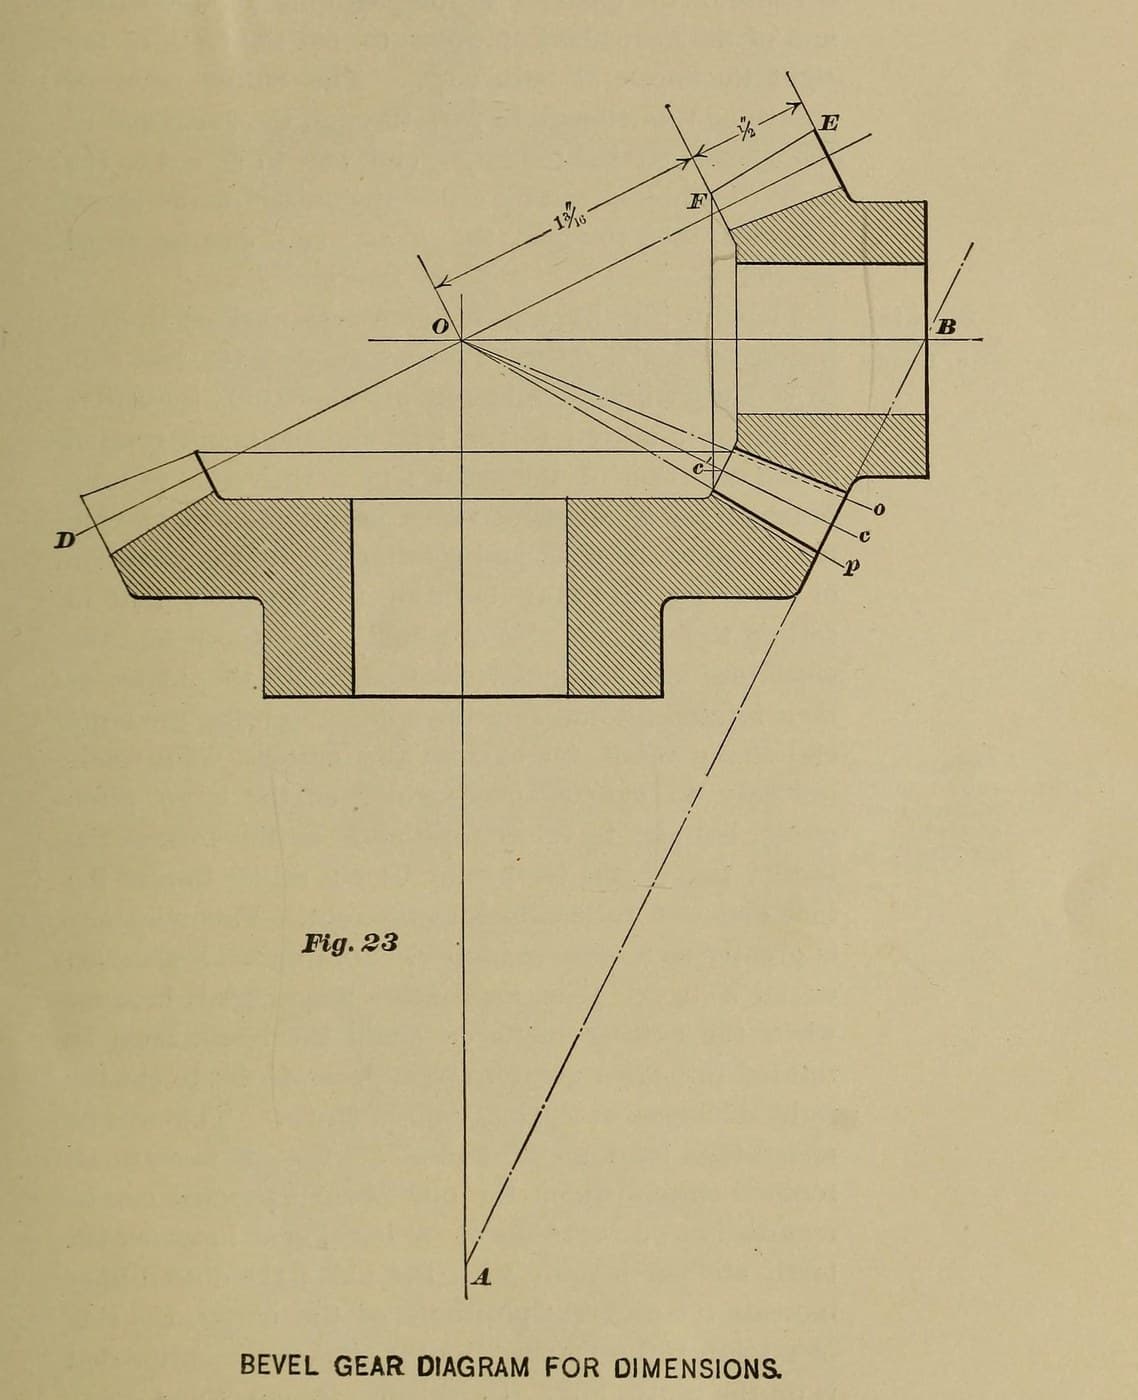
Bevel Pinion with a No. 6 Cutter, Filed at the Small End (Brown & Sharpe 1911)
The same 12-tooth, 8-pitch pinion as Brown & Sharpe's worked example, but cut the way their own shop did it: with a No. 6 cutter instead of the No. 8 they sell for it, cut to the right thickness at the large end, then filed well round at the small end. They did this only for a 12-tooth pinion running with a gear two or three times its size.
Source: Brown & Sharpe, Practical Treatise on Gearing (1911), Fig. 23 example, Part I ch. IX–X, Part II ch. III and the set-over table p. 58. The blank sizes are our arithmetic with their rules; the steel and bore are ours. Picture: their Fig. 23.
Avanzado
1 day
Instrucciones
1
1
Work out and turn the blank
Work out and turn the blank
Pitch diameter 12 ÷ 8 = 1.500 in. Angle of edge 26° 34′ and angle of face 59° 11′ (Brown & Sharpe's figures for every 12 and 24 tooth pair). Diameter increment = cos 26° 34′ × 0.250 = 0.224 in, so turn the steel blank to 1.72 in outside diameter. Face ½ in long. Try both angles with a protractor against the end of the hub.
Materiales para este paso:
 Barra de acero dulce1 length for one blank
Herramientas necesarias:
 Torno de metal
 Herramienta de corte para torno
 Transportador de ángulos
 Micrómetro
2
2
Choose the cutter
Choose the cutter
Twice the back cone radius × 8 comes to about 13, which would call for a No. 8, but take a No. 6, 8-pitch bevel gear cutter (17 to 20 teeth), as Brown & Sharpe's own shop did for this pinion. Measure its thickness Tc at the pitch line, 0.145 in from its tip.
Herramientas necesarias:
 Fresa para engranajes cónicos
 Calibre vernier para dientes de engranaje
3
3
Set the head at 22° 18′
Set the head at 22° 18′
Apex distance = sec 26° 34′ × 1.5 = 1.677 in. Angle increment: tan = sin 26° 34′ ÷ 6, giving 4° 16′. Set the dividing head to the cutting angle 26° 34′ − 4° 16′ = 22° 18′ and index 12 spaces. Depth at the large end 0.270 in.
Herramientas necesarias:
 Fresadora
 Cabezal divisorFresa para engranajes cónicos
4
4
Set over and cut one side
Set over and cut one side
Apex distance ÷ face = 3.35; we take the nearest column, 3¼, where a No. 6 cutter has the factor .318. Set-over = Tc ÷ 2 − .318 ÷ 8 = Tc ÷ 2 − 0.040 in. Set off centre by that amount, take up backlash, and cut round all 12 spaces.
Herramientas necesarias:
FresadoraCabezal divisorFresa para engranajes cónicos5
5
Set over the other way and trim
Set over the other way and trim
Set over the same amount the other side, line the cutter up with the space at the small end, take a trial cut, and rotate toward the cutter until the tooth is right at the faces of the large end: 0.196 in at the pitch line (0.138 in at the small end). Check with the gear tooth vernier, then cut round.
Herramientas necesarias:
FresadoraCabezal divisorFresa para engranajes cónicosCalibre vernier para dientes de engranaje6
6
File the small ends
File the small ends
The No. 6 cuts the tooth sides with a longer curve than the No. 8, so expect considerable filing: round the teeth over at the small ends, without filing them thinner at the pitch line.
Herramientas necesarias:
 Lima fina
Materiales
1- 1 length for one blankMarcador de posición
Herramientas requeridas
9- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
Este plano hace
Blueprints relacionados
Estos blueprints comparten conocimiento — técnicas, materiales o principios
CC0 Dominio público
Este Blueprint se publica bajo CC0. Eres libre de copiar, modificar, distribuir y usar este trabajo para cualquier propósito, sin pedir permiso.
Apoya al Maker comprando productos a través de su Blueprint, donde gana una Comisión del Maker establecida por los vendedores, o crea una nueva iteración de este Blueprint e inclúyela como conexión en tu propio Blueprint para compartir ingresos.