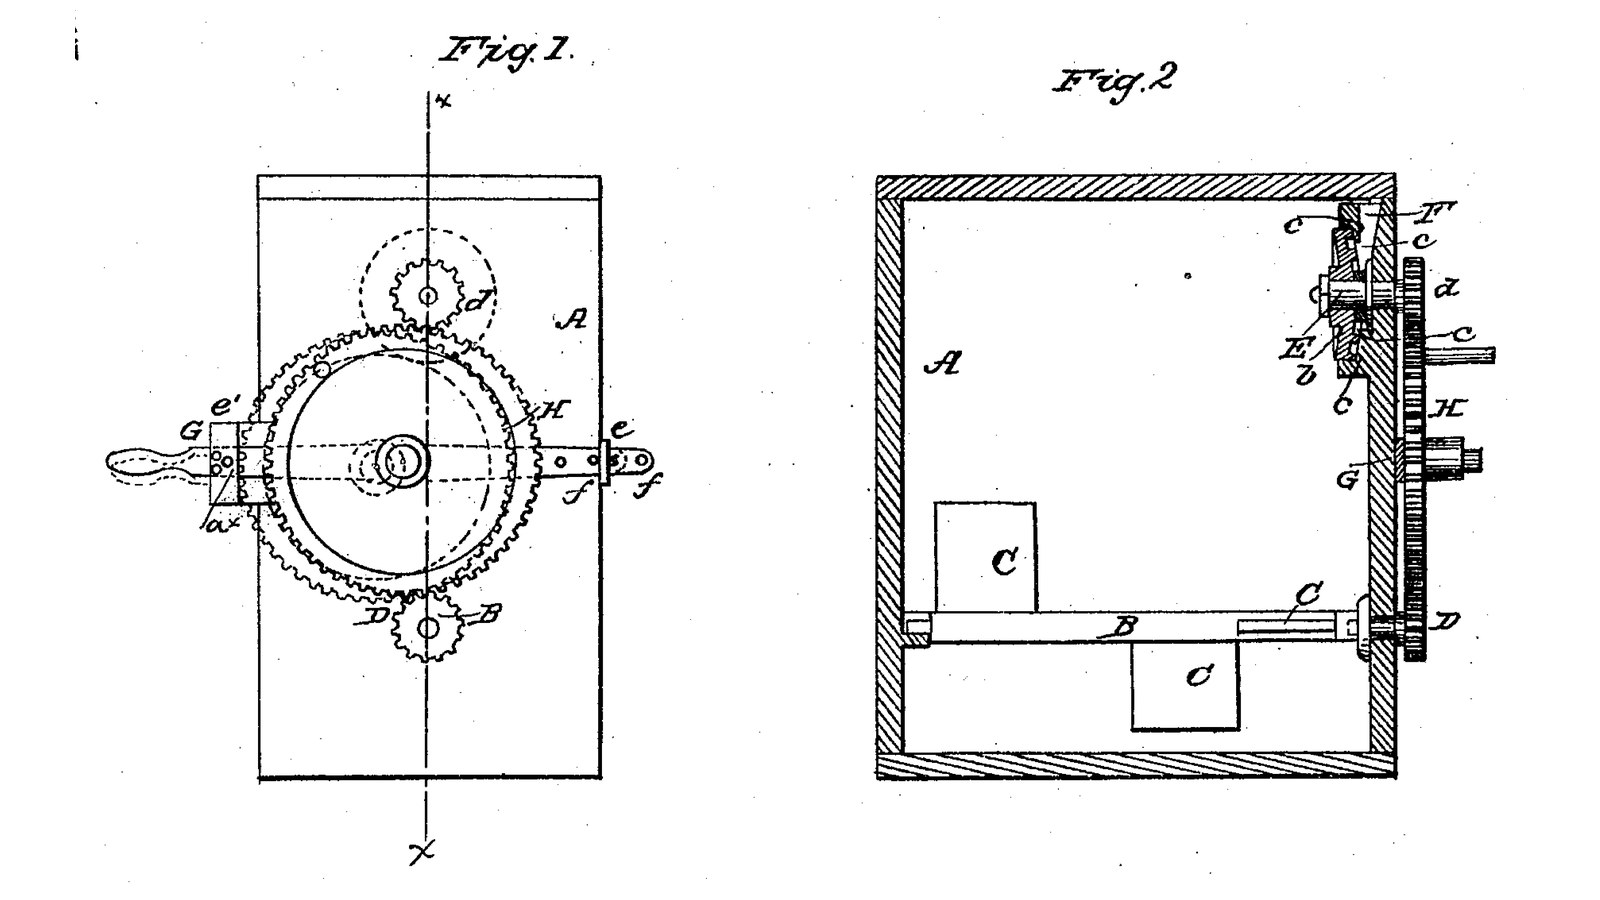

Shifting-Gear Grinding-Disk Churn: One Crank Wheel Is Thrown Into Gear With the Wings Below, the Grinding Disk Above, or Both
Instrucciones
One wheel, two pinions
One wheel, two pinions
Cream ground once between disks as it is poured in, three months before
Cream ground once between disks as it is poured in, three months before
Read US 32,939
Read US 32,939
Body A and lid
Body A and lid
Materiales para este paso:
 Tabla de madera dura4 piezas
 Cola de carpintero1 pieza
 Sellador de silicona1 pieza
 Tornillos para madera30 piezas
Herramientas necesarias:
 Sierra de mesa
 Taladro inalámbrico
 Juego de brocas
 Juego de brocas de pala
 Sargento
 Juego de destornilladores
 Cinta métrica
Shaft B with wings C and pinion D
Shaft B with wings C and pinion D
Materiales para este paso:
 Varilla de acero inoxidable1 piezaTabla de madera dura1 piezaTornillos para madera8 piezas
 Shaft Collar2 piezas
 Pasador de aletas2 piezas
 Filamento PETG1 pieza
Herramientas necesarias:
 Impresora 3D de filamento (FDM)Sierra de mesaTaladro inalámbricoJuego de brocas
 Sierra para metales
 Limas (lima de mano)Juego de destornilladores
Print the pinions D and d (two)
Print the pinions D and d (two)
Print the grinding disk b
Print the grinding disk b
Print the hopper F
Print the hopper F
Disks a and b, shaft E, pinion d and hopper F
Disks a and b, shaft E, pinion d and hopper F
Materiales para este paso:
 Plancha de HDPE1 piezaCola de carpintero1 piezaVarilla de acero inoxidable2 piezasTornillos para madera3 piezasPasador de aletas2 piezasShaft Collar1 piezaFilamento PETG1 pieza
Herramientas necesarias:
Impresora 3D de filamento (FDM) Brújula
 Sierra de calarJuego de brocas de palaSierra para metalesTaladro inalámbricoJuego de brocasJuego de destornilladores
Print the crank wheel H
Print the crank wheel H
Bar G, guides e, e', wheel H and pin a*
Bar G, guides e, e', wheel H and pin a*
Materiales para este paso:
 Pletina de acero dulce1 piezaTabla de madera dura1 piezaTornillos para madera8 piezasVarilla de acero inoxidable1 piezaPasador de aletas2 piezas
 Espigas de madera dura1 piezaFilamento PETG1 pieza
Herramientas necesarias:
Impresora 3D de filamento (FDM)Sierra para metalesLimas (lima de mano) Tornillo de bancoTaladro inalámbricoJuego de brocas
 Juego de formones para maderaJuego de destornilladores
The build in 3D
The build in 3D
Churn: grind, then gather
Churn: grind, then gather
Materiales para este paso:
 Crema de leche espesa12 l
 Sal marina gruesa1 pieza
 Agua1 pieza
Herramientas necesarias:
 Termómetro de sonda permanente
 Cronómetro
 Báscula digital de cocina
 Bol grande de acero inoxidable
Troubleshooting
Troubleshooting
Flow
History and honest limits
History and honest limits
Materiales
14- 4 piezasMarcador de posición
- 2 piezasMarcador de posición
- 1 piezaMarcador de posición
- 49 piezasMarcador de posición
- 2 piezasMarcador de posición
- 2 piezasMarcador de posición
- 6 piezasMarcador de posición
- 3 piezasMarcador de posición
- 1 piezaMarcador de posición
- 1 piezaMarcador de posición
- 1 piezaMarcador de posición
- Marcador de posición
- 1 piezaMarcador de posición
- 1 piezaMarcador de posición
Herramientas requeridas
18- 1 vendor sell this, none ship to you yetMarcador de posición
- 1 vendor sell this, none ship to you yetMarcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- 1 vendor sell this, none ship to you yetMarcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- 1 vendor sell this, none ship to you yetMarcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
- Marcador de posición
Archivos de diseño
5

Blueprints relacionados
Estos blueprints comparten conocimiento — técnicas, materiales o principios
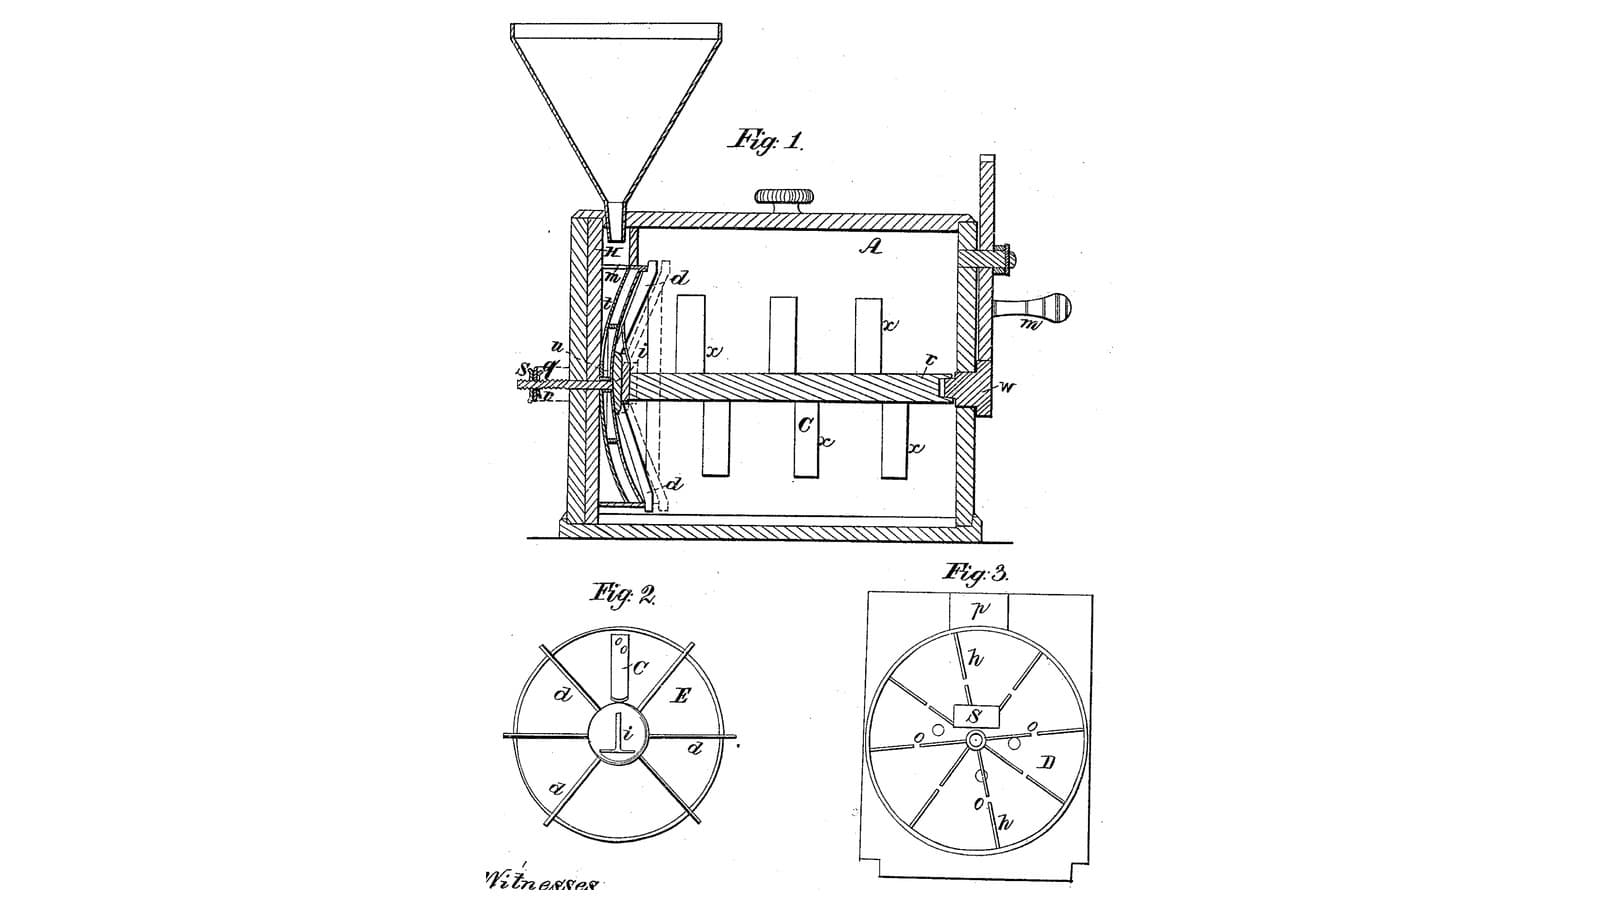
Adjustable-Dish Churn: Cream Is Poured Between a Fixed Ribbed Dish and a Turning One, Then Beaten by Wings and Dashers
por Buttercup
Carpintería
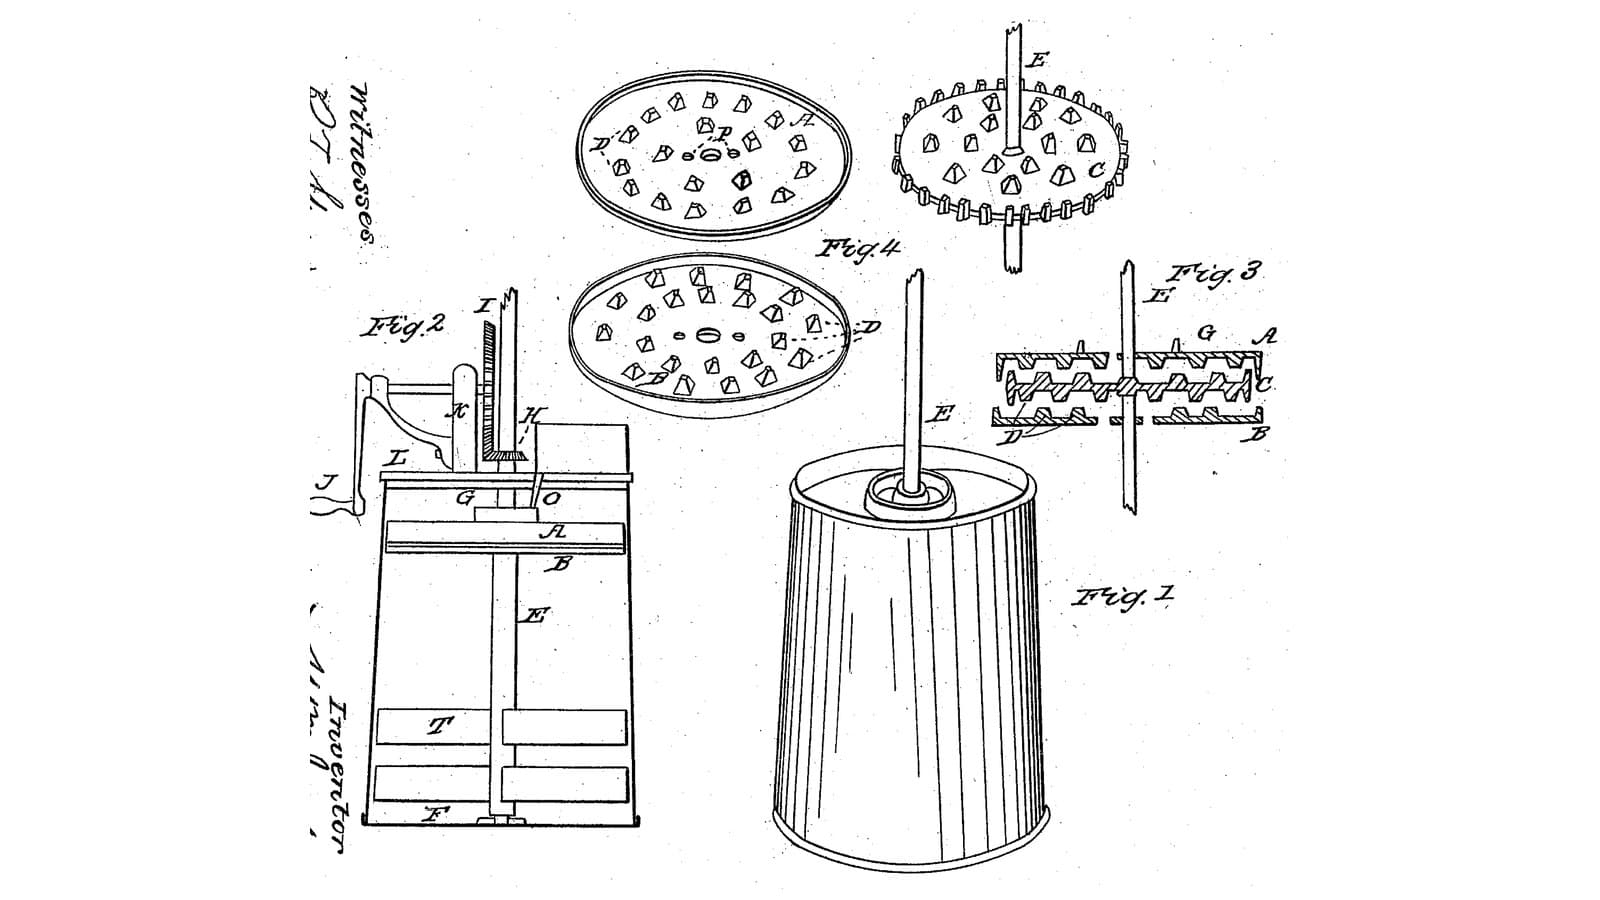
Toothed-Disk Pass Churn: Cream Poured In Passes Once Between Fixed Toothed Disks and a Toothed Wheel Spinning Between Them
por Buttercup
Carpintería
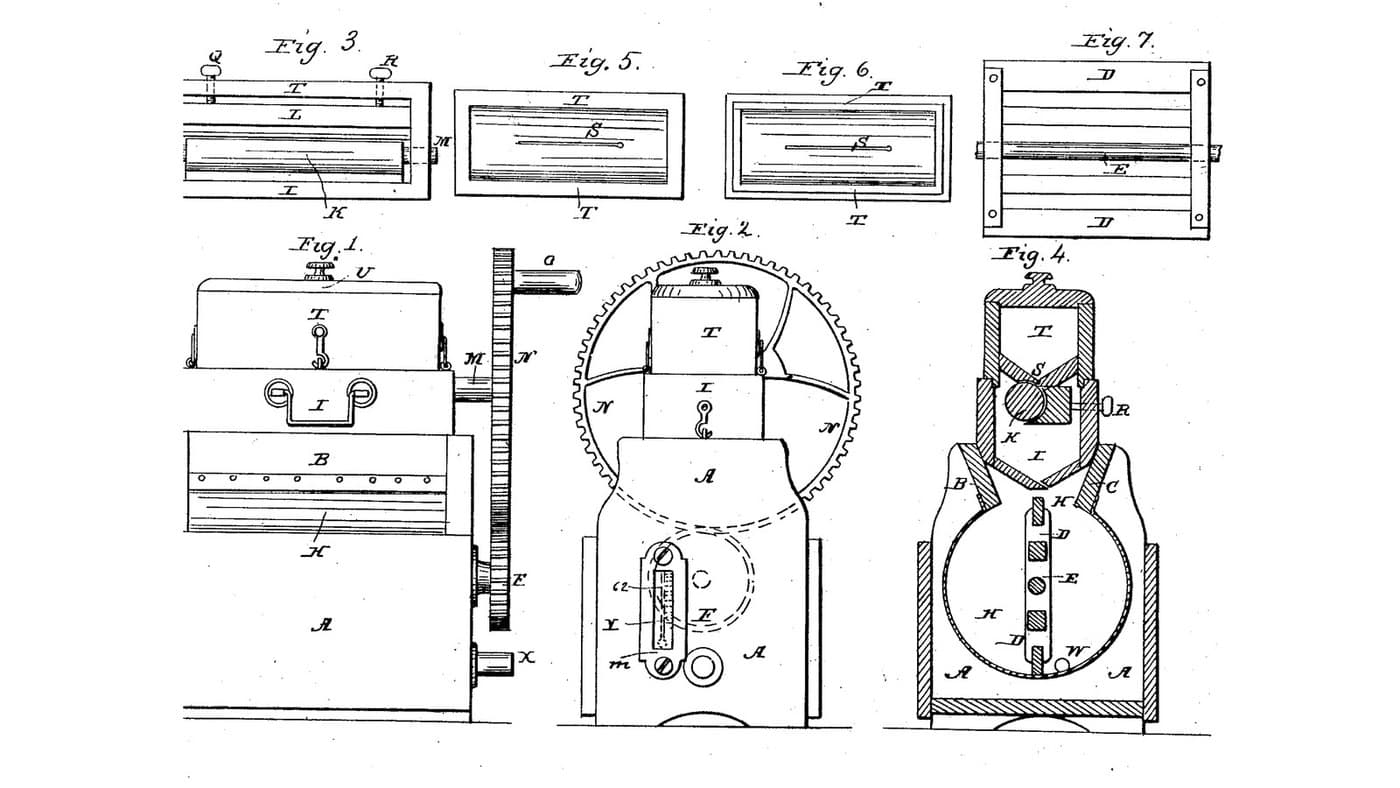
Roller-and-Concave Churn: Cream Falls Between a Turning Roller and an Adjustable Concave, Then Onto a Dasher Below
por Buttercup
Carpintería

Churning Butter from Cream — The 5,000-Year-Old Fat Separation
por TheChef
ARTESANÍA
CC0 Dominio público
Este Blueprint se publica bajo CC0. Eres libre de copiar, modificar, distribuir y usar este trabajo para cualquier propósito, sin pedir permiso.
Apoya al Maker comprando productos a través de su Blueprint, donde gana una Comisión del Maker establecida por los vendedores, o crea una nueva iteración de este Blueprint e inclúyela como conexión en tu propio Blueprint para compartir ingresos.