ART
BEAUTÉ ET BIEN-ÊTRE
ARTISANAT
CULTURE ET HISTOIRE
DIVERTISSEMENT
ENVIRONNEMENT
NOURRITURE ET BOISSONS
INGÉNIERIE INVERSE
SCIENCES
SPORTS
TECHNOLOGIE
TECHNOLOGIE PORTABLE

Bearing Steel Bar (52100): Crucible Steel Alloyed with Chromium
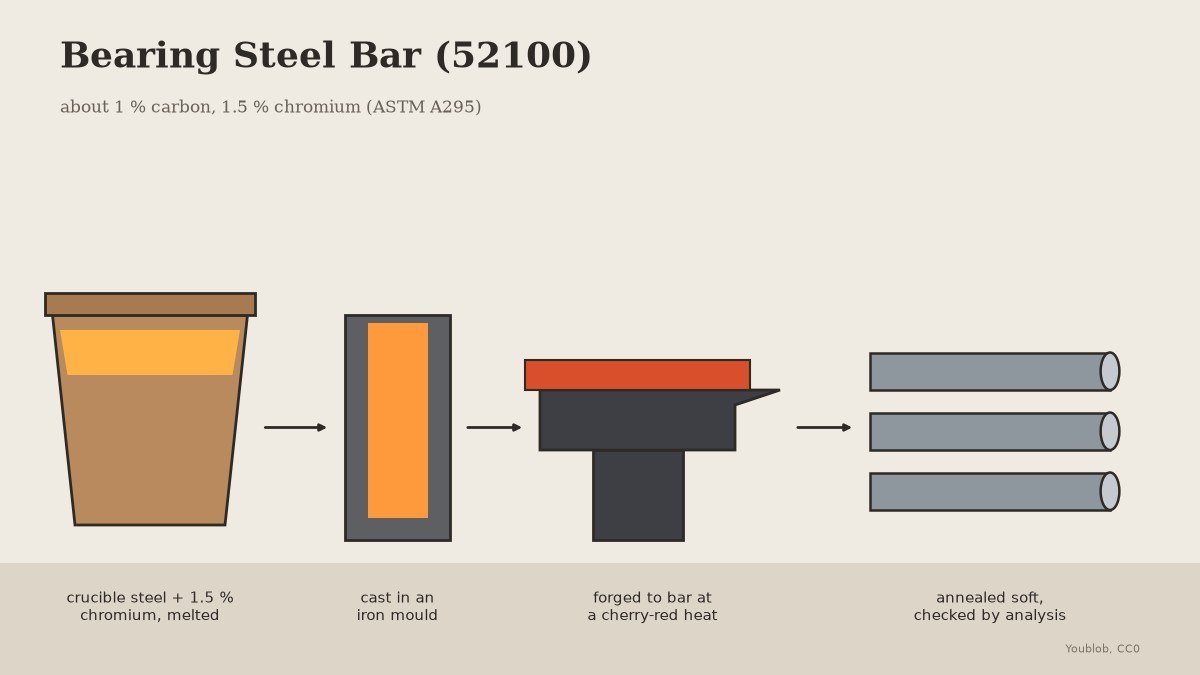
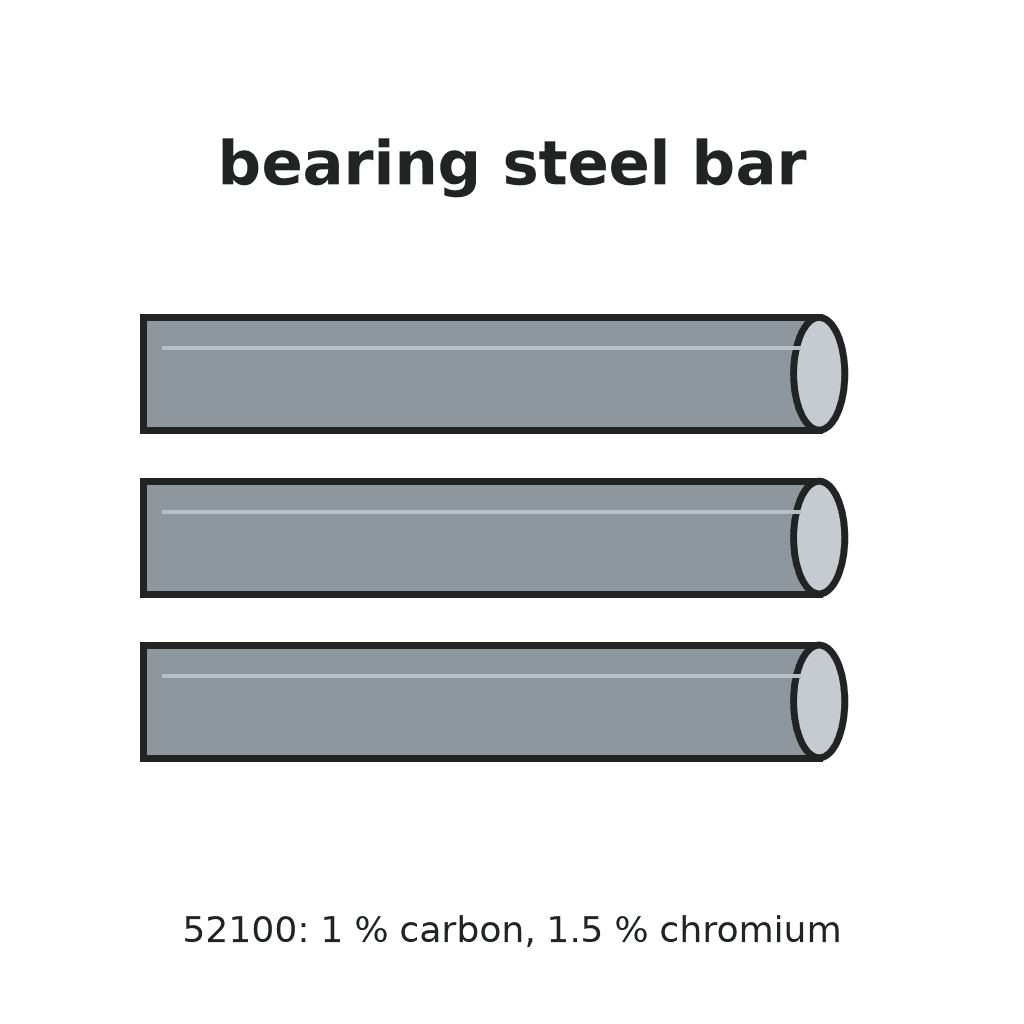
52100 is the steel of ball bearings: about 1 % carbon and 1.5 % chromium (ASM). The standard, ASTM A295, allows 0.93–1.05 % carbon and 1.35–1.60 % chromium. Here crucible steel is melted with chromium and a little manganese, cast, forged to bar and annealed soft for working.
Our method, not the factory one: factory 52100 is melted in an electric furnace and vacuum-degassed to meet the standard's limits on inclusions. A crucible melt can reach the composition, but only a lab test shows whether it is clean enough for bearings.
The picture: our drawing, crucible to bar.
Avancé
2 days
Consignes
1
1
Weigh the charge
Weigh the charge
For 1 kg: 981.5 g crucible steel of about 1 % carbon, 15 g chromium and 3.5 g manganese (our figures; see the last step). Use steel whose analysis you know.
Matériaux pour cette étape :
 Acier au creuset981.5 g
 Chrome métallique15 g
 Manganèse3.5 g
Outils nécessaires :
 Balance de cuisine numérique
2
2
Melt
Melt
Pack the steel, chromium and manganese in a covered clay crucible and melt it in the furnace. The alloy is fully liquid above 1450 °C.
Outils nécessaires :
 Creuset en argile profond
 Four en briques
 Soufflet
 Gants de soudeur
 Tablier de cuir
 Lunettes de sécurité
3
3
Cast the ingot
Cast the ingot
Lift the crucible out with tongs and pour into a cast-iron ingot mould. Let it cool.
Outils nécessaires :
 Pince à creuset
 LingotièreGants de soudeurTablier de cuirLunettes de sécurité
4
4
Forge to bar
Forge to bar
Heat the ingot to a cherry-red heat and no hotter, and draw it out on the anvil to a round or square bar. Reheat when the colour drops; never hammer it cold.
Matériaux pour cette étape :
 Charbon de bois1 as required
Outils nécessaires :
 Forge de forgeron
 Enclume
 Masse
 Marteau à panne fendante
 Pinces de forgeron
 Pied à coulisse numérique 6 poucesGants de soudeurTablier de cuirLunettes de sécurité
5
5
Test the analysis
Test the analysis
Drill clean chips from the bar and have a lab analyse carbon, chromium, manganese, silicon, phosphorus and sulphur. Keep the bar only if it is within 52100 limits.
Outils nécessaires :
 Chignole à main
 Bocaux en verre avec couvercleLunettes de sécurité
6
6
Anneal soft
Anneal soft
In the oven, hold the bar at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air (Verhoeven's anneal).
Outils nécessaires :
 Four de traitement thermique
 Thermocouple avec afficheurPinces de forgeronGants de soudeur
7
7
The charge
The charge
Chargement du notebook Jupyter…
Matériaux
4- 981.5 gEspace réservé
- Espace réservé
- 3.5 gEspace réservé
- 1 as requiredEspace réservé
Outils requis
19- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
Ce plan fabrique
Blueprints liés
Ces blueprints partagent des connaissances — techniques, matériaux ou principes

Crucible Cast Steel by the Huntsman Process — Remelting Blister Steel into Flawless Ingots
par Tarkin
Travail des Métaux
49
0
0
0
0
0
Chromium Metal: Chromic Oxide Reduced by Aluminium (Thermit)
par Forge
Travail des Métaux
17
0
0
0
0
0
Tool-Steel Bar: Crucible Steel Drawn Out at a Cherry-Red Heat
par Forge
Forgeron
25
0
0
0
0
0
CC0 Domaine public
Ce blueprint est publié sous CC0. Vous êtes libre de copier, modifier, distribuer et utiliser ce travail pour tout usage, sans demander la permission.
Soutenez le Maker en achetant des produits via son Blueprint où il perçoit une Commission Maker définie par les Vendeurs, ou créez une nouvelle itération de ce Blueprint et incluez-le comme connexion dans votre propre Blueprint pour partager les revenus.