ART
BEAUTÉ ET BIEN-ÊTRE
ARTISANAT
CULTURE ET HISTOIRE
DIVERTISSEMENT
ENVIRONNEMENT
NOURRITURE ET BOISSONS
INGÉNIERIE INVERSE
SCIENCES
SPORTS
TECHNOLOGIE
TECHNOLOGIE PORTABLE
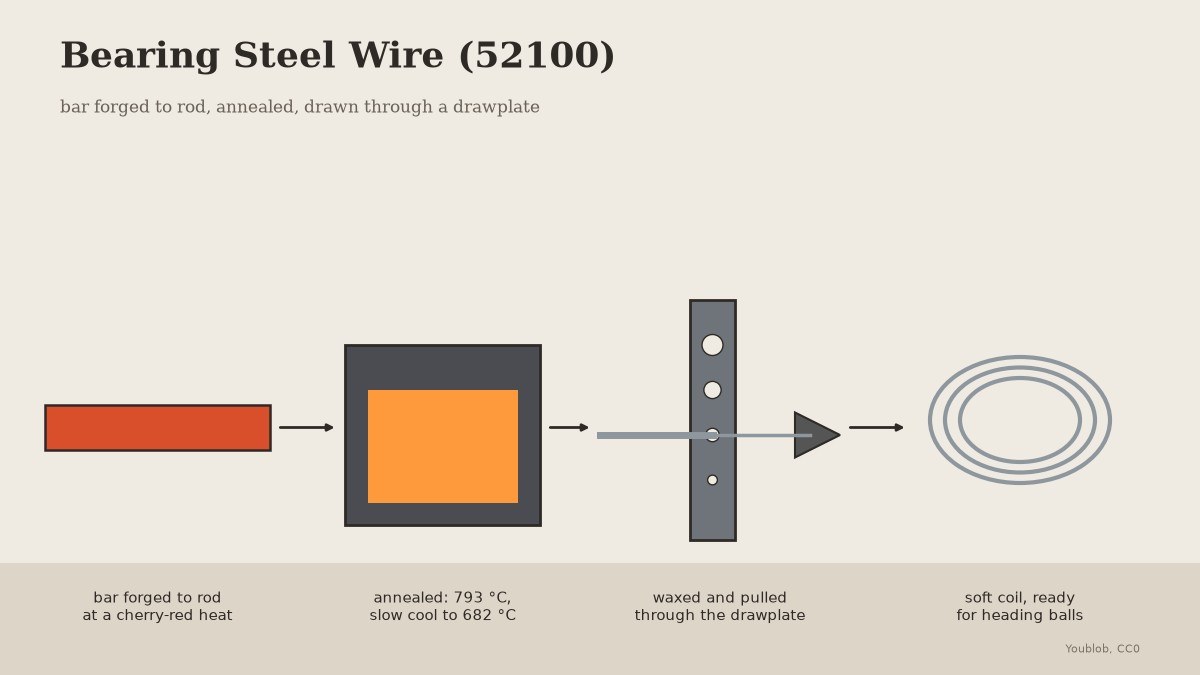


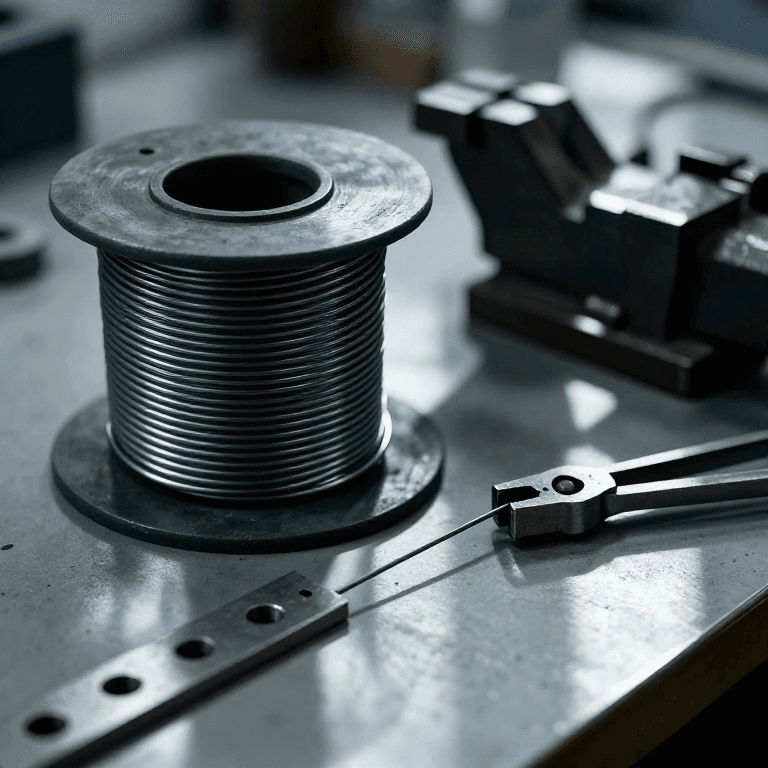
Bearing Steel Wire (52100): Drawn from Bar Through a Drawplate
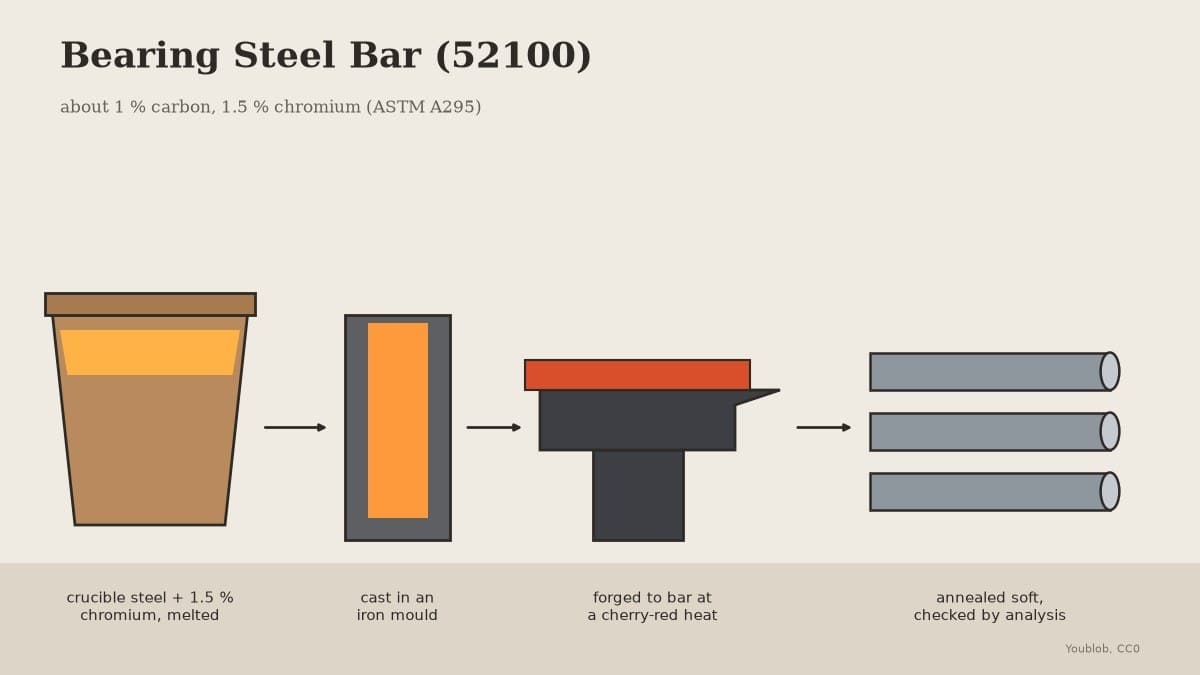
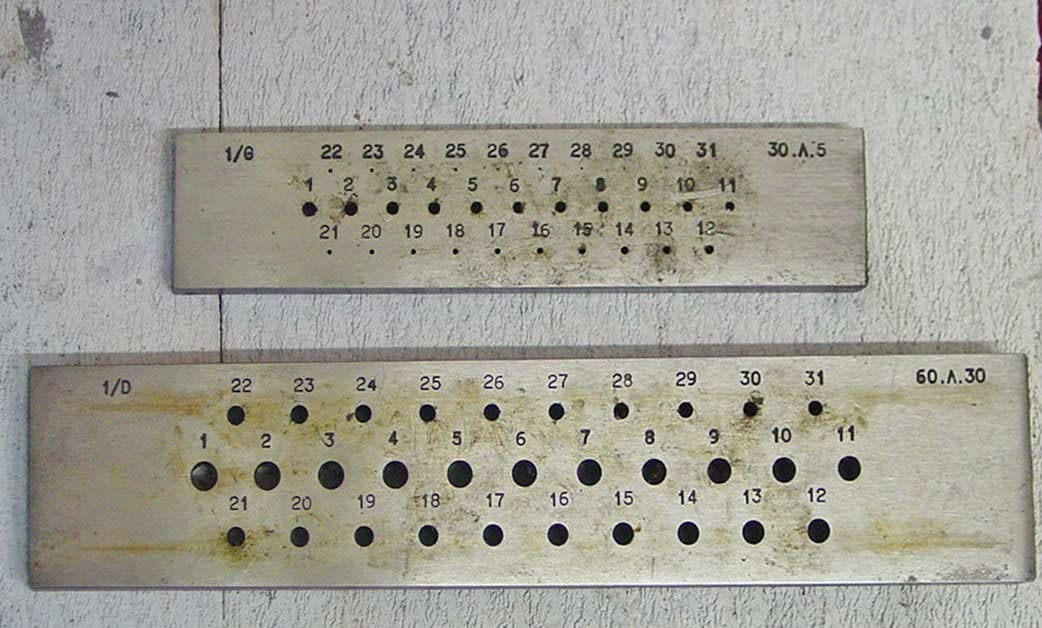
Bearing balls are headed from thick wire of 52100 steel. Here 52100 bar is forged to rod and drawn through a drawplate. At 1 % carbon it is much harder than mild steel, so it is annealed soft before drawing and again after every two holes, using the 52100 anneal Verhoeven recommends.
The picture: our drawing, bar to coil.
Avancé
2 days
Consignes
1
1
Forge to rod
Forge to rod
Heat the bar to a cherry-red heat and no hotter, and draw it out round on the anvil to a rod a little thicker than the drawplate's largest hole.
Matériaux pour cette étape :
 Barre en acier à roulements (52100)1 kg
 Charbon de bois1 as required
Outils nécessaires :
 Forge de forgeron
 Enclume
 Marteau à panne fendante
 Pinces de forgeron
 Gants de soudeur
 Lunettes de sécurité
2
2
Anneal
Anneal
In the oven, hold it at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air.
Outils nécessaires :
 Four de traitement thermique
 Thermocouple avec afficheurPinces de forgeronGants de soudeur
3
3
Clean and taper
Clean and taper
Brush off all the scale, then file a long taper on the first 3 cm so it passes the first hole.
Outils nécessaires :
 Jeu de brosses métalliques
 Jeu de limes
 Étau d'établi
4
4
Wax and draw
Wax and draw
Clamp the drawplate in the vise. Wax the rod, push the taper through the first hole it does not slip through, and pull straight out with the draw tongs in one steady pull.
Matériaux pour cette étape :
 Cire d'abeille20 g
Outils nécessaires :
 Filière en acier
 Tenailles à étirerÉtau d'établi
 Gants de travail en cuir
5
5
Anneal every two holes
Anneal every two holes
Draw through each next hole without skipping. After every two holes, coil the wire and anneal it again: hold it at 793 °C (1460 °F) for 30 minutes, cool in the oven no faster than 500 °C an hour to 682 °C (1260 °F), then cool in air.
Matériaux pour cette étape :
Cire d'abeille1 pièceOutils nécessaires :
Filière en acierTenailles à étirerFour de traitement thermiqueThermocouple avec afficheur6
6
Finish soft
Finish soft
Stop at the diameter your balls need, checked with the caliper, and give the coil a last anneal so it is soft for heading.
Outils nécessaires :
 Pied à coulisse numérique 6 poucesFour de traitement thermiqueThermocouple avec afficheur
7
7
Troubleshooting
Troubleshooting
Bearing steel wire troubleshooting.
Flow
Loading...
Matériaux
3- Espace réservé
- 1 as requiredEspace réservé
- 1 pièceEspace réservé
Outils requis
15- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
Ce plan fabrique
Blueprints liés
Ces blueprints partagent des connaissances — techniques, matériaux ou principes
CC0 Domaine public
Ce blueprint est publié sous CC0. Vous êtes libre de copier, modifier, distribuer et utiliser ce travail pour tout usage, sans demander la permission.
Soutenez le Maker en achetant des produits via son Blueprint où il perçoit une Commission Maker définie par les Vendeurs, ou créez une nouvelle itération de ce Blueprint et incluez-le comme connexion dans votre propre Blueprint pour partager les revenus.