ART
BEAUTÉ ET BIEN-ÊTRE
ARTISANAT
CULTURE ET HISTOIRE
DIVERTISSEMENT
ENVIRONNEMENT
NOURRITURE ET BOISSONS
INGÉNIERIE INVERSE
SCIENCES
SPORTS
TECHNOLOGIE
TECHNOLOGIE PORTABLE
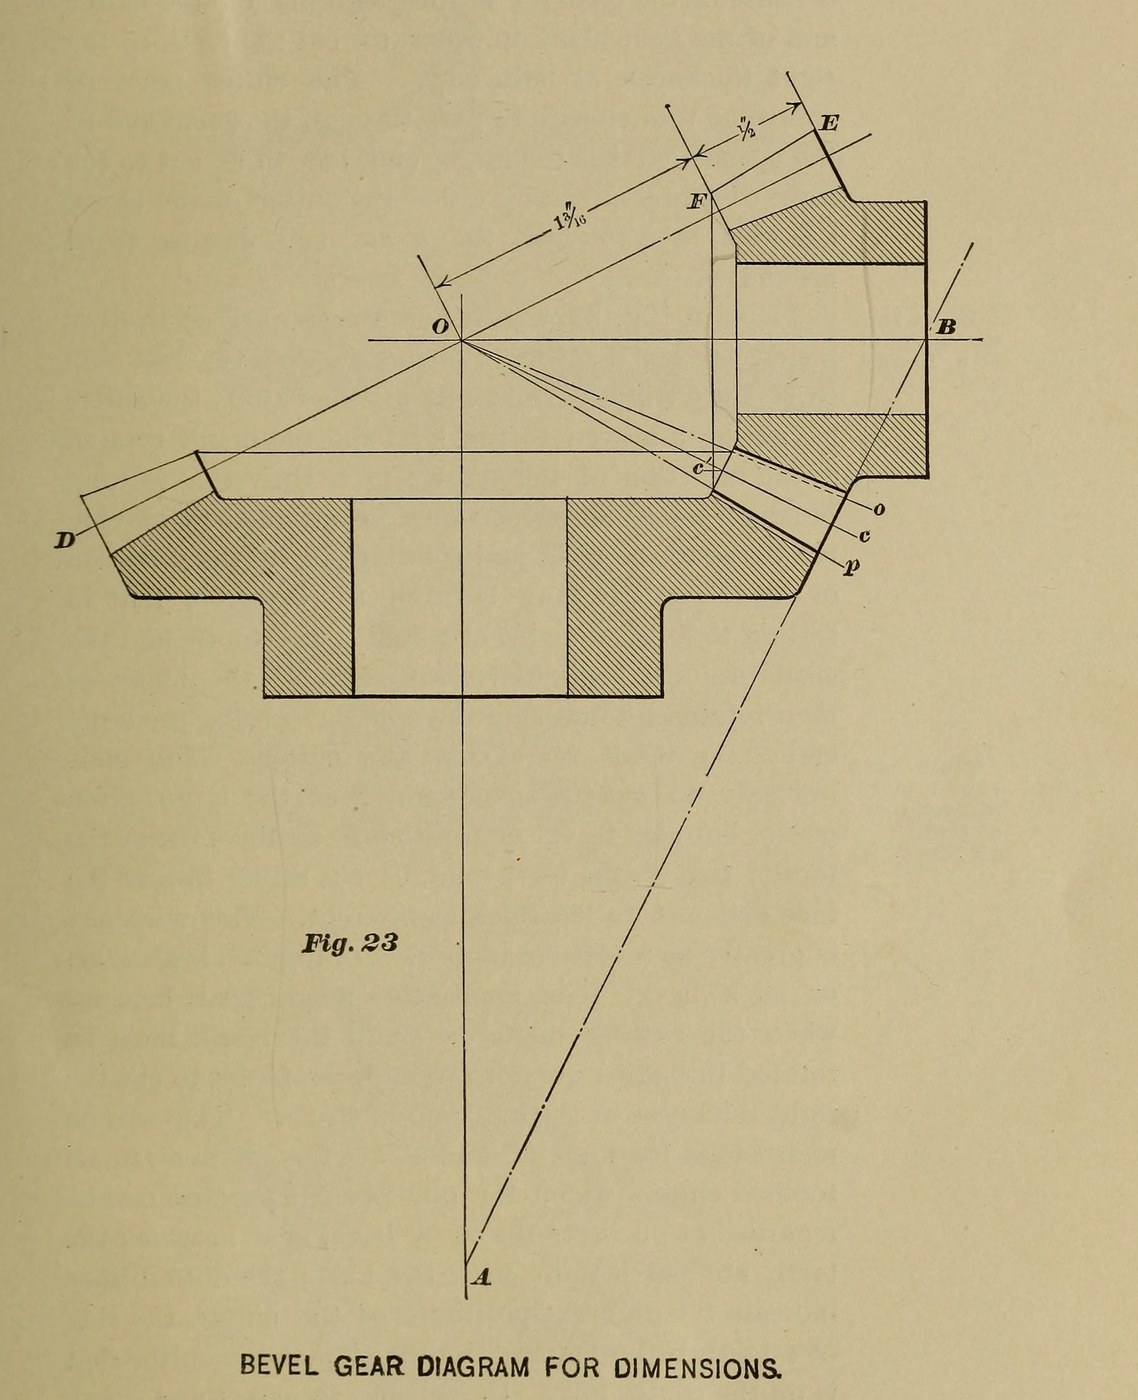


Bevel Pinion: 12 Teeth, 8 Pitch, for a 24-Tooth Gear (Brown & Sharpe 1911)
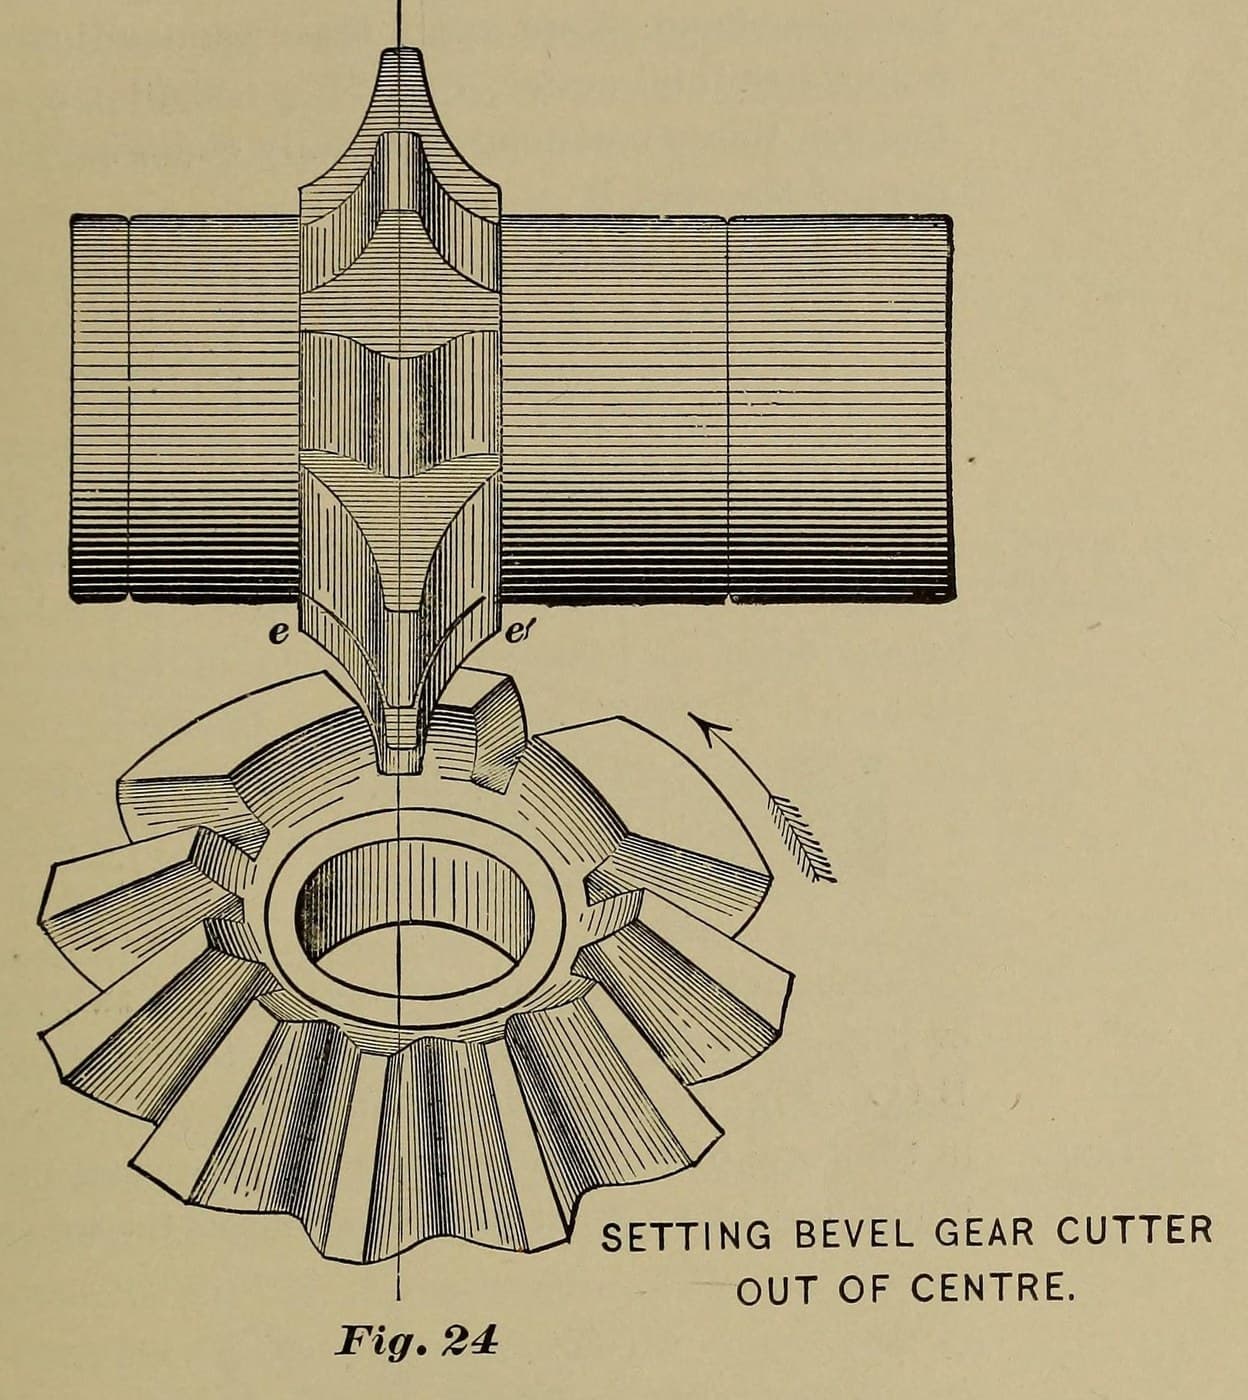
Brown & Sharpe's own worked example: the small gear of a 12 and 24 tooth bevel pair, 8 pitch, shafts at right angles, cut with the No. 8 cutter they send to anyone who orders one for this pinion. The method is the same as for mitre gears: set off centre, cut each side, file the small ends.
Source: Brown & Sharpe, Practical Treatise on Gearing (1911), Fig. 23 example, Part I ch. IX–X, Part II ch. III and the set-over table p. 58. The blank sizes are our arithmetic with their rules; the steel and bore are ours. Picture: their Fig. 23.
Avancé
1 day
Consignes
1
1
Work out and turn the blank
Work out and turn the blank
Pitch diameter 12 ÷ 8 = 1.500 in. Angle of edge 26° 34′ and angle of face 59° 11′ (Brown & Sharpe's figures for every 12 and 24 tooth pair). Diameter increment = cos 26° 34′ × 0.250 = 0.224 in, so turn the steel blank to 1.72 in outside diameter. Face ½ in long. Try both angles with a protractor against the end of the hub.
Matériaux pour cette étape :
 Barre d'acier doux1 length for one blank
Outils nécessaires :
 Tour à métaux
 Outil de coupe pour tour
 Rapporteur
 Micromètre
2
2
Choose the cutter
Choose the cutter
Twice the back cone radius × 8 comes to about 13, so a No. 8, 8-pitch bevel gear cutter. Measure its thickness Tc at the pitch line, 0.145 in from its tip.
Outils nécessaires :
 Fraise pour engrenages coniques
 Pied à coulisse pour dents d’engrenage
3
3
Set the head at 22° 18′
Set the head at 22° 18′
Apex distance = sec 26° 34′ × 1.5 = 1.677 in. Angle increment: tan = sin 26° 34′ ÷ 6, giving 4° 16′. Set the dividing head to the cutting angle 26° 34′ − 4° 16′ = 22° 18′ and index 12 spaces. Depth at the large end 0.270 in.
Outils nécessaires :
 Fraiseuse
 Tête diviseuseFraise pour engrenages coniques
4
4
Set over and cut one side
Set over and cut one side
Apex distance ÷ face = 3.35; we take the nearest column, 3¼, where a No. 8 cutter has the factor .286. Set-over = Tc ÷ 2 − .286 ÷ 8 = Tc ÷ 2 − 0.036 in. Set off centre by that amount, take up backlash, and cut round all 12 spaces.
Outils nécessaires :
FraiseuseTête diviseuseFraise pour engrenages coniques5
5
Set over the other way and trim
Set over the other way and trim
Set over the same amount the other side, line the cutter up with the space at the small end, take a trial cut, and rotate toward the cutter until the tooth is 0.196 in thick at the large end and 0.138 in at the small end. Check with the gear tooth vernier, then cut round.
Outils nécessaires :
FraiseuseTête diviseuseFraise pour engrenages coniquesPied à coulisse pour dents d’engrenage6
6
File the small ends
File the small ends
File the teeth rounder at the small ends, where the cutter could not, without filing them thinner at the pitch line. The cutting angle is under 30°, so the spaces may come out narrower at the face than the cutter suggests; Brown & Sharpe's own shop used a No. 6 cutter here instead.
Outils nécessaires :
 Lime fine
Matériaux
1- 1 length for one blankEspace réservé
Outils requis
9- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
Ce plan fabrique
Blueprints liés
Ces blueprints partagent des connaissances — techniques, matériaux ou principes
CC0 Domaine public
Ce blueprint est publié sous CC0. Vous êtes libre de copier, modifier, distribuer et utiliser ce travail pour tout usage, sans demander la permission.
Soutenez le Maker en achetant des produits via son Blueprint où il perçoit une Commission Maker définie par les Vendeurs, ou créez une nouvelle itération de ce Blueprint et incluez-le comme connexion dans votre propre Blueprint pour partager les revenus.