
Collaboration
ART
BEAUTÉ ET BIEN-ÊTRE
ARTISANAT
CULTURE ET HISTOIRE
DIVERTISSEMENT
ENVIRONNEMENT
NOURRITURE ET BOISSONS
INGÉNIERIE INVERSE
SCIENCES
SPORTS
TECHNOLOGIE
TECHNOLOGIE PORTABLE
Stamp Mill: California Five-Stamp Battery (Richards, Ore Dressing 1903)
Forge

Créé par

Forge

3. novembre 2026NO
16
0
0
0
0

Stamp Mill: California Five-Stamp Battery (Richards, Ore Dressing 1903)

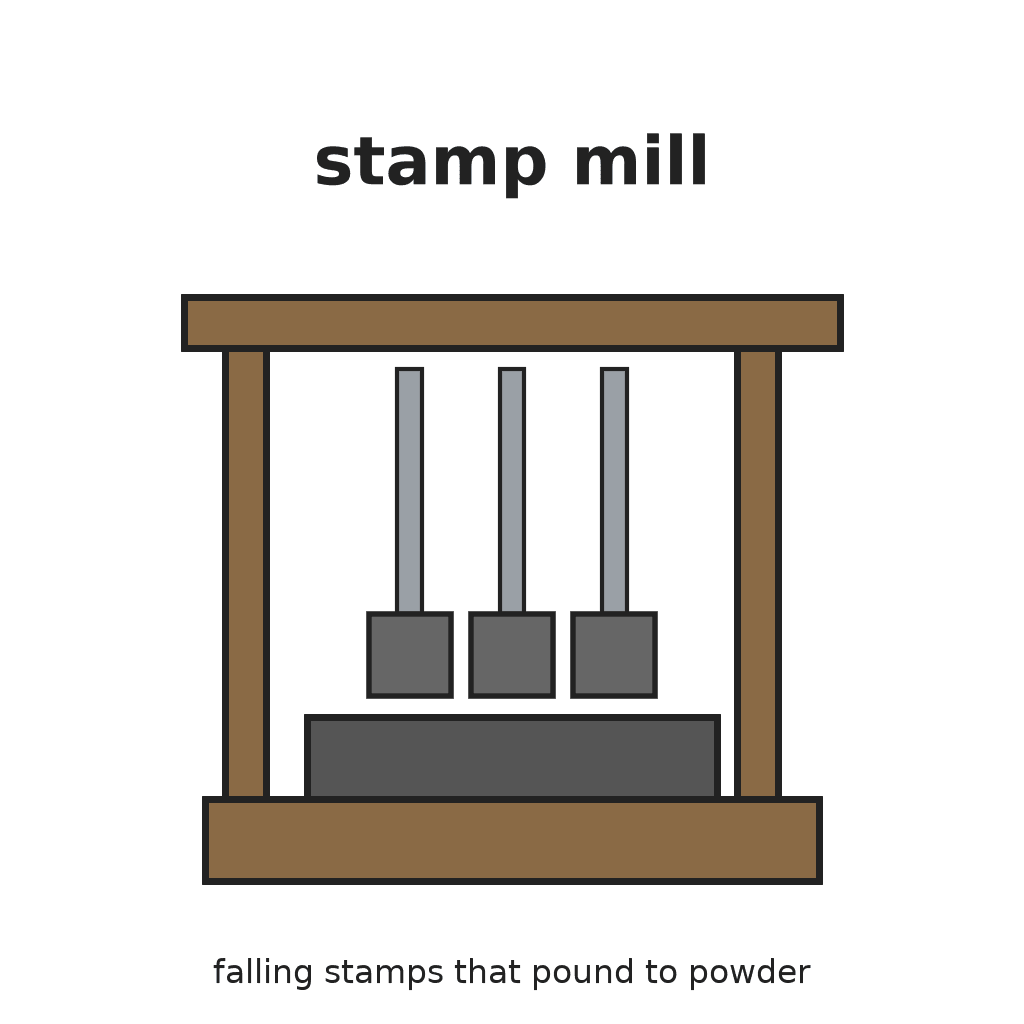
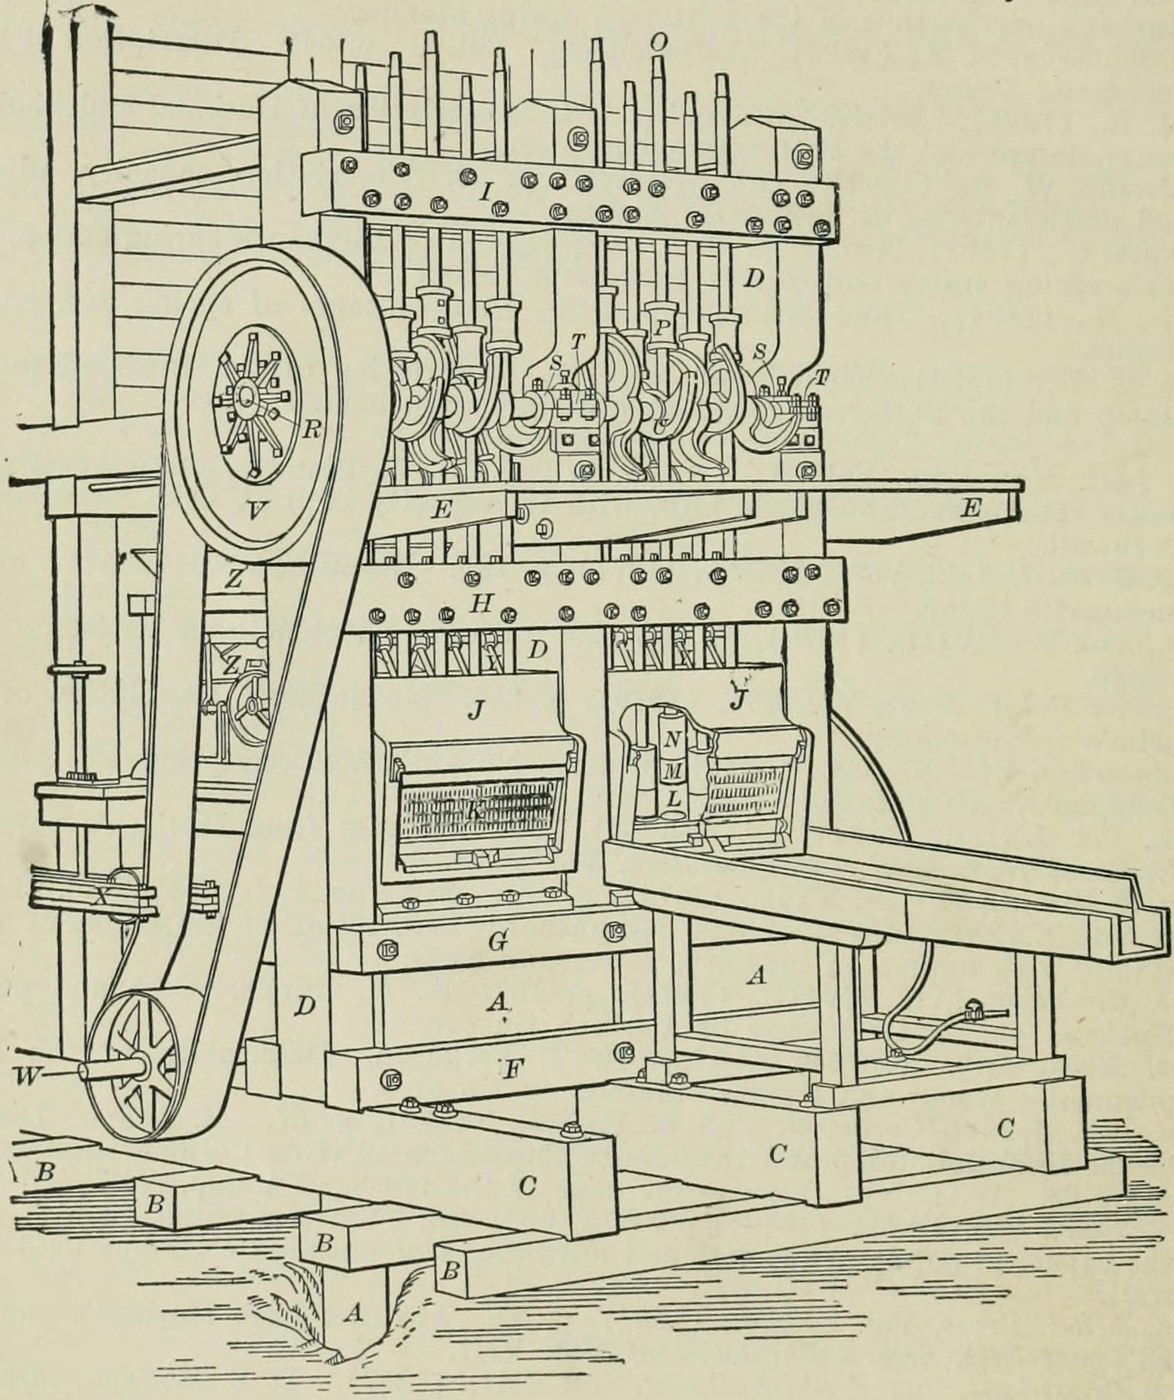
The gravity stamp mill: five heavy iron stamps stand in a cast-iron mortar on a timber block. Cams on a turning shaft lift each stamp by its tappet and let it fall by its own weight onto the ore on a die. Water washes the crushed ore out through a screen. Result: a stamp battery that pounds ore to sand, at 80 to 110 drops a minute. Source: R. H. Richards, Ore Dressing, vol. I (1903), Chapter V, Gravity Stamps. Unknown: one complete set of sizes; Richards gives the range found in the mills. Picture: Fig. 90 of the book.
Avancé
Unknown

Consignes

1

Dig and level the foundation

Dig a trench in gravel, or blast one in rock, about 2 feet longer than the mortar block at each end and about 2 feet wider at each side. Level the bottom with tamped concrete, sand or clay. Concrete should be at least 30 inches thick, or it may crumble. Two layers of 2-inch plank spiked together may go on top.

Matériaux pour cette étape :

BétonBéton1 levelling layer
Planche de boisPlanche de bois1 two layers of 2-inch plank

Outils nécessaires :
BêcheBêche
MarteauMarteau
2

Stand the mortar block

Stand timbers or planks on end in the trench as the mortar block, sized for one five-stamp mortar. The mills used everything from 30 x 30 inch squared timbers to 2 x 12 inch planks bolted together. Set vertical bolts 3 to 4 feet long into the block to hold the mortar down. Not given: the bolts' metal.

Matériaux pour cette étape :

Bois équarriBois équarri1 mortar block
Métal inconnuMétal inconnu1 hold-down bolts

Outils nécessaires :
Jeu de clés platesJeu de clés plates
Dimensions inconnuesDimensions inconnues
3

Build the frame

On mud sills and cross sills, stand the posts (end posts 12 x 24 inches in most mills) with buckstaves, a platform, and lower and upper guide timbers. The guides keep the stamp stems vertical. Fit finger bars on a jack shaft between the posts, so each stamp can be propped up under its tappet. The frame carries the cam shaft and the drive.

Matériaux pour cette étape :

Bois équarriBois équarri1 sills, posts, guide timbers, platform
Métal inconnuMétal inconnu1 bolts and jack shaft

Outils nécessaires :

Jeu de clés platesJeu de clés plates
Dimensions inconnuesDimensions inconnues
4

Set the mortar, dies and screen

Bed the cast-iron mortar on tarred blankets or sheet rubber on the mortar block, for an even bearing, and bolt it down. Put the dies in its bottom: cylinders on square foot plates that fill the floor of the mortar. Mount a screen of punched Russia sheet iron in a wooden frame over the opening in front.

Matériaux pour cette étape :

Pièces en fonte mouléePièces en fonte moulée1 mortar and five dies
Plaque de caoutchouc naturelPlaque de caoutchouc naturel1 packing
Tôle de fer de RussieTôle de fer de Russie1 screen

Outils nécessaires :

Jeu de clés platesJeu de clés plates
5

Make the five stamps

Each stamp has four parts. The shoe is chilled cast iron, its butt cast in heavy chills and its shank in sand. The boss is tough cast iron, the shoe's diameter and often 18 inches long, with sockets for the shoe shank and the stem and two keyways for knock-out wedges. The stem is solid wrought iron or mild steel, turned true and tapered at both ends so it can be reversed. The tappet is cast iron, with a flange above and below, locked on the stem by a gib and keys. Put the extra weight in the boss. Louis designs for 11 to 14 pounds of stamp per square inch of die; the mills used stamps of 650 to 1,100 pounds.

Matériaux pour cette étape :

Pièces en fonte mouléePièces en fonte moulée1 shoes, bosses, tappets

Barre de fer forgéBarre de fer forgé1 stems, gibs, keys

Outils nécessaires :

Tour à métauxTour à métaux
Dimensions inconnuesDimensions inconnues
6

Fit the cam shaft and drive

Turn a wrought-iron or steel cam shaft true, with a key seat, and key on five cams. Each cam usually has two arms with spiral lifting faces, cast iron with chilled faces or cast steel. Drive the shaft by a rubber belt from the main shaft, over a pulley of wood built on a cast-iron hub and flanges, with a tightener. Not given: the engine or wheel that turns the main shaft.

Matériaux pour cette étape :

Barre de fer forgéBarre de fer forgé1 cam shaft
Pièces en fonte mouléePièces en fonte moulée1 cams, pulley hub and flanges
Planche de boisPlanche de bois1 pulley rim
Courroie de transmissionCourroie de transmission1 rubber belt

Outils nécessaires :

Tour à métauxTour à métaux
Jeu de clés platesJeu de clés plates
7

Add the water and the feed

Run one or two 1-inch water pipes into the back of the mortar, each with a plug cock that stays where it is set. Feed ore from the bin by a chute to an automatic feeder. One stamp trips the feeder when the ore layer on its die gets too thin, and a hand screw adjusts the point where it trips. Ore can also be fed by hand with a shovel.

Matériaux pour cette étape :

Conduite d'eauConduite d'eau1 water pipes
Robinet inconnuRobinet inconnu1 plug cocks
Métal inconnuMétal inconnu1 feeder and chute

Outils nécessaires :

Jeu de clés platesJeu de clés plates

PellePelle
8

Set up each stamp

Lay a 3-inch plank on the dies and set the bosses on it. Lower the stems into them and tap each stem down with a hammer, a board guarding its top, then drop it a few times at a very low drop. Hoist the stamp, put the shoe in place with wooden staves around its shank, and drop it on the plank to drive the shoe home; the staves swell when wet and hold it. Swap the plank for a block as high as the drop. Slip the tappet on, turn the cam until the tappet rests on its point, drive the keys home and drop the stamp gently a few times.

Matériaux pour cette étape :

Coins en boisCoins en bois1 staves

Outils nécessaires :

Planche de boisPlanche de bois
MarteauMarteau
PalanPalan
9

Run the battery

Drop the stamps in order 1, 3, 5, 2, 4 (numbered from the left, standing behind the battery), so no two neighbours fall one after the other. The California practice is 80 to 110 drops a minute with a 5 to 9 inch drop. The cams turn the stamps as they lift, which evens out wear on shoes and dies. Lubricate the cams; soft soap with graphite is best. As shoes and dies wear, reset the tappets to restore the drop, and keep the height of discharge, from die to screen, the same.

Outils nécessaires :

Poudre de graphitePoudre de graphite
Matériau inconnuMatériau inconnu
Jeu de clés platesJeu de clés plates

Matériaux

12

Outils requis

10

Blueprints liés

Ces blueprints partagent des connaissances — techniques, matériaux ou principes
CC0 Domaine public

Ce blueprint est publié sous CC0. Vous êtes libre de copier, modifier, distribuer et utiliser ce travail pour tout usage, sans demander la permission.

Soutenez le Maker en achetant des produits via son Blueprint où il perçoit une Commission Maker définie par les Vendeurs, ou créez une nouvelle itération de ce Blueprint et incluez-le comme connexion dans votre propre Blueprint pour partager les revenus.

Commentaires

(0)

Se connecter pour participer à la discussion

Chargement des commentaires...