
Collaboration
ART
BEAUTÉ ET BIEN-ÊTRE
ARTISANAT
CULTURE ET HISTOIRE
DIVERTISSEMENT
ENVIRONNEMENT
NOURRITURE ET BOISSONS
INGÉNIERIE INVERSE
SCIENCES
SPORTS
TECHNOLOGIE
TECHNOLOGIE PORTABLE
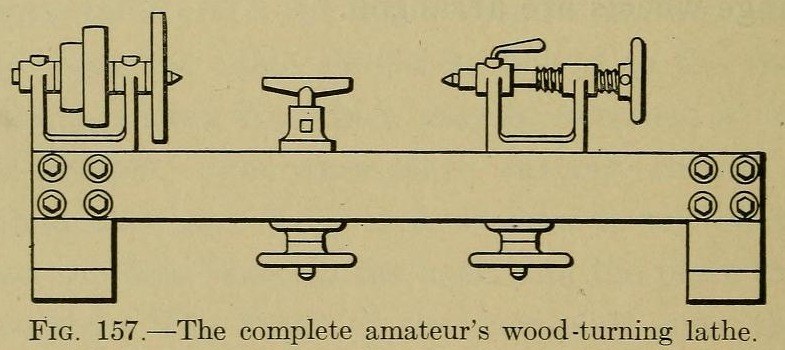
Wood Lathe: Simple Amateur's Lathe with a Maple Bed, 7 in Swing (Lathe Work for Beginners, 1922)
Woody

Créé par

Woody

4. novembre 2026NO
11
0
0
0
0

Wood Lathe: Simple Amateur's Lathe with a Maple Bed, 7 in Swing (Lathe Work for Beginners, 1922)

A wood-turning lathe an amateur can build: two strips of hard maple bolted to maple legs make the 3 ft bed, and cast-iron head-stock, tail-stock, hand-rest body, hand wheels and cone pulleys are cast from home-made patterns. Steel spindles turn in the cast-iron bearings, and a cone pulley drives the head-stock from a countershaft. Result: a wood lathe with a 7 in swing and a 3 ft bed. Source: R. F. Yates, Lathe Work for Beginners (1922), Chapter XII, pp. 208-216. Unknown: the pattern sizes (on the book's drawings) and the drive. Picture: Fig. 157 of the book.
Avancé
Unknown

Consignes

1

Make the patterns and get castings

Make patterns from any handy wood: one for both head-stock and tail-stock, with a web joining the two bearings so the casting does not spring; one for the hand wheels (three castings); one for the washers (two); the cone pulley (two: lathe and countershaft); and the hand-rest body. Give them a slight draw taper. Have them cast in iron at a foundry. Not given: pattern sizes (on the book's drawings).

Matériaux pour cette étape :

Pièces en fonte mouléePièces en fonte moulée1 head-stock, tail-stock, wheels, washers, pulleys, rest body

Outils nécessaires :
Planche de boisPlanche de bois
CubilotCubilot
Dimensions inconnuesDimensions inconnues
2

Build the maple bed

Make the bed of two strips of clear hard maple 1 in thick, 4 in wide and about 36 in long (about 1 1/2 in thick for a longer bed), and two maple legs, the part between the ways cut exactly square. Bore a 5/8 in hole through the head-stock leg in line with the head-stock's 1/2 in tapped hole, recessed below for a nut and washers. Bolt bed to legs with eight 3/8 in carriage bolts. Sand it and give it a coat of clear shellac against warping. White oak will do if there is no maple.

Matériaux pour cette étape :

Planche de bois durPlanche de bois dur1 ways and legs
Boulon de carrosserieBoulon de carrosserie8 3/8 in carriage bolts
Gomme laqueGomme laque1 finish

Outils nécessaires :

Perceuse à colonnePerceuse à colonne
Papier abrasifPapier abrasif
3

Machine the stocks

Face the outside ends of the head-stock and tail-stock bearings on a shaper or milling machine. Drill the bearings between centres in a lathe with a 47/64 in drill, saw off the joining web, face the inner ends and ream to 3/4 in. Line both castings up on a 3/4 in shaft and machine their bottoms. Drill oil holes in the head-stock lugs. Tap the tail-stock front lug 3/16 in for a clamp turned, heated and bent to shape, with soft copper or brass under it; tap the tail-stock rear bearing 7/8 in, 9 threads.

Matériaux pour cette étape :

Métal inconnuMétal inconnu1 clamp and copper pad

Outils nécessaires :
FraiseuseFraiseuse
Tour à métauxTour à métaux
Jeu de tarauds et filièresJeu de tarauds et filières
ForgeForge
4

Turn the spindles and pulley

Turn the head-stock spindle from 1 3/8 in machine steel: 3/4 in diameter, a 7/8 in nose threaded 9 to the inch, a 3/8 in hole right through and a No. 1 Morse taper in the nose. Turn the tail-stock spindle from 7/8 in stock, 3/4 in diameter with a 7/8 in, 9-thread part. Centre each piece, drill halfway from each end with a 3/8 in drill, ream, then finish between centres. Turn the cone pulley with crowned faces, wide enough to run easily between the bearings, and fix it to the spindle with a 3/8 in headless set screw.

Matériaux pour cette étape :

Barre ronde en acier douxBarre ronde en acier doux1 spindles
Métal inconnuMétal inconnu1 set screws

Outils nécessaires :

Tour à métauxTour à métaux
Perceuse à colonnePerceuse à colonne
5

Fit the wheels and hand rest, and assemble

Drill hand wheel N 3/4 in for the tail-stock spindle and hold it with a 1/4 in set screw; tap the other two wheels 1/2 in. Drill the washers 9/16 in. Bolt the head-stock down with a stud through the leg, and fit a 1/2 in stud about 7 in long for the tail-stock and a 1/2 in square-headed bolt for the hand-rest body. Plane the hand rest's bottom, drill it 3/4 in, and fit tee-rests of 1/4 x 1 in flat steel welded to 3/4 in shafting, held by a 1/4 in set screw; make several lengths. The cast iron serves as bearing metal, or the bearings can be bushed or babbitted.

Matériaux pour cette étape :

Plat en acier douxPlat en acier doux1 tee-rests
Métal inconnuMétal inconnu1 studs, bolts, set screws, shafting

Outils nécessaires :

Perceuse à colonnePerceuse à colonne
Jeu de tarauds et filièresJeu de tarauds et filières
ForgeForge

Matériaux

7

Outils requis

9

CC0 Domaine public

Ce blueprint est publié sous CC0. Vous êtes libre de copier, modifier, distribuer et utiliser ce travail pour tout usage, sans demander la permission.

Soutenez le Maker en achetant des produits via son Blueprint où il perçoit une Commission Maker définie par les Vendeurs, ou créez une nouvelle itération de ce Blueprint et incluez-le comme connexion dans votre propre Blueprint pour partager les revenus.

Commentaires

(0)

Se connecter pour participer à la discussion

Chargement des commentaires...