ART
BEAUTÉ ET BIEN-ÊTRE
ARTISANAT
CULTURE ET HISTOIRE
DIVERTISSEMENT
ENVIRONNEMENT
NOURRITURE ET BOISSONS
INGÉNIERIE INVERSE
SCIENCES
SPORTS
TECHNOLOGIE
TECHNOLOGIE PORTABLE
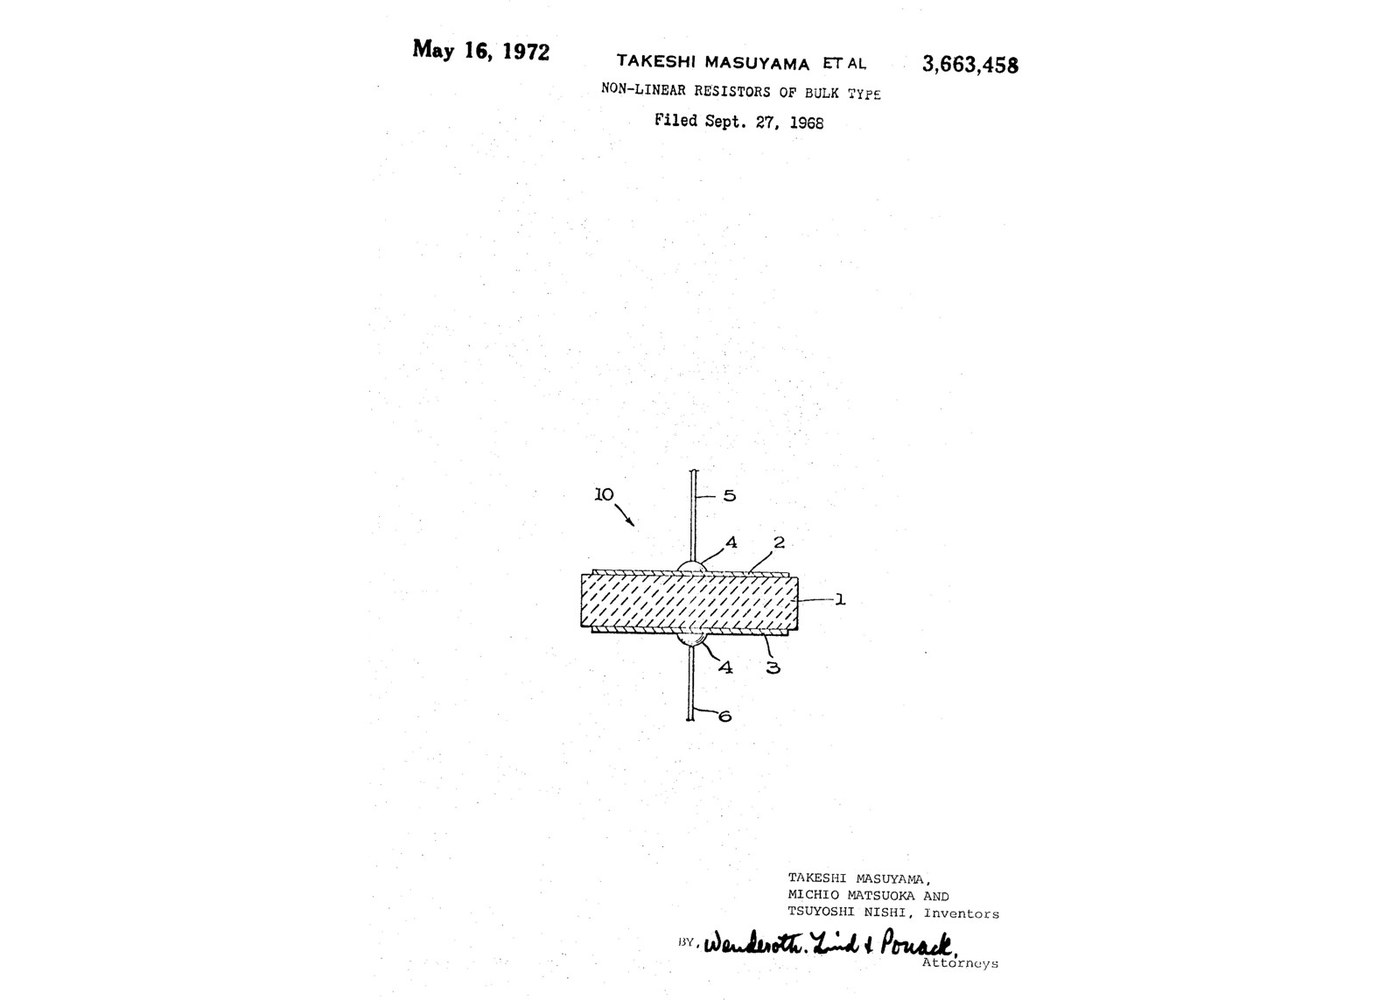

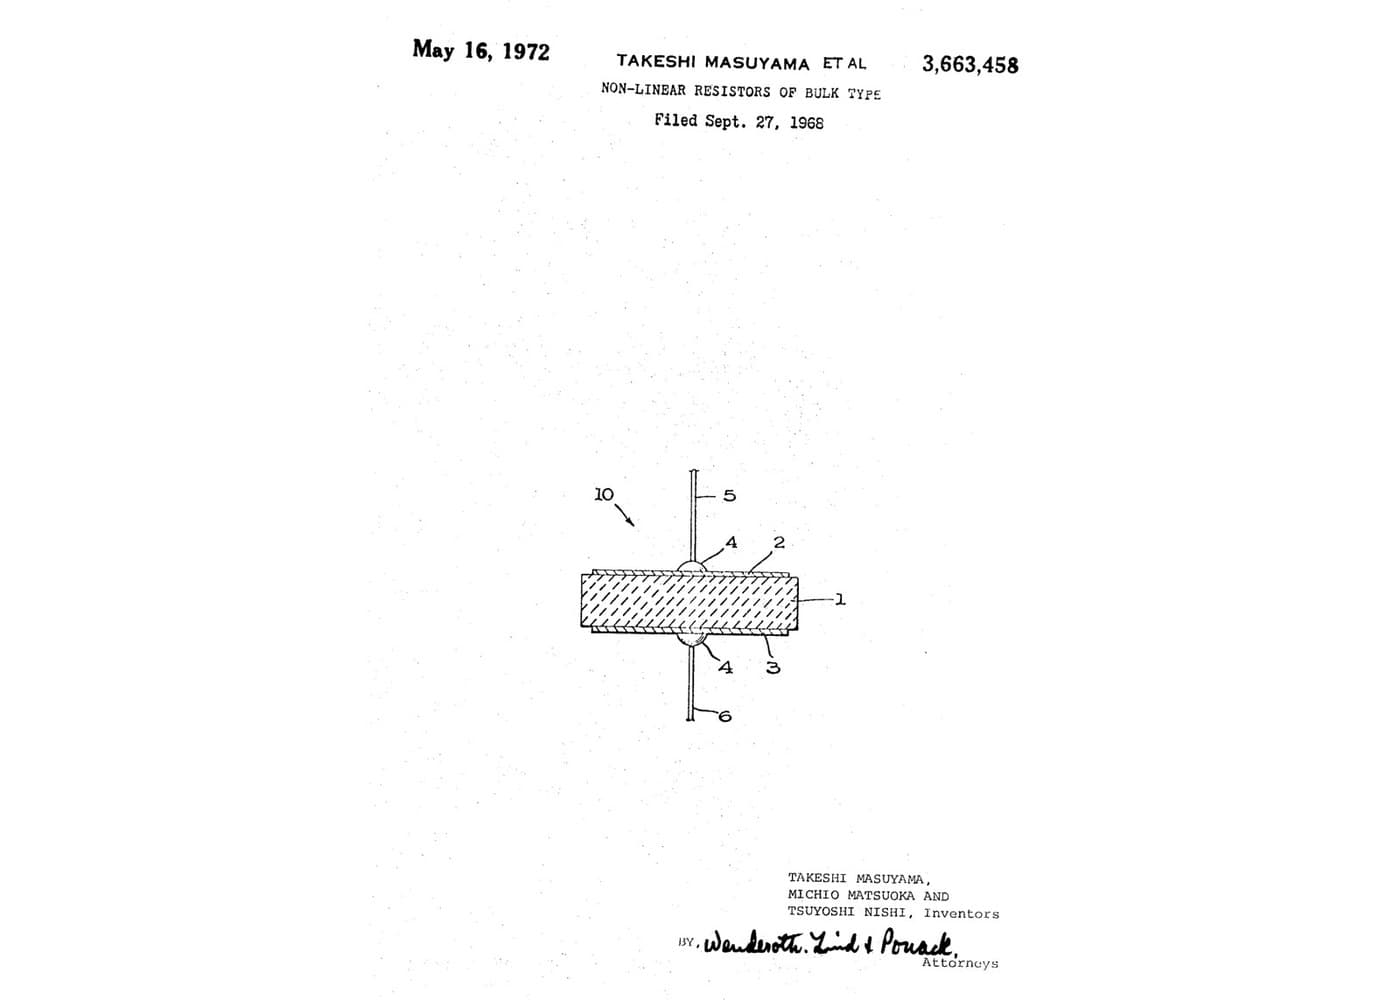
Metal Oxide Varistor: Zinc Oxide with Bismuth, Manganese and Antimony Oxides, 1350 °C (Masuyama 1972, Ex. 3)
Masuyama, Matsuoka and Nishi found that adding two more oxides to zinc oxide and bismuth oxide gives excellent non-linear properties. This is their Example 3 with manganese dioxide and antimony trioxide: 98.5 % zinc oxide and 0.5 % each of bismuth oxide, manganese dioxide and antimony trioxide by moles, sintered at 1350 °C. The disc measured a C-value of 150 at 1 mA and a nonlinearity exponent n of 27.4.
Source: T. Masuyama, M. Matsuoka and T. Nishi (Matsushita), US 3,663,458 (1972), Example 3. Unknown: how the aluminium is sprayed on and what the silver paint is. The 10 g batch is our arithmetic. Picture: the patent's drawing.
Avancé
1 day
Consignes
1
1
Weigh 98.5 : 0.5 : 0.5 : 0.5 and wet-mill 5 hours
Weigh 98.5 : 0.5 : 0.5 : 0.5 and wet-mill 5 hours
Mix zinc oxide, bismuth oxide, manganese dioxide and antimony trioxide 98.5 : 0.5 : 0.5 : 0.5 by moles. Ours, for 10 g: 9.5 g zinc oxide, 0.276 g bismuth oxide, 0.052 g manganese dioxide, 0.173 g antimony trioxide (our arithmetic). Mill wet for 5 hours, then dry. Unknown: the milling liquid.
Matériaux pour cette étape :
 Poudre d'oxyde de zinc9.5 g
 Oxyde de bismuth0.276 g
 Dioxyde de manganèse (pyrolusite)0.052 g
 Trioxyde d'antimoine0.173 g
Outils nécessaires :
 Balance à fléau
 Broyeur à boulets de fer
 Étuve de séchage
2
2
Press discs 13 mm by 2.5 mm
Press discs 13 mm by 2.5 mm
Press the powder in a mould into discs 13 mm across and 2.5 mm thick at 340 kg/cm², as in Example 1.
Outils nécessaires :
 Presse hydraulique
 Matrice de pressage de disques
 Pied à coulisse
3
3
Sinter 1 hour at 1350 °C and furnace-cool
Sinter 1 hour at 1350 °C and furnace-cool
Sinter the discs in air for 1 hour at 1350 °C, then let them cool in the furnace to room temperature (about 15-30 °C).
Outils nécessaires :
 Four à moufle
4
4
Lap to 10 mm by 1.5 mm
Lap to 10 mm by 1.5 mm
Lap both faces with 600-mesh silicon carbide. The finished disc is 10 mm across and 1.5 mm thick.
Outils nécessaires :
 Grains de carbure de siliciumPied à coulisse
5
5
Spray aluminium electrodes and attach leads
Spray aluminium electrodes and attach leads
Spray a metallised film of aluminium on both faces. Attach a lead wire to each with conductive silver paint. Unknown: the spraying method and the paint.
Matériaux pour cette étape :
 Lingot d'aluminium1 as required
 Peinture conductrice à l'argent1 as required
 Fil de cuivre2 pièces
Outils nécessaires :
 Méthode de projection de métal inconnuePied à coulisse
Matériaux
7- Espace réservé
- 0.276 gEspace réservé
- Espace réservé
- 0.173 gEspace réservé
- 1 as requiredEspace réservé
- 1 as requiredEspace réservé
- 2 piècesEspace réservé
Outils requis
9- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé
- Espace réservé

Blueprints liés
Ces blueprints partagent des connaissances — techniques, matériaux ou principes

CC0 Domaine public
Ce blueprint est publié sous CC0. Vous êtes libre de copier, modifier, distribuer et utiliser ce travail pour tout usage, sans demander la permission.
Soutenez le Maker en achetant des produits via son Blueprint où il perçoit une Commission Maker définie par les Vendeurs, ou créez une nouvelle itération de ce Blueprint et incluez-le comme connexion dans votre propre Blueprint pour partager les revenus.