SENI
KECANTIKAN & KESEHATAN
KERAJINAN
BUDAYA & SEJARAH
HIBURAN
LINGKUNGAN
MAKANAN & MINUMAN
REKAYASA BALIK
ILMU PENGETAHUAN
OLAHRAGA
TEKNOLOGI
PERANGKAT PAKAI
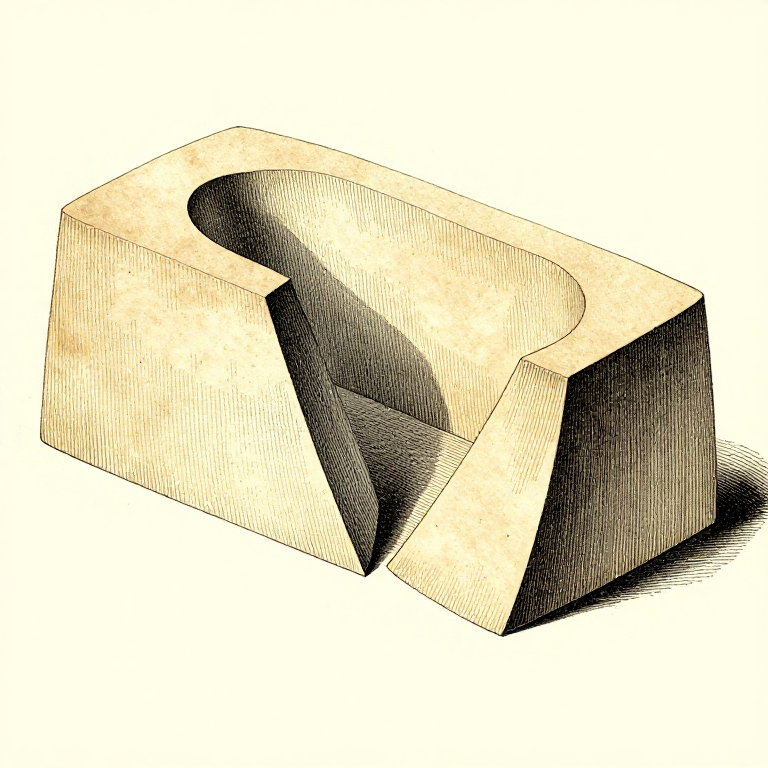

The Pattern Is Not the Part: Draft, Shrinkage and Machining Allowance
A pattern is not a copy of the finished part. It is deliberately LARGER, deliberately TAPERED, and deliberately oversized wherever a machined surface will be cut — and each of those three differences has a separate reason.
DRAFT is the taper that lets the pattern come out of the sand without tearing the mould. SHRINKAGE allowance makes the pattern bigger because metal contracts as it freezes and cools. MACHINING allowance leaves metal for the cutting tool to remove.
Get any of the three wrong and the casting is scrap. Get them right and the same pattern makes identical parts indefinitely, which is the entire economic point of casting.
Menengah
3 hours
Instruksi
1
1
Draft: the pattern has to come out
Draft: the pattern has to come out
Every surface that runs perpendicular to the parting plane must be tapered so the pattern lifts cleanly. A vertical wall drags sand with it and leaves a torn mould, and that tear becomes a lump on the casting.
One to three degrees is usual for sand casting, more for deep pockets and less for shallow ones. The rule of thumb is that a deeper draw needs more draft, because a small angle over a long distance still leaves the sand gripping.
Draft always ADDS material away from the parting line, never removes it. A part that must be a precise size at the bottom of a deep feature has to be machined there, because draft is not optional and it is always in the direction that makes the casting thicker.
Material untuk langkah ini:
 Papan Kayu Keras1 buah
 Pasir cetak1 kg
Alat yang dibutuhkan:
 Set Kikir
 Jangka Sorong Digital 6 Inci
 Penggaris
2
2
Shrinkage: build the pattern oversize by the right amount
Shrinkage: build the pattern oversize by the right amount
Memuat notebook Jupyter…
Material untuk langkah ini:
Papan Kayu Keras1 buah Batangan perunggu1 buah
Alat yang dibutuhkan:
 Komputer DesktopJangka Sorong Digital 6 InciPenggaris
3
3
Machining allowance goes only where a tool will cut
Machining allowance goes only where a tool will cut
A cast surface is rough, slightly scaled, and not accurately placed. Any face that has to be flat, parallel or dimensionally exact must be machined, and the pattern has to carry extra metal there for the tool to remove.
Two to five millimetres is typical for sand casting, and more on large surfaces and on the cope side — the upper half of the mould collects more inclusions, so critical machined faces are placed in the drag where possible.
Do NOT add it everywhere. Extra metal is extra weight, extra cost, extra shrinkage to feed, and extra machining time. Deciding which faces are machined and which are left as-cast is a design decision made before the pattern is started.
Material untuk langkah ini:
Papan Kayu Keras1 buahAlat yang dibutuhkan:
Jangka Sorong Digital 6 InciSet Kikir4
4
Finish the pattern properly, because it prints
Finish the pattern properly, because it prints
Every scratch, dent and grain on the pattern is reproduced in the sand and then in the metal. A pattern sanded smooth and sealed gives a smooth casting; a rough one gives a rough one, and rough castings are harder to clean and harder to machine.
Seal and wax wooden patterns. Bare wood absorbs moisture from green sand, swells and changes size, and it also grips the sand instead of releasing.
Fillet every internal corner. A sharp internal corner in the pattern makes a sharp sand edge that breaks off into the casting, and it makes a stress concentration in the finished part — the same argument as a fillet in a printed part or a forged one.
Material untuk langkah ini:
Papan Kayu Keras1 buah Malam Lebah1 buah
Alat yang dibutuhkan:
Set Kikir Lup PembesarJangka Sorong Digital 6 Inci
Bahan
4- 1 buahPlaceholder
- 1 kgPlaceholder
- 1 buahPlaceholder
- 1 buahPlaceholder
Blueprint terkait
Blueprint ini berbagi pengetahuan — teknik, bahan, atau prinsip
Carving a Stone Mould for Bronze Casting — Open-Face and Bivalve Moulds
oleh Forge
Pengerjaan Logam
76
0
0
0
3
0
Casting a Bronze Socketed Spearhead — Bivalve Mould Method
oleh Forge
Pengerjaan Logam
46
0
0
0
1
0
Fits: Clearance, Transition and Interference — the Difference Is Microns
oleh Martin
Alat Pengerjaan Logam
56
0
0
0
0
0
CC0 Domain Publik
Cetak biru ini dirilis di bawah CC0. Anda bebas untuk menyalin, memodifikasi, mendistribusikan, dan menggunakan karya ini untuk tujuan apa pun, termasuk komersial, tanpa meminta izin.
Dukung Maker dengan membeli produk melalui Cetak Biru mereka di mana mereka mendapatkan Komisi Pembuat yang ditetapkan oleh Penjual, atau buat iterasi baru dari Cetak Biru ini dan masukkan sebagai koneksi di milik Anda sendiri.