همکاری
هنر
زیبایی و سلامت
صنایع دستی
فرهنگ و تاریخ
سرگرمی
محیط زیست
غذا و نوشیدنی
مهندسی معکوس
علوم
ورزش
فناوری
پوشیدنیها
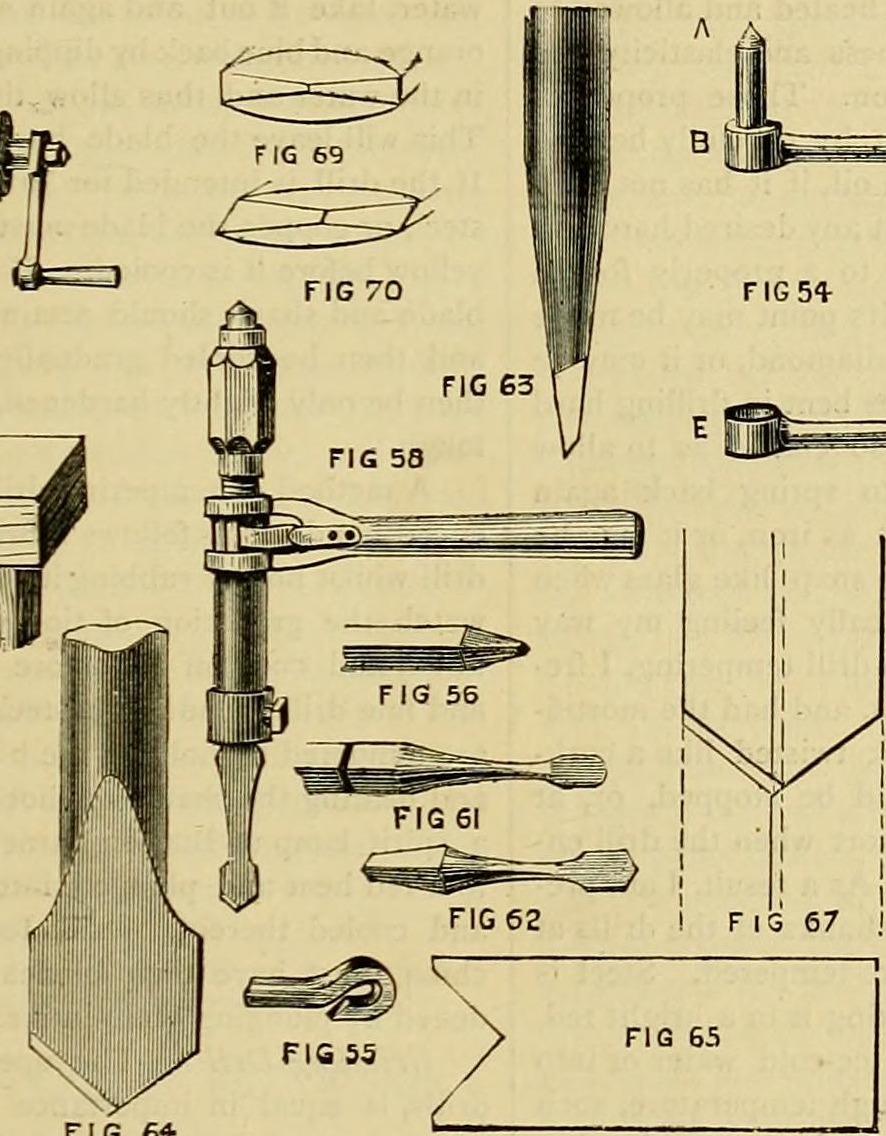

Forged Flat Drills: Tool Steel Drawn to Blade and Square Taper Head, Tempered by Colour for the Metal to Be Drilled (Edwinson, 1886)
How a smith forged his own set of flat drills, from George Edwinson's series in Amateur Work (1886): 3/4 in. square tool steel drawn to a blade and shank with a square taper head, hardened in 45-50 F water and tempered by watching the colours run from a red-hot iron (pale straw for cast iron, orange yellow for wrought iron and copper, purplish yellow for wood), then ground to a notched gauge with clear corners.
پیشرفته
An hour or two per drill
دستورالعملها
1
1
His sizes
His sizes
در حال بارگذاری دفترچهٔ Jupyter…
2
2
Read Edwinson
Read Edwinson
"A good drill may be made to turn out good work even when all other parts are indifferently made."
3
3
Draw the blade
Draw the blade
Cut a two-foot length of 3/4 in. (19 mm) square tool steel. Heat 3 in. to blood red in a clean fire, never hotter, and hammer only down to a dull red before reheating. Draw out the blade and shank first (fig. 61), close to shape.
مواد مورد نیاز این مرحله:
 میلگرد فولاد ابزار1 قطعه
ابزارهای مورد نیاز:
 کورهٔ آهنگری
 سندان
 چکش
 انبر آهنگری
4
4
Forge the head
Forge the head
Cut off the length for the head, hold the blade and shank in grooved flat-bit tongs, and forge a square taper head to fit your brace socket, sides equal, shank and blade central. Finish at a dull red, set true, cool.
ابزارهای مورد نیاز:
 قلم داغکورهٔ آهنگریسندانچکشانبر آهنگری
5
5
Shape and substance
Shape and substance
Taper gradually from head to shank, keep the shank even for an inch or two, then let the blade swell out and thin toward the point (figs. 62, 63). Blade about 1/16 in. at the point and 1/8 in. at the corners for a 1/4 in. drill, up to 3/16 in. for 1/2 or 3/4 in.; a 1/4 in. drill's shank half as thick as a 1/2 in. blade. Leave blades a little full for grinding.
ابزارهای مورد نیاز:
کورهٔ آهنگریسندانچکش6
6
Harden
Harden
Heat to red and plunge the drill straight down into cool water of 45-50 F (7-10 C), holding it until cold: icy water makes the edges brittle. Brighten the blade and part of the shank on a brick or grit-stone.
مواد مورد نیاز این مرحله:
 آب1 قطعه
ابزارهای مورد نیاز:
کورهٔ آهنگری سطل
 دماسنج
 سنگ تیزکنی
7
7
Temper by colour
Temper by colour
Lay the shank across a red-hot piece of stout iron and watch the tints run toward the blade: straw, yellow, orange yellow, purplish yellow, purple, blues. For cast iron and hard brass stop when pale straw reaches the blade, dipping the blade to hold the later colours back while the shank cools in air. For wrought iron, soft steel or copper let the blade reach orange yellow. For wood only, let blade and shank reach purplish yellow and cool slowly.
مواد مورد نیاز این مرحله:
آب1 قطعهابزارهای مورد نیاز:
کورهٔ آهنگری ورقهٔ آهنیسطل
8
8
Grind to a gauge
Grind to a gauge
Cut gauges from thin sheet brass with notches at the point angles (figs. 65, 66): very obtuse for cast iron and hard brass, more acute for wrought iron, tough steel and copper. Grind both edges equal with the point on the centre line, and give the corners clearance (fig. 70). Grind each blade to its finished size.
مواد مورد نیاز این مرحله:
 ورق برنج1 قطعه
ابزارهای مورد نیاز:
 سوهان (سوهان دستی)
 سنگ چرخان تیزکنی
9
9
Troubleshooting
Troubleshooting
Drill troubleshooting.
Flow
Loading...
10
10
History and honest limits
History and honest limits
From George Edwinson, "Smithing and Forging" IV, **Amateur Work, Illustrated**, vol. V (1886), pp. 348-351 and figs. 54-70 (checked on the archive.org scan amateurworkillus05lond; the scan reads 3/4 in. bar where the OCR text says 1/2). He also hardened glass and china drills in mercury: left out here (mercury is a poison). Metric figures, the brass gauge stock and the thermometer are ours.
این نقشه میسازد
نقشههای مرتبط
این نقشهها دانش مشترکی دارند — تکنیکها، مواد یا اصول

Quench Hardening and Tempering a Steel Blade — Heat Treatment Fundamentals
توسط Forge
باستان
۹۸
۰
۰
۰
۲
۰
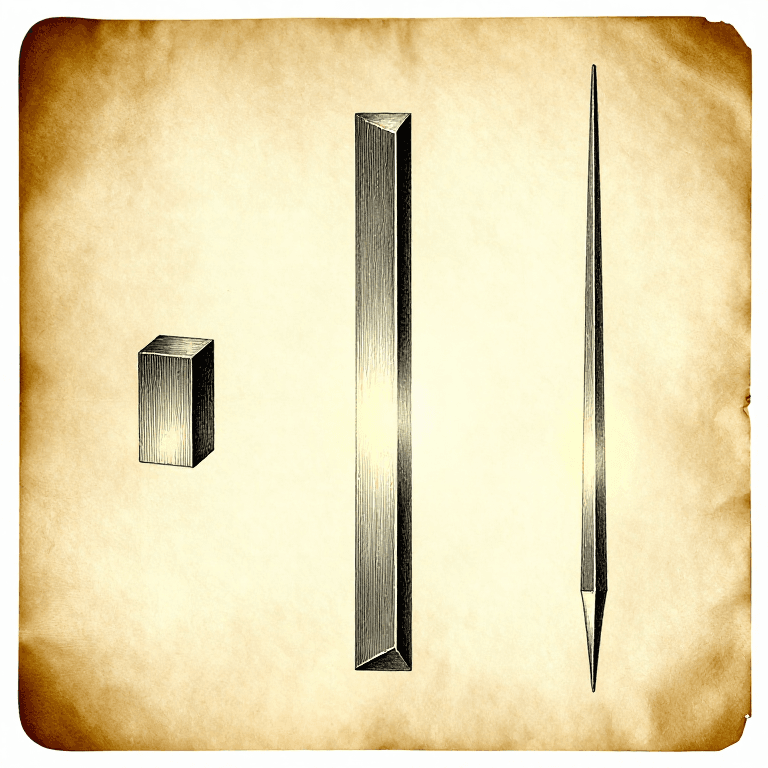
Drawing Out: Making It Longer by Making It Thinner
توسط Forge
ابزارهای فلزکاری
۵۳
۰
۰
۰
۰
۰
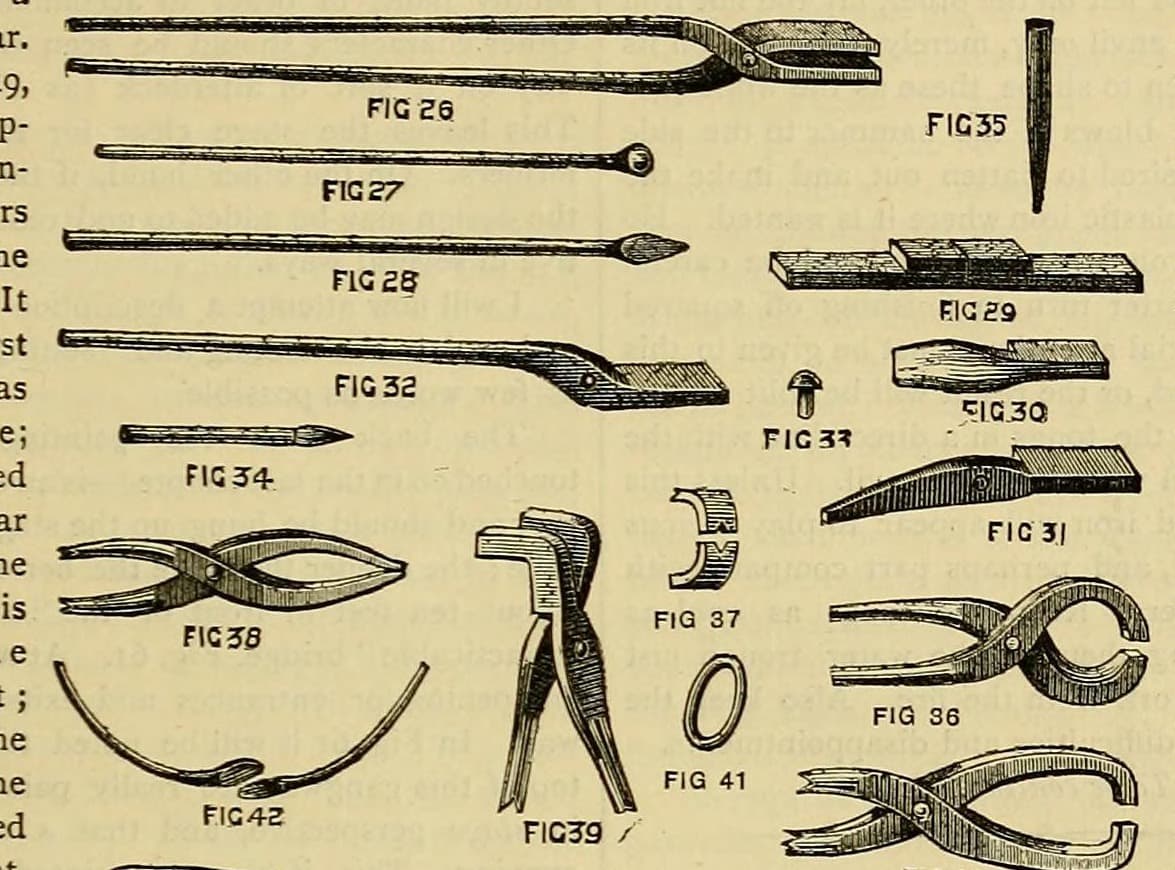
Flat-Bit Tongs and the Tongs Made from Them, down to Crucible Tongs: Welded Reins, Riveted Joint (Edwinson, 1886)
توسط Forge
فلزکاری
۱۰
۰
۰
۰
۰
۰
CC0 مالکیت عمومی
این نقشه تحت مجوز CC0 منتشر شده است. شما آزاد هستید آن را کپی، ویرایش، توزیع و برای هر هدفی بدون نیاز به اجازه استفاده کنید.
با خرید محصولات از طریق نقشه از سازنده حمایت کنید و او کمیسیون سازنده تعیین شده توسط فروشندگان، دریافت میکند یا یک نسخه جدید از این نقشه ایجاد کنید و آن را به عنوان اتصال در نقشه خود قرار دهید تا درآمد به اشتراک گذاشته شود.