Samvinna
LIST
FEGURÐ OG VELLÍÐAN
HANDVERK
MENNING OG SAGA
SKEMMTUN
UMHVERFI
MATUR OG DRYKKUR
ÖFUGVERKFRÆÐI
VÍSINDI
ÍÞRÓTTIR
TÆKNI
KLÆÐANLEG TÆKNI
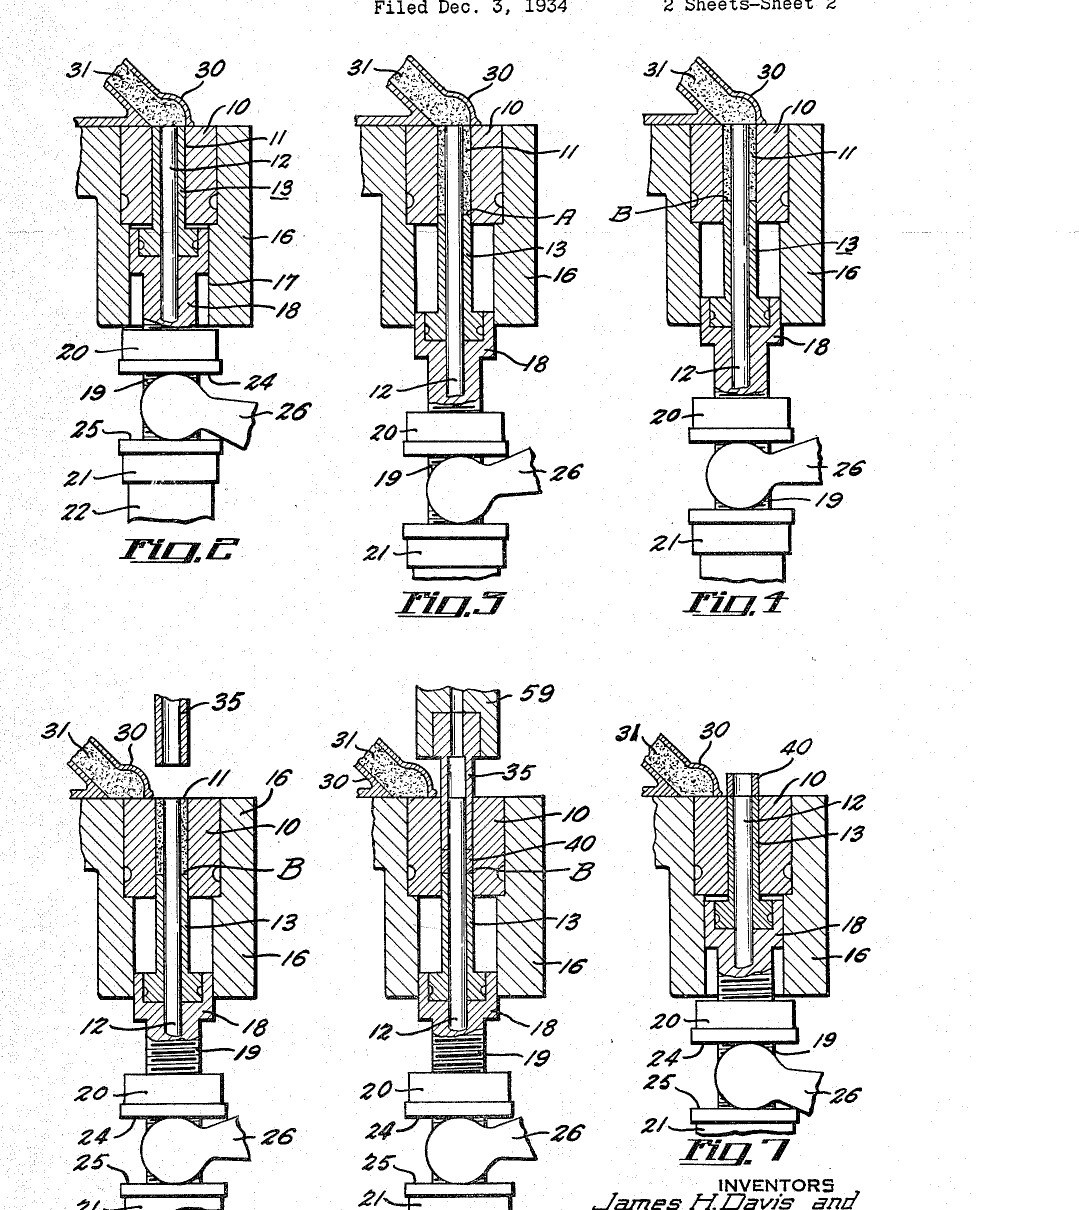


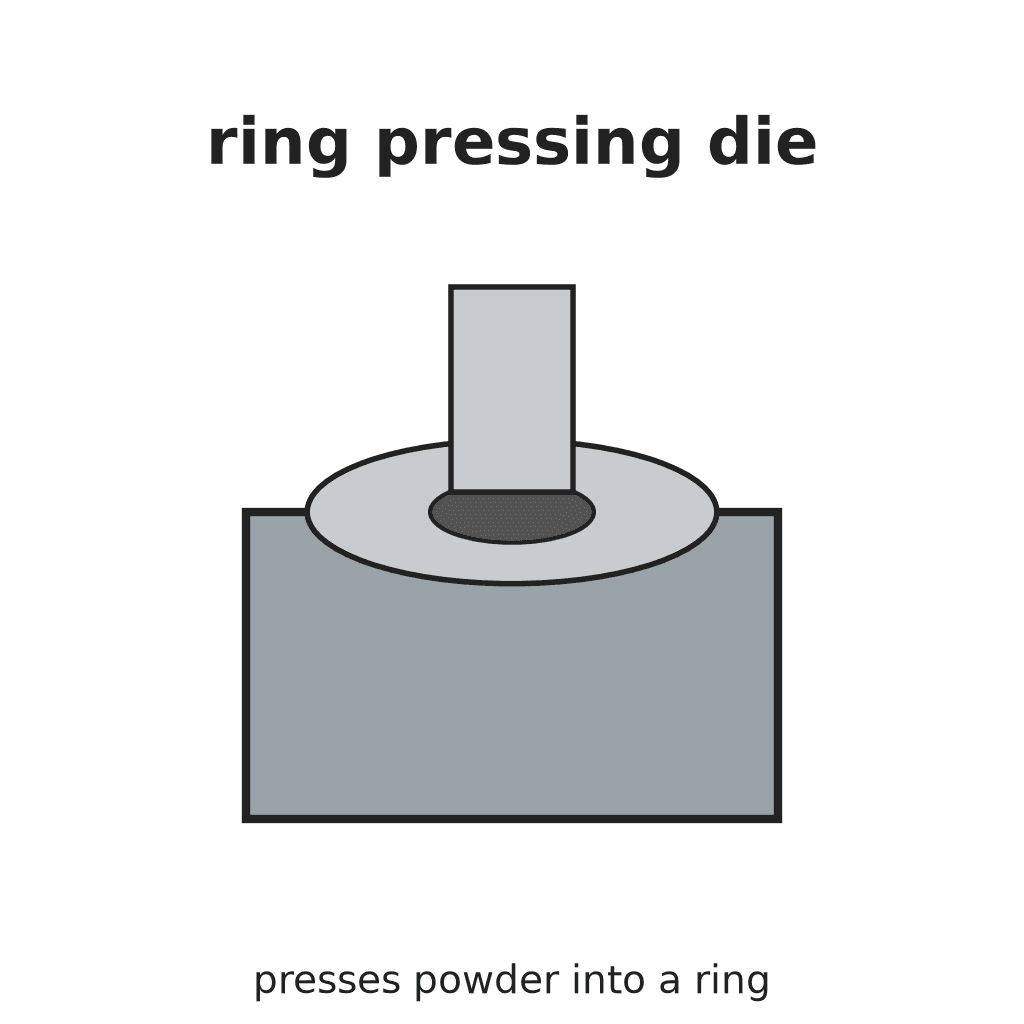
Ring Pressing Die: Core-Rod Die with Tubular Punches and Overfill Filling (Davis & Lemming, GM, US 2,127,994, 1938)
The die set for pressing metal or other powder into rings (bushings, ring cores). A die with a round cavity has a fixed core rod standing up through its middle, so the cavity is ring-shaped; a tube-shaped lower plunger slides up and down round the core rod, and a tube-shaped upper punch comes down to press. Filling is the trick: the lower plunger drops past the pressing point under a shaking shoe of powder, then rises a little to push the surplus back, so every ring gets the same charge with no trapped air.
Result: a die that presses powder into rings of even weight and density, ejected flush with the die top.
Source: J. H. Davis and J. C. Lemming (General Motors), US 2,127,994 (1938). Unknown: steels, sizes, clearances, pressure. Picture: the patent drawing.
Lengra kominn
Unknown
Leiðbeiningar
1
1
Make the die, core rod and punches
Make the die, core rod and punches
Make a die block with a straight round cavity open at both ends. Make a core rod that stands up through the middle of the cavity, its top flush with the die top, threaded at its foot to be anchored in the base with a lock nut. Make a tube-shaped lower plunger that slides in the cavity round the core rod, and a tube-shaped upper punch to match. Not given: the steel, sizes, clearances. Ours: tool steel, turned and threaded on the lathe.
Efni fyrir þetta skref:
 Ferstrent verkfærastál1 die, core rod, punches
 Óþekktur málmur1 lock nut
Nauðsynleg verkfæri:
 Málmrennibekkur
 Snittsett
 Óþekkt mál
2
2
Harden and finish
Harden and finish
The powder wears the cavity wall, so harden the die and punches and polish the working faces. Not given: the hardening or finish. Ours: a heat-treating oven and quench, then lapping with rouge along the stroke as for the disc die.
Nauðsynleg verkfæri:
 Hitameðferðarofn
 Herslufata
 Gullsmiðarautt
3
3
Set it in the press
Set it in the press
Fix the die in a heavy table, anchor the core rod in the base through the lower plunger, and drive the lower plunger up and down by a cam lever. Fix the upper punch to the press crosshead. Beside the die, pivot a filling shoe full of powder that can swing over the cavity and shake. Ours: a punch press.
Nauðsynleg verkfæri:
 Gatapressa
4
4
Fill, press and eject
Fill, press and eject
Start with the lower plunger right up, filling the cavity. Swing the shaking shoe over and lower the plunger: the powder falls in after it by gravity and suction, so no air is trapped. Take the plunger below the pressing position, then raise it to the pressing position, pushing the surplus back into the shoe so every charge is the same. Swing the shoe away, bring down the upper punch to press the ring between the punches, lift the punch and raise the lower plunger to push the ring out flush with the die top; the returning shoe sweeps it aside. Sinter the rings afterwards.
Nauðsynleg verkfæri:
GatapressaEfni
2- 1 die, core rod, punchesStaðgengill
- 1 lock nutStaðgengill
Nauðsynleg verkfæri
7- Staðgengill
- Staðgengill
- Staðgengill
- Staðgengill
- Staðgengill
- Staðgengill
- Staðgengill
Efni úr tengdum teikningum


Þessi teikning býr til
CC0 opinbert ríki
Þessi teikning er gefin út undir CC0. Þér er frjálst að afrita, breyta, dreifa og nota þetta verk í hvaða tilgangi sem er, án þess að biðja um leyfi.
Studdu smiðinn með því að kaupa vörur í gegnum teikningu hans þar sem hann fær þóknun smiða sem seljendur ákvarða, eða búðu til nýja endurskoðun á þessari teikningu og tengdu hana sem tengingu í þinni eigin teikningu til að deila tekjum.